
Blister Line Capability FAQ: Servo, Splicing, Tooling
Blister Line Capability FAQ: Servo, Splicing, Tooling
A pharmaceutical packaging machine is judged less by the number printed on its specification sheet than by what happens between scheduled stops. In solid-dosage projects, the questions that decide a blister-cartoning line converge on four areas: how the servo axes are controlled, how forming and lidding material is replenished while the machine is running, how tooling is changed and remembered, and what the buyer is contractually entitled to verify before the balance is paid. This FAQ works through those four areas using verified specification detail from Zhejiang Hoping Machinery Co., Ltd. (HOPING) and the DHL8005H automatic blister-cartoning line as a worked example.
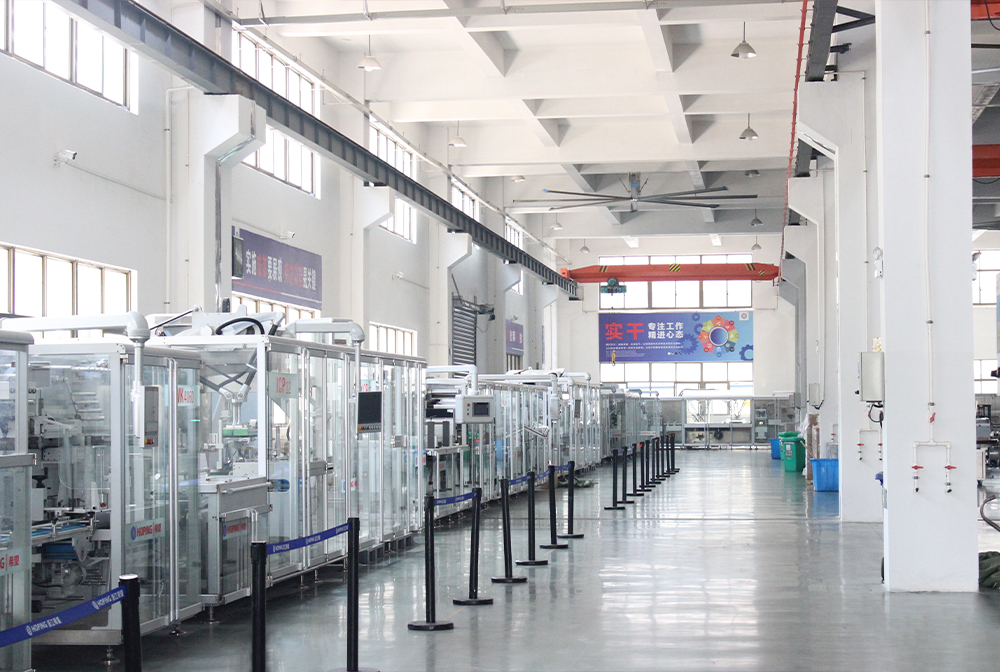
Blister-cartoning configurations are selected against format range, replenishment strategy and acceptance protocol, not headline speed alone.
Why these four questions decide a blister-cartoning evaluation
A blister-cartoning line loses output through two different kinds of stop. Scheduled stops are known in advance: roll changes, format changes, cleaning and inspection routines. Unscheduled stops are the ones that damage a batch plan, and they usually trace back to material handling, a tooling fit, or a control response the buyer never examined because the quotation only listed speed.
That is why the useful evaluation questions are structural rather than promotional. Does the machine control its own motion on an industrial platform that can also hold recipes and pass data onward? Is material replenishment built as independent servo channels or as one mechanically linked drive? Does the line splice PVC and aluminium foil automatically, and what happens to the blisters formed across a splice? Which parts touch the product, and against which standard are they accepted? Each of these can be written into a technical agreement and tested at factory acceptance. None of them can be verified from a catalogue page.
Control architecture: what a Beckhoff motion controller and a CP9315 industrial PC actually change
The line's servo axes are coordinated by a Beckhoff motion controller, with a CP9315 industrial PC in the same control architecture. Stated plainly: motion control of the machine's servo axes and the computing layer that hosts the operator interface and parameter management are specified as one platform rather than as separate, loosely coupled systems.
What the specification states
Two components are named. The Beckhoff motion controller is the unit that executes coordinated motion for the servo-driven stations. The CP9315 industrial PC is the computing platform in the control cabinet. In PC-based control architectures of this type, the same platform typically carries the sequence program, the recipe or parameter store, and the interface through which the line exchanges data with a factory system. That is a general characteristic of PC-based control, not a performance claim about any particular format or output.
What to verify in the control scope
Four items belong in the technical agreement rather than in a conversation:
- Axis list and ownership. How many servo axes are controlled, and whether the blister section and the cartoner share one controller or run on two that must be synchronised. The answer decides who diagnoses a timing fault at 2 a.m.
- Recipe and parameter storage. How many product recipes can be held simultaneously, and whether a stored recipe restores every axis position or only the main sequence.
- Data interface. Which protocol the line exposes and what data it can pass upward — production counts, reject reasons, alarm history. HOPING lists data interface and interface language among the configurable items for its lines, which means the buyer should name the requirement instead of accepting a default.
- Language and access rights. Interface language and the operator/engineer access levels are configuration decisions that affect training and, later, audit trails.
A control platform is not a compliance certificate. Naming Beckhoff components establishes what hardware is in the cabinet; it does not by itself establish that the line's data handling meets any particular regulatory expectation. That separation should stay explicit through the whole evaluation.
Three-channel servo-driven independent replenishment: the uptime question
The line uses a three-channel, servo-driven independent replenishment system. The wording matters more than it first appears. Three channels means material is supplied through three separate paths. Servo-driven means each path is positioned by its own servo axis. Independent means those paths are not rigidly tied to a single common mechanical drive.
For a buyer, the practical consequence is diagnostic rather than decorative. When channels share one mechanical drive, a fault or a roll-end on one path propagates through the whole material feed, and the operator's first task is to find which path caused the stop. Independently driven channels give the control system a way to isolate a channel, which changes both the failure mode and the recovery procedure. It also changes the maintenance picture: a servo axis can be replaced or re-referenced on its own, while a shared drive cannot.
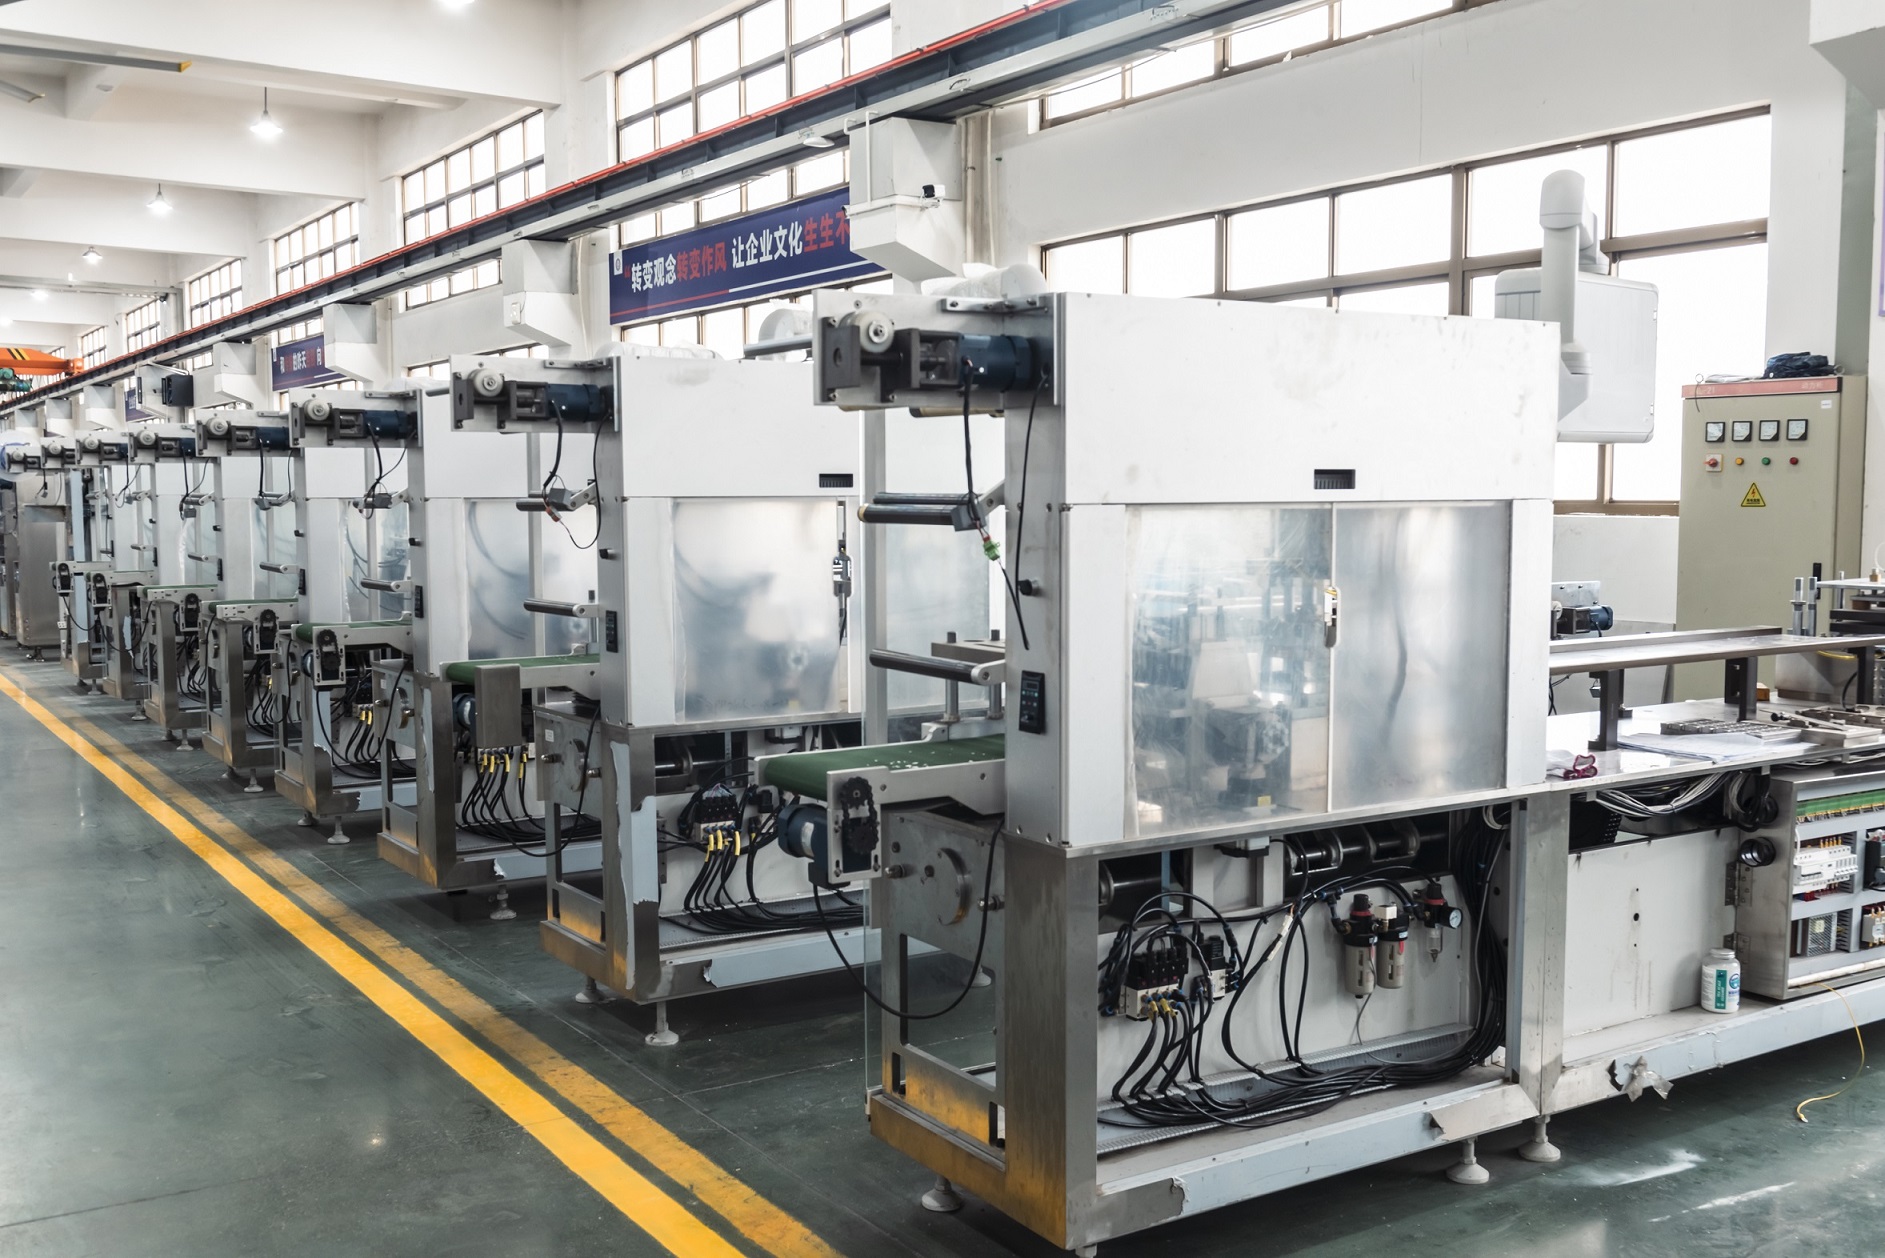
Servo-driven stations are assembled and run before factory acceptance, where axis behaviour and material feed can be observed under load.
What the specification does not say — and what a buyer should therefore put in writing — is what each channel carries on their specific format, and how a replenishment event on one channel affects output on the others. Those two answers determine whether "three-channel independent" translates into fewer stops on the buyer's actual product mix. The technical agreement is the right place to fix them, because the answer changes with blister layout, forming material and lidding material.
PVC and Alu foil auto splicing: what it removes from the shift, and what it does not
PVC and aluminium foil auto splicing lets the machine join a new roll to the expiring one and continue running instead of stopping for a roll change. The gain is straightforward in principle: a task that would otherwise be a scheduled stop becomes a non-stop event, and the operator's attention moves from threading to monitoring. In a multi-shift operation, that is the difference between a roll change appearing in the batch record as downtime and not appearing at all.
The gain is also bounded, and the boundary is where serious evaluations separate from casual ones. Auto splicing addresses roll changes. It does not address format changes, cleaning, tooling swaps or inspection routines. Nor does it remove the need to decide what happens to the blisters that are formed while the splice passes through the forming and sealing stations. Three questions belong in the technical agreement:
- At what speed is the splice performed? A splice demonstrated at reduced speed and a splice performed at the line's rated output are different engineering events.
- How is the splice detected, and what is the reject window? Whether the control system identifies the splice and rejects affected blisters automatically, or relies on the operator, determines the downstream inspection burden.
- Which materials and roll formats are covered? PVC and aluminium foil behave differently in tension and heat, and the roll diameter, core and splice consumables should be named rather than assumed.
None of those answers changes the value of the feature. They change whether the feature is verifiable on the buyer's own material, which is the only version of the feature that survives the first production campaign.
Tooling, GMP-oriented design and construction: the agreement, not the brochure
The machine is designed with GMP orientation, and product-contact parts and tooling meet GMP standards as fixed in the technical agreement. That final clause is the whole point. "Per technical agreement" means the standard is not established by the marketing description; it is established by the document the buyer signs. An evaluation that never names the standard has not evaluated anything.
Tooling and product-contact parts
The first task is a boundary task: list every part that can touch the product, the blister forming material or the lidding foil, and confirm that each is covered by the tooling and contact-part scope in the agreement. The second task is documentary: request the material identification and surface specification for those parts, so the acceptance file records what was actually installed rather than what was intended.
Mold change and preset memory
The line provides mold-change functions together with preset memory. In practice, preset memory is what converts a tooling change from a re-setup into a recall: the parameters associated with a previously qualified format are stored and restored, so the operator is confirming a saved state rather than rebuilding one by hand. The buyer-relevant questions follow directly. How many format parameter sets can be stored? Are the stored sets revision-controlled, so that a change to one format does not silently overwrite another? What is the documented changeover sequence and who is authorised to alter a saved set?
Construction materials
The line is built in stainless steel and aluminium alloy. Those two families cover the structure, guards and many of the machined elements, but the specification at this level of detail does not fix the grade of stainless used at each contact point. If the buyer's cleaning regime, product chemistry or internal standard requires a particular grade on product-contact surfaces, that requirement has to be written into the agreement explicitly. The same applies to surface finish and to the accessibility of surfaces for cleaning — a material choice supports cleanability, it does not by itself deliver it.
The DHL8005H as a worked example
The HOPING DHL8005H automatic blister-cartoning line is specified at up to 800 blisters per minute and up to 500 cartons per minute. It is a useful worked example precisely because the two figures are not directly comparable. They are reported in different units, and the relationship between them depends on how many blisters are packed into each carton for the format being run. A buyer who divides one number by the other without knowing the blister-per-carton count is not calculating line balance; they are guessing at it.
The correct use of the two figures is to treat them as two rated capacities that must be reconciled against the buyer's own carton configuration. Ask for the blister-per-carton assumption behind the quoted carton rate, then check whether that assumption matches the product being planned. If it does not, the carton figure needs to be restated for the actual format before it can support a capacity decision.
Both figures are also stated as maximums. A maximum is a screening number, not a production plan. The number that belongs in a business case is sustained output on the buyer's format, with the reject rate and the stop pattern included. That is exactly what a factory acceptance test is for, and it is why the acceptance clause deserves as much negotiation attention as the speed clause.
Where the configuration fits: application scenarios
A blister-cartoning line of this class is normally specified for tablets, capsules and other solid dosage forms, in three commercial situations: a new line build, a capacity expansion, or the replacement of an existing packaging line. The three situations produce different priorities. A new build can optimise the whole layout; an expansion usually has to match an existing carton format and an existing batch size; a replacement has to fit into a room and a validation history that already exist.
The representative project objectives recorded for this class of installation are about removing manual labour from the transfer between primary and secondary packaging: raising packaging automation, reducing manual transfer of blisters, tightening the blister-to-carton connection, reducing the risk of wrong insertion or a missing leaflet, and preparing the line to feed downstream automation. These are project objectives, not measured outcomes, and they should be read that way. What they do indicate is where the payback is normally sought — in the gap between the blister machine and the cartoner, not inside either machine.
That gap is also where configuration flexibility earns its place. HOPING lists the configurable scope for its lines as blister size, blister materials, quantity per carton, carton specification, leaflet format, coding and inspection method, feeding method, connection to downstream bundling, case packing or palletising, interface language, electrical component brand and data interface. A buyer with a defined multi-format future should treat several of those items as specification inputs rather than options to be settled later, because the cost of adding a downstream connection after installation is not the same as the cost of specifying it at order.

Changeover discipline and preset-memory handling are taught during commissioning; the acceptance file should record who was trained.
Purchasing terms and acceptance criteria to settle before order
The commercial framework is short enough to settle in one meeting, provided it is settled before the technical agreement is signed rather than after. The stated terms are as follows.
- Minimum order quantity: 1 set, or 1 complete line.
- Delivery terms: EXW Ruian/Wenzhou; FOB Ningbo or Shanghai; CIF or CFR destination port. Final terms are subject to the contract and to the customer's country requirements.
- Payment terms: subject to quotation, contract value, customer credit, project scope, destination market and the final project agreement.
- Lead time: typically 60 to 120 days after technical confirmation, with the final figure subject to model, configuration, project complexity and contract terms.
- Quality sequence: incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, factory acceptance test, customer witness acceptance and pre-shipment inspection.
- After-sales scope: on-site installation and commissioning, operator training, maintenance training, remote video and phone support, spare parts supply, process-parameter guidance, regular follow-up and troubleshooting, all subject to the contract and project configuration.
The acceptance clause is the part most often written too loosely. The stated sequence is technical agreement confirmation, sample testing, factory acceptance before shipment, site acceptance at the customer's plant, with third-party inspection arrangeable on request. Each of those steps needs a pass criterion, or it becomes a ceremony. Sample testing needs a named format and a named material. Factory acceptance needs a defined run length and a reject-rate threshold. Site acceptance needs the utility conditions and the trained operators who will run the test.
What belongs in the agreement
| Agreement item | State precisely | Why it changes the outcome |
|---|---|---|
| Control scope | Axis count; one controller or two; recipe capacity; data protocol | Determines fault diagnosis and whether recipes survive a version change |
| Replenishment channels | What each of the three channels carries on the buyer's format | Decides whether an independent channel actually isolates a stop |
| Splicing performance | Splice speed; detection method; reject window; materials covered | Converts a claimed non-stop into a testable event |
| Tooling and contact parts | Standard to be met; part list; material grades; surface finish | "Per agreement" is meaningless until the standard is named |
| Preset memory | Number of stored formats; revision control; edit authorisation | Decides whether changeover is a recall or a rebuild |
| Output basis | Format, blister-per-carton count, run length, reject threshold | Makes 800 blisters/min and 500 cartons/min comparable to the buyer's plan |
| Acceptance | FAT and SAT pass criteria; third-party inspection; witness rights | Turns a sequence of steps into an enforceable release condition |
| Documents | Certificates valid on the contract date; material records; manuals | Populates the qualification file before the line is installed |
Comparing two lines that quote similar output
When two suppliers quote the same speed, the speed has stopped being a differentiator and the comparison moves to the items that surround it. The documented comparison dimensions that actually separate lines at this level are: number of controlled servo axes, number of independent replenishment channels, whether PVC and aluminium foil splicing is automatic, the standard fixed for product-contact tooling, the number of stored format parameters, and the acceptance protocol each supplier is willing to sign.
There is a fit boundary worth stating plainly. A line dedicated to one format at high volume, with few changeovers and long campaigns, gains relatively little from an elaborate preset-memory library and from a splicing strategy that only matters at roll changes; for that buyer, sustained output and recovery time after a fault dominate. A line serving many formats in short batches inverts the weighting: changeover time, stored parameter integrity and the repeatability of a recalled setup become the deciding criteria, and a fast single-format machine can be the wrong purchase. Servo architecture is an enabler in both cases, but it is not an automatic advantage — it is an advantage where changeover frequency and format count make it one.
Industry context: what is documented and what is not
Two externally documented points are worth keeping in view during evaluation. ISO 15378:2017 specifies Good Manufacturing Practice requirements for primary packaging materials for medicinal products — it is a standard about packaging materials and the systems that produce them, and it should not be cited as a machine-design certification. Separately, commercial research published by Mordor Intelligence reports that horizontal cartoning systems held 70.12% of the cartoning market in 2024, which is consistent with the horizontal orientation used across pharmaceutical secondary packaging but does not, on its own, establish suitability for any specific product.
Trade media reporting association (PMMI) content also describes pharmaceutical manufacturers moving toward digitised data collection and integrated solutions in order to meet regulations and improve visibility. That is a directional signal rather than a measurement, and it should be treated as one. Its practical implication for a buyer is modest but real: if data capture is likely to be specified later, the data interface and interface language are better named at order than retrofitted.
On certification evidence specifically, the documents supplied for this review include CE certificates covering blister packing machine series and cartoning machine series, with issue dates between 2006 and 2019, and ISO 14001:2015 and ISO 45001:2018 management-system certificates issued in October 2023 with recorded validity to October 2026. Because certificates carry fixed validity windows and fixed scopes, the acceptance file should hold the certificate version valid on the contract date and the version whose scope covers the exact model ordered — not the version printed in a brochure.
Outlook
The direction of travel in solid-dosage packaging is toward lines that are specified as one controlled process rather than as a sequence of separately purchased machines. Control platforms that hold recipes, splicing that removes a class of scheduled stop, and preset memory that makes a format change a recall instead of a rebuild all serve the same objective: fewer decisions left to the operator in the middle of a shift. Buyers who write those behaviours into an agreement, with pass criteria attached, will get more of them than buyers who compare catalogue speeds. The remaining constraint is not technical ambition but documentation discipline — the standard, the material, the splice speed and the acceptance threshold only exist once they are written down.
FAQ
Which control platform does a servo blister-cartoning line use, and why does it matter to a buyer?
The HOPING line specification names a Beckhoff motion controller for coordinating the servo axes, together with a CP9315 industrial PC in the same control architecture. It matters because the control platform determines how recipes are stored, how faults are reported and which data the line can pass to a factory system. The buyer's verification items are the axis count, whether the blister section and cartoner share one controller, the number of storable recipes and the exposed data protocol.
How does a three-channel servo-driven independent replenishment system affect uptime?
It supplies material through three separately driven channels rather than one mechanically linked feed. Because each channel has its own servo axis, a fault or roll-end on one path does not propagate mechanically through the others, which changes the failure mode and shortens the diagnostic step. The specification does not state what each channel carries on a given format, so that detail — and the effect of a replenishment event on output — should be fixed in the technical agreement.
Does PVC and Alu foil auto splicing remove all roll-change downtime?
No. Auto splicing addresses roll changes by joining a new roll to the expiring one so the machine continues running. It does not address format changes, cleaning, tooling swaps or inspection routines, and it does not by itself decide what happens to blisters formed while the splice passes through the forming and sealing stations. The splice speed, the detection method, the reject window and the materials covered are the four items that determine whether the feature is verifiable on a buyer's own material.
Which tooling and construction details belong in a GMP-oriented technical agreement?
The design is GMP-oriented, and product-contact parts and tooling meet GMP standards as fixed in the technical agreement, so the agreement must name the standard rather than refer to it generally. It should also list every part that can touch the product, blister material or lidding foil, with material identification and surface specification. The line is built in stainless steel and aluminium alloy; because the grade used at each contact point is not fixed at that level of description, any grade required by the buyer's cleaning regime or internal standard should be written in explicitly, together with the number of stored format parameters and the changeover procedure.
What purchasing terms and acceptance criteria should be settled before order?
The minimum order quantity is 1 set or 1 complete line. Delivery terms are EXW Ruian/Wenzhou, FOB Ningbo or Shanghai, or CIF/CFR destination port, with final terms subject to contract and customer country requirements. Lead time is typically 60 to 120 days after technical confirmation, subject to model, configuration, project complexity and contract terms. Acceptance follows technical agreement confirmation, sample testing, factory acceptance before shipment and site acceptance at the customer's plant, with third-party inspection arrangeable on request. Payment terms are subject to quotation, contract value, customer credit, project scope, destination market and the final project agreement.
The full HOPING product range, including blister packaging machines, cartoning machines, case packers and end-of-line equipment, is documented in the Hoping Machinery catalog. Company information is available at hopingcn.com.
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.