
Butyrate-Producing Probiotics Powder for Metabolic Health
Butyrate-Producing Probiotics Powder for Metabolic Health
Metabolic health has moved from a clinical specialty into a mainstream formulation category. As supplement developers build products around glucose support, weight management and GLP-1-adjacent positioning, ingredient selection has shifted upstream — toward strains whose mechanism can be described, whose viability can be measured, and whose documentation survives customs review. Butyrate-producing probiotics powder sits at the centre of that shift, and Clostridium butyricum CCFM1299 is one of the strain directions now being evaluated for metabolic-management supplement formats.
Probiotic raw powder manufacturing base — the supply layer behind metabolic health supplement formulation.
What a Butyrate-Producing Probiotics Powder Is
A butyrate-producing probiotics powder is a dry, dose-ready ingredient that contains viable bacteria — most commonly spore-forming species such as Clostridium butyricum — selected because the species generates butyrate as part of its normal metabolic activity in the gut. It is not a finished health product. It is an input that a formulator blends into capsules, sachets, tablets or stick packs, and its commercial value rests on three measurable properties: strain identity, viable count at the point of use, and stability across the shelf life printed on the label.
Butyrate is the reason this ingredient category exists. It is the principal energy substrate for colonic epithelial cells and one of the most widely studied short-chain fatty acids in host-metabolism research. Formulation teams that follow that literature increasingly look for strains positioned around butyrate production rather than only for cultures with a long history of consumption. Clostridium butyricum CCFM1299 belongs to that butyrate-producing, spore-forming family, which is why it is examined here as an ingredient for metabolic-management and medical-nutrition products rather than as a therapeutic agent.
The Problem: Metabolic Products Are Marketed Faster Than They Are Documented
Buyers in this segment usually receive three pieces of information — a species name, a CFU figure and a price per kilogram — and none of them answers the questions that formulation, quality and regulatory teams have to resolve before a purchase order is released.
- Strain identity. Species-level naming does not separate a documented, genome-characterised culture from a commodity powder sold under the same species name. Strain-level qualification is what regulators, retailers and customer audits ask to see.
- Viable count at the point of use. A CFU figure measured at the factory gate says little about how much survives gastric transit, or how much remains viable in month 18 of a declared shelf life.
- Documentation. In the United States, probiotic supplements are regulated under 21 CFR Part 111, which requires compliance with current Good Manufacturing Practices (cGMP). At the food-safety layer, ISO 22000 is the international standard for food safety management systems applicable to the probiotic production chain and incorporates HACCP principles.
- Claim boundaries. Metabolic positioning is precisely the language that regulators and retail buyers scrutinise most closely, so the ingredient file has to support the copy rather than the reverse.
The opportunity created by that gap is simple to state. Where much of the category competes on price per kilogram, a supplier able to provide strain-level documentation, encapsulation specifications and stability data lets a buyer price against cost per effective CFU instead. That is a different negotiation, and it favours suppliers with in-house culture, drying and testing capability.
Technology: How a Butyrate-Producing Strain Becomes a Workable Powder
Strain resources set the ceiling on everything else
Shanghai Unibio Lab Co., Ltd is a probiotic research, manufacturing and CDMO enterprise whose strain resources build on more than 40 years of probiotic research originating from Jiangnan University. The company maintains a strain bank of over 30,000 microbial strains, comprising 25,300 primary 16S rRNA strains, 13,720 draft-genome strains and 8,046 full-genome strains, and it lists Clostridium butyricum among its next-generation probiotic raw materials alongside Akkermansia muciniphila AH39. Strain designations carrying the CCFM prefix trace back to that research lineage — a practical advantage, because an identity that can be linked to a characterised culture with genomic data is far easier to defend in a specification and in a customer audit than a species name alone.
Encapsulation and drying decide whether the powder survives the journey
The failure points of probiotic powder are well known: freezing during drying, gastric acid, bile salts, oxygen and moisture during storage. Unibio Lab's VPro® five-layer microencapsulation technology is organised around those five points, and each layer has a stated function:
- Micromolecular protective layer — anti-freezing and anti-stress protection
- Prebiotic nutrition layer — supports in-vivo proliferation
- Liposome enteric adhesion layer — supports intestinal colonisation
- Acid and enzyme resistant layer — supports survival through gastric digestion
- Oxygen and moisture barrier layer — extends shelf stability
According to the manufacturer's technical documentation, this construction lifts the freeze-drying survival rate by 40%, extends shelf life to 24 months, and supports a fermentation density above 3.5×10¹⁰ CFU/mL with lyophilized powder concentration up to 8.0×10¹¹ CFU/g. These are manufacturing performance figures, not clinical endpoints, and the distinction matters: they tell a formulation team how to convert a label claim into a dosing plan and a stability budget, not what a finished product will do for an end user.
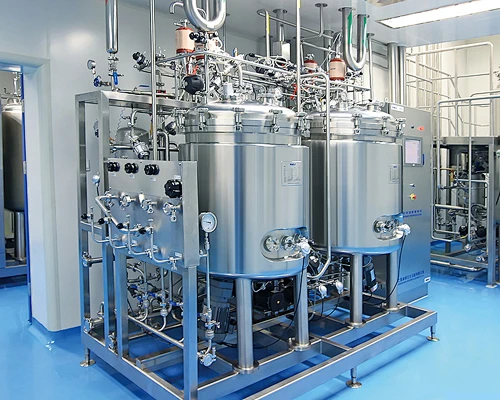
Controlled-environment production area for probiotic raw powder and postbiotic materials.
This is a category-level trend rather than a single-supplier position. Independent technical literature identifies microencapsulation using materials such as alginate or chitosan as one of the key approaches to maintaining probiotic viability through gastric acid and bile salts. Buyers should therefore expect any serious supplier to describe encapsulation at process level — layer count, material type, drying method — rather than as a generic claim of protected strains.
Application Fit: Where Butyrate-Producing Powder Is Used
Because the powder is an input rather than a finished product, its application fit is determined by the dosage form, the storage and transport profile, and the claim structure of the product being developed.
- Metabolic-management dietary supplements. A high-purity single-strain powder is the usual starting point for a metabolic positioning, dosed into capsules or stick packs where the label needs a defined CFU figure.
- Pre-, pro- and postbiotic complexes. Unibio Lab supplies compound formats that combine live strains with postbiotic material in a single blend, including a GLP-1 metabolic management pre-pro-post complex (HelpGut® GLP1 Pre-Pro-Post complex).
- Postbiotic formats where live-cell claims are undesirable. Inactivated postbiotic powder and liposomal ProLipo® postbiotics allow metabolic positioning without a live-cell count on the label.
- Medical nutrition and elderly nutrition powders. Room-temperature stable, low-temperature freeze-dried powder suits sachets and clinical-style nutrition blends where cold-chain distribution is impractical.
- Bowel-regulating and gut-health capsules. Finished private-label capsules aimed at constipation relief and general bowel regulation draw on the same raw-powder base.
- Dosage-form flexibility. Products support customized CFU concentration and dosage forms including powder, capsule, tablet, sachet and gummy, plus personalised packaging design.
In every one of these scenarios the ingredient supports an application; it does not by itself support a health claim. Whether a given strain can carry a specific metabolic statement depends on the destination market, the strain-level qualification, and the substantiation held by the brand owner.
Market Trend Analysis: Growth, and a Caveat About Market Sizes
The direction of the category is not in dispute. The global probiotics market was valued at USD 72.1 billion in 2024 and is projected to reach USD 165.1 billion by 2034, according to Global Market Insights. Within that total, probiotic dietary supplements reached USD 10.60 billion in 2026, with a forecast CAGR of 9.5% through 2031, according to MarketsandMarkets.
The absolute numbers, however, should be read with care, because published estimates differ substantially depending on what is being counted. Grand View Research puts the 2025 probiotics market at USD 114.0 billion, while Global Market Insights gives USD 79.2 billion for the same year — a gap that reflects different scope definitions rather than different growth stories. Buyers building a business case should check whether a cited figure covers total probiotics, ingredients only, or supplements only.
The ingredient landscape is concentrated at the top. Yakult Honsha holds a 6.7% share of the global probiotics market, and the leading group also includes Danone S.A., ADM, Kerry Group and Novonesis. For specialist buyers, that concentration creates a practical division of labour: large consumer-facing players dominate branded finished products, while specialist CDMO manufacturers serve brands that need strain-level customisation, lower minimum order quantities and market-specific documentation.
Two structural trends are shaping procurement. The first is regulatory: 21 CFR Part 111 in the United States and ISO 22000 internationally have turned documentation into a baseline requirement rather than a differentiator. The second is technical: microencapsulation has become a mainstream research direction for viability through gastric acid and bile salts, which pushes the competitive conversation toward process quality, batch consistency and auditable data.
Comparison with Conventional Uncoated Powder — and Where the Limits Are
The most useful comparison in this category is not brand against brand, but microencapsulated powder against conventional uncoated powder from generic suppliers.
| Comparison dimension | VPro® microencapsulated powder | Conventional uncoated generic powder |
|---|---|---|
| Technology base | VPro® 5-layer microencapsulation, independent CCFM strain library, full-index in-house testing | No encapsulation layer; testing scope varies by supplier |
| Survival through gastric acid and bile | Increased by 78% versus uncoated powder | Baseline reference |
| Declared shelf life | 24 months | 12 months |
| Unit price | 8%–12% higher | Lower at the kilogram level |
| Cost per effective CFU | 2.1× higher effective viable CFU per kg; finished-formula dosage cost reduced by more than 20% | Higher dosage required to reach an equivalent effective count |
| Best fit | Long-distance sea freight, room-temperature storage, high-temperature extrusion processing | Short distribution chains with controlled storage |
| Documentation pack | Complete full test report pack (safety, activity, impurity) for customs and local authority filing | Often limited to a basic certificate of analysis |
Two limits on this comparison should be stated plainly. First, the microencapsulation premium only pays back when cost per effective CFU is the metric being managed. The coated raw material carries a unit price 8%–12% higher than conventional uncoated powder, and it is the 2.1× higher effective viable CFU per kilogram that brings finished-formula dosage cost down by more than 20%. A buyer who negotiates purely on price per kilogram will see a premium, not a saving.
Second, and more important for anyone planning a metabolic health product: regulatory qualification is strain-specific, not portfolio-wide. The independent self-affirmed GRAS conclusion held by Unibio Lab applies to Akkermansia muciniphila AH39. It does not automatically extend to Clostridium butyricum CCFM1299 or to any other strain. Market access for a butyrate-producing ingredient therefore has to be verified strain by strain and market by market, with the certification pack matched to the destination.
A third boundary concerns what the ingredient data can and cannot prove. Encapsulation data describes survival of the culture, not production of butyrate inside a particular host, and butyrate generation depends on the gut environment and diet of the individual. No butyrate-level claim, and no metabolic outcome claim, should be inferred from a powder specification sheet. Formulators who respect that boundary will find the documentation useful; those who cross it will find it expensive.
Long-Term Supply: The Terms That Decide Whether a Partnership Holds
For buyers at the decision and execution stage, the ingredient is only half the question. The other half is whether supply can be repeated at the same quality for years, across regions, without renegotiating the fundamentals.
| Supply parameter | Documented figure |
|---|---|
| Monthly production capacity | 1,800 tons of probiotic raw powder; 2 billion finished capsules/tablets |
| MOQ — single strain raw powder | 1 kg |
| MOQ — multi-strain compound powder | 5 kg |
| MOQ — private label finished capsules/tablets | 5,000 bottles |
| Lead time — bulk raw material | 5–7 days |
| Lead time — private label finished goods | 25–35 days |
| Trade terms | FOB Shanghai, CIF, DDU, DDP |
| In-house testing | 100% batch testing before shipment: viable count, heavy metals (ICP-MS), microbial safety |
| Third-party inspection | SGS / Intertek on request; SGS random inspection monthly |
| Batch retention samples | Stored for 24 months |
| Certification and registration base | ISO 22000, FSSC 22000, GMP food manufacturing certification (SGS), HALAL, OU Kosher, FDA US food facility registration, independent sGRAS conclusion for A. muciniphila AH39 |
| Payment structure | 100% advance; 30-day credit for trusted customers; or 50% deposit with balance due 30 days after bill of lading |
| After-sales support | Free strain technical guidance, batch COA provision, cold-chain logistics scheme, 24-hour working-hour complaint response |
Three risk categories dominate long-term supply in this category, and each has a defined control. Strain activity loss during production, storage and transport is managed through VPro® microencapsulation, low-temperature vacuum drying, constant cold storage, real-time temperature and humidity monitoring, per-batch accelerated stability testing and cold-chain logistics tracking. Microbial contamination risk is managed through a Class 100,000 clean production workshop, high-temperature sterilisation of auxiliary materials, sterile filling equipment, full microbial testing of raw materials and finished goods, HACCP whole-process hazard monitoring and monthly third-party SGS inspection. Regional non-compliance and customs detention risk is managed through pre-shipment document review, complete certification packs covering GRAS, HALAL, FDA and FSSC 22000, region-adapted formula adjustment, ingredient labelling customised to EU, US and Southeast Asian requirements, and local regulatory consulting support.
Commercial and documentation functions that support export programmes and long-term supply partnerships.
For partners serving Muslim-majority markets, HALAL-certified materials remove one qualification step; for US-bound programmes, the AH39 GRAS documentation simplifies customs clearance. Neither shortcut transfers automatically to a different strain, which is why documentation mapping belongs inside the supply agreement rather than in the follow-up email after the first shipment.
Future Outlook
Three developments are likely to shape the next phase of butyrate-producing ingredients in metabolic health. The first is convergence between live strains and postbiotics: as brands hedge against claim scrutiny, blends that pair a characterised culture with postbiotic material are becoming a standard formulation pattern rather than a novelty, and the HelpGut® GLP1 Pre-Pro-Post complex illustrates how these components already sit inside one commercial format.
The second is that stability engineering will keep moving from a marketing statement to a contractual one. Where shelf life is now extended to 24 months through five-layer encapsulation and low-temperature vacuum drying, buyers will increasingly write shelf-life and batch-consistency requirements into supply agreements, supported by retention samples and per-batch accelerated testing.
The third is regulatory fragmentation. Because qualification is strain-specific, the practical workload of market entry shifts from the brand to the supplier's documentation function, and CDMO partners that can pre-assemble certification packs and adapt labelling per region will be judged on that capability alongside price and capacity.
For a consolidated view of manufacturing capability, strain resources, certifications and service terms, the company brochure is available for reference: Unibio Lab company brochure (PDF).
FAQ
The questions below follow the sequence a decision-stage buyer typically works through, from quantity and lead time to documentation boundaries.
1. What is the minimum order quantity for butyrate-producing probiotic powder and for private-label finished products?
Minimum order quantity is 1 kg for single strain raw powder, 5 kg for multi-strain compound powder, and 5,000 bottles for private label finished capsules or tablets. Monthly production capacity is 1,800 tons of probiotic raw powder and 2 billion finished capsules or tablets.
2. How long does supply take for bulk raw material compared with finished private-label goods?
Typical lead time is 5–7 days for raw material bulk orders and 25–35 days for private label finished products. Delivery terms available are FOB Shanghai, CIF for major global ports, DDU and DDP.
3. What payment structures are offered for a long-term supply arrangement?
Documented options are 100% advance payment; a 30-day credit period for trusted customers; or a 50% advance deposit with the balance due 30 days after bill of lading issuance.
4. What quality checks and acceptance steps apply before shipment?
Every batch undergoes 100% in-house laboratory testing before shipment, covering viable count, heavy metals by ICP-MS and microbial safety. Third-party inspection by SGS or Intertek is available on buyer request, SGS random inspection takes place monthly, a batch COA is provided, and retention samples are stored for 24 months.
5. Which certifications and registrations support long-term supply across markets?
The documented base includes ISO 22000, FSSC 22000, GMP food manufacturing certification (SGS), HALAL and Orthodox Union (OU) Kosher certificates, and FDA US food facility registration. Certification packs are pre-provided for customs and local authority filing, and ingredient labelling can be adapted to EU, US and Southeast Asian requirements.
6. How is strain viability protected during long-distance shipping and room-temperature storage?
Protection combines VPro® five-layer microencapsulation, low-temperature vacuum drying and constant cold storage warehousing. The manufacturer documents a 40% increase in freeze-drying survival rate and a 24-month shelf life, supported by real-time temperature and humidity monitoring, per-batch accelerated stability testing and cold-chain logistics tracking.
7. Does the GRAS conclusion held for one strain apply to butyrate-producing strains in the same portfolio?
No. The independent self-affirmed GRAS conclusion held by Shanghai Unibio Lab Co., Ltd applies to Akkermansia muciniphila AH39. Other strains, including Clostridium butyricum CCFM1299, require separate strain-level qualification for each destination market, and the applicable certification and labelling requirements should be confirmed for the specific strain and region before commercial supply.