
CNC Machining Repeat Orders: Pricing, Delivery, Tolerance
A CNC machining program is not decided by its first article. It is decided by the twenty-fourth delivery — same drawing, same tolerance band, same price basis, same promised date. Buyers who have already chosen a supplier and are moving into execution are therefore not buying a machining capability. They are buying a production system that must repeat.
That distinction matters because the CNC sector is large and fragmented. Grand View Research values the global CNC machining and turning centers market at USD 31.3 billion in 2026, and IBISWorld puts the U.S. machine shop services market at USD 46.3 billion across roughly 16,400 active businesses. Almost any buyer can find a supplier able to cut one good part. The harder question is whether that supplier can hold the same dimensional result and the same commercial terms across a year of monthly releases.
This reference sets out how to evaluate a CNC machining supplier specifically for long-term repeat production: the evidence to request on tolerance consistency, the parts of a price that should stay stable, and the delivery and capacity facts that determine whether a monthly schedule is realistic.
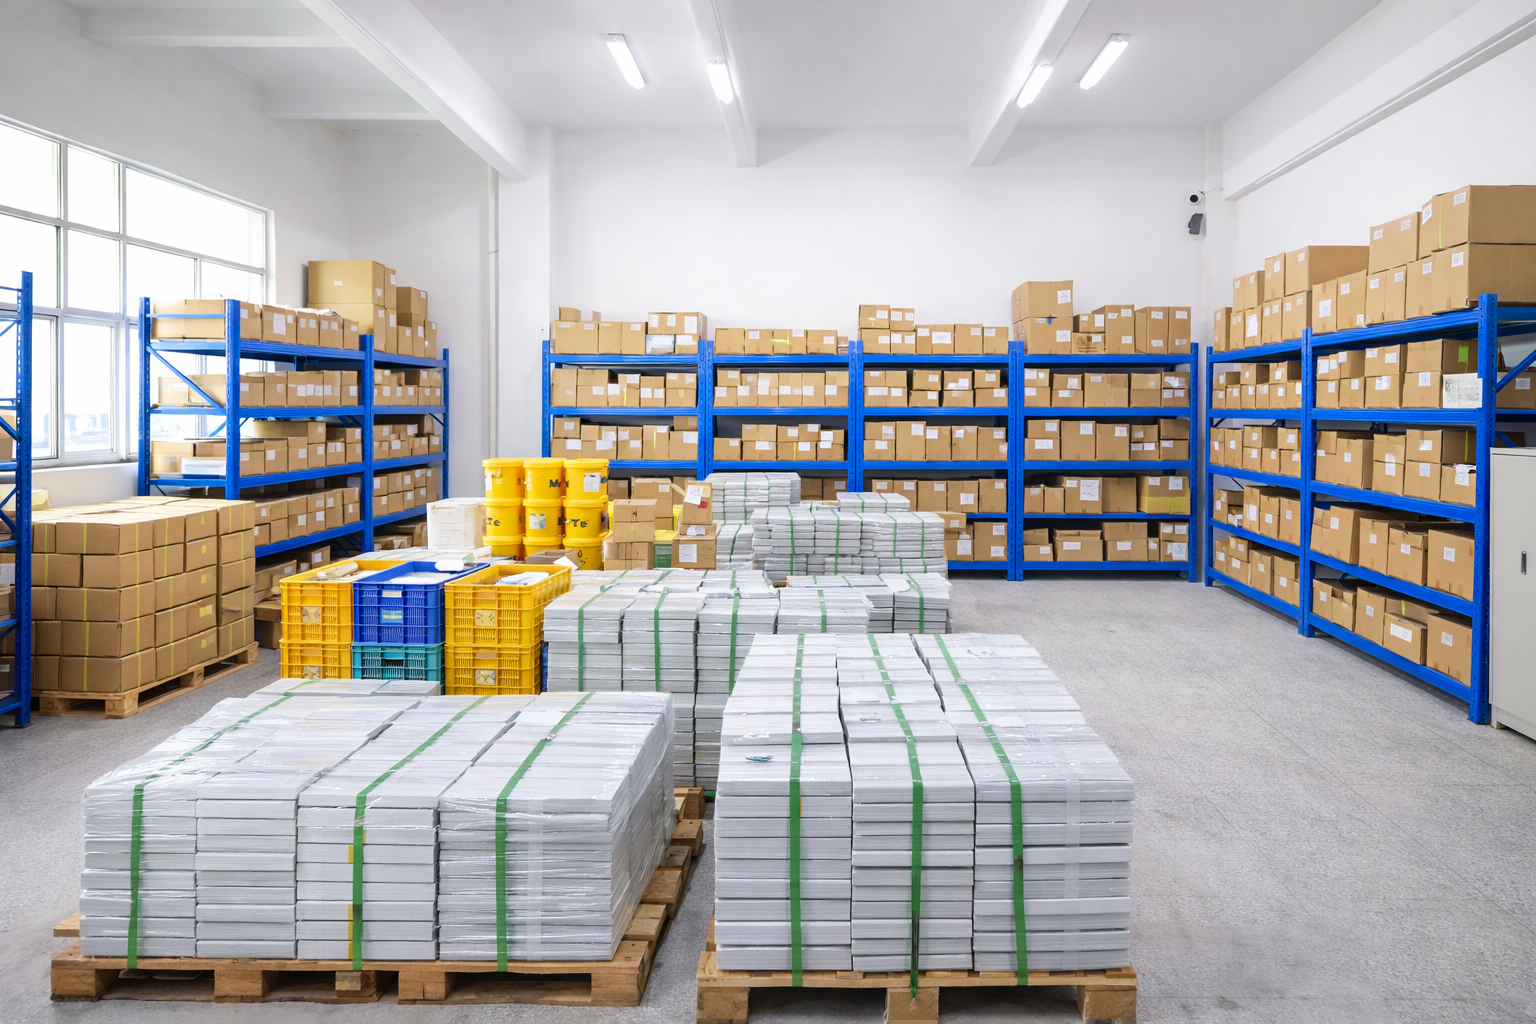
Repeat-order supply depends less on machining capability alone than on staging, documentation and dispatch discipline that lets every monthly release look like the one before it.
Why repeat orders, not prototypes, expose supplier quality
Prototype performance is a weak predictor of long-run performance, because a prototype is usually produced under favourable conditions: the most capable machine, a senior setter, generous time, and a quality team watching closely. A repeat order has none of those advantages. It runs on a schedule, across shifts, with the same operators and the same programming standards as every other job in the shop.
Four failure modes account for most repeat-order breakdowns:
- Process drift. The trial batch and the volume batch are not built from the same process file, so tool wear, fixturing and feeds-and-speeds assumptions diverge.
- Price creep. A quotation built around an assumed annual volume does not survive an order pattern that arrives in smaller, irregular releases.
- Capacity substitution. A supplier that accepts a long-term programme without the machine hours to support it will eventually sub-contract, and the buyer discovers this through dimensional variation rather than through disclosure.
- Documentation gaps. Without per-batch records, a buyer cannot demonstrate to its own customer that batch 14 was produced and verified the same way as batch 1.
The buyer-side consequence is straightforward: evaluation criteria that were appropriate for supplier discovery or prototype validation are insufficient for execution. The questions change from what can you make to what can you keep making.
What a long-term CNC machining partner has to prove
Independent of any single supplier, a repeat-order evaluation should rest on five verifiable evidence blocks. Each can be checked from documents rather than from assurances.
- Tolerance consistency evidence. First-article inspection for every new batch, in-process monitoring, and final inspection with named instruments — plus a stated method for tight-tolerance features.
- Inspection ownership. Whether metrology is performed in-house or outsourced, and which equipment is actually on site.
- Quality management scope. An ISO 9001 certificate is only meaningful once the certified entity, site and scope statement are matched against the processes the buyer is purchasing.
- Stated capacity. A monthly figure that can be compared with the buyer's forecast, rather than a qualitative claim of large capacity.
- Commercial basis. What the unit price is conditional on, and which inputs would legitimately reset it.
Companies that can answer all five with documents tend to be the ones whose repeat orders hold. Companies that answer with adjectives tend not to.
SUNPREC CNC Machining: the repeat-order capability set
SUNPREC CNC Machining is the machining service line of SUNPREC HARDWARE CO., LTD, a one-stop metal parts manufacturer founded in 2020 and located in Dongguan City, China. The company operates a 3,500 m² factory with 200 employees, including a 10-engineer team, exports approximately 90% of its output to EU and USA markets, and reports cooperation with more than 300 clients across more than 50 countries. Its production scope covers CNC machining, die casting, extrusion and surface finishing.
For buyers whose decision is about sustaining a programme rather than starting one, the relevant facts are these:
- Stated monthly production capacity of 4,200,000 units — a figure that can be modelled directly against a monthly forecast instead of interpreted.
- Minimum order quantity of 10 units for low-volume and small-batch custom orders, which allows a buyer to run a genuine trial release before committing a full schedule.
- FANUC machining centres with a machine tolerance of 0.005 mm, with 3-axis, 4-axis and 5-axis capability for complex geometry and tight-tolerance components.
- In-house metrology including a HEXAGON CMM, 2.5D optical comparators and TRIMOS high-precision height gauges, alongside calipers, micrometers and surface roughness testers.
- Prototype turnaround in 3–5 days with urgent order support, which shortens the gap between validation and the first repeat release.
- After-sales quality assurance and customer technical support, including technical support for repeat and ongoing production orders.
Material coverage spans aluminium, stainless steel, carbon steel, brass, copper, titanium, POM, ABS, nylon and PEEK, with one-stop surface finishing that includes anodizing, hard anodizing, powder coating and sandblasting. For a repeat programme, that breadth matters less as a selling point than as a risk reduction: the fewer processes that leave the supplier's control, the fewer handoffs at which a dimensional or cosmetic result can shift.
How tolerance consistency survives the jump from trial to volume
Three different numbers are routinely confused in supplier conversations, and separating them is the first step in a credible tolerance review.
Machine tolerance describes the equipment. SUNPREC's FANUC centres are specified at a machine tolerance of 0.005 mm. Process capability describes what the shop can hold once fixturing, tooling, material behaviour and inspection method are included; SUNPREC states part tolerance capability of up to ±0.005 mm for suitable work. Part tolerance describes what a specific drawing will actually achieve, and it depends on geometry, wall thickness, material and datum strategy. A buyer who treats the machine figure as a guaranteed part figure will be disappointed by any supplier, not just this one.
What can be verified is the mechanism used to keep the result stable between batches:
- First-article inspection on every new batch. Not only on the first order — every new production batch is first-article inspected, which is the control that catches drift before it becomes a shipment.
- Incoming, in-process and final inspection. SUNPREC's quality control runs incoming material screening at receiving, continuous quality monitoring during production, and final testing before shipment, with final inspection using calipers, micrometers, height gauge and surface roughness tester.
- CMM verification for critical features. Tight-tolerance and critical components are verified on a CMM coordinate-measuring machine rather than by hand tools alone.
- Automated programming discipline. The company combines high-precision machining hardware with intelligent automated programming to reduce human-induced dimensional deviation, which is the practical answer to the most common cause of batch-to-batch variation.
- Traceability records. Standardized process files and unified inspection record management capture processing parameters and test data, so production and inspection records remain traceable for all orders.
The documentary outputs that support this are an FAI report, material certificate, COC and dimensional inspection report — the four documents a buyer's own customer is most likely to request during an audit.
Pricing: what should stay fixed, and what legitimately moves
Price stability in a repeat programme is not the same as a price lock. It is an agreement about which inputs are held constant and which ones reset the quotation. For CNC machining, SUNPREC states that quotation depends on part complexity, material, process and order quantity, with precise quotes supported by detailed drawings. That is a clear, honest basis — and it tells the buyer exactly where to anchor the negotiation.
Four inputs should be held constant across monthly releases:
- Drawing revision. Any revision, however small, is a new quotation event. Freeze the revision at programme start and control changes formally.
- Material grade and specification. Substituting an equivalent grade changes machinability and therefore cycle time and tool consumption.
- Process route. Adding or removing a finishing step, a secondary operation or an inspection stage changes cost structure.
- Release pattern. A programme forecast at 5,000 units per month but released as four irregular batches carries different setup economics from a smooth monthly release.
On scale economics, SUNPREC reports that mass-order unit cost is 10%–15% lower than scattered small workshops. Buyers should read that statement for what it is: a comparison of order structures, not a guaranteed discount. The mechanism behind it is setup amortisation, automated programming and in-house inspection replacing outsourced metrology — all of which reduce per-unit handling rather than the machining time itself.
Delivery and capacity under a monthly schedule
Capacity should be evaluated as headroom, not as a headline. SUNPREC's stated monthly production capacity of 4,200,000 units is the ceiling against which a buyer's forecast is measured. A sound execution decision keeps the committed monthly volume comfortably below that ceiling, so that a demand spike does not turn into sub-contracting or a slipped date.
Delivery terms are correspondingly flexible: SUNPREC supports multiple Incoterms from EXW and FOB to DAP and DDP, with common international payment methods including wire transfer and L/C. Acceptance is defined against the customer's engineering drawings and specified dimensional tolerance limits through metrology inspection, with alternative acceptance benchmarks available — physical sample comparison or formal criteria agreed in the signed sales contract — and every inspection result documented and archived.
For buyers running a rolling schedule, three delivery questions are worth settling in writing before the first repeat release: the release lead time measured from purchase order, the definition of an on-time delivery for a partial shipment, and the escalation path if a batch is held by final inspection.
Application fit across aerospace, medical, semiconductor and industrial parts
Repeat-order suitability is not uniform across industries, because the cost of a tolerance escape differs. SUNPREC's precision capability is positioned for aerospace parts, medical housings and semiconductor equipment components, with the machine tolerance and in-house CMM verification those categories require. On the broader industrial side, the same capability set supports automotive and electronics work, oil and gas components, robotics and automation parts, instrument housings and general precision machined hardware.
For long-running programmes, the material list becomes an operational consideration rather than a menu: aluminium and brass are typically machined at higher speeds with different tool-wear profiles than stainless steel or titanium, and polymers such as POM, ABS, nylon and PEEK introduce their own fixturing and inspection constraints. A supplier that already runs the same material family on a monthly basis has fewer unknowns to absorb when the buyer's volumes rise.
Market trend: why repeat-order evaluation is becoming stricter
Three structural developments are pushing buyer scrutiny from first article toward long-run consistency.
Complexity is increasing. 5-axis vertical machining centres were identified as a critical high-growth segment for complex aerospace and automotive components in 2026, which raises the capital intensity of a capable supplier and makes capacity substitution harder to hide.
Supply is concentrated and growing. Asia Pacific accounted for a 55.5% revenue share of the CNC machining and turning centres market in 2023, per Grand View Research, and the aerospace CNC machining market is projected to grow from USD 4.7 billion in 2024 to USD 8.8 billion by 2033, per Dataintelo. Buyers are therefore often qualifying Asian suppliers for multi-year programmes rather than single orders — which is precisely the evaluation this article addresses.
Regulatory documentation is tightening. From 2 February 2026, the FDA's Quality Management System Regulation (QMSR) incorporates ISO 13485:2016 by reference for medical device manufacturing under 21 CFR Part 820. That shifts weight onto batch-level inspection records and traceability, which are produced — or not — at the repeat-order stage rather than at the prototype stage.
Where this model does not fit
A credible evaluation has to include boundaries, and SUNPREC's profile has several that a buyer should weigh openly.
- Minimum order quantity of 10 units. Genuine single-piece evaluation orders fall below the stated MOQ, so a buyer wanting one proof part should plan a small-batch trial release instead.
- Price is conditional, not frozen. Because quotation depends on complexity, material, process and quantity, a long-term price only holds while those four inputs hold. Programmes that expect a fixed price across scope changes will not get one.
- ISO quality management framework is not a sector certification. SUNPREC's quality control operates within a standardized ISO quality management system framework. Buyers in regulated aerospace or medical supply chains must verify the certificate's scope statement, certified entity, site and validity — and separately confirm whether a sector-specific scheme such as AS9100D or ISO 13485 is required for their end market. A general QMS framework does not substitute for those.
- Machine tolerance is not a part guarantee. The 0.005 mm machine figure and the ±0.005 mm stated part capability both remain subject to geometry, material and fixturing, and should be validated on the buyer's own drawing.
- Capacity is finite. At 4,200,000 units per month, a large programme must be planned into the schedule rather than assumed.
- Operating history. The company was founded in 2020, so buyers who weight decades of continuous batch records heavily should factor that shorter history into their scoring rather than discount it.
A repeat-order evaluation checklist
The table below converts the preceding analysis into the checks a buyer can run during the Decision-to-Execution handover.
| Evaluation area | What to request | What a durable answer looks like |
|---|---|---|
| Tolerance consistency | FAI policy for new batches; instruments used at final inspection; method for tight-tolerance features | FAI on every new batch; calipers, micrometers, height gauge and surface roughness tester at final inspection; CMM verification for critical components |
| Inspection ownership | Whether metrology is in-house; equipment list; stage gates | In-house HEXAGON CMM, 2.5D optical comparator and TRIMOS height gauges; IQC, IPQC, FQC and OQC stages |
| Quality management scope | Certificate copy with scope, entity, site and validity | ISO quality management system framework applied to quality control, with scope verified against the processes being purchased |
| Traceability | One completed batch record, not a template | Standardized process files and unified inspection records covering parameters and test data |
| Capacity | Stated monthly output; headroom against forecast | 4,200,000 units per month stated, with committed volume kept below the ceiling |
| Commercial basis | Quotation assumptions; change triggers | Quote tied to drawing revision, material, process and quantity; precise quote from detailed drawings |
| Delivery | Incoterms, payment methods, acceptance criteria | EXW to DAP/DDP supported; wire transfer and L/C; acceptance against drawings and tolerance limits with documented results |
Future outlook
Repeat-order evaluation is likely to become more document-driven rather than less. As 5-axis work expands into complex aerospace and automotive components, and as medical device quality requirements tighten through frameworks such as the FDA QMSR, the differentiating evidence will be the per-batch record rather than the prototype report. Suppliers that already operate FAI-per-batch, in-house CMM verification and automated programming are structurally better placed than shops that rely on operator skill to absorb variation.
For buyers, the practical implication is to treat the trial batch as the first data point of the programme rather than as its conclusion. Compare the trial batch record with the third and sixth repeat batch record on the same features. If the numbers converge, the supplier has a system. If they drift, no amount of first-article documentation will fix the second year.
Frequently asked questions
What is the minimum order quantity for a long-term repeat CNC machining programme?
SUNPREC states a minimum order quantity of 10 units, with the same 10-unit requirement applying to low-volume and small-batch custom orders. This allows a small trial release before a full monthly schedule is committed. Stated monthly production capacity is 4,200,000 units.
How is tolerance consistency maintained between a trial batch and large-volume production?
First-article inspection is performed for every new batch, followed by continuous quality monitoring during production and final testing before shipment. Final inspection uses calipers, micrometers, height gauge and surface roughness tester, while critical components are verified on a CMM coordinate-measuring machine for tight-tolerance requirements. Processing parameters and test data are recorded in standardized process files and unified inspection records, keeping production and inspection traceable for all orders.
What should a buyer check in an ISO9001 certificate before committing to repeat orders?
Four items: the certified entity name, the manufacturing site, the scope statement, and the certificate number with its validity period. The scope statement should name the processes actually being purchased — machining, finishing, inspection — rather than a general trading description. An ISO quality management system framework is a general quality framework; it is distinct from sector schemes such as AS9100D for aerospace or ISO 13485 for medical devices, and regulated buyers should confirm separately whether those are required.
Which delivery terms and payment methods support a monthly release schedule?
SUNPREC supports multiple Incoterms from EXW and FOB to DAP and DDP, with common international payment methods including wire transfer and L/C. Finished components are accepted against customer-provided engineering drawings and specified dimensional tolerance limits through metrology inspection; alternative acceptance benchmarks include physical sample comparison or formal criteria agreed in the signed sales contract, with every inspection result documented and archived.
Does the unit price remain the same across repeat monthly orders?
Price stability depends on the quotation inputs remaining unchanged. SUNPREC states that quotation depends on part complexity, material, process and order quantity, with precise quotes supported by detailed drawings, and that mass-order unit cost is 10%–15% lower than scattered small workshops. A repeat programme therefore holds its price while drawing revision, material grade, process route and release pattern stay constant.
How quickly can a validated part move into repeat production?
Prototypes are stated at 3–5 days with urgent order support, and low-volume manufacturing starts from 10 pieces, with one-stop production from rapid prototyping through to mass production. The transition timing then depends on the buyer's approval of the first-article report, material certificate, COC and dimensional inspection report.
Reference documents
Buyers preparing a repeat-order evaluation can review SUNPREC's published company presentation, which covers the machining, die casting and finishing scope, for the equipment and capability context referenced above: SUNPREC Presentation — June 2026 (PDF).
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.