
Cable Accessory Supplier Continuity: Materials and Lifecycle Evidence
Cable Accessory Supplier Continuity: Materials and Lifecycle Evidence
Long-term cable accessory supply is rarely lost on price. It is lost on discontinuities: a silicone formulation that shifts between production batches, an installation drawing that changes the stress-cone dimension, a sealing compound that is discontinued, or a technical contact who cannot answer a jointing question in the third year of a framework agreement.
For buyers moving from supplier selection into project execution, supplier sustainability is better tested against three evidence classes than against a quotation. The first is material continuity — whether the named silicone rubber, polyurethane prepolymer, SS304/SS316/SMC FRP or tin-plated copper is held to grade across orders. The second is documented test evidence — what was measured, under which conditions, and by which laboratory. The third is installation-support continuity — whether the same termination and jointing logic can be repeated across a multi-year programme without invalidating crews' training.
Production workshop: cable accessory manufacturing for medium-voltage terminations, joints and protective housings.
Tonyhoo Cable Accessories (Ningbo Tonyhoo Electrical Technology Co., Ltd., founded 1997) manufactures cold shrink and heat shrink terminations, cold shrink intermediate joints, separable connectors, cable lugs, grounding boxes, polyurethane sealant, explosion-proof blankets, and FRP or aluminium-magnesium alloy protection housings, and also lists oil-immersed transformers and switchgear within its stated business scope. This article uses that portfolio to show what continuity evidence looks like in practice, and where the evidence stops.
Why continuity outranks unit price in medium-voltage accessory supply
The purchase price of a termination or joint occupies one budget line. The consequences of its failure occupy several others: outage time, re-excavation where the joint is buried, re-termination labour, re-testing, and the schedule risk created by a repeat visit to site. That asymmetry — not any single product specification — is why long-term supplier evaluation belongs in the lifecycle-risk column rather than the price column.
The operating environment explains part of the risk. Outdoor accessories face rain, ultraviolet radiation, temperature differentials and surface contamination. Over time these can drive insulation ageing, seal failure and water ingress, and a water-ingress breakdown typically presents as a short circuit and trip rather than as gradual, easily observed degradation. Practical mitigation is unglamorous and repeatable: select weather-resistant cold shrink and heat shrink accessories, complete sealing strictly according to process, inspect periodically for cracked outer sheaths and seepage at sealing positions, and replace rather than re-energize damaged units.
Installation accounts for the other half. IEEE 1816-2024, the IEEE guide for preparation of shielded cables and installation of mating accessories, addresses cable preparation for 2.5 kV through 46 kV applications (IEEE SA, effective 2025-04-04). Its existence does not remove the interface risk; it locates it. Cable preparation dimensions and the accessory's stress-control geometry must match, and that match is delivered through instructions, drawings and trained people — the parts of a supplier relationship that are hardest to replace when a supplier changes mid-programme.
Mapping the portfolio to the risk each product controls
A continuity assessment is easier when each product group is tied to a specific failure mode. The table below maps the portfolio to the operational risk each item addresses, together with the parameter that should be re-confirmed on every order rather than only on the first one.
| Product group | Risk it controls | Continuity parameter to re-confirm |
|---|---|---|
| Cold shrink termination | Electric stress control and sealing at the cable end, indoor or outdoor | Silicone body specification, stress-cone position, voltage class |
| Cold shrink intermediate joint | Conductor connection and insulation restoration on buried and trench routes | Dimensional range against cable cross-section, instruction revision |
| Heat shrink termination | Insulation and sealing where heating equipment and certified operators are available | Tubing wall, adhesive liner, heating procedure |
| Separable connector | Interface between cable and switchgear or transformer | Partial discharge value and the conditions it was measured under |
| Cable lug | Conductor termination and contact corrosion | Tin-plated copper grade, barrel dimensions, plating coverage |
| Grounding box | Armour and metallic screen earthing, plus enclosure sealing | Air-tightness test record |
| Polyurethane sealant | Moisture and dust ingress at the connection area | Prepolymer grade, batch, shelf life |
| Explosion-proof blanket | Thermal and arc containment in confined or high-risk locations | Material and coverage matched to the stated application |
| FRP protection housing (SS304/SS316/SMC FRP) | Mechanical and environmental protection of joints on accessible routes | Material grade and wall construction |
| Aluminium-magnesium alloy protection housing | Corrosion-resistant mechanical protection where weight matters | Alloy grade and surface treatment |
Read the table as a specification checklist rather than a product list. Two buyers can both order “a cold shrink termination” and receive non-equivalent items if neither purchase order names the silicone body, the stress-control element and the dimensional range. That gap is the single most common source of discontinuity in accessory supply, because it survives the first delivery and only surfaces at the second or third re-order.
Product display: terminations, joints, lugs and protective housings grouped by function.
Material continuity: what the specification must actually name
Material continuity is the least visible and most expensive form of supplier drift. Four material families carry most of the lifecycle risk in a medium-voltage accessory programme, and each has a different failure signature.
Silicone rubber provides the elastic memory on which cold shrink installation depends. Because the body is stretched over a support core and then allowed to contract onto the cable, its retention of elasticity over thermal cycles governs how long the interface pressure — and therefore the sealing and stress control — is maintained. Tonyhoo's own comparison material for cold shrink against traditional heat shrink terminations cites a 35% higher retention of product elasticity and a 40% longer waterproof sealing life, alongside better performance under high salt-spray and humid conditions. Those figures are supplier-stated and project-dependent, but they identify the correct variable to test: elasticity retention, not initial hardness.
Polyurethane prepolymer is the chemistry behind the sealant used at connection areas. Its behaviour depends on surface condition at the moment of application, which is why the sealant is a process-controlled item rather than a commodity tube. A change of prepolymer grade between batches is difficult to detect after installation and easy to detect on the delivery note — if the grade is written there.
SS304, SS316 and SMC FRP are the material options behind protection housings. Stainless grades and sheet-moulding compound composites differ in corrosion behaviour, mass and mechanical response, and they are not interchangeable on a like-for-like basis simply because both are described as “FRP” or “protective shell”. The grade, not the family name, is the continuity parameter.
Tin-plated copper governs the cable lug. Tin plating limits oxidation of the copper contact surface, so plating coverage and thickness belong in the purchase specification rather than in the cosmetics column. A lug that meets its dimensional requirement but not its plating requirement will pass goods-in inspection and fail in service.
Industry technical descriptions show why this level of specification matters. 3M, for example, describes its cold-shrink QT-II and QT-III terminations as a pre-stretched high-dielectric-constant stress-control tube combined with a silicone-rubber termination insulation body (3M, 2026). Buyers do not need to copy one manufacturer's construction, but they do need to know which material families their own approval depends on — because that list is what a re-order has to reproduce.
Documented test evidence: three values and how to read them
Test evidence converts a material claim into a repeatable one, provided the number is read together with the condition and the sample identity. Three values in the Tonyhoo accessory range illustrate the pattern.
Grounding box air tightness at 0.2 MPa for 30 minutes. The value describes an enclosure held under internal pressure for a defined duration without loss of seal integrity. For the buyer, the relevant question is not whether 0.2 MPa is impressive but whether the test object is the same box, with the same gasket and the same cable entry configuration, that will be delivered. Air tightness is a direct proxy for the water-ingress path that outdoor and underground installations are exposed to.
A 37.5 kV impact test repeated ten times. Repetition is what distinguishes this from a single-pass mechanical check: it addresses whether the assembly remains serviceable after repeated mechanical events rather than after one. When reviewing the report, confirm whether 37.5 kV is the applied test level or a withstand level, what the impact configuration was, and whether the sample was subsequently subjected to an electrical check.
Separable connector partial discharge at or below 10 pC. Partial discharge is the most sensitive indicator of voids, interface defects and incomplete stress control in a separable connector, because it responds to defects that a power-frequency withstand test can pass. The number is only comparable when the applied voltage, the measuring method and the sample configuration are stated. A “≤10 pC” figure quoted without those three conditions cannot be benchmarked against another supplier's figure.
At supplier level, Tonyhoo states that its products have been tested by the State Grid High Voltage Testing Center, SGS, or the Shanghai Cable Research Institute, with corresponding reports issued. For a long-term agreement, the practical rule is simple: a test report is continuity evidence only if the model and voltage class on the report match the model and voltage class on the purchase order, and if the report carries a date. A report that cannot be matched line-by-line to the delivered item documents a different product.
Installation-support continuity: cold shrink versus heat shrink
Installation support is where a supplier relationship is either repeatable or fragile. Cold shrink and heat shrink terminations solve the same insulation, electric-field-control and sealing requirements, but they distribute the work differently, and that difference has direct consequences for a multi-year programme.
| Dimension | Cold shrink termination | Heat shrink termination |
|---|---|---|
| Installation method | No heat gun or open flame; body contracts when the support core is pulled | Requires external heating equipment and a certified flame operator |
| Best-fit conditions | Outdoor distribution lines, underground cable pits, confined spaces, locations where open flame is prohibited | Budget-limited projects where heating equipment and qualified operators are already available |
| Cost profile | Slightly higher unit purchase cost; supplier comparison material cites roughly 50% less on-site working time and about 30% lower total cost over the full life cycle | Lower unit cost; total cost depends on labour rate, equipment and operator availability |
| Support dependency | Instruction revision, support-core pull method and stress-cone positioning | Heating procedure, temperature control and operator certification |
Neither method is universally superior. Both can meet the insulation, electric field control and sealing requirements of medium-voltage cables; the selection question is whether open flame is permitted on site, what the schedule and budget allow, and which installation competence is available. The comparison percentages above are drawn from supplier comparison material and depend on cable size, site conditions and operator experience; they are a starting hypothesis for a buyer's own measurement, not a substitute for it.
The installation sequence itself is the support asset. The documented steps for a cold shrink termination are: confirm cable specifications and product compatibility; prepare the cable to the specified dimensions; clean and dry the cable surface; position the stress control and sealing components; position the cold shrink body and remove the supporting core according to the instructions; check component positioning and sealing; and complete the required inspection and testing before energizing.
Each step maps to a known failure mode. Scratches on the main insulation, a rough cut on the semi-conductive layer, moisture or dust on the installation interface, and an offset stress cone are the principal inducements of later breakdown in cold shrink terminations. Stripping strictly to process dimensions, keeping the insulation surface clean and dry, and positioning the stress cone accurately are what prevent them. For a long-term buyer, this means the supplier's obligation does not end at delivery: if the instruction revision, the support core or the stress-cone geometry changes without notice, a trained crew's established method is silently invalidated. Instruction version control is therefore a continuity clause, not paperwork.
Sealing practice with polyurethane sealant
Sealing is the lowest-cost and highest-leverage step in the whole accessory installation. Polyurethane sealant is applied to cable connections to help prevent moisture, dust and other contaminants from entering the connection area, and reliable protection depends on surface preparation, correct application and complete coverage rather than on quantity applied.
The documented procedure is short: isolate and disconnect the cable; clean and dry the cable and connection surfaces; prepare the sealant according to the product instructions; apply it evenly around the required sealing area; ensure complete coverage without gaps or exposed areas; then inspect the finished seal before the connection is returned to service. Installation should be carried out by qualified electrical personnel using appropriate personal protective equipment, and the cable should not be energized until the connection has been inspected.
The limitation is worth stating plainly: sealant compensates for a correctly prepared surface, not for a contaminated one. A seal applied over moisture or dust will look complete and behave as a void. In a lifecycle-risk assessment, sealant quality and sealant discipline are separate line items — the first is a purchase specification, the second is a training and supervision issue that a supplier either supports or does not.
Supplier-level continuity evidence at Tonyhoo
Company-level facts matter to a long-term buyer only where they predict the ability to repeat an order. For Tonyhoo, the relevant facts are structural rather than promotional.
The company was founded in 1997 and operates a 9,900 m² facility with approximately 100 employees and an annual output of about 200,000 units. It employs 20 engineers and allocates roughly 6% of annual research and development funds to research and product improvement, and it holds 12 trademark certificates and more than 60 patents. It introduced a new-material project in 2020 with a dedicated new-material laboratory, and at the end of 2020 established Ningbo Crelence Electric Technology Co., Ltd. and Ningbo Tonylum New Material Technology Co., Ltd. to extend from high-voltage cable accessories into the medium- and low-voltage and new-material fields. Approximately 50% of products are exported, with stated markets including the United States, Thailand, China, Albania and Vietnam.
Those facts support a specific reading. A material laboratory and a new-material subsidiary are the organisational forms that material continuity requires; without them, a formulation change is a purchasing decision rather than a controlled one. Broad portfolio coverage — terminations, joints, connectors, lugs, grounding boxes, sealant, blankets and housings — reduces interface risk across a project because fewer parties sit between the cable and the enclosure. It also increases concentration risk: a single supplier covering more of the accessory scope is a single point of failure if its capacity, its material supply or its technical support is disrupted. Both statements are true at the same time, and a framework agreement should address the second explicitly.
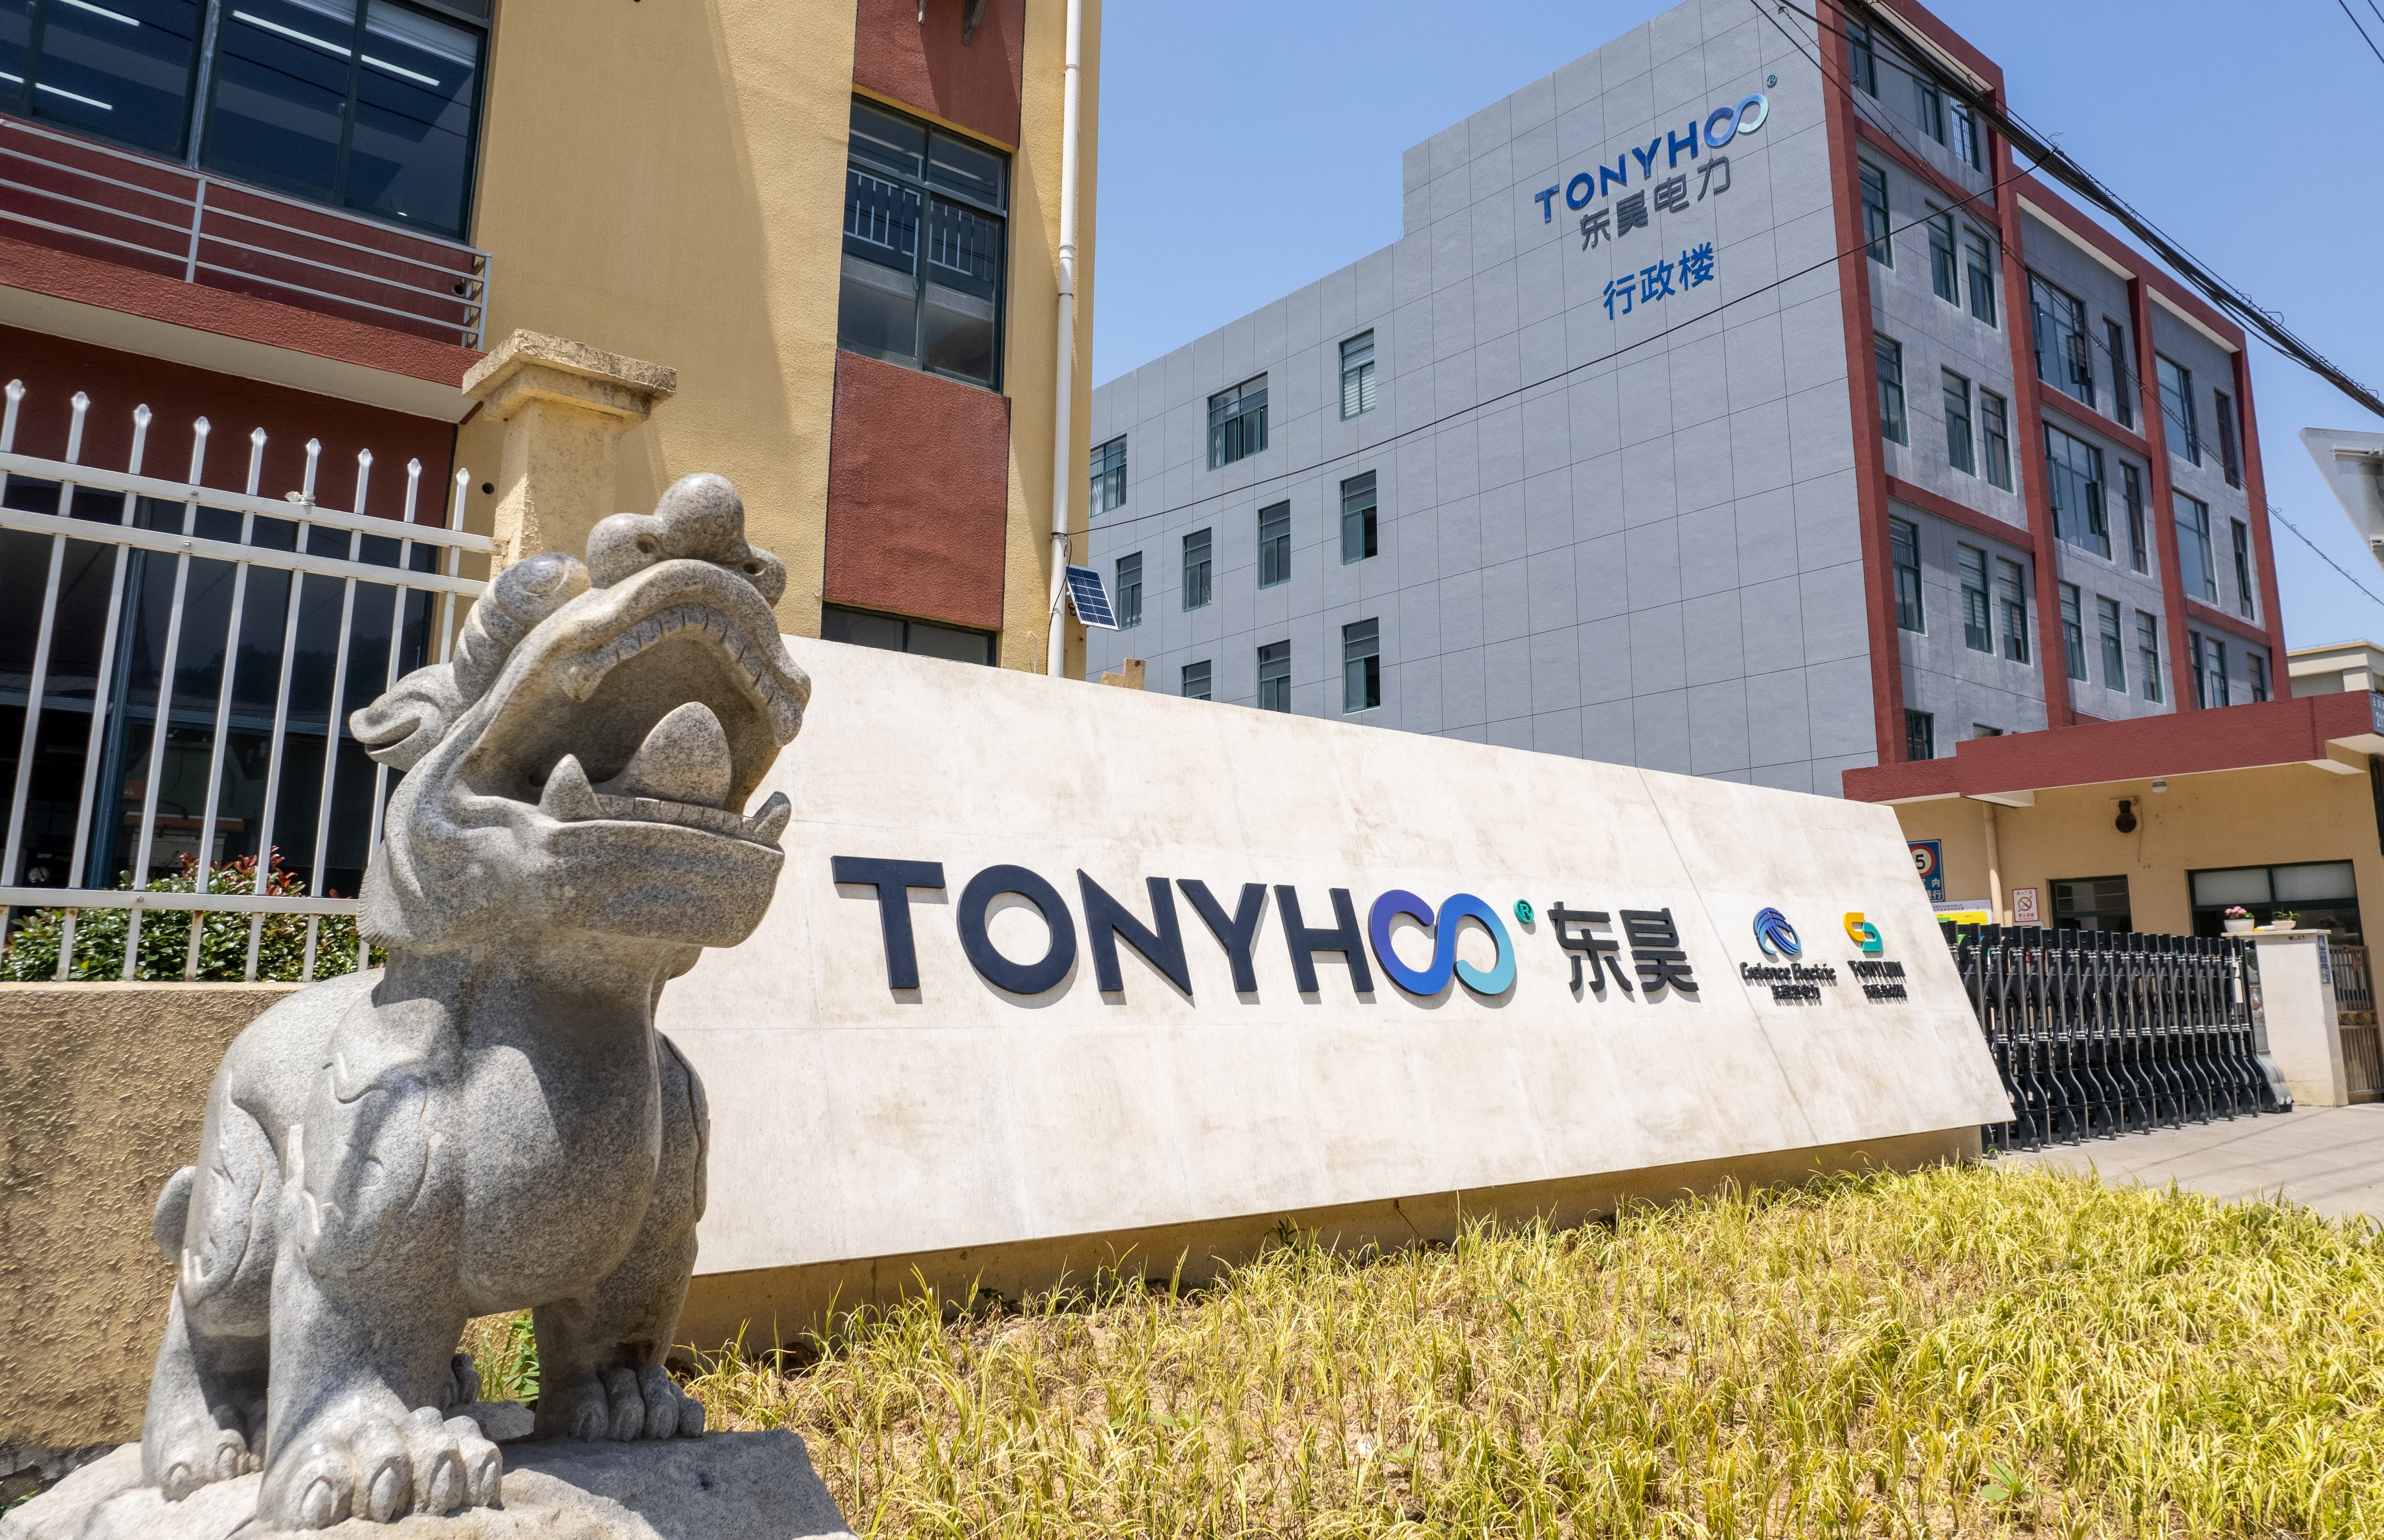
Manufacturing site: the facility and material laboratory behind medium-voltage accessory supply.
Execution-stage checkpoints for a framework order
Once a supplier is selected, continuity is protected by documentary checkpoints rather than by goodwill. Tonyhoo's stated commercial terms provide a concrete example of what those checkpoints look like: a minimum order quantity of 20 units; delivery terms of FOB, CFR or CIF; acceptance based on a pre-shipment test; and payment terms of 50% deposit in advance with the remaining 50% payable before shipment.
Four checks should sit alongside those terms. First, that the purchase order names material grades and not only product categories. Second, that the pre-shipment test scope is written into the order and matched to the agreed standard. Third, that instruction revision numbers are recorded in the contract, so a change is notified rather than discovered on site. Fourth, that delivery lead time is confirmed at the selection stage — a step Tonyhoo's own guidance places at the end of the selection process precisely because it is what framework agreements depend on. Buyers should confirm current terms, voltage-class availability and documentation directly with the supplier, since commercial terms and product availability may change between orders.
Market context: what the demand data can and cannot tell a buyer
Category-level market research gives directional context for a continuity argument but cannot size an individual supplier relationship. Global Market Insights estimates the global cable accessories market at USD 35.84 billion in 2025, with a projected USD 37.88 billion in 2026, covering low-, medium-, high- and extra-high-voltage accessories, and identifies Asia Pacific as the largest and fastest-growing region on the basis of grid modernization (GMI, 2026). Adjacent segment indicators from the same source put cold shrink tubing at USD 2.38 billion in 2024 and heat shrink cable accessories at USD 2,113.7 million in 2024; the two figures use different product scopes and unit bases and should not be read as a like-for-like ranking.
Trade statistics are a weaker input than they appear. HS heading 8544 covers insulated wire, cable and other insulated electric conductors, whether or not fitted with connectors (UK Trade Info, 2026), and does not isolate accessory hardware such as joints, terminations, separable connectors, lugs, sealants or housings. A buyer therefore cannot map medium-voltage accessory supply through customs data; the substitute is direct supplier qualification with the documentary checks described above. That is a structural feature of this category, not a data gap that better reporting will close.
Where the evidence stops
Three boundaries should be stated openly. First, the test values quoted in this article — 0.2 MPa for 30 minutes, 37.5 kV impact repeated ten times, and partial discharge at or below 10 pC — are documented supplier values; they have not been independently reproduced here, and buyers should request the underlying reports for the specific model and voltage class being ordered. Second, the comparison percentages between cold shrink and heat shrink are supplier-stated and depend on cable size, installation conditions and operator experience; they describe a direction, not a guaranteed outcome. Third, portfolio breadth demonstrates scope, not capacity for any single item, and current availability by voltage class should be confirmed in writing at order stage.
Outlook: conditional, not forecast
If grid modernization in Asia Pacific continues at the pace implied by the 2026 market estimates, pressure will move from accessory demand to accessory inputs — silicone compound, copper, FRP laminates — and to the availability of trained jointing crews. In that scenario, the suppliers most able to hold a framework agreement are those that control material specification and instruction revision, because those are the two variables a buyer cannot re-verify at goods-in. Conversely, if project pipelines soften, the same evidence set becomes a consolidation argument: fewer, better-documented suppliers rather than a wider panel competing on unit price. Neither scenario is a prediction; both identify the same preparation.
Tonyhoo Cable Accessories publishes its product scope and technical documentation through Tonyhoo.
Frequently asked questions
What parameters should a buyer provide to a cable accessory supplier?
Confirm the rated voltage level, the cable model, conductor cross-section and core quantity, and the application environment — indoor, outdoor or direct burial — before requesting a quotation, and state whether the item is a termination or a joint. Complete parameters allow the supplier to match the correct specification and to ensure electric field control, sealing performance and compatibility with the cable body. Incorrect parameters cause product mismatch and can trigger insulation failure after energization, so dimensions and voltage class should be double-checked against the cable data sheet before the order is released.
How should a buyer choose between cold shrink and heat shrink cable accessories?
Start with the site: cold shrink accessories are preferred where open flame is not permitted and where construction schedules are tight, because they require no torch heating and are straightforward to install. Heat shrink accessories suit projects with a limited budget where certified flame operators and heating equipment are already available, and offer a clear cost advantage in that setting. Both types can meet the insulation, electric field control and sealing requirements of medium-voltage cables, so the decision is normally driven by site rules, schedule and operator competence rather than by electrical capability.
Which installation errors most often cause later breakdown of cold shrink terminations?
Scratches on the main cable insulation, rough treatment of the cut semi-conductive layer, moisture or dust on the installation interface, and offset stress-cone positioning during construction are the main inducements of later breakdown. Stripping strictly to the process dimensions, keeping the insulation surface clean and dry, and positioning the stress cone accurately avoid these risks and support long-term stable operation. Power isolation, voltage testing and earthing must be completed before work begins, operators should hold a valid cable construction qualification, and construction in wet or rainy conditions should be avoided.
How should polyurethane sealant be applied to protect a cable connection?
Isolate and disconnect the cable first, then clean and dry the cable and connection surfaces. Prepare the sealant according to the product instructions, apply it evenly around the required sealing area, and ensure complete coverage without gaps or exposed sections. Inspect the finished seal before the connection is returned to service. Installation should be performed by qualified electrical personnel using appropriate protective equipment, and the cable should not be energized until the connection has been inspected — sealant applied over a wet or contaminated surface will appear complete while leaving a void.
What safety risks affect cable accessories operating outdoors, and how are they managed?
Outdoor accessories are exposed to rain, ultraviolet radiation, temperature differences and contamination, which can lead to insulation ageing, seal failure and water-ingress breakdown, and from there to short circuit and tripping. Management combines weather-resistant cold shrink and heat shrink accessories, sealing installed strictly to process, and periodic inspection for cracked outer sheaths and seepage at sealing positions. Any accessory showing insulation damage should be taken out of service and replaced rather than re-energized; coastal salt-fog areas and locations with wide temperature swings are the conditions where this discipline matters most.
Reference: Tonyhoo product catalog (PDF)
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.