
Custom Toner Cartridge Orders: How Buyers Qualify a Batch
Custom Toner Cartridge Orders: How Buyers Qualify a Batch
A custom compatible toner cartridge order is a manufacturing commitment rather than a catalogue purchase. Once a buyer fixes a model list, a housing specification, a packaging format and a delivery schedule, the commercial risk shifts from “which product” to “which batch” — and the only reliable defence is a qualification process agreed before the first cartridge is filled.
A qualification process for custom toner cartridge orders has four moving parts: acceptance criteria defined during pre-sales, batch-level testing of incoming toner, independent verification of the factory either on site or by live video walkthrough, and a documented after-sales route when a batch underperforms. This reference sets out how each part works, what records a buyer should hold at the end of it, and where the limits of any supplier-side evidence sit.
Examples in this article are drawn from Far Industries Co., Ltd., a Zhongshan-based manufacturer of A3 office consumables producing compatible toner cartridges, drum unit assemblies, fuser unit assemblies and developing unit assemblies in-house. The intent is not to describe one company’s brochure, but to show what a buyer should be able to inspect, request and compare across suppliers bidding for the same custom order.
Toner powder warehouse and in-house testing laboratory: the two physical assets that determine whether batch-level toner verification is possible at all.
Why Custom Compatible Toner Orders Fail at the Qualification Stage
The typical failure in a compatible toner cartridge programme is not a single catastrophic defect. It is a slow divergence between what the buyer believed it approved and what the factory believes it is permitted to ship. In practice, that divergence appears in four recurring places.
Sample approval is treated as product approval. A buyer tests one or two cartridges, finds the print acceptable, and issues a bulk order. Nothing in the approval record defines which machine was used, which print attributes were checked, or what would constitute a rejection. When the first container arrives, both parties discover they were measuring different things.
The toner source changes between lots. Toner is the single largest determinant of print behaviour in a compatible cartridge, and it is a purchased material. A supplier that does not test each incoming toner lot against a retained reference can ship a cartridge that is dimensionally identical to the approved sample but prints differently, because the powder inside it changed.
Housing and tooling variance is invisible from the outside. Empty cartridge shells are injection-moulded parts. Dimensional accuracy and structural strength affect fit, sealing and drive engagement, and they are governed by the mould and the moulding machine rather than by the assembly line. A buyer who never asks where the tooling lives cannot distinguish a factory that controls its own moulds from one that buys shells on the open market.
No record survives the shipment. Without a batch record — lot code, toner lot, moulding date, test result, retained sample — a complaint three months later becomes a negotiation about memory rather than evidence.
Fixing Acceptance Criteria Before Price Is Discussed
Acceptance criteria are the contract’s technical spine. They should be written, measurable and agreed before a quotation is finalised, because a price quoted without them is a price for an undefined product. The following ten items cover what a custom compatible toner cartridge order should specify.
- Model coverage list. Every machine family the order covers, written with the same naming the factory uses internally. Broad phrases such as “Konica range” invite substitution; a named family list does not.
- Housing and component specification. The resin or housing grade, the tooling source, and the moulding platform used for empty cartridges. If the order specifies virgin PET housing, that specification belongs in the document, not in an email thread.
- Toner specification and lot traceability. The origin type of the toner (for example, imported material from specialised, publicly traded toner manufacturers), and the requirement that each incoming lot carry a traceable code.
- Print performance definition. Which attributes are evaluated, on which reference machine, at which settings, and against which retained sample.
- Sampling plan. How many units are drawn per batch, from where in the batch, and at what inspection level.
- Retained samples. One sealed, dated and labelled reference cartridge per batch, held by both parties, so that a future dispute is settled against an object rather than an opinion.
- Packaging, labelling and private-label artwork control. Artwork version approval, label placement, and the rule for handling obsolete packaging stock.
- Non-conformance terms. Whether a failed batch is reworked, replaced or credited, who carries freight, and within what window the decision must be made.
- Documentation set per shipment. The batch record, test summary and lot mapping that travel with the goods.
- After-sales response route. A named technical contact, an agreed response window, and the escalation path when a defect is suspected in the field.
Criteria of this kind are not bureaucracy. They convert a quality argument into a comparison against a written standard, which is the only basis on which two suppliers quoting different prices can be judged on the same terms.
What an Integrated Production Configuration Changes
Far Industries Co., Ltd. was founded in 2011 and operates a 9,000 m² facility in Zhongshan City with 88 employees, an engineering team of 8, and annual output of approximately 6,000,000 units. Its compatible toner cartridge range is offered under the Tenon toner cartridge name alongside drum unit, fuser unit and developing unit production.
The configuration matters to qualification because it determines how many of the ten criteria above the factory can actually control. Three corpus-verified points are directly relevant.
Tooling is held in-house. The company’s Mold Division owns more than 90% of the moulds used for copier toner cartridges, which allows product precision to be controlled from the source rather than negotiated with a third-party moulder. Empty toner cartridges are moulded exclusively on Yizumi precision injection moulding machines, selected for stable operation, precise temperature control and high repeatability — the properties that support dimensional accuracy and structural strength across a long production run.
Toner is tested lot by lot. Approximately 90% of the toner used in production is imported from specialised, publicly traded toner manufacturers. Every batch of incoming toner is tested in the company’s own dedicated testing laboratory to verify print quality and consistency after the toner is installed in a printer. This is the specific link between material sourcing and batch-level output stability.
The evaluation fleet is broad. The testing department runs 90 machines covering Canon, Ricoh, Kyocera, Konica Minolta, Sharp, Toshiba, HP, Samsung and Xerox platforms, which is what allows a model coverage list spanning Konica, Sharp, Xerox, Canon and Toshiba to be verified on real hardware rather than on specification sheets.
For a buyer, the practical translation is straightforward: when a supplier owns the mould, moulds the shell, fills the cartridge and tests the toner in the same building, the number of parties who can change an input without the buyer knowing is small. That is the structural argument for an integrated supplier — not that defects cannot occur, but that each production stage is inspectable at the point where it happens.
Technical Explanation: What Batch-Level Testing Actually Verifies
“We test every batch” is a claim, not a control. What makes batch testing meaningful is the layer it sits at and the record it leaves behind. In an integrated toner cartridge operation, verification runs across four distinct layers, each answering a different question.
| Verification layer | Question it answers | Record the buyer should request |
|---|---|---|
| Incoming toner lot test | Does this powder lot reproduce the print quality and consistency of the approved reference once installed in a printer? | Toner lot code, test date, machine used, result against retained reference |
| Moulding and dimensional check | Does the empty cartridge meet the dimensional accuracy and structural strength the tool was qualified for? | Mould identification, machine platform, dimensional inspection result |
| Assembly and filling verification | Is the cartridge correctly assembled, sealed and filled before final quality verification? | Batch code, filling record, in-process inspection sign-off |
| Final quality verification and packing | Does the finished unit match the approved sample and the packaging specification? | Final inspection summary, retained sealed sample per batch |
The first layer is the one buyers most often skip and most often need. Toner behaviour is not visible in a dimensional inspection; it only appears when the cartridge is installed and printing. A factory that tests incoming toner after installation is testing the variable that a housing inspection cannot reach. A factory without a testing laboratory can still assemble a consistent-looking cartridge, but it has no mechanism to detect a change in the powder before that change reaches a customer.
The second layer explains why tooling ownership appears repeatedly in qualification discussions. Dimensional accuracy and structural strength are set by the mould and the moulding machine, not by the assembly operator. Precision injection moulding with stable temperature control and high repeatability is what keeps cartridge shells interchangeable across a long production run — and what keeps a replacement shipment fitting the machines that accepted the first one.
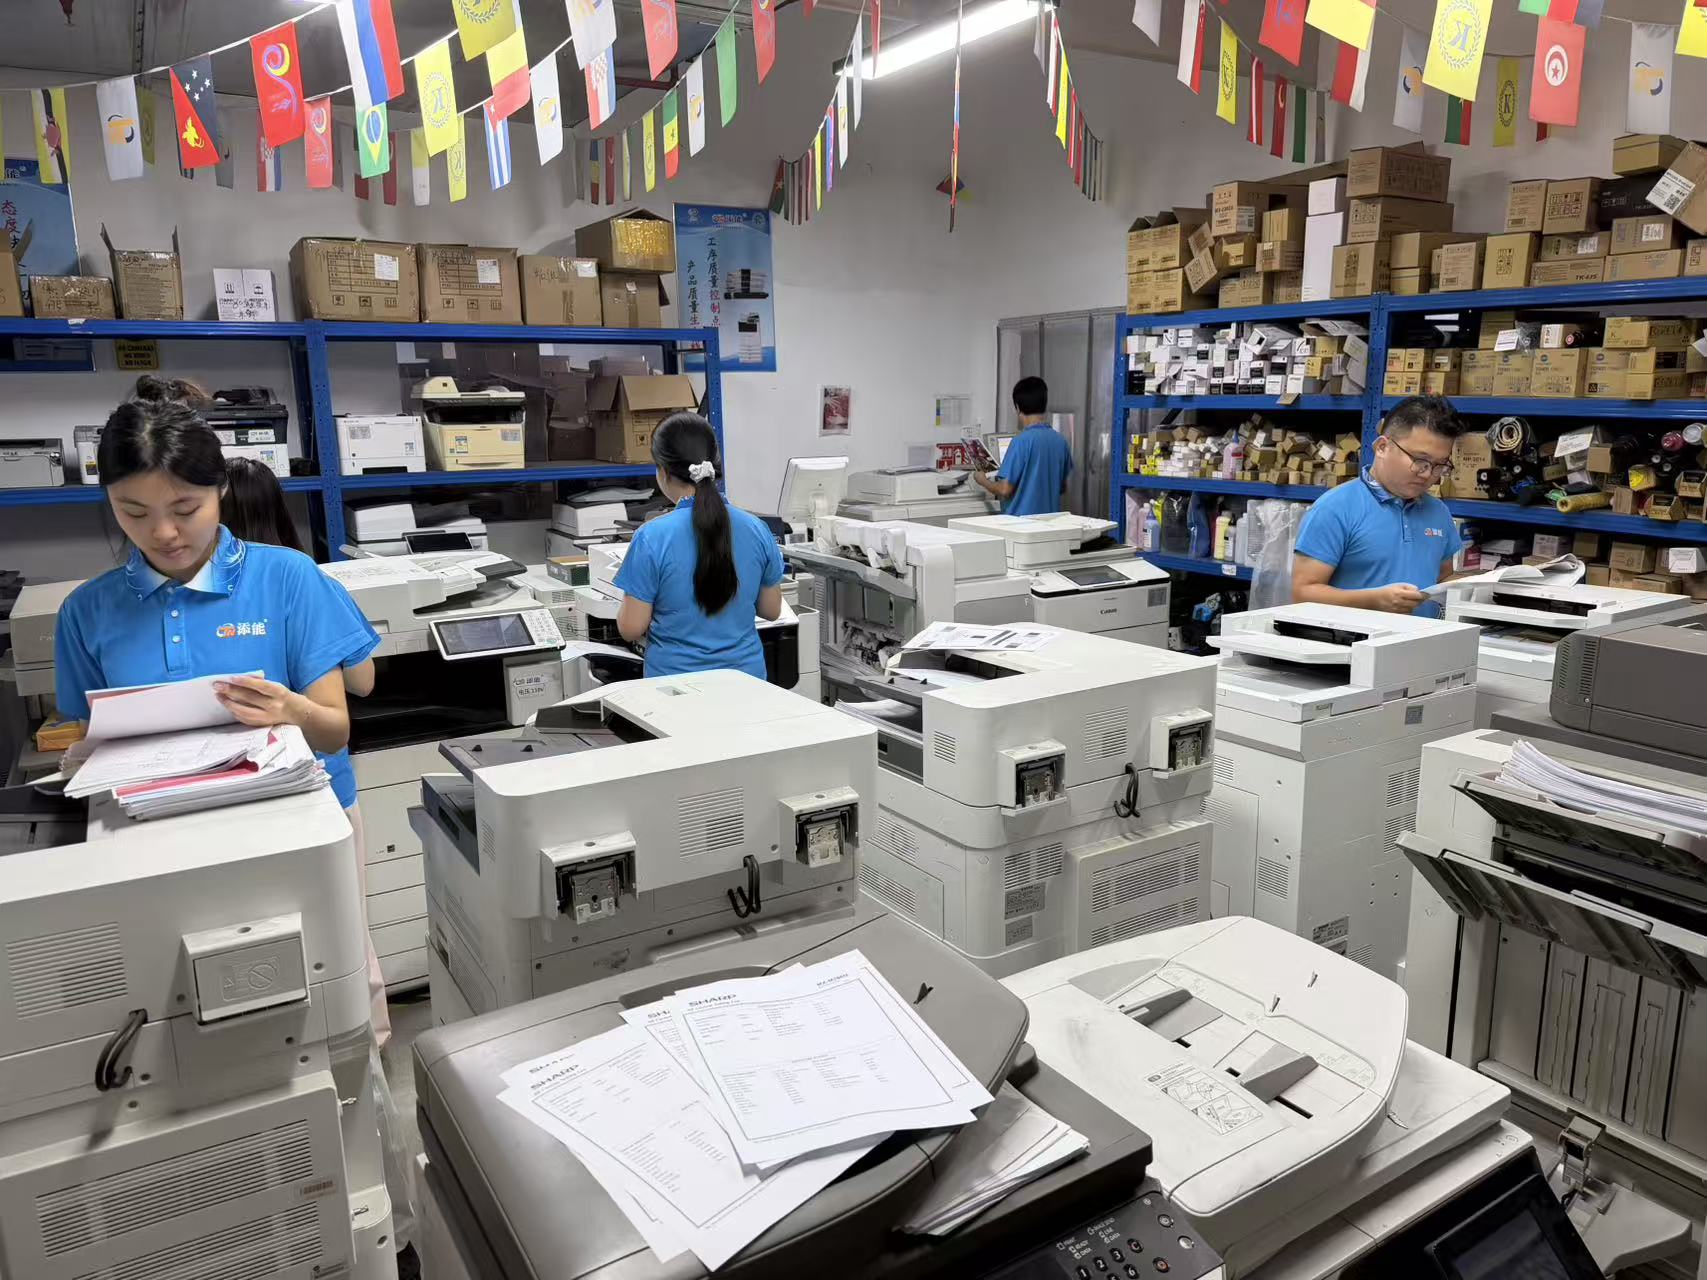
Batch-level toner evaluation in the testing laboratory. The test is performed after installation in a printer, because print behaviour is the property being verified.
Why the surrounding consumables belong in the same conversation
A toner cartridge does not perform in isolation. Print defects that a buyer attributes to the cartridge are frequently produced by the developer, the drum unit, the OPC drum inside it, the fuser unit or a worn fuser film. This is especially true for buyers running a second hand copier machine fleet or a reconditioned machine programme, where the host machine’s condition varies from unit to unit. When a supplier also manufactures copier parts and developing unit assemblies, a failure can be diagnosed across the consumable set instead of being argued about at the cartridge boundary — which shortens the after-sales loop considerably.
Verifying the Factory Without Travelling: The Video Walkthrough
Most first orders are placed without a site visit. The substitute is a live video walkthrough, and it is a reasonable substitute provided the buyer specifies what must be shown rather than accepting a pre-recorded tour. Far Industries offers both an on-site inspection in Zhongshan and a virtual walkthrough via video meeting, which is the format most overseas buyers use during the qualification stage.
A walkthrough built for qualification should follow the material flow, not the showroom. Ask to see, live and in sequence: the mould division with tooling storage visible; injection moulding machines in operation, with the machine platform identifiable; the toner powder warehouse with lot labels legible; the testing laboratory with machines running and a batch under evaluation; the filling area; and the packing line with private-label artwork in place.
Three questions separate a walkthrough from a performance. First, ask the camera operator to open a toner container and read the lot label aloud — a warehouse that cannot show lot labelling is not operating lot traceability. Second, ask for a cartridge shell to be taken from a production bin and inspected on camera for the dimensional features the order specifies. Third, ask what happens when an incoming toner lot fails its test, and who signs the release decision. The answer to the third question reveals more about the quality system than the first two combined.
A video walkthrough is evidence, not proof. It confirms that equipment exists, that it is running, and that the claimed layout is real. It does not confirm long-run consistency, which is why it should always be paired with batch records and retained samples from the first production run.
Where Third-Party Testing Fits, and Where It Does Not
Third-party testing is a buyer-side control, and it is worth commissioning in four situations: the first bulk order of a newly tooled model; entry into a market with specific compliance or import requirements; supply against a tender or framework contract that mandates independent verification; and the resolution of a dispute where supplier records and buyer experience disagree.
Its value depends entirely on how the sample is drawn and what the laboratory is asked to measure. A decision-grade third-party report should specify that samples are drawn from a sealed production batch with the lot code recorded, that the reference machine is defined in advance, and that the test scope is agreed in writing. A laboratory asked only to “check print quality” will return an opinion; a laboratory asked to evaluate defined attributes against a retained approved sample will return evidence.
What third-party testing does not do is replace the supplier’s own batch testing. An independent test samples a moment in time. It cannot tell a buyer whether the next toner lot will behave the same way. That assurance can only come from a factory that tests every incoming lot as routine practice — which is why the two controls are complementary rather than alternatives.
Application: Which Buyers Need Which Level of Acceptance Rigour
Acceptance rigour should scale with the cost of a failed batch in the buyer’s own operation. Compatible toner cartridge buyers generally fall into distinct groups, and the qualification emphasis differs by group.
Office supplies group purchasing and large distributors
These buyers aggregate demand across many end users and cannot afford a batch that behaves differently from the last one, because their customers notice. Their priority is consistency of output plus a documentation set that lets them answer a complaint without contacting the factory. For them, retained samples per batch and a written non-conformance clause carry more weight than a marginal price difference.
Copier leasing companies and managed print operators
Leasing fleets are contractual: a device under a service agreement must print to an agreed standard for the term of the lease. Acceptance emphasis falls on model coverage accuracy and on the supplier’s ability to hold specification across repeat orders, since the same model may be replenished five times over a lease period.
Large printing plants
High-volume environments surface drift quickly. These buyers tend to define print performance narrowly and to test incoming cartridges themselves, which makes the retained sample the central document in the relationship — it is the shared reference both parties test against.
Copy shops, advertising agencies and educational institutions
Smaller buyers rarely run formal qualification, but they are sensitive to the failure mode that qualification prevents: a mid-term switch in toner behaviour. For them, the practical control is ordering in batch-identified quantities and keeping a small sealed reference from each delivery. Educational fleets in particular mix machine generations, so a model coverage list covering Konica, Sharp, Xerox, Canon and Toshiba families is a genuine operational requirement rather than a commercial convenience.
Market Trend Analysis
Three verified market signals explain why batch-level qualification is becoming a procurement norm rather than an optional extra.
Volume growth concentrates risk in repeat orders. The global ink and toner market is projected to reach USD 38.47 billion in 2026 according to Business Research Insights, and toner cartridges accounted for 58.4% of the total global ink and toner product market in 2025 according to Dataintelo. Asia Pacific led regional revenue in 2025 at USD 8.7 billion, or 36.9% of the total, on the same Dataintelo dataset. When a category carries this share of a consumables market, buyers are almost never placing single orders — they are placing repeat orders, and repeat orders are where batch-to-batch consistency is won or lost.
Installed hardware keeps renewing itself. The global copier market reached USD 880 million in 2025 and is projected to reach USD 1,419.83 million by 2035 at a CAGR of 4.9%, according to Market Growth Reports. The OPC drum market is separately projected to reach USD 5.2 billion by 2033, growing at a CAGR of 5.5% from 2026, according to Cognitive Market Research. Both figures point the same direction: a large, slowly renewing installed base that consumes toner cartridges, drum unit assemblies, developing unit assemblies and fuser unit components year after year. Suppliers who can document consistency across that base have a structural advantage over suppliers who cannot.
Refurbished hardware is now a mainstream channel. Multifunctional refurbished printers and copiers accounted for 52% of total refurbished printer revenue in 2025, per Future Market Insights. This matters directly to toner cartridge qualification: a reconditioned machine population has variable host conditions, so cartridge acceptance cannot be settled on a single reference device. Suppliers serving this channel need a broader machine fleet in their testing laboratory and a model coverage list deep enough to match what the refurbishment trade actually resells.
Compliance is moving onto the cartridge itself. Spain reclassified toner cartridges as electronic waste under WEEE via Regulation TED/1032/2024, effective 2 January 2025, as reported by Tonernews citing the Boletín Oficial del Estado. Regulatory reclassification changes collection, labelling and take-back obligations for empty cartridges in that market. Buyers exporting into Europe should confirm with their supplier how packaging and batch labelling support their own compliance obligations, because a batch record without a legible lot code is difficult to reconcile against a take-back scheme.
Comparison with Traditional Supply Models, and the Boundaries of This One
Custom compatible toner orders are commonly quoted by three types of supply model, and the differences show up almost entirely in qualification rather than in unit price.
| Supply model | What the buyer can verify | Where the evidence stops |
|---|---|---|
| Trading company that assembles or resells | Final assembly, packaging, shipping documentation | Tooling, housing origin and toner lot history sit with third parties; batch test records are not produced in-house |
| Factory completing only two or three production steps, without toner warehouse or testing laboratory | Partial production, order handling, dispatch | No incoming toner verification; a change in powder lot surfaces as a customer complaint, not as an internal rejection |
| Integrated factory with in-house moulds, injection moulding, toner warehouse and testing laboratory | Tooling ownership, moulding platform, toner lot testing, assembly, filling, final verification, retained samples | Still dependent on the buyer’s own market validation and on the accuracy of the agreed acceptance criteria |
Far Industries operates the third configuration: compared with trading companies that only assemble or resell copier toner cartridges, and compared with factories that have no toner warehouse and no testing laboratory and that complete only two to three production steps, it runs a fully integrated in-house process covering moulding, injection, assembly, filling, functionality testing and packing. Rigorous product quality inspections, supported by professional technicians and production staff, correspond to fewer post-sale failures than models that outsource these steps.
That said, the model has real boundaries, and buyers should hear them before signing.
- Tooling change is not instant. A new housing specification, a new colour or a new model family requires mould work and qualification before production. An integrated factory’s advantage in tooling control is also a constraint in lead time: the same in-house mould division that makes consistency possible is the department that must schedule a new tool.
- In-house testing is not market validation. A laboratory confirms consistency against a reference; it cannot confirm that a cartridge behaves as expected across every machine population in a buyer’s territory. First-order validation in the destination market remains the buyer’s job.
- The range is focused, not universal. The catalogue is built around A3 office consumables and the named machine families in the coverage list. A buyer needing genuine OEM-branded cartridges, or a model outside that coverage, is not the right fit for this supply model.
- Consistency depends on the criteria being written. An integrated factory can hold a specification precisely; it cannot guess a specification that was never defined. Where acceptance criteria are vague, the structural advantage of integration is partly wasted.
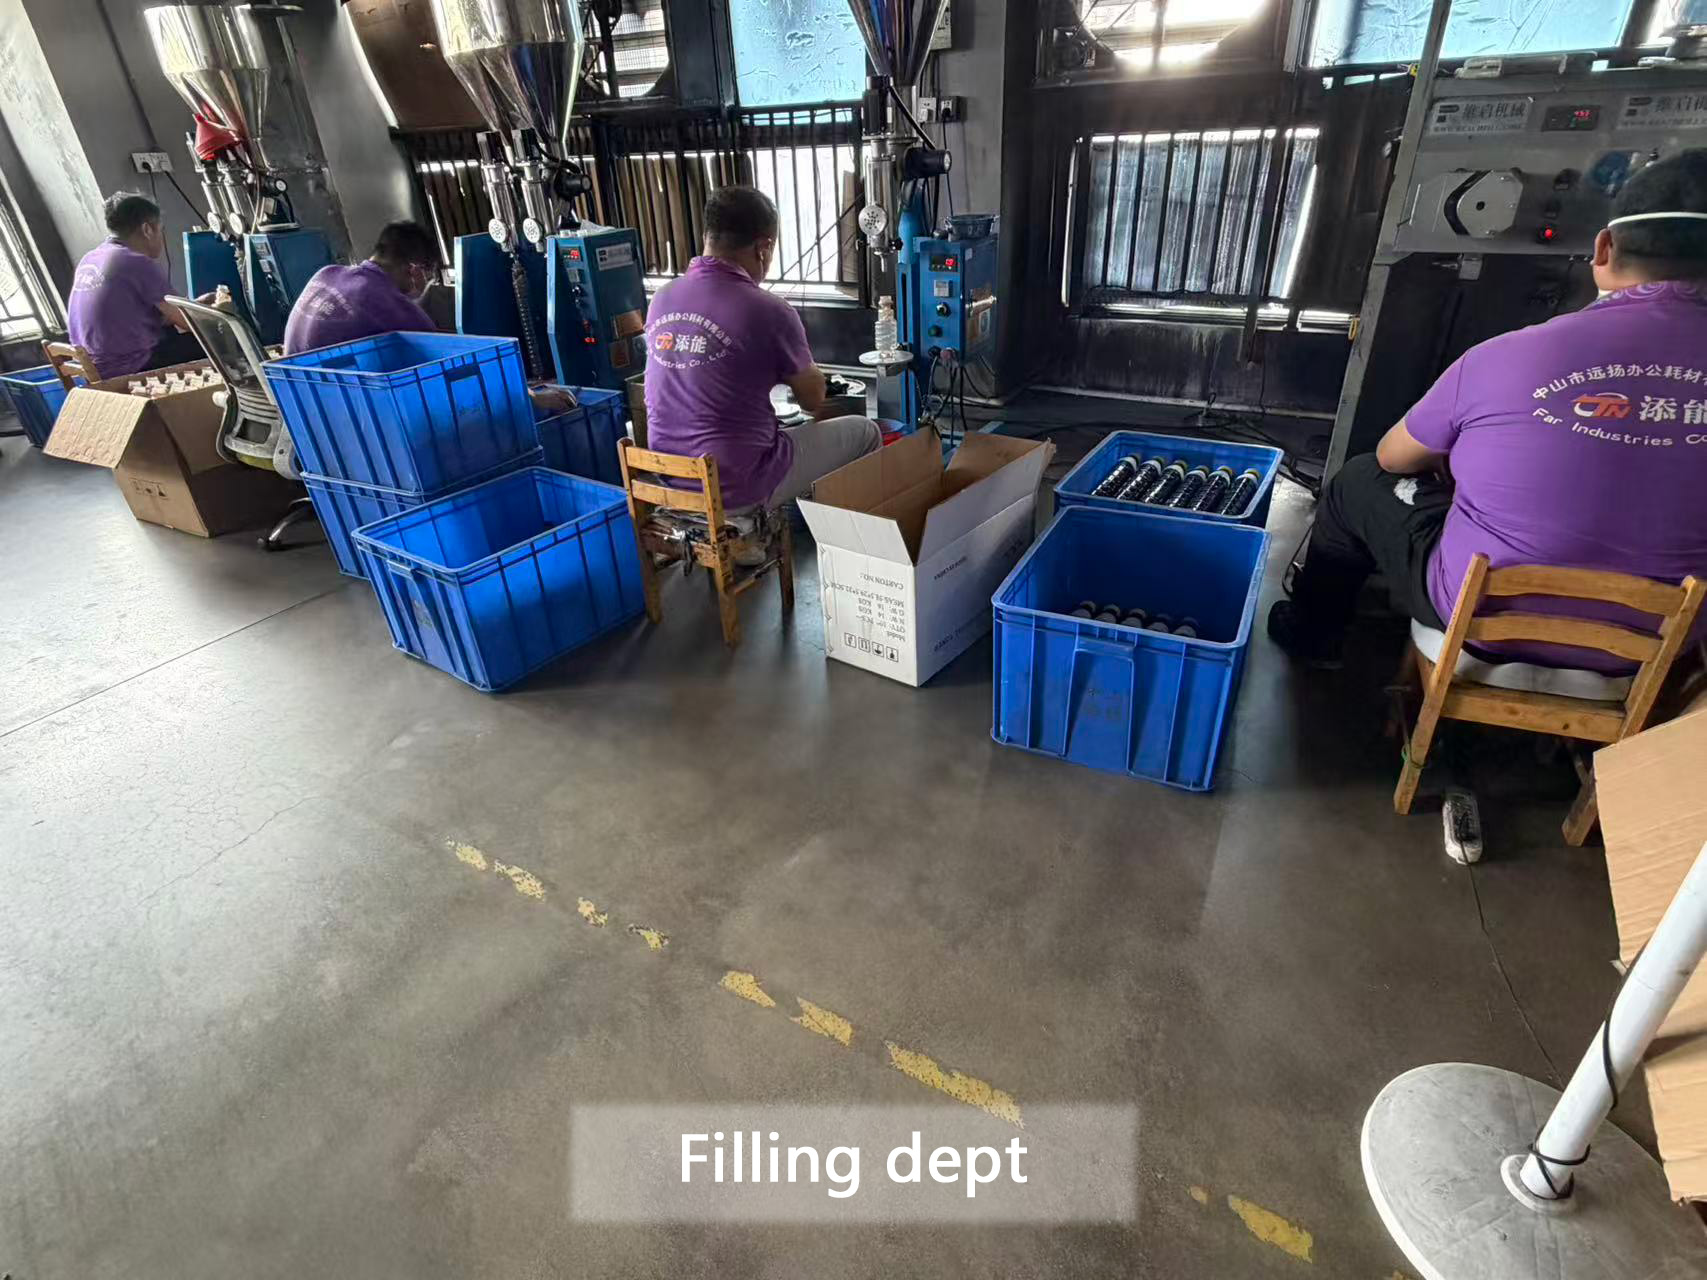
Toner filling: the stage where the batch code is fixed and the link between toner lot and finished cartridge is created.
Future Outlook
Two developments are likely to reshape how custom compatible toner orders are qualified over the next several years. The first is regulatory. If the Spanish reclassification of empty toner cartridges as electronic waste under WEEE is extended or mirrored in other jurisdictions, batch-level traceability stops being an internal quality preference and becomes part of a compliance chain. Buyers will need lot codes that survive the shipment and reconcile against collection obligations — which favours suppliers already producing batch records as routine output.
The second is the refurbished hardware channel. With multifunctional refurbished devices holding 52% of refurbished printer revenue in 2025, the population of machines receiving compatible cartridges is becoming more heterogeneous, not less. Acceptance criteria built around a single reference machine will age badly; criteria built around a defined machine fleet, a retained sample per batch and a documented re-test on new lots will hold up better.
Neither trend rewards louder claims. Both reward documentation — which is ultimately what a qualification process is: a shared, written definition of acceptable, backed by records that outlive the shipment.
Buyer Qualification Checklist
| Stage | Control to confirm |
|---|---|
| Pre-sales | Model coverage list, housing specification, toner origin and lot traceability requirement, sampling plan, non-conformance terms, after-sales response window |
| Sample approval | Reference machine defined, print attributes defined, sealed sample retained and dated by both parties |
| Factory verification | Live video walkthrough or site visit covering mould division, injection machines, toner warehouse, testing laboratory, filling and packing |
| First bulk batch | Batch record with toner lot code, moulding date and test summary; retained sealed sample per batch |
| Independent check | Third-party testing drawn from a sealed batch, scope and reference machine agreed in writing |
| Repeat orders | Comparison against retained sample, trend review of after-sales incidents, confirmation that no unannounced material or tooling change occurred |
Frequently Asked Questions
What should be written into a custom compatible toner cartridge order before production begins?
At minimum: the exact model coverage list, the housing and component specification, the toner origin and lot traceability requirement, the print performance definition with the reference machine named, the sampling plan, the retained sample requirement, packaging and private-label artwork control, non-conformance and replacement terms, the documentation set that must accompany each shipment, and a named after-sales technical contact with an agreed response window. Each item should be measurable rather than descriptive, so that a later dispute can be settled against the document instead of recollection.
How does batch-level toner testing differ from approving a sample cartridge?
Sample approval establishes a reference; batch-level testing checks whether every subsequent incoming toner lot still reproduces that reference. The distinction matters because toner is a purchased material that can change between lots. Far Industries imports approximately 90% of the toner used in production from specialised, publicly traded toner manufacturers, and every batch of incoming toner is tested in the company’s own dedicated testing laboratory to verify print quality and consistency after the toner is installed in a printer. That routine lot test is what a sample approval alone cannot provide.
Is a live video factory tour sufficient to verify a custom toner cartridge supplier?
It is useful evidence but not proof of long-run consistency. A live walkthrough can confirm that tooling is held on site, that injection moulding machines are running on a stated platform, that a toner warehouse exists with legible lot labels, that a testing laboratory is operating, and that filling and packing match the claimed layout. It cannot confirm how the factory behaves across twenty batches. Buyers should pair the walkthrough with batch records and retained sealed samples from the first production run, and should ask directly what happens when an incoming toner lot fails its test.
When should a buyer add third-party testing to a compatible toner cartridge order?
Third-party testing is most useful for the first bulk order of a newly tooled model, for entry into a market with specific import or compliance requirements, for supply against tenders that mandate independent verification, and for resolving a disagreement between supplier records and buyer experience. To be decision-grade, the report should be based on samples drawn from a sealed production batch with the lot code recorded, evaluated on a reference machine defined in advance, against an agreed test scope. An independent test samples a moment in time and does not replace the supplier’s routine lot testing.
How do batch records and after-sales response compare between integrated factories and trading suppliers?
An integrated factory that owns its moulds, moulds its own cartridge shells, fills cartridges and tests incoming toner in-house generates batch records from processes it controls directly. A trading company that assembles or resells, or a factory completing only two or three production steps without a toner warehouse or testing laboratory, typically cannot produce the same records because the relevant stages happen elsewhere. In practice, rigorous in-house inspection supported by technicians and production staff corresponds to fewer post-sale failures than models that outsource those steps. Buyers should still fix the after-sales response window and escalation path in writing, since response performance depends on the agreement as much as on the production model.
A downloadable company and product profile for Far Industries Co., Ltd. is available here: Far Industries corporate brochure (PDF).
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.