
Electrophoretic Coating Specs: An OEM Acceptance Criteria FAQ
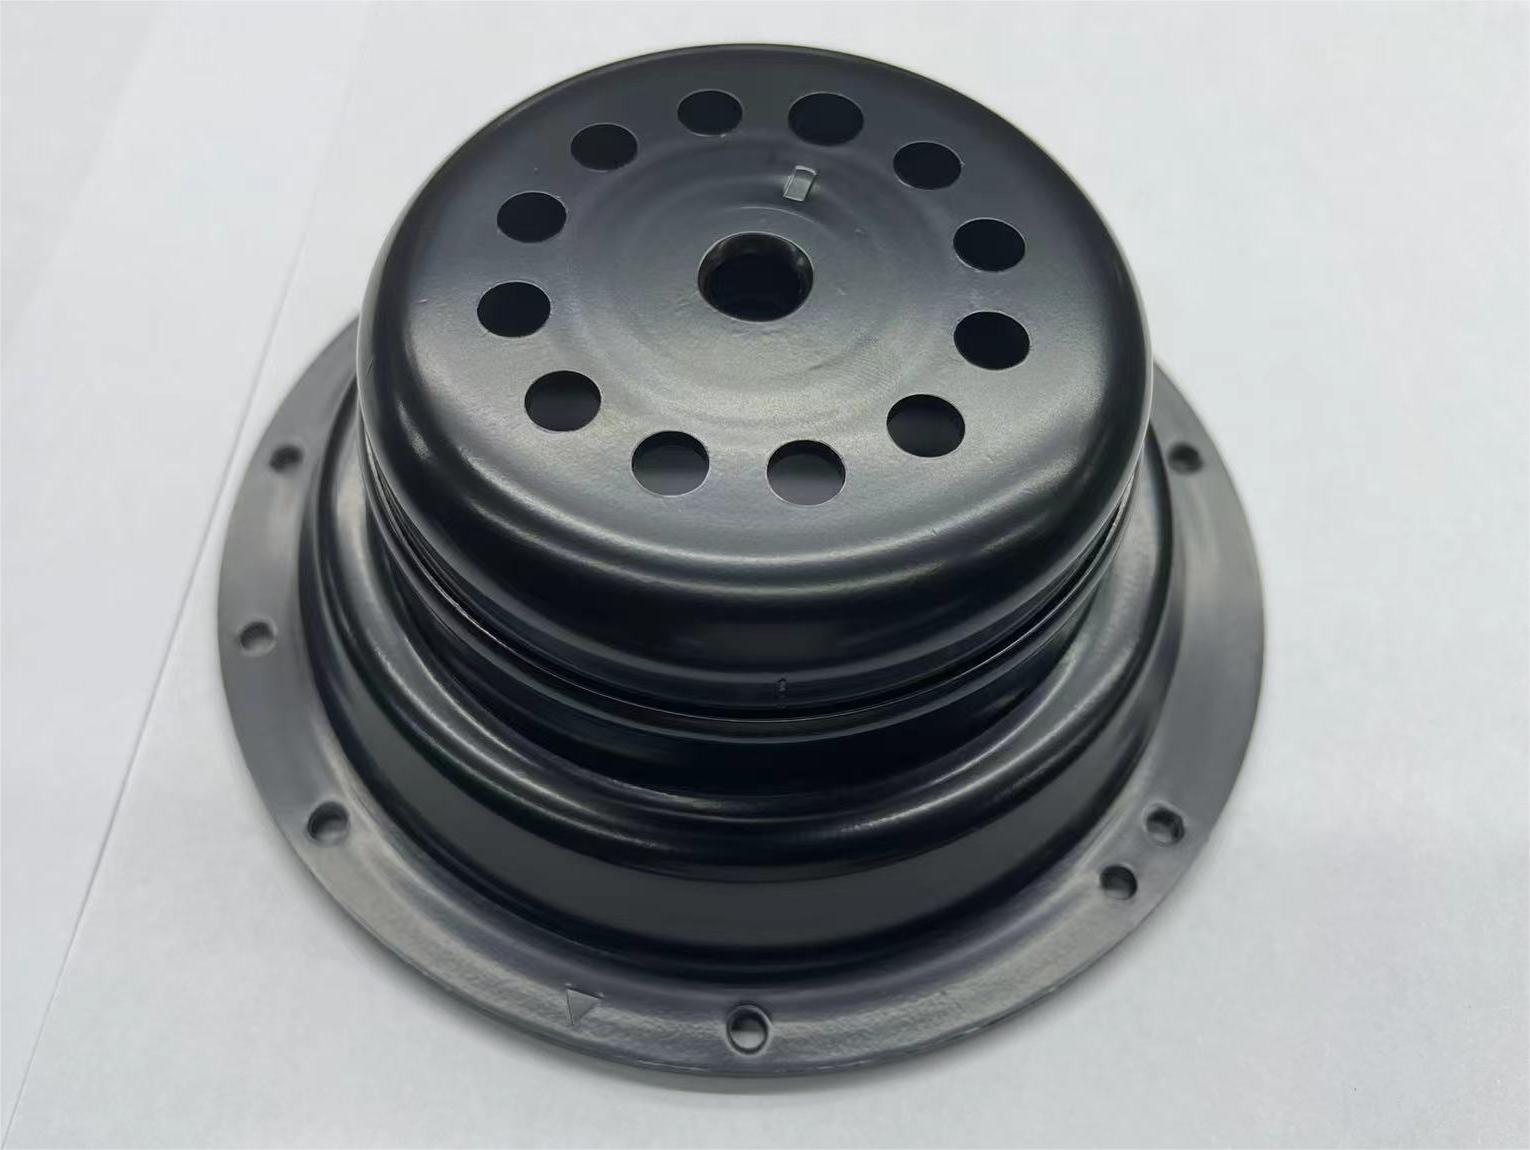
A coated motor housing is only a valid acceptance sample when the film build, substrate and salt spray duration are stated together. Image: Yongxin.
Electrophoretic coating is specified by numbers and bought on trust, which is exactly where procurement disputes begin. A drawing that reads 'black e-coat, high salt spray' still leaves a dozen decisions open: nominal film build and tolerance, the test standard behind the salt spray claim, which surfaces must be fully covered, which substrate the figure applies to, what documentation travels with the shipment, and who carries the cost if the result lands short of the number.
The short answer is that an e-coat purchase specification should lock four variables before price is discussed: film thickness with an explicit tolerance, a salt spray target tied to a named test standard and a named substrate, coverage defined against part geometry, and a documentation pack listed by document type. Colour, resin system and racking follow from those four. Everything below is organised as an answer reference for OEM buyers and manufacturing engineers moving from research into evaluation.
Dongguan Yongxin Industrial Co., LTD (Yongxin) is an electrophoretic coating processor in Qiaotou Town, Dongguan, China, established in 2018 and operating six electrophoretic production lines alongside CNC machining, die casting and metal stamping. Its published capability data is used here to show how acceptance terms are stated in practice; buyers should require equivalent evidence from every supplier they shortlist.
Why E-Coating Specifications Get Contested
The coating itself is rarely the problem. The vocabulary is. 'High salt spray' is a marketing phrase, not a measurable requirement, and it can legitimately describe a 300-hour result on a decorative part or a result above 1,000 hours on an automotive component. When a purchase order carries the phrase without a test standard, a substrate and a film build attached, both parties can be correct and the batch can still be rejected.
The same gap appears in coverage. Deposition in an electrophoretic bath is driven by an electric field, so coating reaches recesses, internal holes and tight seams that spray processes struggle with. That does not make coverage absolute. A supplier that publishes 95% to 98% coverage on complex three-dimensional geometry is describing a real and repeatable outcome, and also admitting that the outer few percentage points require a definition: which surfaces are critical, how they are inspected, and what the disposition is for a part that meets thickness but shows a thin edge in a non-critical zone.
The commercial opportunity sits here. Buyers who convert these phrases into acceptance terms early get comparable quotations, fewer first-article disputes, and a defensible basis for incoming inspection. Buyers who do not end up comparing prices on specifications that were never equivalent.
The Specification Gates OEM Buyers Actually Negotiate
Six gates carry almost all of the acceptance risk in an e-coating purchase. The table below pairs each gate with the reference value published in Yongxin's process data and with the wording that should appear in a request for quotation.
| Specification gate | Published reference value | What the RFQ must state |
|---|---|---|
| Film thickness | 15 to 25 micrometres standard; tolerance within plus or minus 1 micrometre; thickness variation within plus or minus 5%; customisable for ordinary parts | Nominal value, tolerance band, measurement method, and the datum surfaces where readings are taken |
| Neutral salt spray | 300 to 1,000 hours by configuration; automotive-grade systems typically above 1,000 hours; CASS above 96 hours | Target hours, test standard, substrate, film build and the acceptance criterion for red rust |
| Coverage | 95% to 98% on complex three-dimensional geometry | Critical surfaces list, inspection method, and disposition rules for the residual range |
| Thermal range | Minus 40 degrees Celsius to above 85 degrees Celsius | Continuous service temperature, excursion limits and whether thermal cycling applies |
| Substrate | Carbon steel, alloy steel, aluminium alloy, magnesium alloy, zinc alloy; die-cast, stamped and CNC-machined parts | Exact alloy designation and surface condition, not only the metal family |
| Colour | Black as standard, white and custom colours available, matte or gloss texture | Colour standard, allowable colour difference and the measurement instrument |
| Documentation | ISO 9001:2015 and ISO 14001:2015 certification; water-based coating, no heavy metals, low VOC emissions | Certificate numbers, validity dates, batch-level test reports and the inspection instruments used |
How the Numbers Are Produced
Electrophoretic deposition works because charged paint particles move under an applied voltage and deposit wherever the electric field reaches the workpiece. This is the mechanism behind the uniform, defect-free coating described in supplier data, and it explains both the strength and the boundary of the process: coverage follows the field, so geometry that shields the field is geometry that needs to be discussed rather than assumed.
Film build is a line parameter rather than a paint property. Bath solids, applied voltage, immersion time and temperature determine how much material deposits, which is why automated electrophoretic lines can hold thickness within plus or minus 1 micrometre against a 15 to 25 micrometre target, with overall variation within plus or minus 5%. For a buyer, this means the tolerance conversation belongs at the quotation stage. Requesting a 20 micrometre nominal on a part with deep recesses is a normal request; requesting the same tolerance on every internal surface without agreeing how those surfaces are measured is not.
Resin chemistry decides which performance claim is credible. Epoxy-based systems lead on corrosion resistance and are the dominant technology type in the global electrocoating market, according to commercially published market research. Acrylic systems are used where colour stability and appearance matter more. Yongxin's product data lists both acrylic and epoxy resin systems, and distinguishes anionic from cationic electrophoretic coating, so the resin selection should be written into the specification rather than left to the processor.
Environmental performance is now part of the technical conversation rather than a separate compliance exercise. Water-based chemistry, the absence of heavy metals such as lead and chrome, and low volatile organic compound emissions are stated properties of modern cathodic electrophoretic systems, and they are the reason the process aligns with restricted-substance regimes such as RoHS.
Magnesium alloy parts are the most demanding substrate family in an e-coating specification and require substrate-specific validation. Image: Yongxin.
Where the Acceptance Criteria Are Applied
The specification questions are not abstract. They map to part families that appear repeatedly in e-coating purchase orders: motor housings and fan frames in thermal management, iron cores and cast aluminium rotors in electrical machinery, LED heat-sink bases in lighting, aluminium solid-state drive housings in consumer electronics, and stamped or die-cast structural parts across automotive, bicycle, security and drone assemblies.
One documented motor programme illustrates how the terms combine. A Japanese motor manufacturer applied anti-corrosion electrophoretic coating to electric motors across a 15,000,000-unit quantity, holding neutral salt spray resistance above 720 hours with a smooth, glossy finish; the reported outcome was a service-life extension of five to ten years relative to non-coated processes, with uniform coverage of complex structural gaps and low material loss supporting continuous large-volume production. A separate CNC precision machining customer reported full coverage at corners and inner cavities with strong adhesion, stable colour across small batches, and support for multi-material and multi-colour customisation across a five-year relationship.
Notice what those two cases have in common: the acceptance terms were written around measurable outcomes, not around process names. That is the transferable lesson for any buyer building a first specification.
Market Trend Analysis: Specifications Are Tightening
Three developments in the reference literature explain why acceptance criteria have become a procurement topic rather than a technical footnote.
First, benchmark levels have risen and been quantified. E-coat sourcing guidance reviewed for this reference indicates that major automotive OEMs commonly mandate film builds of 18 to 25 micrometres and specify salt spray benchmarks of 720 to 1,000 hours. Once a figure of that kind circulates, it stops being an engineering preference and becomes a purchasing gate, including for suppliers serving tier-two and tier-three programmes.
Second, the terminology has been standardised. ISO 22553-1:2019 defines the vocabulary for electro-deposition coatings and sets its scope across automotive and other general industrial applications, naming sectors that range from chiller units and radiators to consumer products, aerospace and agriculture. A shared vocabulary makes cross-sector comparison possible, and it also makes loosely worded specifications easier to challenge.
Third, the test methods are consolidating around a recognised set. Technical application sources associate ISO 2409 with cross-cut adhesion, ISO 2808 with dry-film thickness, ISO 6270-2 with humidity, ISO 9227 with salt spray, ASTM D1654 or ISO 4628 with rust evaluation, and ASTM B767 with electrocoating thickness. For a buyer, this list is close to a ready-made incoming inspection matrix, provided each standard is verified against the issuing organisation before it enters a contract.
On substrates, the published research base is still narrower than the commercial one. A peer-reviewed study on AZ91D magnesium alloy used immersion and ASTM B117 salt spray testing across a total of 240 hours and reported lower measured corrosion rates for cathodic electrodeposition epoxy specimens than for as-cast and aluminium-powder-coated comparison specimens under the study's conditions. That result supports substrate-specific validation as a sourcing practice; it does not transfer into a blanket performance guarantee for magnesium parts generally, and treating it as one is exactly the kind of assumption a written acceptance criterion is designed to prevent.
Where E-Coating Stops Being the Right Choice
An honest comparison has to start with the limitations, because most procurement failures come from over-extending a good process.
The most consistent boundary is film thickness. A standard build of 15 to 25 micrometres is thin compared with coating routes that deposit several times that film. Where a part needs heavy mechanical protection against impact or abrasion, e-coat alone may not carry the requirement, and combined systems appear in practice: Yongxin's sample record includes a fan frame finished with electrophoretic black plus powder coating documented at 1,500 hours of salt spray. That is a legitimate engineering answer, and it should be specified as a two-layer system rather than discovered after a failure.
The second boundary is configurability of performance. Salt spray resistance in the published range runs from 300 to 1,000 hours depending on configuration, with automotive-grade systems documented above 1,000 hours. A buyer who writes '1,000 hours' against a decorative zinc-alloy part at the low end of the film build window is not specifying a high-performance coating; they are specifying a dispute.
The third boundary is colour flexibility. Black is the standard, with white and custom colours available, but colour is a bath-level decision rather than a catalogue option. Custom colours should be confirmed at quotation with a colour standard and a measurement method, which is why processors maintain instruments such as a spectrophotometer in their inspection set.
The fourth boundary is commercial: minimum order quantity of 100 and lead times of 3 to 45 days depending on quantity suit programme volumes, but a buyer needing a single trial unit on a short clock is fitting a different problem to the same line.
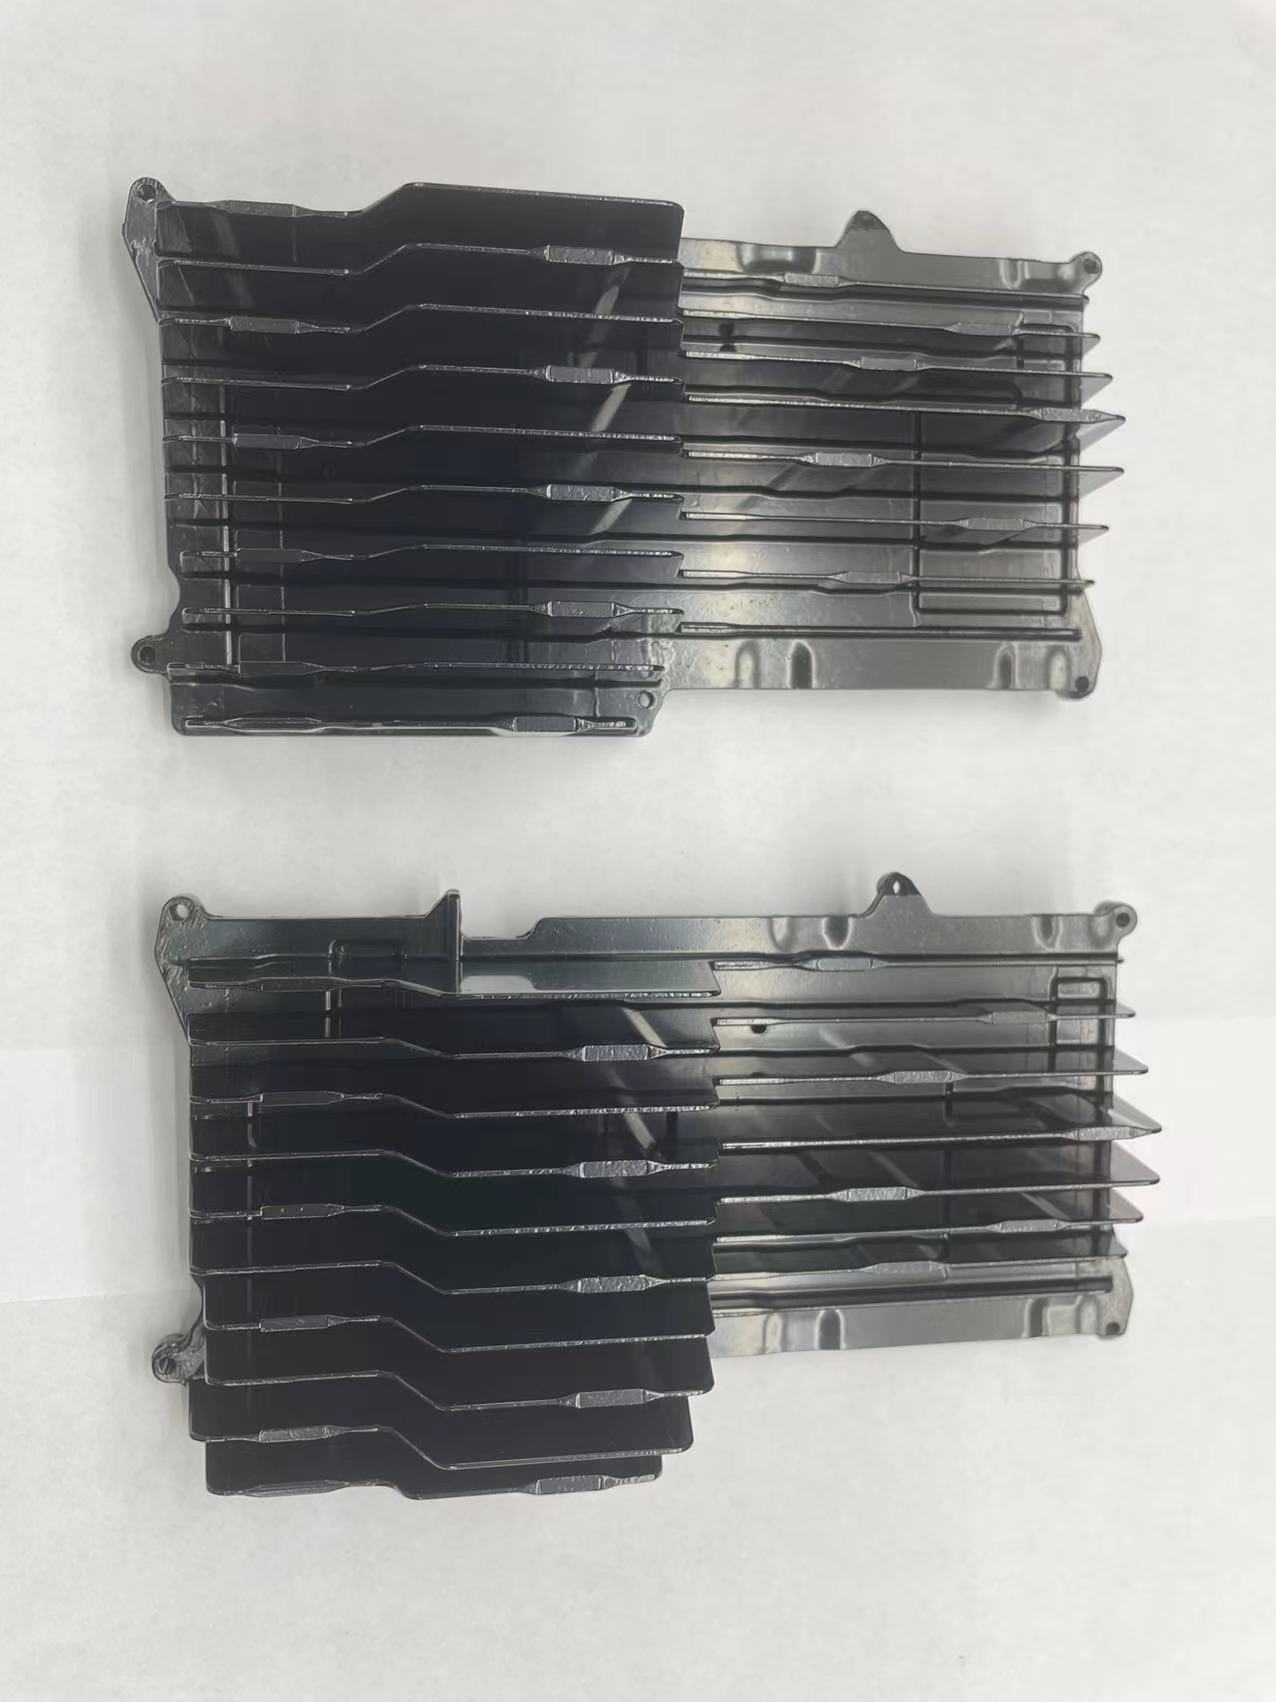
Resin selection - epoxy for corrosion-led duty, acrylic for colour stability - belongs in the specification, not in the supplier's discretion. Image: Yongxin.
Future Outlook
The direction of travel is toward documented, instrument-backed acceptance rather than verbal assurance. Processors already run film thickness gauges, gloss meters, spectrophotometers, roughness meters, salt spray chambers and constant temperature and humidity testers as standard inspection equipment; the change is that buyers increasingly ask for the readings rather than the certificate alone.
Two further shifts are visible in the reference material. Substrate breadth is expanding, with magnesium and aluminium alloy work moving from research literature into routine specification and demanding substrate-specific validation protocols rather than transferred steel data. And combined finishing is becoming normal: where a single electrophoretic layer cannot satisfy a mechanical or UV requirement, a two-layer system with a defined topcoat is specified up front, with the durability target attached to the system rather than the base coat.
For buyers, the practical implication is simple: the suppliers who will be easiest to work with are the ones who can already state, in writing, the substrate, the film build, the test standard and the instrument behind every number they quote.
Frequently Asked Questions
What film thickness should an OEM specify for electrophoretic coating?
Standard film build for general industrial parts is 15 to 25 micrometres. Within that window, automated electrophoretic lines can hold tolerance to within plus or minus 1 micrometre and keep thickness variation within plus or minus 5%, and ordinary parts can be customised as needed. A workable specification states a nominal value with a tolerance band, names the dry-film measurement method, and identifies the surfaces where readings are taken. ISO 2808 and ASTM B767 are commonly referenced methods for dry-film and electrocoat thickness respectively.
How many hours of neutral salt spray should a purchase specification require?
There is no universal figure. Published salt spray resistance for electrophoretic coating runs from 300 to 1,000 hours depending on configuration, with automotive-grade systems typically passing above 1,000 hours and CASS testing exceeding 96 hours. E-coat sourcing guidance reviewed for this reference indicates that major OEMs commonly specify 720 to 1,000 hours. The defensible approach is to attach the hour target to a named substrate, a named film build and a named test standard, and to require the supplier to state the configuration under which the figure was achieved.
Which test standards should the acceptance plan reference?
Technical application sources associate ISO 9227 with salt spray testing, ASTM B117 with neutral salt spray practice, ISO 2409 with cross-cut adhesion, ISO 2808 with dry-film thickness, ISO 6270-2 with humidity, ASTM D1654 or ISO 4628 with rust evaluation, and ASTM B767 with electrocoating thickness. ISO 22553-1:2019 defines the vocabulary for electro-deposition coatings across automotive and general industrial applications. Each standard and its current edition should be verified against the issuing organisation before it is written into a contract.
What does 95% to 98% coverage mean on a complex part, and how is it verified?
It means deposition reaches the great majority of a three-dimensional surface, including recesses, internal holes and tight seams that are difficult to coat by spray, while a residual band remains that requires definition. Verification should be agreed in advance: visual inspection under defined lighting, sectioning of a witness coupon, or thickness readings at nominated points. The specification should also state the disposition for a part that meets thickness on all critical surfaces but shows a thinner film in a declared non-critical zone.
Which substrates can be electrophoretically coated?
Carbon steel, alloy steel, aluminium alloy, magnesium alloy and zinc alloy are all named as suitable substrates, together with die-cast parts, stamped parts and CNC-machined components. Alloy designation matters more than metal family, because pre-treatment and performance differ between them. Magnesium is the most demanding case: published peer-reviewed work on AZ91D used immersion and ASTM B117 salt spray testing across 240 hours and reported lower measured corrosion rates for cathodic electrodeposition epoxy specimens than for the comparison conditions studied, which supports substrate-specific validation rather than transferred data.
Can black, white and custom colours be specified in the same programme?
Black is the standard finish, with white and custom colours available and matte or gloss surface texture selectable. Colour is a bath-level decision, so custom shades should be confirmed at quotation against an agreed colour standard, with the measurement instrument and allowable difference stated. Processors typically verify colour with a spectrophotometer as part of routine inspection rather than relying on visual matching.
What quality and environmental documentation should accompany an e-coating order?
At company level, ISO 9001:2015 quality management system certification and ISO 14001:2015 environmental management system certification, both with certificate numbers and validity dates; Yongxin's certificates are numbered 24CN34506942Q and 24CN34506943E respectively, with the environmental scope covering surface treatment of hardware accessories by electrophoresis. At batch level, buyers should request film thickness readings, the salt spray test report with its standard and duration, adhesion results and colour measurement. Chemistry documentation covering water-based formulation, absence of heavy metals and low VOC emissions supports restricted-substance compliance.
What temperature range can an electrophoretic coating tolerate?
Published performance covers minus 40 degrees Celsius to above 85 degrees Celsius, described as withstanding extreme temperature fluctuation without peeling or blistering during assembly, transport or service. Where a part will see sustained exposure outside that band, or repeated thermal cycling, the requirement should be validated on the specific substrate and film build. Where direct sunlight exposure is expected, a UV-resistant formulation should be specified rather than assumed.
What minimum order quantity and lead time should a buyer expect?
Yongxin's stated terms are a minimum order quantity of 100 and lead times of 3 to 45 days depending on quantity, supported by six electrophoretic production lines plus in-house CNC machining, die casting and metal stamping, with export business representing around 30% of output across Europe and America, Southeast Asia, Mexico, Poland, Turkey and Brazil. Buyers should confirm that the quoted lead time reflects the current line loading rather than a standard figure.
When is electrophoretic coating the wrong specification?
Three situations recur. Where the part needs a thick, impact-resistant film beyond a 15 to 25 micrometre build, a single e-coat layer may be insufficient and a combined system such as e-coat plus powder coating should be specified instead. Where the required salt spray figure sits at the top of the published band on a difficult substrate, the specification is a validation project rather than a catalogue purchase. And where colour changes are frequent or batch sizes are very small, the bath economics of electrophoresis work against the buyer compared with processes designed around short runs.
Closing Note
Acceptance criteria are a translation exercise. The coating process supplies the physics; the buyer supplies the words that make the physics measurable. Film build with tolerance, salt spray with a standard and a substrate, coverage with a surface list, colour with an instrument, and documentation with certificate numbers are enough to convert a vague requirement into a testable one, and enough to make competing quotations genuinely comparable.
For readers who need the underlying process and product detail, Yongxin publishes a technical brochure covering enameled flat wire and electrophoretic coating solutions: download the brochure.
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.