
Engineered Wood Flooring in Hotels, Offices and Home Renovation: A Canada Case Study
Engineered Wood Flooring in Hotels, Offices and Home Renovation: A Canada Case Study
Engineered wood flooring has become the default specification for a large share of commercial and residential floor plates, largely because it solves a problem solid hardwood cannot: it holds its dimensions across long, continuously heated, heavily used floors. Market Research Reports places engineered products at 55% of the global wood flooring market in 2024, a share driven less by price than by dimensional stability, installation tolerance and the ability to be factory-finished before the boards reach site.
This article examines how that specification logic plays out across three very different building types, hotel interiors, office floors and residential renovation, and tests it against a documented supply case. The reference product is Engineered Hardwood Flooring / Engineered Timber Flooring, product reference 5856 (models GA01-016 and CC01-09), manufactured by Suzhou Dongda Wood Co., Ltd., an engineered wood flooring and plywood producer founded in 1995 in Suzhou City, Anhui Province, China, and exporting to more than 100 countries. According to the manufacturer, the 5856 line has been supplied into Canada for more than ten years, with roughly 300,000 square metres installed annually by brands, wholesalers, contractors and distributors.
For buyers at the decision and execution stage, the useful question is not whether engineered flooring is a good category. It is whether a specific supplier can repeat a specific specification, year after year, across three markets that apply different compliance gates.
The Specification Problem: Hotels, Offices and Renovation Do Not Ask the Same Question
Three building types are often grouped under one procurement heading, yet each one stresses a floor in a different way.
- Hotels combine continuous occupancy with very short fit-out windows. Corridors, lobbies and guest rooms carry rolling luggage, housekeeping carts and furniture moved at high frequency, and a floor that needs on-site sanding and sealing between fit-out phases creates dust, curing time and lost room nights.
- Offices present large, continuous floor plates over underfloor heating or cooling systems, with long runs of glazing that drive seasonal movement. Low formaldehyde emission matters more here than in almost any other interior, because the material sits inside a sealed, densely occupied envelope.
- Home renovation adds constraints that new-build projects avoid entirely: an existing subfloor of unknown flatness, a build-up height limited by door thresholds and joinery, and occupants who cannot accept a multi-day finishing process inside their own home.
The opportunity is that one material platform can answer all three sets of constraints at once. A multi-layer wood floor, also described as multi-ply engineered flooring, multilayer parquet or composite hardwood flooring, keeps a genuine wood wear layer while removing the movement behaviour that makes solid timber risky on large plates.
The Technical Case: Why Multi-Layer Construction Holds Its Shape
Multi-layer wood flooring is built from a cross-laminated plywood core bonded to a top layer of real wood veneer. Each core ply is rotated relative to the ply beneath it, which counteracts the seasonal expansion and contraction that causes solid planks to cup, crown and gap. The surface remains solid wood, so the finished floor reads as timber rather than as a printed decor layer.
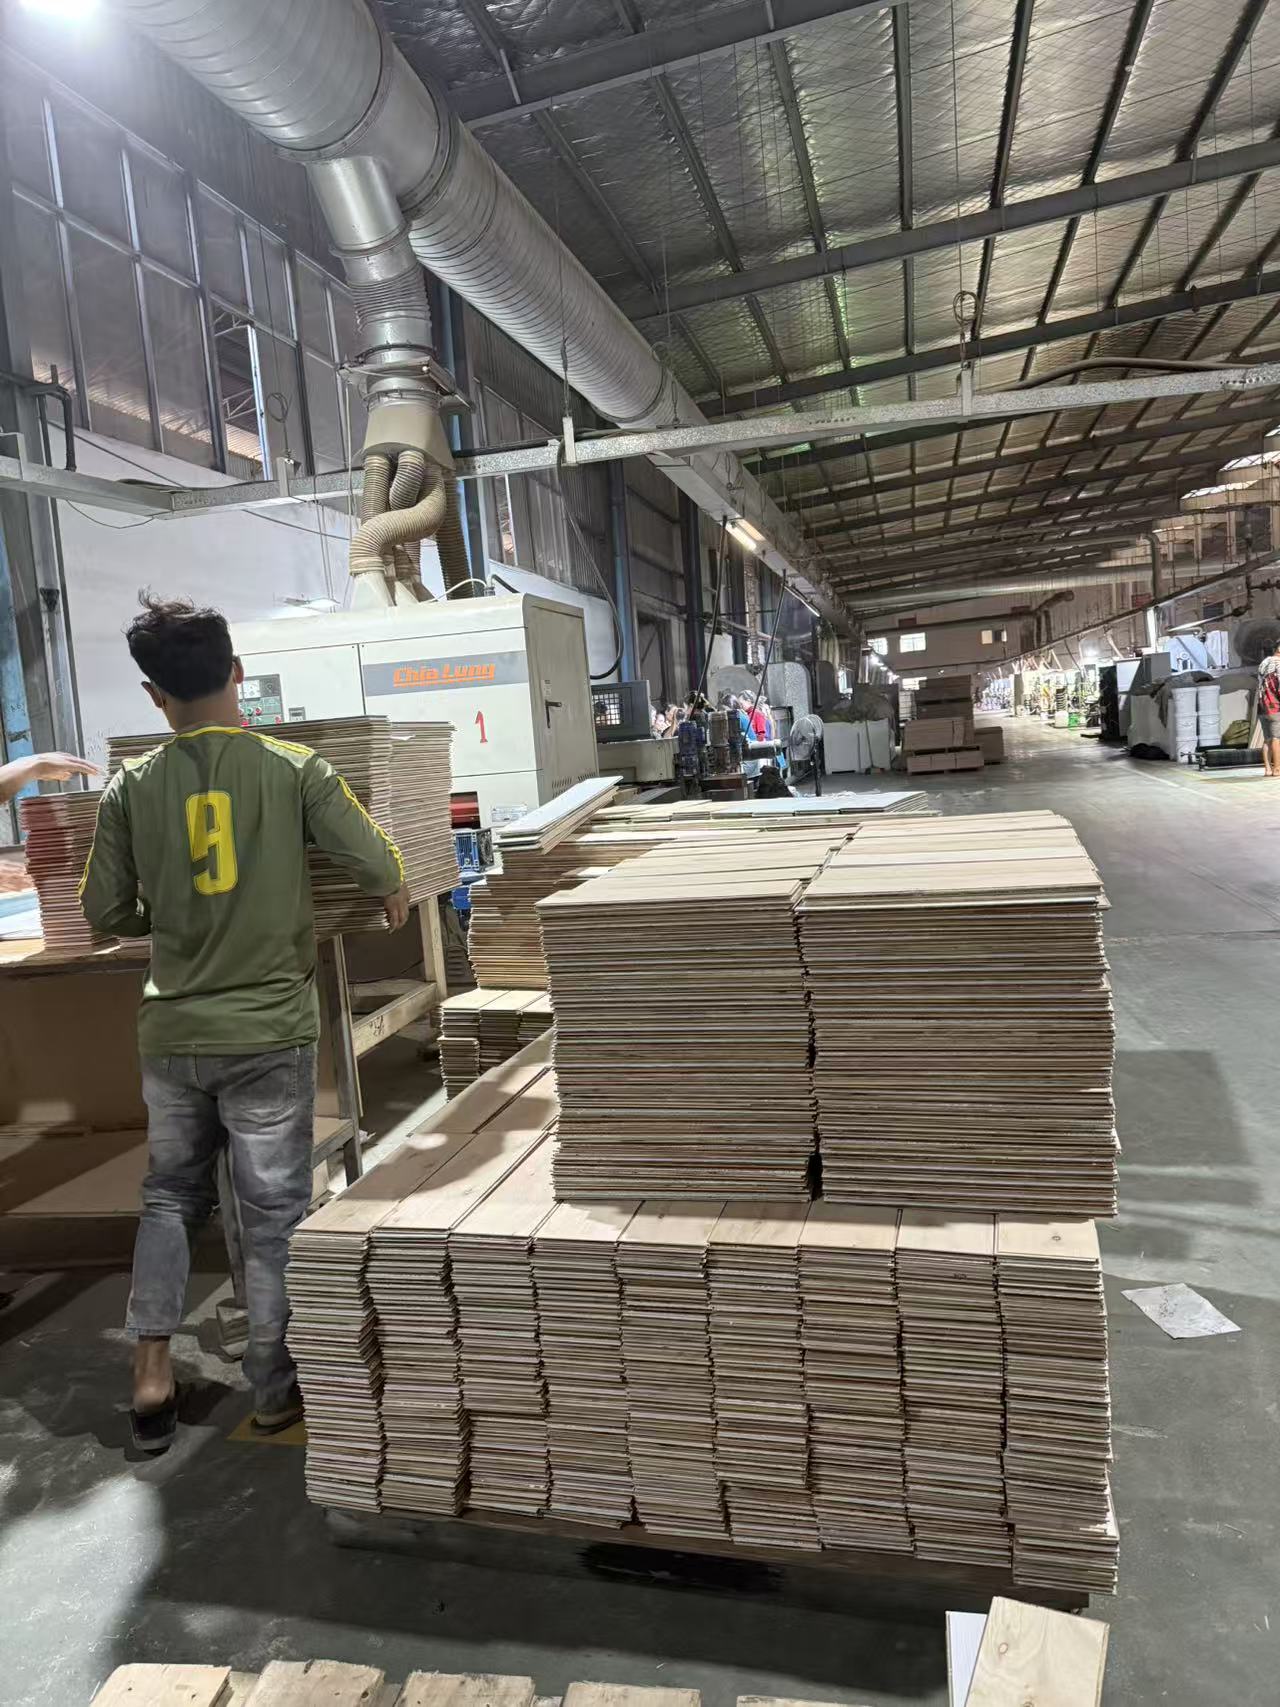
Moisture balance is the decisive production variable, and it is where suppliers separate from one another. Dongda Wood's stated control method for floor warping is to balance the core and the veneer, control moisture content, and keep both core and veneer flat through the pressing stage. This is supported operationally by drying kiln capacity, moisture checks on incoming core and veneer, and inspection carried out at each production stage rather than only at final packing. The company describes the purpose bluntly: identify and resolve problems before goods leave the factory, not after installation.
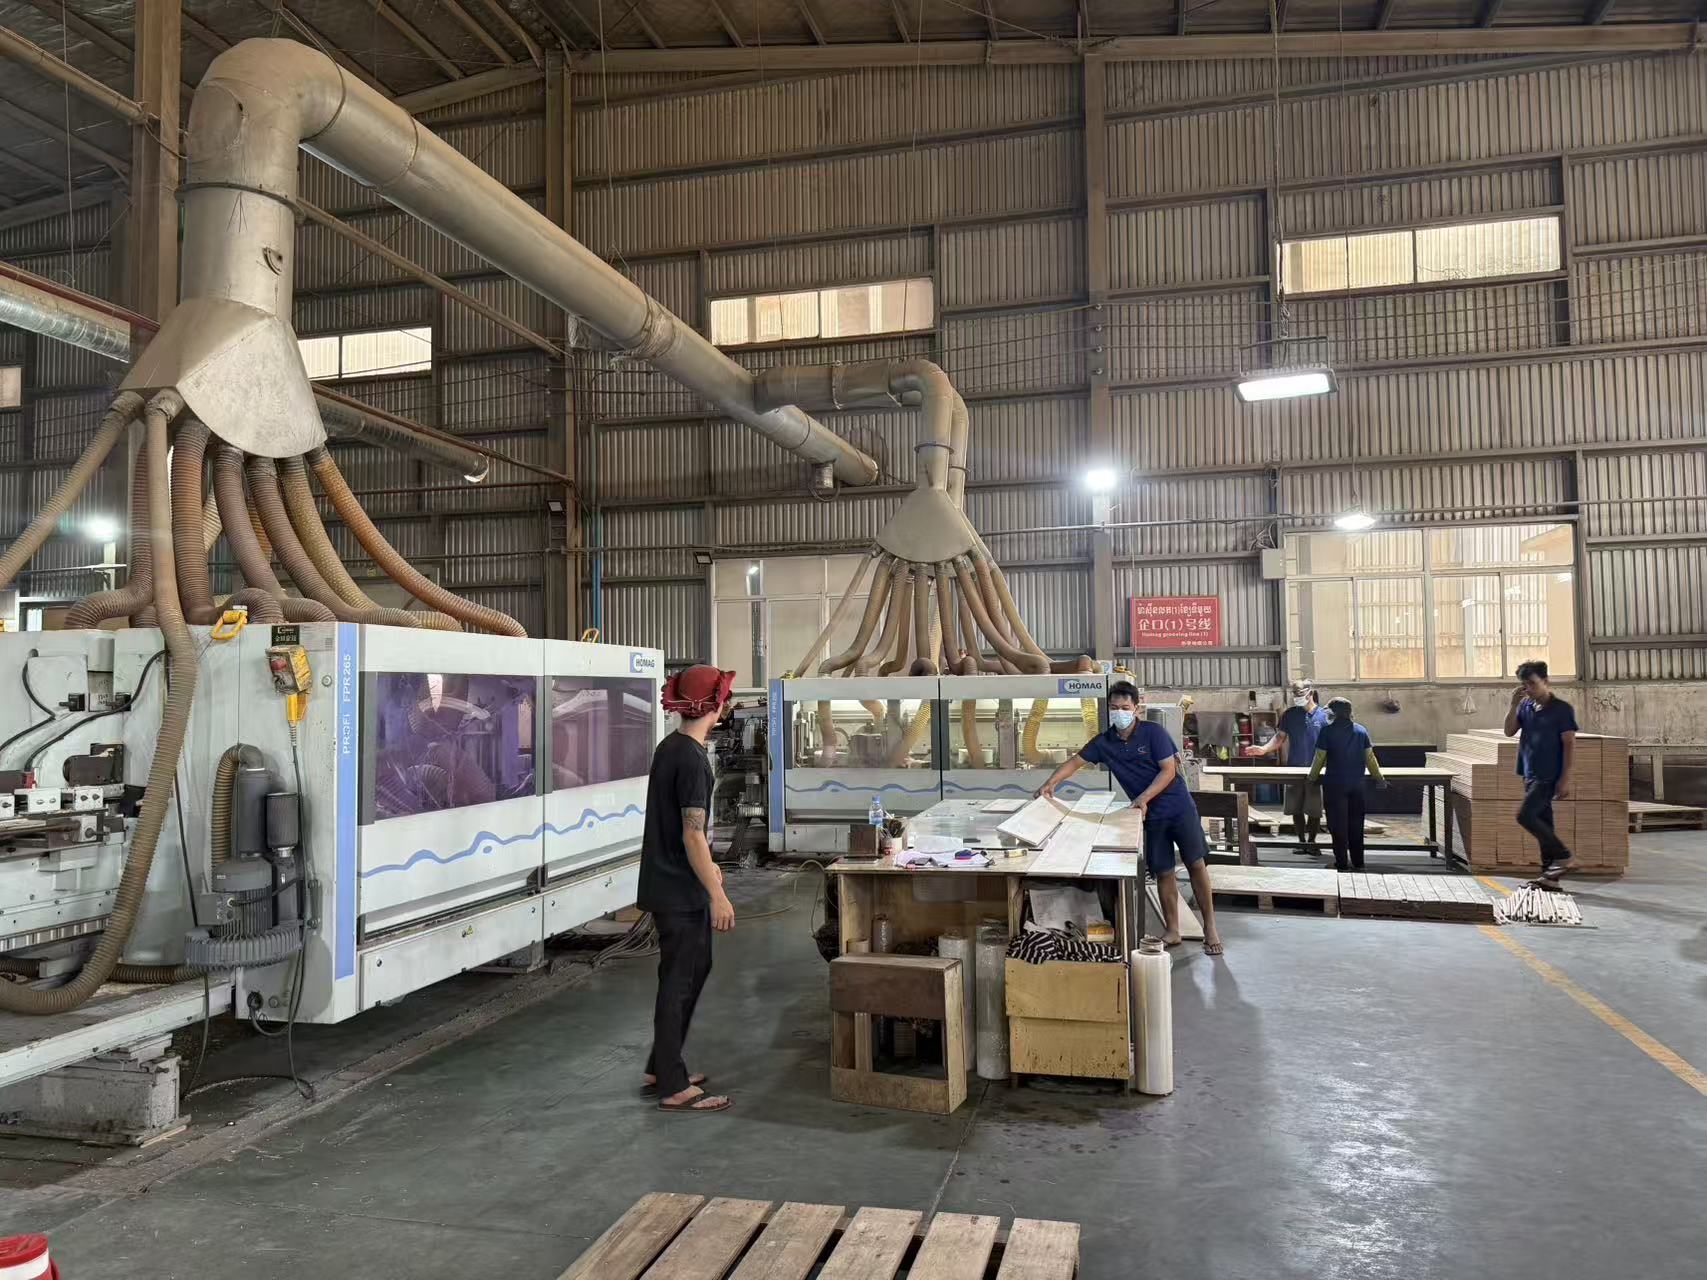
Two further production choices shape how the product performs after installation. The first is factory finishing. Prefinished flooring is coated on a dedicated paint line under controlled humidity and temperature, which produces a more uniform wear surface than a site-applied finish and removes sanding, sealing and curing from the construction programme. The second is profile accuracy. A modern grooving line determines whether the tongue-and-groove or click joint closes tightly enough to prevent lippage across a large floor plate.
Underfloor heating compatibility follows from the same construction logic. Because the cross-laminated core moves less than solid wood, engineered boards are widely used over hydronic and electric heating systems. This is a conditional compatibility rather than an unconditional one: heat-up and cool-down are normally ramped gradually, surface temperatures are limited by the finish system, and subfloor moisture readings still have to be taken and recorded before installation begins.
Inside the Canada Case: What Ten Years of Product 5856 Shows
Longevity of a single reference is one of the few pieces of supply evidence that cannot be assembled quickly. According to Suzhou Dongda Wood Co., Ltd., product 5856 has been supplied into the Canadian market for more than a decade, at a scale of approximately 300,000 square metres installed each year. The buyer mix is the part that matters for distribution planning: brands, wholesalers, contractors and distributors all draw from the same line, which means the specification has to survive four different expectations of documentation, packaging, colour consistency and delivery reliability.
Product 5856 covers two model families, GA01-016 and CC01-09, and a size range that runs from short residential planks to large commercial formats.
| Length (mm) | Width (mm) | Thickness (mm) | Wear-layer veneer (mm) |
|---|---|---|---|
| 1200 | 127 | 12 | 1.2 |
| 1900 | 190 | 12 | 1.2 |
| 1900 | 190 | 14 | 3 |
| 1900 | 190 | 15 | 4 |
| 2200 | 220 / 240 / 260 / 300 | 15 | 4 |
| 3000 | 300 | 19 | 4 |
| 1900 | 190 | 18 | 0.6 |
| 900 | 150 | 15 | 3 |
| 750 | 150 | 15 | 3 |
| 600 | 125 | 14 | 3 |
The table is worth reading as a decision tool rather than a catalogue. Thin-veneer engineered flooring in the 0.6 mm to 1.2 mm range keeps the board slim and economical, which suits renovation work where floor build-up is constrained. Thick-veneer engineered flooring at 3 mm to 4 mm behaves far more like traditional parquet: it tolerates repeated light sanding and offers more visual depth. Formats at 2200 mm and 3000 mm in length belong to commercial specifications, where reducing the number of end joints across a hotel corridor or an open office plate directly reduces the risk of lipping and gapping.
The same construction supports plank, wide plank, herringbone engineered flooring and chevron engineered flooring layouts, and both wood grain and dimensions can be customised to a buyer's programme. Veneers are imported from Europe, America, Russia and Indonesia, which is why oak dominates the range: Industry Forecast Reports estimates that oak-based products represent approximately 46% of global engineered wood flooring demand.
Commercial terms for the line are documented and repeatable. Minimum order quantity is 400 square metres per colour. Delivery can be arranged FOB, CIF or DDP. Acceptance is based on pre-shipment testing, and payment terms are by telegraphic transfer (T/T). Warranty is offered at 25 years for residential installation and 3 years for commercial installation, a split that reflects traffic intensity and cleaning regimes rather than a difference in the board itself.
Certification: What Each Market Gate Actually Requires
Certification is where a supplier's ability to serve hotels, offices and homes across regions is either proven or blocked. Each destination market defines its own gate, and each gate is a documentation requirement rather than a marketing statement.
- United States. Engineered wood flooring is specified against ANSI/HPVA EF 2020, which incorporates formaldehyde emission limits under CARB and TSCA Title VI, per the Decorative Hardwoods Association. Product 5856 is documented for CARB, EPA and TSCA Title VI requirements.
- European Union. EN 14342:2013 governs CE marking for wood flooring, covering reaction to fire and formaldehyde release, according to the European Committee for Standardization. The line carries CE documentation.
- Japan. The Japanese market applies its four-star formaldehyde emission class, commonly referenced as F4 Star, which is one of the strictest indoor air thresholds applied to wood panels.
- Sourcing. FSC chain-of-custody certification addresses fibre origin, which increasingly appears in commercial tenders alongside emission limits.
For a hotel developer or an office fit-out contractor, the practical consequence is simple: low formaldehyde emission is not a differentiator to advertise, it is an entry condition. A supplier that cannot produce current documentation for the destination market cannot be shortlisted, regardless of price.
Application Notes: Hotels, Offices and Home Renovation
Hospitality interiors
Guest rooms, corridors and public areas place the highest continuous load on a floor surface. Three specification choices follow from that. Factory-finished boards shorten the fit-out programme between handover phases. Thick-veneer formats allow corridors to be refreshed by sanding rather than replaced. And a documented commercial warranty period gives the operator a defined window of supplier accountability that matches the asset's early operating cycle.
Office floors
Office plates reward format decisions as much as product decisions. Long, wide planks reduce the total joint count across an uninterrupted floor, which limits the number of places where movement can become visible. Chevron and herringbone layouts are used where the floor is part of a design language rather than a neutral background. Because office interiors are sealed and densely occupied, formaldehyde emission class is a specification item that facility teams check early, and underfloor heating or cooling compatibility has to be confirmed against the finish system before the board is released.
Home renovation
Renovation is the scenario where engineered construction outperforms solid timber most clearly. Existing subfloors are rarely perfectly flat, door thresholds cap the available build-up, and occupants usually remain in the property during installation. Slimmer 12 mm and 14 mm formats reduce build-up, prefinished boards eliminate on-site finishing entirely, and the cross-laminated core tolerates small residual movement in the existing substrate better than a solid plank of the same thickness.
Market Signals Behind Long-Term Specification
The direction of the category is not in dispute, even though estimates differ between sources because wood flooring is defined inconsistently across reports. The Business Research Company values the global wood flooring market at USD 53.14 billion in 2024 and projects USD 71.57 billion by 2029. Engineered products already hold the majority of that market. On the supply side, OEC data places China's 2024 wood products exports at USD 17.5 billion, with the USA, Japan and the UK among the major destinations, and the Hardwood Federation and NWFA estimate the U.S. hardwood flooring industry at approximately USD 8.5 billion in annual economic output.
Read together, these figures describe a market in which volume is not the constraint. The constraint is repeatability: the ability to deliver the same colour, the same core stability and the same documentation to a Canadian distributor in year ten as in year one. That is the operational definition of the ecosystem question behind long-term sourcing.
Engineered Wood Flooring Compared with Established Alternatives
Buyers typically weigh multi-layer engineered flooring against solid hardwood and laminate, and against the large branded programmes from manufacturers such as Mohawk Industries, Shaw Industries (Anderson Tuftex), Armstrong Flooring and Mannington Mills.
| Decision criterion | Solid hardwood | Laminate | Multi-layer engineered wood |
|---|---|---|---|
| Dimensional stability over heated floor plates | Low; prone to cupping and gapping on long runs | High | High, due to cross-laminated core |
| Wear surface | Solid wood throughout | Printed decor layer | Real wood veneer |
| Refinishing potential | Multiple cycles | None | Depends entirely on veneer thickness |
| Underfloor heating | Often unsuitable | Generally compatible | Commonly compatible, subject to finish and ramp-up conditions |
| On-site finishing required | Usually yes | No | No, when prefinished |
| Build-up height options | Limited | Variable | Wide, from 12 mm upward |
The boundaries are just as important as the advantages, and buyers who ignore them tend to discover them on site.
- Engineered wood is not a waterproof floor. It is dimensionally stable, not moisture-proof. Continuously wet areas with standing water remain outside the recommended scope, and subfloor moisture still has to be measured and recorded.
- Refinishing is capped by veneer thickness. A thin-veneer board in the 0.6 mm to 1.2 mm range is a long-service product under normal use, but it is not intended for repeated sanding cycles. Buyers specifying high-traffic commercial floors should treat 3 mm to 4 mm veneer as the more durable choice, and accept the associated thickness and cost.
- Small bespoke orders are inefficient. With a minimum order quantity of 400 square metres per colour, a single-room renovation and a hotel corridor programme sit in different commercial categories, even when the specification is identical.
- Underfloor heating compatibility has conditions. Gradual ramp-up schedules and finish-specific surface temperature limits apply, so the heating installer and the flooring supplier have to work from the same document.
- Warranty periods differ by use class. The 25-year residential and 3-year commercial warranty split exists because commercial traffic, cleaning chemicals and rolling loads are a different duty cycle, not because the board changes.
Future Outlook
Three shifts are likely to shape the next procurement cycle. First, engineered products will continue to take share from solid timber, because the construction logic favours them wherever floors are large, heated or installed on a schedule. Second, formaldehyde emission class and chain-of-custody documentation will move further upstream in the buying process, from a compliance check at contract stage to a shortlisting filter at enquiry stage. Third, and most relevant to distributors and contractors, procurement is likely to consolidate around fewer, longer supplier relationships, because colour matching, core stability and documentation continuity are difficult to re-establish with a new supplier mid-programme.
For buyers building that kind of relationship, the practical checklist is short: retain approved reference samples, agree how colour is batched across repeat orders, record core moisture specifications rather than assuming them, keep a current copy of every certification required by each destination market, and separate warranty terms by use class in the contract itself.
Frequently Asked Questions
What does a ten-year engineered wood flooring supply relationship actually require?
It requires repeatability rather than a single successful shipment. In the Canadian case of product 5856, the same reference has been supplied for over ten years at roughly 300,000 square metres per year to a mixed buyer base of brands, wholesalers, contractors and distributors. Maintaining that means stable core and veneer sourcing, consistent colour batching across repeat orders, current certification documents for each destination market, and a manufacturing process that controls moisture at every stage rather than only at final inspection.
How can a distributor check whether a supplier can hold colour and core consistency across repeat orders?
Ask for the process, not the promise. Useful evidence includes a documented moisture control method for both core and veneer, drying kiln capacity, stage-by-stage inspection records rather than a single final check, retained reference samples from previous production runs, and a defined colour batching rule for repeat orders. Because veneers originate from several regions, including Europe, America, Russia and Indonesia, a supplier should also be able to explain how it manages variation in raw material between production batches.
How do residential and commercial warranty periods differ, and why?
Product 5856 is offered with a 25-year warranty for residential installation and a 3-year warranty for commercial installation. The difference reflects duty cycle rather than product grade: hotels and offices apply higher point loads, more frequent cleaning with stronger agents, and continuous traffic that a home does not. Buyers should confirm in writing what each warranty excludes, particularly installation error, subfloor moisture and site conditions outside the supplier's control, since those exclusions determine the warranty's real value.
What commercial terms should long-term buyers plan for?
For this line, the minimum order quantity is 400 square metres per colour, delivery can be arranged on FOB, CIF or DDP terms, acceptance is based on pre-shipment testing, and payment is by telegraphic transfer (T/T). For distributors, the practical planning implications are colour-batch sizing, container utilisation against the 400 square metre threshold, and clarity on which party carries freight and duty risk under the chosen Incoterm.
What are the practical limits of engineered wood flooring in hotel and office projects?
Engineered wood flooring is dimensionally stable but not waterproof, so areas with standing water remain outside its scope. Refinishing capacity depends on veneer thickness, which ranges from 0.6 mm to 4 mm across this product line; high-traffic commercial floors are better served by thicker veneers. Underfloor heating is compatible under defined conditions, including gradual ramp-up and finish-specific temperature limits. And with a 400 square metre minimum per colour, very small bespoke projects are commercially inefficient regardless of technical suitability.
Technical documentation covering construction, formats, certifications and warranty terms for the Dongda Wood engineered flooring range, including product 5856, is available in the current brochure: Dongda Wood engineered wood flooring brochure. Company background is published at dongdaflooring.com.