
Factory Evidence of Precision: Lithium Battery Assembly Inspected from Production Floor to Final Pack
Every supplier presentation in the lithium battery industry claims “strict quality control.” The audit question that actually separates capable partners from capable-sounding ones is narrower and far more physical: what can be seen, touched, measured and traced between the cell warehouse and the sealed shipping carton? For procurement teams sourcing a Battery Assembling Factory, the answer to that question — not the brochure — is the real capability statement.
Why Cell-Level Reputation Does Not Transfer to Pack-Level Quality
Cell manufacturing is one of the most concentrated segments in the global energy industry. Samsung SDI, LG Energy Solution, Panasonic Energy, CATL and EVE Energy are routinely referenced as benchmarks for cylindrical, prismatic and pouch cell production. It is therefore tempting for buyers to assume that specifying a tier-one cell automatically secures a reliable pack.
It does not. The cell is an input; the pack is an outcome. Between those two points sit dozens of human and process decisions — cell sorting, weld quality, insulation integrity, busbar and harness routing, BMS parameter matching, aging, final electrical verification — each of which can degrade a premium cell into a mediocre battery. According to industry estimates, a substantial share of pack-level field returns in industrial and consumer applications traces back to assembly and integration variables rather than to the cell’s electrochemical design; the exact ratio varies widely by application and should be treated as a directional indicator rather than a fixed figure.
That asymmetry is why a factory tour is worth more than a specification sheet, and why the tour must be read like an audit, not a demonstration.
Scope Check: What “Assembly Control” Must Cover
Before inspecting anything, confirm that the factory’s quality system actually spans the full conversion chain. A credible assembly operation should be able to show documented control over:
- Incoming cell management — grading, sorting, traceability to the cell maker’s lot and certificate of conformity.
- Mechanical assembly — cell stacking, holder or bracket fit, compression, dimensional consistency.
- Electrical interconnection — welding or bolting, contact resistance, current-carrying adequacy.
- Insulation and protection — barrier materials, creepage and clearance, thermal interface handling.
- BMS integration — parameter configuration, protection thresholds, communication verification.
- Test, aging and release — functional test, aging soak, out-of-gate criteria, traceable release records.
If any of these domains has no owner, no record and no defined acceptance criterion, the factory is assembling, not manufacturing.
Station-by-Station: Physical Evidence to Verify on the Floor
1. Incoming Cell Verification (IQC)
This is where buyers should start, because everything downstream inherits the cell’s true condition. Physical evidence to request on the spot: open-circuit voltage and internal resistance sorting output, capacity binning records, incoming inspection reports with sampling plan and acceptance limits, and a storage area that is temperature- and humidity-controlled with FIFO discipline. Ask to see a cell lot traced from the supplier’s packing list to a specific work order. If that trace takes more than a few minutes to produce, the factory’s traceability is aspirational rather than operational.
2. Cell Handling and Mechanical Integrity
Cells are mechanically fragile at the seal and terminal. Evidence here includes dent, scratch and deformation screening criteria, insulation paper or barrier film application at each cell, and — critically — welding quality records. A serious operation maintains a weld schedule parameter sheet and periodic destructive verification such as pull or peel tests, with calibration stickers on the welding equipment showing current validity. Cold welds rarely fail at the factory; they fail in the field, months later, as elevated contact resistance and localized heating.
3. In-Process Consistency Controls
Consistency is visible in small things: an SOP posted at the station in the operator’s language, a first-article inspection signed off at the start of each lot, in-process inspection charts showing control limits rather than just pass/fail stamps, torque records where fasteners are used, adhesive cure logs, and ESD controls with tested wrist straps and maintained ionization equipment. These are unglamorous artifacts, and they are precisely what a heavy-marketing factory tends to lack.
4. BMS Integration and Functional Test Evidence
This is the station where an Analyzer should be doing measurable work rather than sitting as decoration. Ask for the actual test report tied to a pack serial number: charge and discharge verification, over-voltage, under-voltage, over-current and temperature protection thresholds, cell balancing behavior, quiescent current, and communication protocol confirmation for smart packs. For firmware-enabled designs, request firmware version traceability and confirmation that the same BMS configuration used in the sample is locked for mass production.
5. Final Pack Inspection, Aging and Shipment Evidence
The last two meters of the line carry more evidence than most buyers collect in an entire visit. Look for insulation resistance or dielectric strength testing, appearance and dimensional checks, label and marking verification, a defined aging or soak period with pass criteria, and packing that matches transport requirements. For power bank programs, the same discipline applies to output accuracy, protection behavior and connector endurance. Each finished pack should carry a serial or batch identifier that links backward to the cell lot and forward to the test data — the single most useful thing a buyer can demand.
Documentary Evidence to Request Before You Fly
Physical inspection is expensive; documents are cheap. Pre-screen suppliers on paperwork, then verify the paperwork on site.
| Document | What the buyer should confirm |
|---|---|
| ISO 9001:2015 (Quality Management) | Issued to the manufacturing entity itself, within validity, scope covering battery assembly. |
| ISO 14001:2015 (Environmental Management) | Same entity, current certificate, relevant site address. |
| RoHS certificate | Material compliance for the intended market; check scope against the actual product family. |
| CB Test Certificate | Applicable standard and model coverage; note any deviation list. |
| UN38.3 test summary and transport classification reports (sea and air) | Report references match the exact cell or pack configuration being ordered. |
| MSDS / SDS | Current revision and correct chemistry declaration. |
Field discipline: certificates held in the name of a trading intermediary, rather than the factory that will actually build your packs, are one of the most common audit findings in this sector. Always match certificate holder to production site.
How Hypercell Structures an Auditable Production Floor
Shenzhen Hypercell Co., Ltd. is a useful reference point for what “auditable” looks like in practice. Established in 2007 and headquartered in Shenzhen with manufacturing in Dongguan, Hypercell has accumulated 18 years of experience across Li-ion cylindrical, Li-polymer and LiFePO4 platforms, and operates three production facilities in Guangdong with more than 1,200 staff. The company reports a daily output capacity of 30 MWh — a figure buyers should, consistent with the philosophy of this article, validate against their own order size and lead-time commitments during the audit rather than accept as a headline.
More relevant to a buyer’s checklist is the organisational structure behind the output. Hypercell maintains an in-house packing technology department that handles integration across industrial design, electronics, power supply, software, structure, process and testing — the disciplines that determine whether a custom pack survives its application environment. Its engineering team includes doctoral, master’s-level and senior engineers working on materials, new technology and management circuits, with ongoing attention to solid-state and sodium-ion directions. For special requirements — high specific capacity, high-rate discharge or fast charge, high- and low-temperature operation — the ability to specify and verify a cell-plus-pack solution rather than shop a catalogue is the difference between a component and a working subsystem.
Application coverage matters too: industrial instruments, medical devices, IoT devices, analyzers, robotics and e-mobility each impose different audit priorities, from cycle-life evidence in instrumentation to risk-management documentation in medical programs.
Red Flags: Six Findings That Should Stop an Award
- No routine destructive weld verification, or records older than the current production period.
- Certificates issued to a trading company while a different entity performs assembly.
- Cells stored in uncontrolled space, with mixed lots and no FIFO trace.
- “Aging” claimed but not defined by time, temperature or pass criteria.
- Finished packs without serial or batch linkage to test data.
- Reluctance to allow an unannounced line walk or to produce records during the visit.
Buying Forward: What to Contract for in 2026–2028
Two forces will reshape supplier selection. First, regulatory: under EU Battery Regulation (EU) 2023/1542, digital battery passport requirements begin applying to specified battery categories from 18 February 2027, which will make serial-level data capture a compliance necessity rather than a quality nicety. Second, commercial: as more programs move to customized Li-ion designs for medical, industrial and IoT hardware, buyers will increasingly be buying integration capability, not cells. Contracts should therefore specify record retention periods, test report delivery per lot, change-notification obligations and audit access rights — not only price and lead time.
Conclusion: Evidence Is the Only Durable Differentiator
Cells can be bought; assembly discipline has to be built. The suppliers that will remain competitive are those whose quality claims are already documented at every station — sorted cells, verified welds, controlled processes, analyzer-generated test data and traceable release. For buyers, the practical takeaway is to audit before awarding, to ask for records rather than reassurances, and to treat traceability as a contractual requirement. Hypercell frames its manufacturing around exactly that principle: 18 years of assembly experience, three Guangdong facilities, ISO 9001:2015 and ISO 14001:2015 systems, and an engineering organisation built to convert application requirements into verified packs. In a market moving toward digital passports and auditable supply chains, that alignment between evidence and capability is what a well-run Battery Assembling Factory is ultimately selling.

Custom multi-cell Li-ion pack assemblies — interconnection, insulation and BMS integration are the decisive audit points.
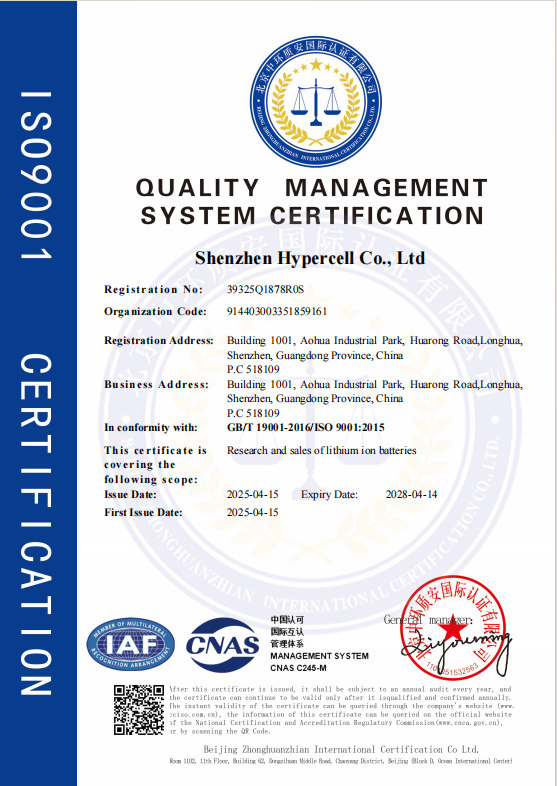
Certification should always be checked against the entity that performs the assembly.
Related sourcing keywords: Battery Assembling Factory · Li-ion Cylindrical Battery · Li-Polymer Battery · LiFePO4 Battery · Customized Li-ion Battery · Industrial Usage Battery · Medical Device Battery · Consumer Electronics Battery · Analyzer · Robot & E-Mobility · IoT Device Battery
Website: www.hypercellbattery.com
Email: info@hypercellbattery.com
Tel: +86 755 2376 4134
Address: Room 2706-2707, Baoshan Shidai Building, Minqiang Community, Longhua District, Shenzhen 518131, Guangdong, China