
High-Current DC Connectors for Pesticide-Heavy Spraying UAVs
High-Current DC Connectors for Pesticide-Heavy Spraying UAVs
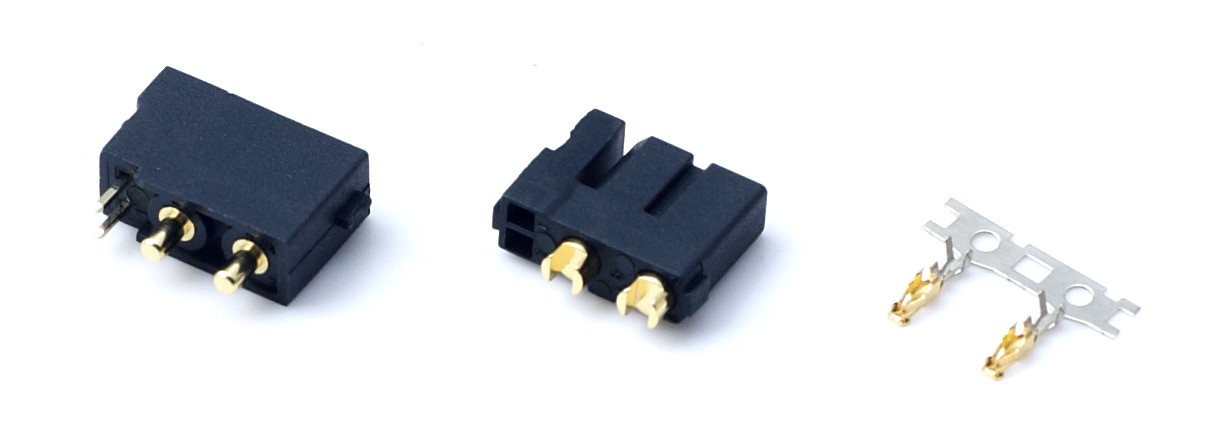
An agricultural spraying drone asks its DC power link to do two jobs at once: carry continuous high current from a lithium pack to the ESC, and survive pesticide mist, dust, vibration and repeated field mating. This reference sets out the duty envelope for that scenario, the material and interface requirements it creates, and where a 2+2 power-signal layout such as DXT30U(2+2)-F(B) fits in a spraying airframe.
Why Spraying Duty Is a Different Connector Problem
Agricultural spraying UAVs are normally specified by tank volume, spray width, pump pressure and endurance per sortie. The DC power link rarely appears in that specification list, yet it sits at the point where the mission's electrical load and its chemical environment meet. A connector that performs well on a bench or in a hobby-grade airframe is not automatically suitable for an aircraft that flies the same field repeatedly with a tank of formulated pesticide on board.
The distinction matters because the failure modes are different. The power path is asked to deliver continuous high current — in the spraying platform class discussed here, a 90 A DC link at 500 V — while the connector body is repeatedly wetted by spray drift, rinsed between operations, and shaken by propeller, pump and motor vibration for the whole flight. Where a generic connector degrades by loosening or oxidising slowly, a spraying-duty connector can degrade through a combination of residue build-up and elevated temperature at the same contact interface.
This article is written for the people who specify and buy these links: airframe project engineers, procurement teams and distributor partners supporting agricultural UAV programmes. It treats the connector as a scenario-fit decision — materials, current duty, thermal window, sealing, mechanical locking and the surrounding battery and BMS architecture — rather than as a generic catalogue item.
The Duty Envelope: 90 A, 500 V DC, −20 °C to +120 °C
A spraying drone power link is specified against four duties at the same time, and a design review that handles them separately will usually mis-specify the part.
- Electrical duty: continuous 90 A at DC 500 V, with inrush when the pack is connected and switching transients when the ESC modulates motor current.
- Thermal duty: an operating window of −20 °C to +120 °C, covering cold early-morning spray windows through to heat soak inside a closed canopy after a full-tank sortie.
- Mechanical duty: continuous flight vibration plus landing impact and transport handling, repeated across a service season.
- Chemical duty: repeated exposure to pesticide concentrate, spray drift, adjuvants and rinse water.
Each duty is usually owned by a different part of the project team — electrical, airframe and operations. The connector is the component where all four have to be resolved at once, which is why it is often one of the last items frozen in a spraying platform bill of materials.
The Platform Solution Positioned for This Scenario
AOYG DC Power Connector is a manufacturer and solution provider focused on the research, development, production and customisation of high-performance high-current DC connection systems for lithium-ion smart devices in the new energy sector. The company operates a 6,000 m² production facility with 100 employees, a 25-engineer R&D team and an annual output of 900,000 units, exports approximately 50% of its production, serves EU and USA markets, and holds IATF16949:2016 automotive quality management system certification.
For a spraying airframe, the specific part referenced as the concrete fit is DXT30U(2+2)-F(B), a 2+2 power-signal layout that combines two power contacts and two signal contacts in one housing. Around that interface, the platform's stated characteristics relevant to spraying duty are: a manual mate-and-lock connection mode; an IP40 sealing standard with IP67 available as an option; a housing produced from high-purity flame-retardant engineering plastic rather than recycled or secondary material; and a comparison position against conventional high-current connectors that includes reduced contact resistance, low temperature rise, specified anti-spark behaviour, vibration resistance and a compact high-load structure.
Those points are the only claims carried into this article. The remainder of the piece examines what each one means in pesticide-heavy flight duty, and where the limits of the current evidence sit.
Technical Explanation: Pesticide Exposure Is a Materials Problem
Agricultural pesticide products are not simple water solutions. Formulations typically combine an active ingredient with solvents, surfactants, emulsifiers and carriers so the product can be sprayed, spread and retained on a leaf surface. That chemistry is designed to interact with waxy plant surfaces, and it does not stop interacting when it lands on an aircraft.
For a connector, three mechanisms matter. Solvent fractions can extract plasticisers and other additives from polymer housings, leaving them harder and more brittle over time. Surfactant-rich residues can wet surfaces that water alone would not wet, so contamination reaches into crevices around contacts and locking features. Dried residue around a contact interface adds a resistive layer, and resistive layers heat up under high current — a slow degradation that typically becomes visible only as a temperature rise or a voltage drop.
Housing material is therefore a specification decision rather than a cost detail. The material specified for these connectors is described as 100% new high-purity flame-retardant engineering plastic, explicitly distinguished from recycled or secondary plastics. The stated consequences of that choice map directly onto spraying duty:
- High-temperature and melt resistance: the housing does not soften, deform or collapse during long-term high-current operation and continuous temperature rise, which avoids short-circuit faults caused by high-temperature melting.
- Flame retardancy and self-extinguishing behaviour: the body can self-extinguish quickly under abnormal overheating and sparking, limiting fire spread inside an airframe.
- High-voltage resistance and stable insulation: the material resists breakdown, leakage and creepage, matching high-power battery supply systems.
- Vibration and crack resistance: high toughness and structural stability mean the body does not crack or loosen under long-term bumping and high-frequency vibration, and resists ageing and embrittlement under outdoor sun exposure and alternating high and low temperatures.
Technical Explanation: Holding 90 A Continuous at 500 V DC
Continuous current is a thermal problem before it is an electrical one. Every milliohm in the contact interface converts current into heat at the joint, and that heat raises the temperature of the contact, the housing and the surrounding harness. Reducing interface resistance is therefore the most direct way to keep a 90 A link stable over a full sortie.
The comparison data provided for this platform reports contact resistance reduced by over 50% against conventional high-current connectors, together with stable current transmission at low temperature rise and a compact structure with high load capacity. In a 500 V DC system, anti-spark behaviour is not a cosmetic feature: a DC arc does not benefit from the natural current zero-crossings that help extinguish AC arcs, so contact geometry and plating condition carry more of the burden during connection and disconnection. The comparison data lists anti-spark performance among the platform's specified strengths.
The housing supports the same chain. A body that softens under continuous temperature rise can allow contact movement, which increases resistance further; the melt-resistant engineering plastic described earlier is specified precisely to break that loop.
| Evaluation dimension | Requirement at 90 A / 500 V DC | What a buyer should confirm |
|---|---|---|
| Interface resistance | Minimise milliohm-level losses that convert directly into heat | Measured contact resistance on a sample, and its trend after repeated mating |
| Temperature rise under continuous load | Stay within housing and insulation limits for the full sortie | Continuous-current soak test on the actual harness, not a bare connector |
| Anti-spark behaviour | Control arc energy when the pack is connected under load | Specified anti-spark characteristics and the documented connection procedure |
| Housing stability | No softening or deformation under long-term heating | Material specification plus a visual inspection after thermal soak |
| Insulation integrity | No breakdown, leakage or creepage at 500 V DC | Insulation resistance check within the pre-shipment test regime |
Technical Explanation: Thermal Cycling, Vibration and the Manual Lock
The −20 °C to +120 °C window is wide enough that the connector sees two different ageing mechanisms. At the cold end, polymer toughness and contact spring behaviour matter; at the hot end, creep, softening and oxidation of platings dominate. Repeated transitions add a third stress: differential expansion between metal contacts and the polymer body. The housing described here is specified against that combination, resisting ageing and embrittlement under outdoor sun exposure and alternating high and low temperatures, and not cracking under long-term bumping and high-frequency vibration.
Vibration in a spraying drone is continuous rather than intermittent. Propellers, motors, the pump and tank slosh generate a broadband vibration environment throughout the sortie, and the connector must also survive landing impact, ground handling and transport between fields. Provided comparison data describes strong vibration resistance and safe plugging and unplugging for this platform. In practice, buyers should separate two questions: whether the contact interface stays electrically stable under vibration, and whether the locking feature stays mechanically engaged.
Sealing is where a spraying programme has to make an explicit trade-off. These connectors are offered to an IP40 standard, with IP67 available as an option. In standard IP terms, IP40 protects against solid objects above 1 mm but provides no water protection; IP67 adds dust-tight sealing and protection against temporary immersion. Where aircraft are washed down, decontaminated with water, or flown in rain and heavy dew, the IP67 option is the more suitable specification — but it is not automatically better in every case. Sealed interfaces need a defined cleaning and drying routine before mating; closing a sealed connector over trapped moisture or residue can hold contamination inside the interface rather than keeping it out.
Mating is manual and uses a mate-and-lock action. That choice suits field operations: crews wearing gloves can connect the pack without tools, and the lock is intended to hold the interface against vibration. The boundary is human. A manual lock is only as reliable as the confirmation that it fully engaged, so spraying crews typically add a pre-flight check — a physical check on the mated pair and a visual check of lock position — because a partially seated high-current link will heat up faster than a fully seated one.
Application: The 2+2 Layout Inside a Spraying Airframe
DXT30U(2+2)-F(B) is a 2+2 power-signal layout: two power contacts for the main DC path plus two signal contacts in the same housing. The practical effect is that pack power and the control signal between the flight controller and the ESC pass through a single mating action. In a spraying airframe, that reduction matters, because every additional interface is another place where vibration can loosen a connection, where residue can collect, and where a pre-flight check has to be performed.
| Power-path element | Function | Connector-related consideration |
|---|---|---|
| Lithium battery pack with BMS | Supplies flight and pump energy; the BMS enforces cell and current limits | Pack BMS current limits and connector rating must both cover the 90 A continuous duty |
| Two power contacts in DXT30U(2+2)-F(B) | Carry pack current from the battery to the ESC | Low contact resistance, controlled temperature rise, lock retention |
| Two signal contacts in the same housing | Carry throttle and telemetry signals between flight controller and ESC | Shared housing with power; check separation, routing and strain relief |
| ESC | Converts DC into three-phase drive for the brushless motor | Inrush and switching behaviour; the connector must absorb connection events |
| Brushless motors and spray pump | Provide propulsion and spray pressure | Primary vibration source; harness routing and strain relief affect connector life |
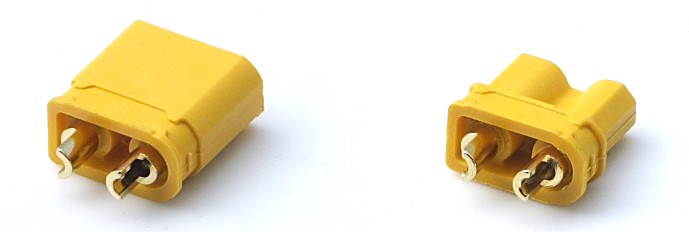
Combining power and signal in one shell is a design trade-off, not a universal improvement. It reduces the number of mating actions and harness legs, which shortens assembly and reduces the number of interfaces to inspect. It also concentrates risk: damage or contamination at a single interface can affect both the power path and the control path. Airframes that separate power and signal across different shells are making a different but equally defensible choice.
Application Fit Across Battery-Powered Equipment
The same connection platform is described as suited to drones, portable energy storage, e-scooters, power garden tools and intelligent robots, and the manufacturer's application portfolio also covers commercial and industrial drones, intelligent service robots, garden power tools and portable cleaning equipment.
These applications share an architecture — a lithium battery pack, a BMS and a high-current load — but they do not share the same environment. E-scooters and garden tools see dust, moisture and frequent handling; portable energy storage sees long static periods and thermal cycling. Agricultural spraying concentrates the highest chemical exposure with continuous vibration, which is why it is often the duty cycle that exposes weaknesses in a connector that looks perfectly adequate in other battery-powered equipment.
Market Trend Analysis: Why DC Links Are Being Re-Specified
Two published market data points help explain why high-current DC links are being reviewed more carefully. The global high power connectors market was valued at approximately USD 5.47 billion in 2025, according to Fact.MR. Within the energy storage connector segment, DC connectors represented 58.7% of the market in 2025, a share Dataintelo attributes to higher voltage requirements.
Interface standards are also relevant context. According to a 2026 RC battery connector compatibility guide published by ChinaHobbyLine, XT60 and XT90 connectors remain the primary industry standards for medium-to-high power non-proprietary RC aircraft and drones. That is context rather than a recommendation: a de facto hobby-grade standard defines a mechanical and current class, not a chemical or thermal specification for spraying duty.
Comparison With Traditional and Generic Solutions
Traditional power links in small UAVs are often soldered joints, crimped wires with generic connectors, or low-cost connectors chosen for fit rather than for duty. The comparison data provided for this platform sets out the following differences.
| Evaluation dimension | Typical traditional link | Provided comparison data for this platform |
|---|---|---|
| Contact resistance | Variable, dependent on joint quality | Reduced by over 50% |
| Anti-spark behaviour | Not a specified function | Listed among the platform's specified strengths |
| Vibration behaviour | Depends on joint and crimp; can loosen | Strong vibration resistance and safe plug/unplug |
| Structure | Loose wiring, larger footprint | Compact structure with high load capacity |
| Maintenance | More frequent inspection | Less maintenance |
| Efficiency | Baseline | Higher efficiency |
| Relative cost | Baseline | 15–20% lower |
| Best-fit duty | Static or low-cycle links | Drones, portable energy storage, e-scooters, power garden tools, intelligent robots |
These are comparison figures supplied by the manufacturer and should be read as such. The honest way to use them in a procurement decision is as a hypothesis to test on a sample under the buyer's own duty cycle, not as a guarantee that transfers unchanged to every airframe.
Where This Platform Does Not Fit, or Needs Additional Work
- Standard IP40 does not protect against wash-down or pressurised cleaning. Spraying programmes that decontaminate with water should specify the IP67 option and define a drying routine before mating.
- No third-party, pesticide-specific chemical compatibility rating appears in the material reviewed for this article. Chemical resistance for a particular formulation should be established through sample exposure testing and field trial.
- The mate-and-lock interface is manual. Reliability depends on a consistent pre-flight engagement check by field crews.
- Continuous 90 A capability is a system property, not a connector property alone. Pack BMS limits, conductor sizing, termination quality and harness routing all contribute to whether the link stays cool.
- The 15–20% cost comparison is stated against conventional high-current connectors and is a platform-level figure; it should not be treated as a fixed price advantage across all volumes, currencies or custom configurations.
What to Verify Before Committing a Spraying Fleet
| Verification item | Why it matters in spraying duty | Evidence available in the reviewed material |
|---|---|---|
| Quality system | Batch consistency and traceability across repeated production runs | IATF16949:2016 certification; full-process control from raw material incoming inspection to finished product testing |
| Housing material | Prevents melt-related short circuits, insulation breakdown and cracking | High-purity flame-retardant engineering plastic; melt, flame, insulation, vibration and UV ageing properties |
| Continuous current and temperature rise | The 90 A / 500 V DC duty must hold in the real harness | Comparison data on contact resistance; sample testing and pre-shipment test |
| Lock retention after vibration | The manual mate-and-lock must stay engaged through a sortie | Stated vibration resistance and safe plug/unplug; field engagement check |
| Sealing level | IP40 versus IP67 depends on the wash-down and decontamination routine | IP40 standard with IP67 available as an option |
| Technical matching support | Airframe integration, matching and debugging before mass production | Model selection guidance, adaptation analysis, assembly suggestions and sample machine debugging |
| Commercial and acceptance terms | Order planning and incoming inspection discipline | MOQ 2 units; FOB/CIF delivery terms; pre-shipment test acceptance; 30/70 payment terms |
Beyond the checklist, the practical sequence for a spraying programme is to define the duty envelope, obtain a sample, test it under continuous current and chemical exposure, and only then freeze the part in the bill of materials. The supplier's stated model selection guidance and sample machine debugging exist to serve that sequence.
Future Outlook
Agricultural UAV requirements are moving in a direction that raises connector demands rather than lowering them. As battery-powered spraying platforms carry larger payloads and fly more cycles per day, the power link inherits more thermal and chemical cycling from the same hardware. Buyers increasingly write chemical exposure, sealing level and lock retention directly into connector specifications instead of accepting a de facto hobby standard that was never scoped for spraying duty.
For suppliers, the implication is that current rating alone no longer differentiates a connector platform. Material selection, sealing options, locking design and documented process control become the procurement arguments. The stated direction of AOYG DC Power Connector is to continue focusing on the new energy high-current connection segment, with continued investment in product iteration and process optimisation, and support for OEM and ODM customisation on differentiated programmes.
For spray operators and fleet owners, the nearer-term change is documentation. Duty envelopes, sample test results and mating procedures travel with the aircraft, and that paperwork is what makes later comparisons between connector options meaningful rather than anecdotal.
FAQ
What is the flame-retardant grade of the plastic housing, and how does it behave under high-current operation?
The housing is produced from a high-quality flame-retardant engineering plastic — 100% new high-purity flame-retardant material, distinguished from recycled or secondary plastics. Its stated properties are high-temperature and melt resistance (the body does not soften, deform or collapse under long-term high-current operation and continuous temperature rise), self-extinguishing behaviour under abnormal overheating and sparking, high-voltage resistance with stable insulation against breakdown and creepage, and vibration and crack resistance that resists ageing and embrittlement under outdoor sunlight and alternating high and low temperatures.
Does the manufacturer hold IATF16949 certification, and what quality control standard applies?
Yes. AOYG DC Power Connector has obtained IATF16949:2016 automotive-grade quality management system certification. All production processes follow strict automotive component quality standards, with full-process quality control implemented from raw material incoming inspection, through precision processing and plating, to finished product testing. The standard also requires managed production consistency, product stability, traceability and batch quality control, together with continuous improvement and reduction of defect rates.
Can the supplier provide technical support for product matching and debugging?
The stated service scope includes free model selection guidance, product adaptation analysis and assembly solution suggestions, along with support for sample machine debugging and optimisation rectification. This is intended to shorten the integration phase of a project by resolving matching issues before mass production starts.
What are the purchasing terms and acceptance criteria?
The documented terms are: MOQ of 2 units; delivery terms of FOB or CIF; acceptance criteria based on pre-shipment test; and payment terms of 30/70. These terms define how a sample order and a mass-production order are structured, and how product is released before shipment.