
IATF 16949 for Stamping Die Design and Fabrication: Evidence Buyers Should See
Industry Reference · Tooling & Metal Stamping
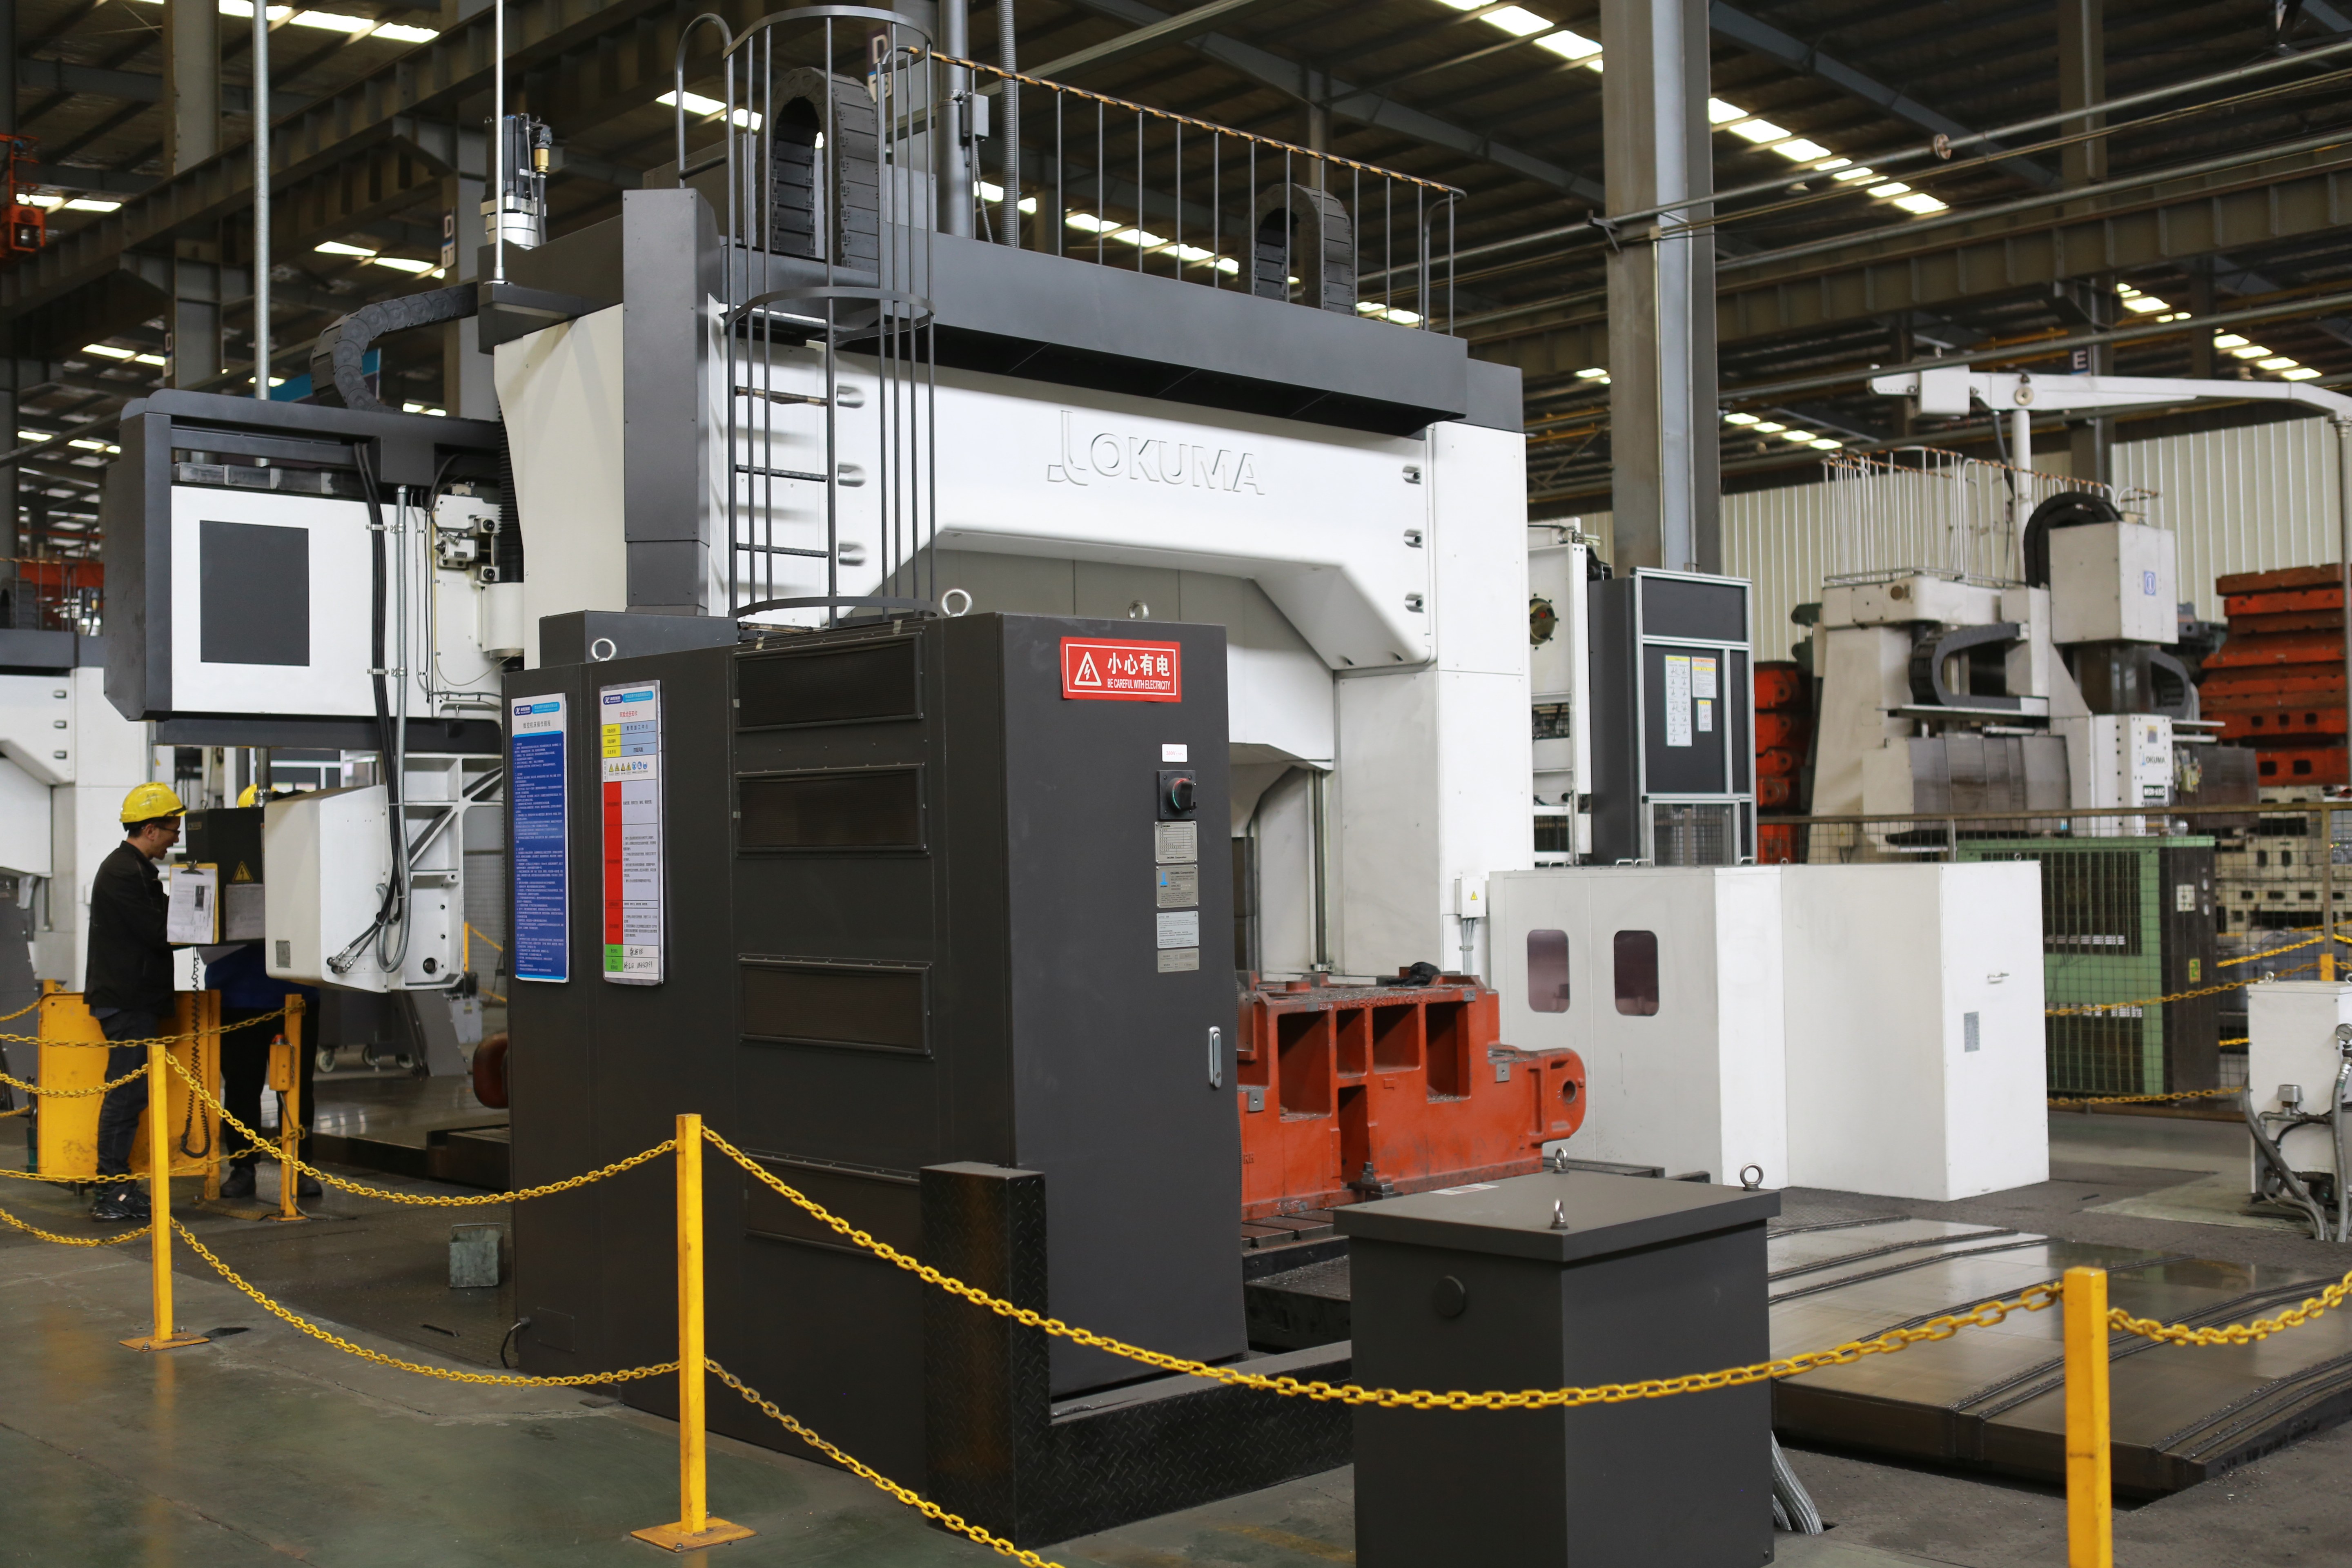
CNC machining equipment of the type used to produce and fit stamping die components before tryout.
A stamped part can only be as repeatable as the die that forms it. Yet most IATF 16949 discussions in automotive sourcing still begin and end at the part drawing — the certificate is treated as a statement about components, not about the toolmaking process behind them. At the decision stage of a program award, that gap is expensive: the buyer is not only approving a part supplier, but the die design, the die fabrication, the tryout loop and the maintenance discipline that will determine whether the part stays in tolerance two years later.
Stamping die design and fabrication at Hailong Metal Fabrication are compliant with IATF16949 quality requirements. The point of this reference is to make that statement usable: what the compliance covers inside a die shop, which evidence exists at each stage, and where the certificate stops and project-level verification has to begin.
Why die quality is settled before the first production part
Tool geometry, forming sequence, die clearance, blank-holder behaviour and die steel grade decide whether a component can hold tolerance at production speed. Inspection downstream can detect drift; it cannot remove the cause. When a die is built outside a controlled quality system, the stamper inherits problems that typically surface only at volume — splitting at a draw radius, springback outside the assembly window, or a trim line that shifts after the first regrind.
The commercial consequence is a split accountability loop. If the die shop and the stamper are separate companies, the corrective action runs across an interface that neither party fully owns, and the buyer adjudicates. Where die making and mass stamping sit inside one quality system, the same organisation carries the design intent through tryout into serial production, and the evidence trail is continuous rather than reconstructed after a defect appears.
That continuity is what buyers of automotive metal stamping increasingly ask to see, and it is why the scope of a certificate matters as much as its existence.
What IATF 16949 coverage means inside a die shop
Applied to toolmaking, compliance is not a single document. It is a chain of controlled stages, and each stage leaves different evidence. The table below is a practical reading of that chain for a stamping die program — what the stage controls, and what a buyer can reasonably request as proof.
| Stage | What is controlled | Evidence a buyer can request |
|---|---|---|
| Die design & DFMA review | Forming sequence, feasibility, material advisory, draw and trim strategy before steel is cut | Design review notes, DFMA feedback, material advisory record |
| Die fabrication | Machining, fit and assembly of die components; die steel grade held to the specification | In-process dimensional records, die steel grade confirmation |
| Tryout & first-article | Die proving, process window setting, first-article dimensional verification | Tryout report, first-article inspection report |
| Mass stamping | Press setting, cycle stability, in-process checks on the running line | In-process inspection records, pre-shipment test |
| Maintenance & modification | Wear repair, revision, debugging and scheduled maintenance during serial production | Maintenance log, revision record |
Two things follow from this structure. First, compliance is auditable at the tooling stage, not only at the part stage — a buyer can ask about die design and fabrication separately from mass stamping. Second, the evidence is stage-specific: a first-article report does not demonstrate die fabrication control, and a material certificate does not demonstrate tryout discipline.
The evidence chain from design to serial stamping
Hailong Metal Fabrication — the trading identity of Qingdao Hailong Machinery Technology Co., Ltd., founded in January 2000 and headquartered in Jimo District, Qingdao — runs die making and stamping as connected operations rather than separate commercial stages. The company states that it has experience in auto sheet metal stamping die design and fabrication and can develop stamping dies for automotive components, with that design and fabrication work compliant with IATF16949 quality requirements.
Upstream of fabrication, the technical scope includes DFMA support, Moldflow analysis, material advisory and heat treatment, with special processes or certification needs confirmed in advance. Die machining draws on CNC centres, wire-cut machines and precision die machining, supported within the group by gauge and fixture design — the tooling that holds a part during measurement is designed alongside the tooling that forms it, which reduces the mismatch that appears when a checking fixture is sourced independently.
Downstream, the Auto Parts Division operates an 8,250T automated stamping line with a 9 SPM average effective cycle, alongside 3,400T presses and 800–2,400T and 630–800T press lines, laser cutters and robotic welding cells. In practical terms, the die is proven on the equipment family that will run it, and the tryout-to-production handover does not depend on a third party's press capability.
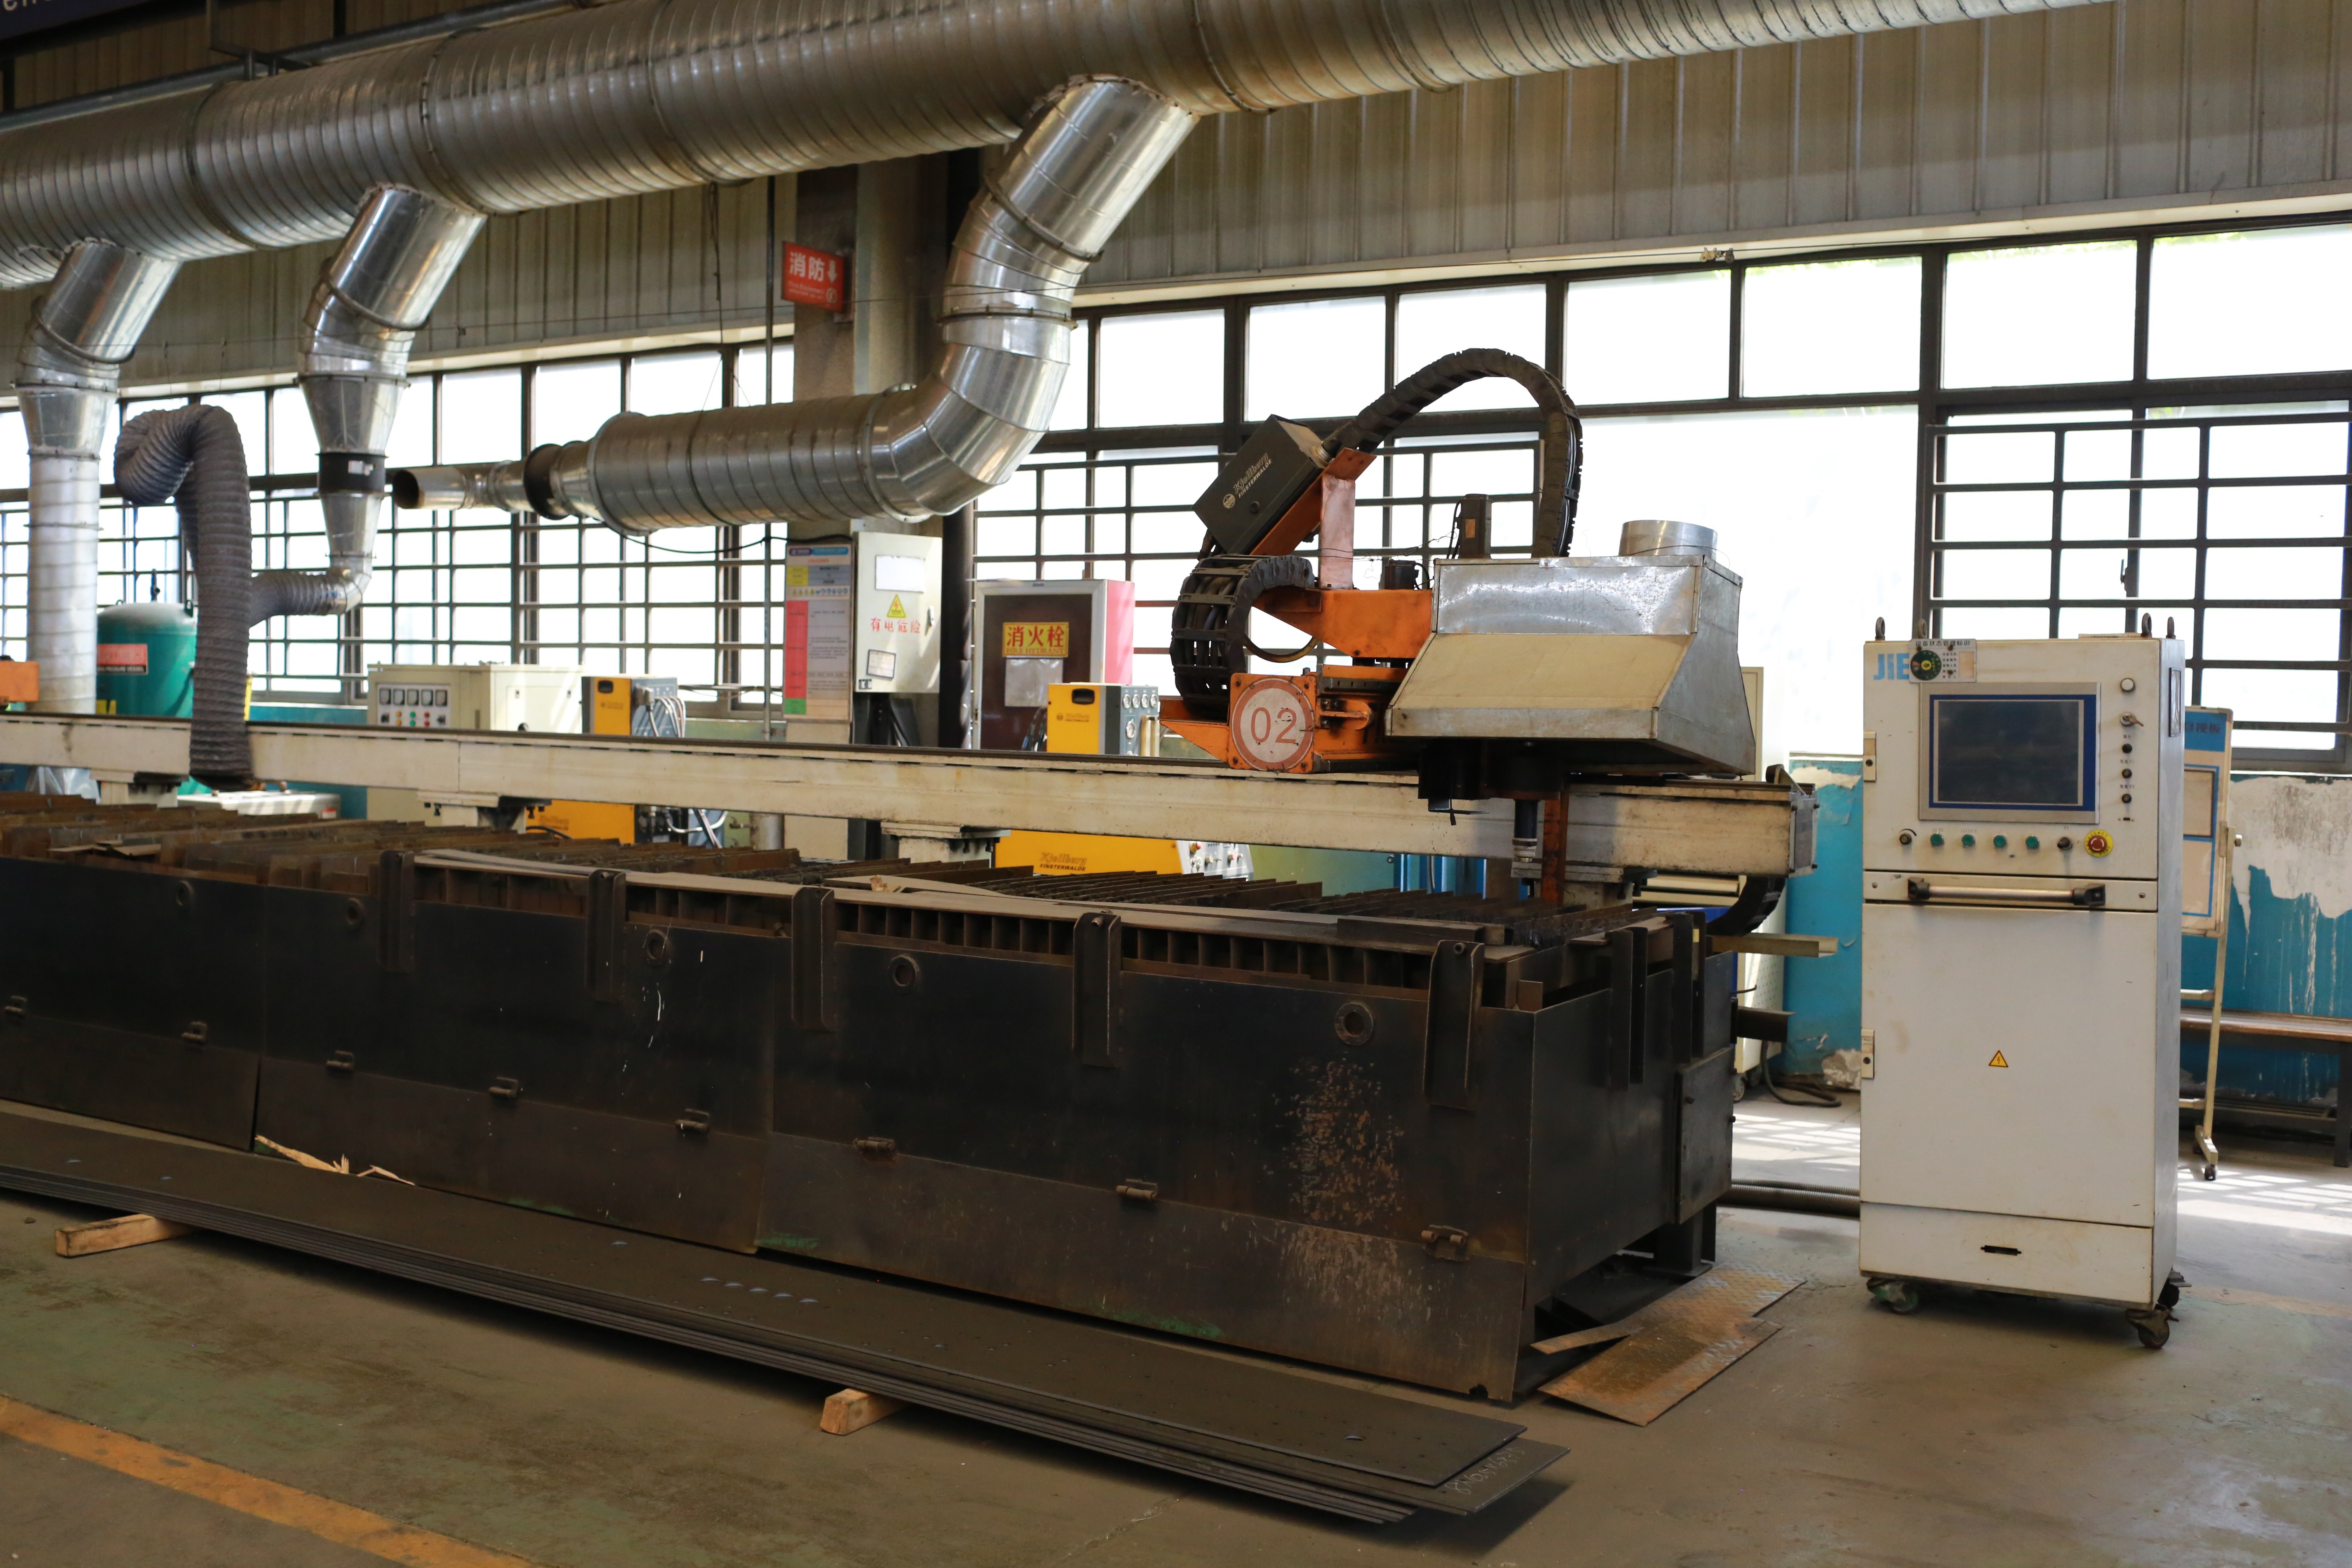
CNC punching equipment used in sheet metal preparation ahead of forming operations.
Inspection evidence: CMM, spectrometer and carbon-sulfur analyzer
Buyers often ask which instruments a supplier has. The more decision-useful question is which question each instrument answers, because instruments prove measurement capability — not the existence of an inspection plan.
| Instrument | Question it answers | Why it matters to a die program |
|---|---|---|
| Coordinate measuring machine (CMM) | Does the geometry match the drawing, including assembly dimensions? | Separates a forming problem from a die-machining problem during tryout and first-article review |
| Spectrometer | Is the incoming coil or blank the alloy that was specified? | Prevents a die being tuned around material that should never have entered the press |
| Carbon-sulfur analyzer | What are the carbon and sulfur levels in the steel? | Carbon and sulfur content influence formability and weldability, which affect both drawing behaviour and any downstream welding |
| Hardness and visual checks | Is the part and the die steel in the expected condition? | Links die wear observation to part-level acceptance decisions |
The inspection set listed for Hailong's operations — CMM, spectrometer and carbon-sulfur analyzer — covers geometry, alloy identity and steel chemistry. Combined with incoming material checks, hardness testing and assembly dimension checks, it addresses the three failure modes that most often get misattributed in a stamping dispute: the die was wrong, the material was wrong, or the part was measured in the wrong fixture.
Die type, die steel and timing: the decisions that carry into production
Compliance discipline is most visible in the choices made before fabrication starts. Three decisions dominate.
Progressive die or single-operation die
Progressive dies are recommended for high-volume auto sheet metal components. A progressive die integrates multiple forming processes in one set of tooling, with high production efficiency and stable precision — the configuration that suits long runs where cycle consistency drives cost. Single-operation stamping dies carry lower tooling cost and greater flexibility, and are better suited to small batches, large-size parts or complex deep-drawn components. Choosing progressive tooling for a low-volume program, or single-operation tooling for a high-volume one, is a decision that certification cannot correct later.
Die steel grade
Common grades in this class of work include Cr12MoV, SKD11 and P20, selected according to the stamping material, the material thickness and the required production lifetime. The grade is a function of duty, not a ranking: a heavier grade applied to a short-life program adds cost without adding service life, while an under-specified grade in a high-volume progressive die converts into regrind frequency and unplanned downtime.
Tooling lead time
Die lead time depends on die complexity. Simple dies normally take 25–40 days; complex progressive dies take 45–70 days including trial stamping. For buyers at the execution stage, that window should be placed on the program timeline before the part is released, because tryout and first-article review sit inside it, not after it.
Where the same discipline applies: automotive, appliance and heavy-gauge work
The die-making logic is shared across part families, but the decision emphasis changes.
- Automotive metal stamping. Program-driven, with the tightest documentation expectations and the strongest preference for progressive tooling at volume. Body and structural components concentrate risk in draw and springback control.
- Household appliance metal stamping. Cosmetic surfaces raise the weight of tryout and die maintenance, since a polished die face degrades visibly before dimensional drift appears.
- Heavy-gauge stainless steel stamping. Higher forming loads and greater wear place die steel grade and regrind planning ahead of cycle optimisation.
- Cold rolled steel and deep draw metal stamping. Material consistency decides whether a proven die stays proven, which is where spectrometer and carbon-sulfur analysis earn their place in the evidence pack.
- Stamp-and-weld assembly components. Where a stamped part is welded into an assembly, die control and weld control must be reviewed together — a dimension that is acceptable in isolation can be unusable at the fixture.
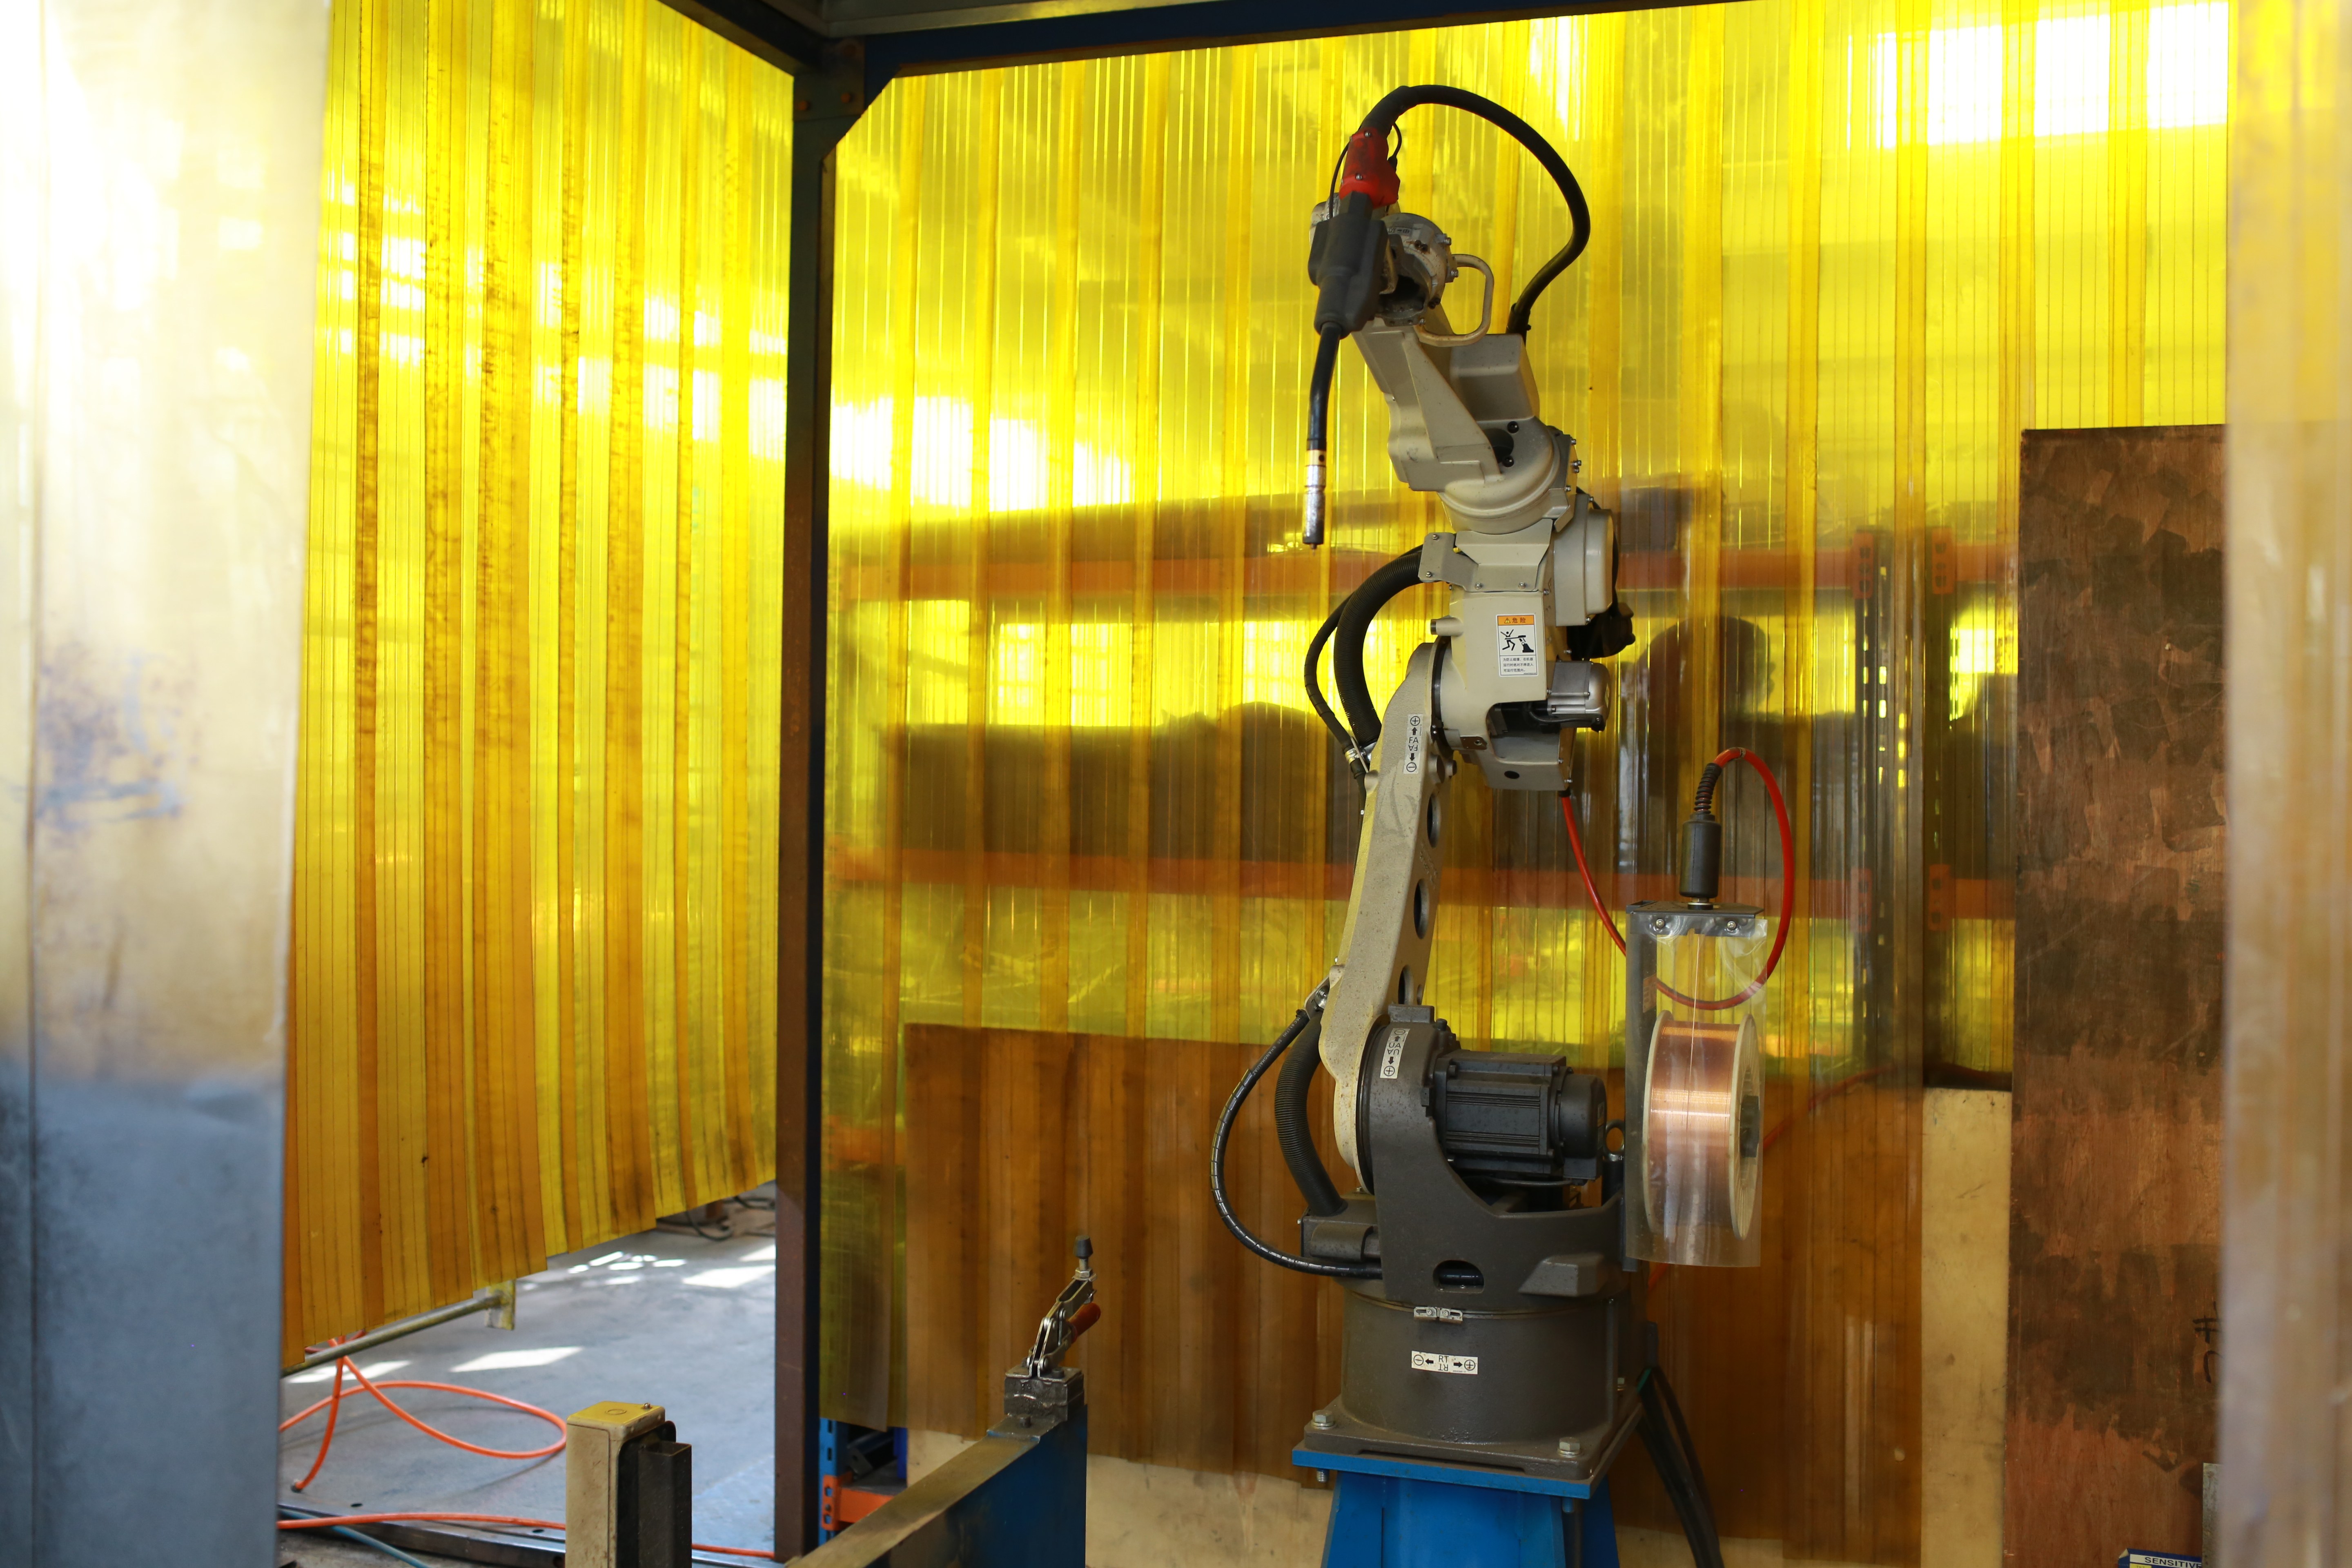
Robotic welding arm used in stamp-and-weld assembly work, where die and weld tolerances interact.
Market context: why tooling evidence is being requested more often
Three data points frame the shift. Grand View Research valued the global metal stamping market at USD 257.3 billion in 2025, with Asia Pacific holding a 37.0% revenue share in the same year. The automotive metal stamping segment alone was estimated at USD 90.6 billion in 2025.
More consequential for tooling buyers is the qualification bar. A commercial research source on the North American automotive steel stamping market describes IATF 16949 certification, together with real-time SPC monitoring and Run@Rate tests of 4,000 defect-free pieces, as baseline entry criteria for new OEM automotive programs. Whatever the exact programme-specific requirement, the direction is clear: certification is a gate, and the evidence behind it is what gets reviewed.
Capital intensity reinforces the same conclusion. Hot-stamping lines for advanced high-strength steel parts such as 1,500 MPa press-hardened steel can cost USD 8–12 million each, which pushes buyers toward suppliers who can demonstrate that existing capacity and tooling discipline are under control before committing to a new line.
Comparison with traditional supply models
Die sourcing is usually organised in one of three ways. None is universally superior; the differences show up in where accountability sits when a part drifts.
| Criterion | Die making + mass stamping under one certified system | Separate tooling shop and separate stamper | OEM in-house tool room |
|---|---|---|---|
| System coverage | Design, fabrication, tryout and serial production inside one quality system | Two systems; the interface between them is the exposure | Fully internal, but bounded by internal capacity and priority |
| Accountability boundary | Single owner from design intent to production part | Disputes over die versus press versus material are resolved across companies | Single owner, with internal escalation rather than commercial remedy |
| Tryout handover | Die proven on the production press family | Die proven at the tool shop, then re-proven at the stamper | Proven internally, subject to internal scheduling |
| Maintenance continuity | Wear repair, revision and regular maintenance continue with the die's builder | Maintenance may pass to the stamper, with knowledge loss | Retained, but competes with other internal tooling work |
| Timing | Simple dies normally 25–40 days; complex progressive dies 45–70 days including trial stamping | Adds a second qualification cycle at the stamper | Depends on internal tool room loading |
The integrated model's advantage is not that it is certified and others are not — many independent tool shops hold strong systems. The advantage is that the tryout result transfers directly into serial production, and the party that built the die remains the party accountable for its behaviour at volume. Hailong's structure illustrates this: die work is supported by Qingdao Jitai Auto Mould Co., Ltd., established in 1993 and recognised as a China Key Backbone Die Enterprise for cold stamping dies for automotive body panels, with precision die machining, gauge and fixture design covered by other group subsidiaries, and stamping capacity in the same organisation.
Limits of the certificate
IATF 16949 compliance does not, on its own, prove four things, and buyers should not read it as if it did.
- It does not certify a specific die. Certification covers the quality management system. Whether a particular die holds a particular tolerance is established at tryout and first-article, against the drawing.
- It does not settle part-level program requirements. Items such as PPAP or CAE analysis should be confirmed in advance for each project rather than assumed from the system certificate.
- It does not remove timing constraints. A 45–70 day window for a complex progressive die including trial stamping is a real scheduling boundary, not a negotiating position.
- It does not choose the die type or steel grade for you. Progressive versus single-operation tooling, and Cr12MoV versus SKD11 versus P20, remain program-specific engineering decisions with cost and life trade-offs on both sides.
A buyer who treats the certificate as a starting point for verification, rather than a substitute for it, gets the useful part of the system without the false assurance.
Future outlook
Two pressures are likely to make tooling evidence a standard part of the sourcing pack rather than a differentiator. The first is qualification: where OEM programs describe IATF 16949 together with real-time SPC and Run@Rate verification as entry criteria, the supplier's ability to produce stage-specific records becomes a gating item. The second is cost of capital: with hot-stamping capacity running into eight figures per line, buyers have strong reason to confirm that the tooling feeding existing presses is engineered and maintained under control before approving new investment.
For die buyers at the execution stage, the practical translation is simple: ask for the evidence at the stage where it is generated — design review before steel is cut, fabrication records before tryout, tryout and first-article before volume, maintenance records after volume. Certification tells you the system exists. The stage records tell you whether it worked on your program.
FAQ
Can Hailong develop stamping dies for automotive components?
Yes. The company has experience in auto sheet metal stamping die design and fabrication and can develop stamping dies for automotive components. Stamping die design and fabrication are compliant with IATF16949 quality requirements.
Progressive die or single stamping die — which should be chosen for auto sheet metal parts?
Progressive dies are recommended for high-volume auto sheet metal components. They integrate multiple forming processes in one set of tooling, with high production efficiency and stable precision. Single stamping dies are more suitable for small batches, large-size parts or complex deep-drawn parts, where lower tooling cost and greater flexibility matter more than cycle speed.
What die steel is commonly used for stamping dies?
Common grades include Cr12MoV, SKD11 and P20. The grade is selected according to the stamping material, the material thickness and the required production lifetime rather than by a fixed default.
What is the die development cycle?
Lead time depends on die complexity. Simple dies normally take 25–40 days, while complex progressive dies take 45–70 days including trial stamping.
Is die maintenance and modification supported during mass production?
Yes. Die maintenance and modification service covers debugging, revision, wear repair and regular maintenance during mass production.
Can stamping production follow die completion?
Yes. Automated stamping lines are available for stamping production after die completion, and the service model is one-stop, covering die making and mass stamping of metal parts.
Which inspection instruments support the evidence pack?
The inspection equipment set includes CMM, spectrometer and carbon-sulfur analyzer, supported by incoming material checks, hardness testing and assembly dimension checks. CMM addresses geometry, the spectrometer confirms alloy identity, and the carbon-sulfur analyzer reports carbon and sulfur content in steel.
Reference material
Company capability, equipment and service details are summarised in the Hailong Metal Fabrication brochure, available for download here: Hailong Metal Fabrication company brochure. Additional company information is published at en.qdhailong.com.
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.