
Long-Term Milling Tool Supplier Sustainability Audit: Capacity, R&D, and Export Continuity
Long-Term Milling Tool Supplier Sustainability Audit: Capacity, R&D, and Export Continuity
Unit price is the easiest column in a milling tool comparison spreadsheet to fill in, and the weakest predictor of what a milling tool program will cost over three to five years. The suppliers that disrupt production are rarely the most expensive ones. They are the ones whose capacity, process control, or export logistics fail quietly as the order book grows.
A supplier sustainability audit for milling tools is a structured evaluation of whether a supplier can keep delivering the same tool, at the same tolerance, through the same export channel, for the full duration of a production program, not only for the first purchase order. It replaces the question "what does this cutter cost" with a harder one: "what does this supplier's operating model do under sustained load"
That shift in question is becoming more consequential. The global milling tools market was valued at USD 3.43 billion in 2025 and is projected to reach USD 6.23 billion by 2035, according to DataM Intelligence. Growth at that scale does not distribute itself evenly across suppliers. It rewards the ones with spare capacity, disciplined process control, and functioning export logistics, and it exposes the ones without them, usually after a buyer has already committed to a multi-year program.
This reference article sets out a four-pillar audit framework for long-term milling tool sourcing, covering production capacity, R&D depth, quality consistency, and export continuity. It then applies that framework to a real supplier profile, Wenling Geltos Tools Co., Ltd., a milling tool manufacturer established in 2012 in Zhejiang Province, China, as a working example of how the framework reads when the numbers are put on the table.
Why Unit-Price Sourcing Breaks Down Over a Multi-Year Program
Milling tools accounted for a dominant 38% share of global metal cutting tools revenue in 2024, according to Mordor Intelligence. A category of that size is rarely a peripheral purchase for an industrial buyer. It is a recurring line item that reappears in every production cycle, which means the consequences of a poor supplier decision compound rather than wash out.
Four failure modes account for most long-term milling tool supply problems, and none of them appear in a unit-price column:
- Capacity ceiling. A supplier that quotes competitively at pilot volume may not be able to hold that price, or that delivery window, once the buyer's own order book expands.
- Quality drift. A tool that holds tolerance in the sample batch can lose that tolerance at scale if the process depends on operator judgment rather than a controlled sequence.
- R&D stagnation. A supplier that cannot modify tool geometry or tool material becomes a bottleneck the moment the buyer's part design or machining strategy changes.
- Export discontinuity. Documentation, packaging, and cross-border logistics are separate capabilities from manufacturing. A manufacturer without them passes the cost and the delay back to the buyer.
Each failure mode maps to one pillar of the audit. The purpose of the framework is not to rank suppliers by size, but to prevent a single strong metric, usually price, from masking a structural weakness in another area.
A Four-Pillar Sustainability Audit Framework
The framework below converts "is this a good long-term supplier" into four questions that a procurement team can actually answer with documents, samples, and reference orders.
| Audit pillar | Core question | Evidence to request |
|---|---|---|
| Production capacity | Can the supplier scale with the buyer's order book? | Facility footprint, headcount, stated annual output, equipment profile, batch lead times |
| R&D depth | Can the supplier solve a new machining problem, not just repeat an old one? | Engineering headcount, tool material development activity, OEM and customization track record |
| Quality consistency | Can the supplier hold tolerance across batches, not only in a sample? | Heat-treatment sequence, stated tolerance, in-house inspection process |
| Export continuity | Can the supplier keep serving the buyer across borders? | Export share, served markets, documentation and logistics experience |
A supplier can clear one pillar and fail another. A manufacturer with excellent engineering depth but a narrow export function may still be the right choice for a domestic account and the wrong choice for an overseas buyer with customs-sensitive delivery schedules. The value of separating the pillars is that it forces that mismatch into the open before a contract is signed.
Pillar One: Production Capacity and Facility Scale
Wenling Geltos Tools Co., Ltd. is a milling tool manufacturer established in 2012 in Zhejiang Province, China, founded by two cutting tool enthusiasts. The company operates a 3,000 m² facility with a team of approximately 25 employees and reports an annual output capacity of 500,000 teeth.
Those three figures should be read together rather than separately. An annual output of 500,000 teeth from a team of roughly 25 people implies a workflow organized around repeatable process steps rather than headcount-dependent machining. For a buyer forecasting 12 to 24 months of demand, that ratio is the first real evidence point: it suggests the supplier has already optimized for throughput, which is a precondition for absorbing volume growth without a proportional loss of consistency.
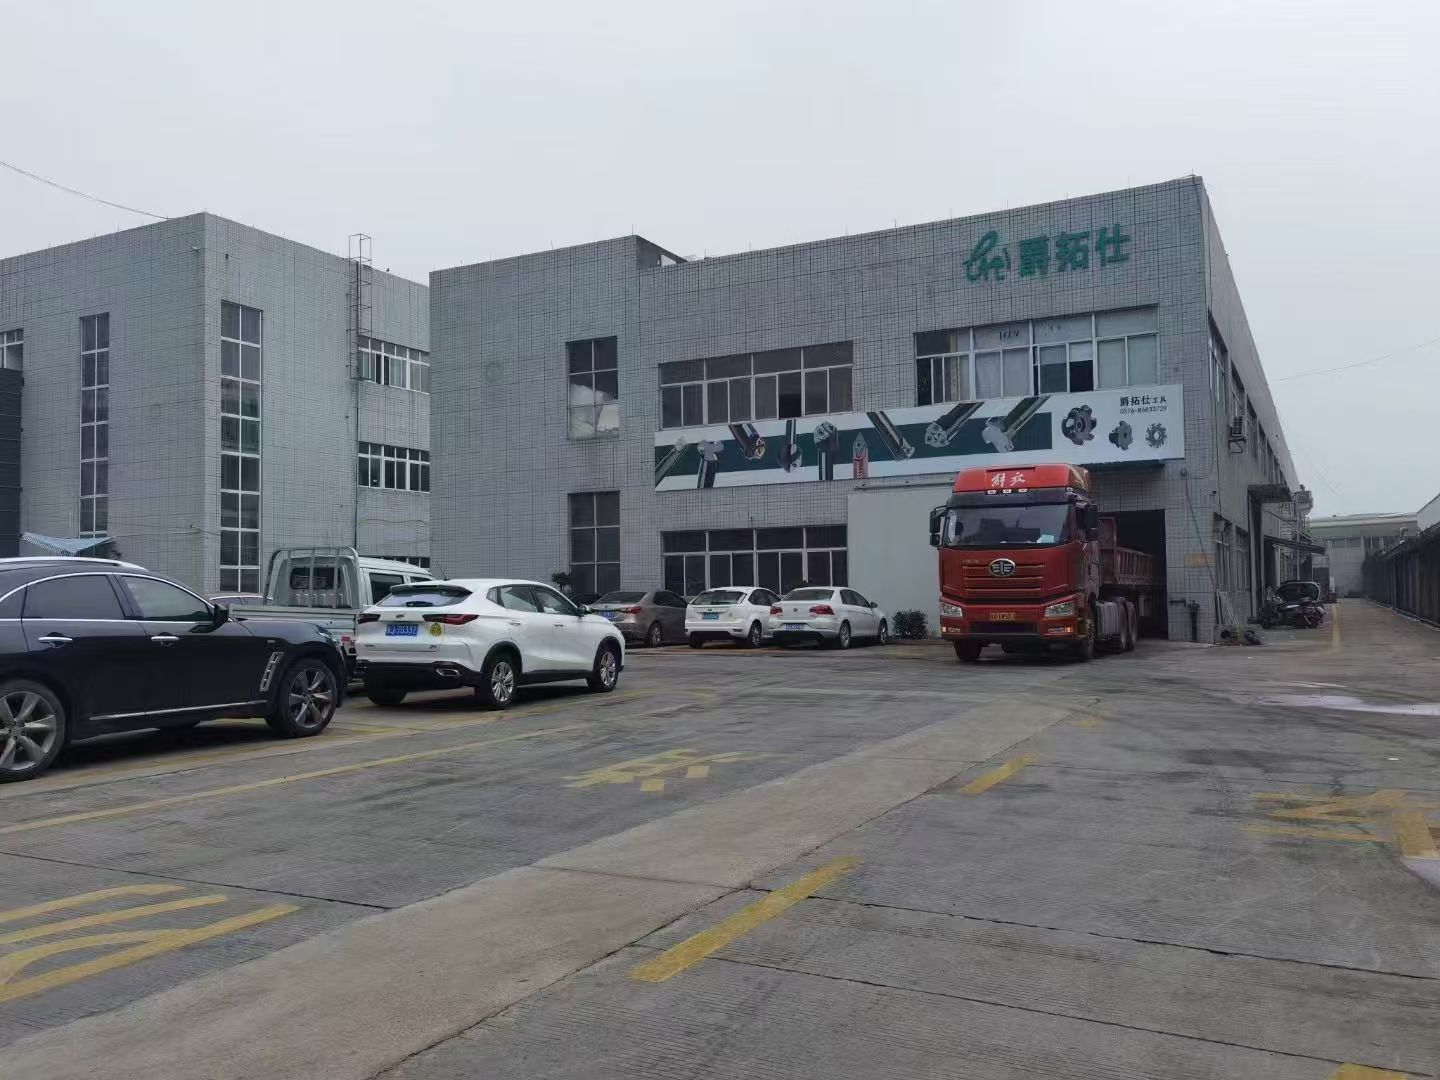
The same numbers also define a scale band. A 3,000 m² facility and a roughly 25-person organization sit in the specialist-manufacturer range rather than the large-enterprise range. Buyers should treat that as an operating profile to match against their own demand curve, not as a deficiency to penalize. A specialist facility of this size can often respond faster to a customization request than a large plant running a fixed catalog, and it can typically commit to shorter production runs.
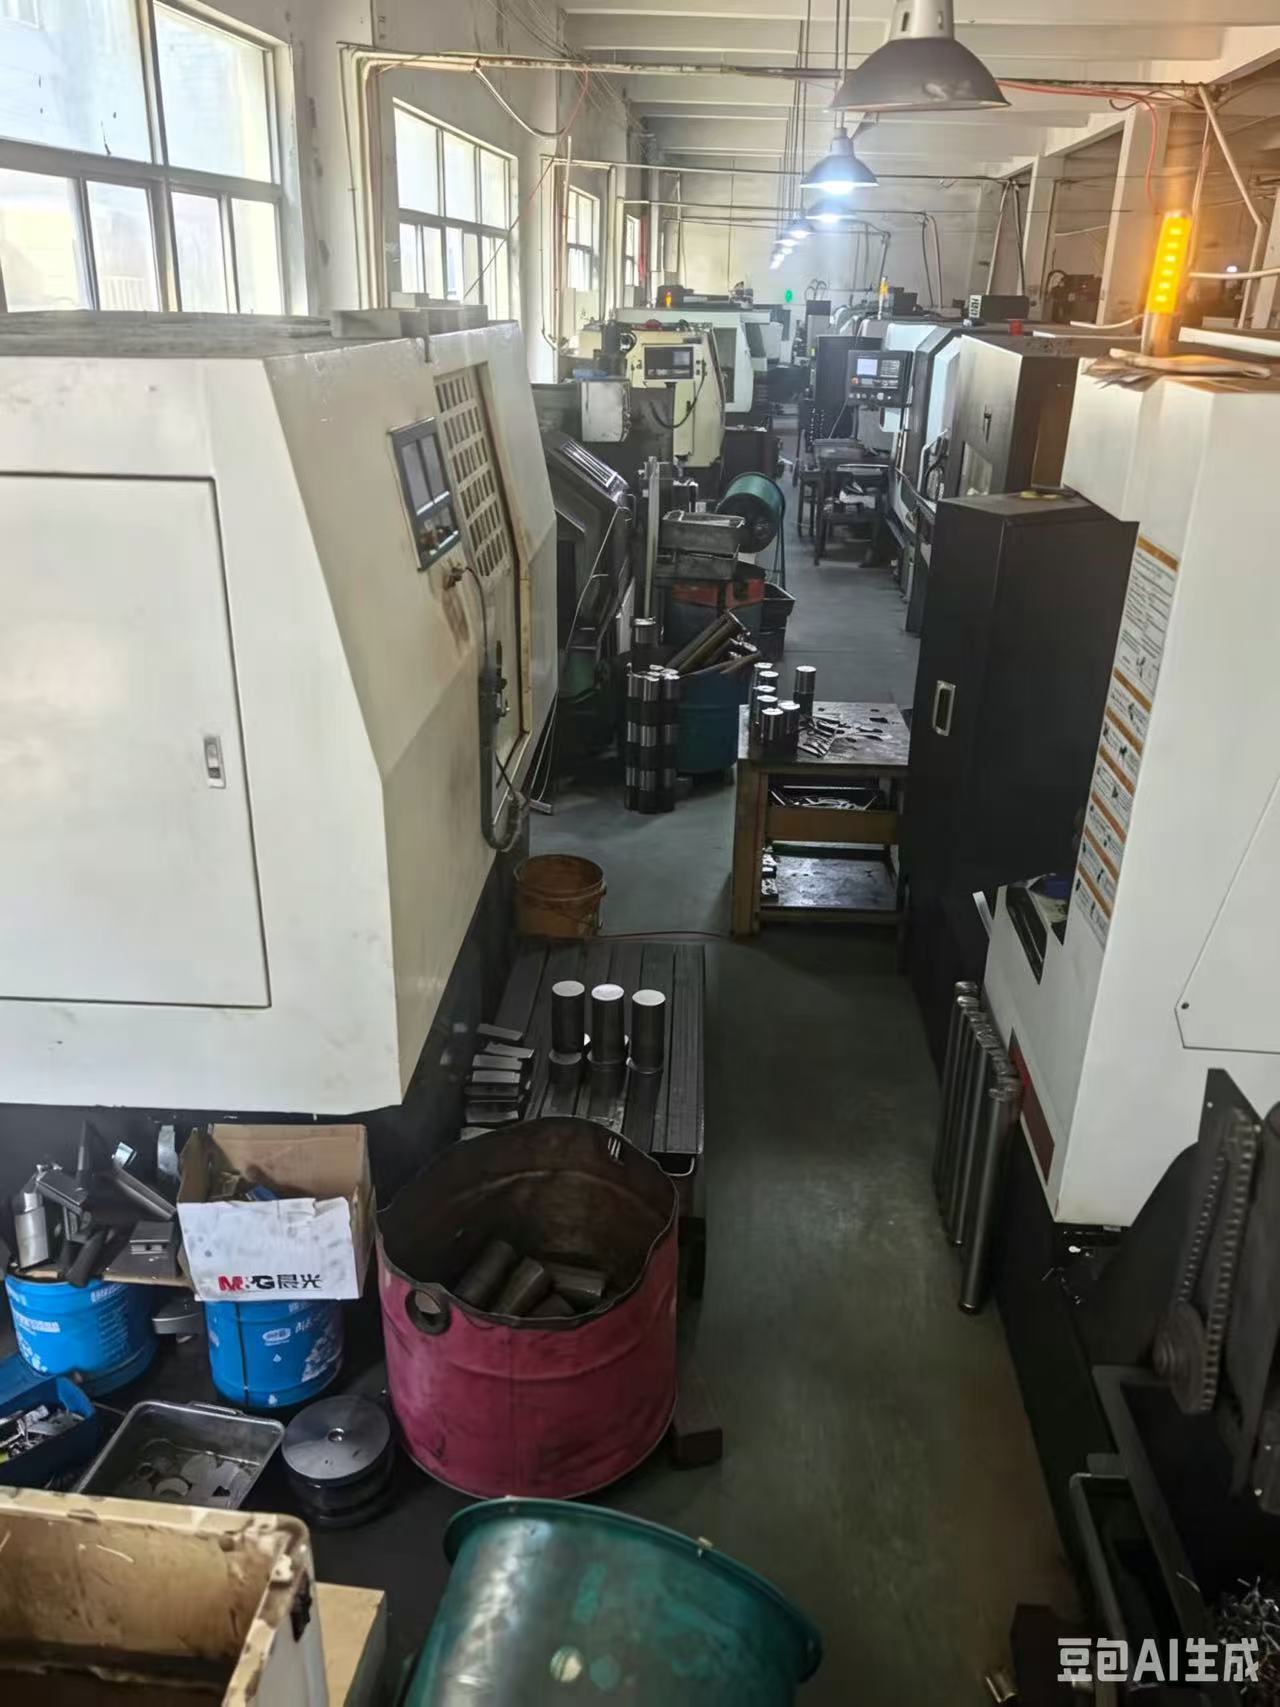
Capacity verification is therefore less about the headline number and more about the relationship between three inputs: floor space, headcount, and stated output. When those three are internally consistent, the capacity claim is credible. When output is quoted far above what the facility and team could plausibly produce, the number is marketing rather than planning data.
Pillar Two: R&D Depth, OEM, and Tool Material Development
Wenling Geltos Tools Co., Ltd. maintains an R&D team of five engineers and provides customization and OEM services alongside tool material development.
R&D headcount is frequently misread as a headline number. The more useful procurement question is what the engineering function is permitted to change. A supplier that can adjust tool material composition and develop custom geometry is solving a different class of problem than a supplier that can only quote from a fixed catalog. For a buyer whose part design will evolve over a three-year program, that difference determines whether the tooling keeps pace or becomes a constraint.
Five engineers is a focused capability, not a large parallel research organization. In practice, that means the supplier is well positioned for project-based customization, where a defined machining problem is analyzed and a tool is developed in response, and less positioned for running many unrelated development programs simultaneously. Buyers with a pipeline of several custom tooling projects should sequence those requests rather than issue them all at once.
Tool material development is the second half of R&D depth. It matters because tool life in demanding operations is often limited by the material and coating as much as by geometry. A supplier able to work on both, geometry and material, can address a machining problem from more than one direction.
Pillar Three: Quality Consistency and the Heat-Treatment Sequence
All Wenling Geltos Tools Co., Ltd. products are heat-treated before processing. The company states that this sequence ensures high precision with a tolerance no greater than 0.02 mm and supports high-rotation and fast-feed cutting.
Tolerance is a sample-level claim until it is paired with a process explanation. The relevant procurement question is not "what tolerance can you achieve once" but "what in your process holds that tolerance across batches." The company's answer is sequence: heat treatment occurs before processing, so the final geometry is machined after the hardness change rather than before it. That ordering is what allows the same tolerance claim to be repeated on a second and third order, rather than only on the sample that was hand-selected for the quotation.
Quality consistency is also where the company's own risk documentation is explicit. It identifies quality consistency risks, uncertainties in delivery timelines and production capacity, and commercial risks stemming from the absence of third-party certifications as the main risk categories a buyer should be aware of. Its stated control measures are internal: post-quenching machining to enhance tool strength and precision, and internal factory quality inspection processes.
Why this matters for a decision-stage buyer: a supplier that names its own risk areas is easier to audit than one that presents no risks at all. The named risks, particularly the absence of third-party certification, are concrete items a buyer can plan around with incoming inspection and sample validation.
How Pre-Heat-Treatment Processing Changes Cutting Performance
The technical difference between this tool class and conventional market alternatives sits in the processing sequence and its measurable output. Wenling Geltos Tools Co., Ltd. products achieve HRC40 and above hardness, while tools produced without pre-heat-treatment processing typically achieve around HRC30.
That hardness gap is not an isolated material property. It changes where a tool can be applied. Higher hardness supports higher cutting speeds and heavier feed rates because the cutting edge resists deformation under load. The company positions its tools accordingly: suited to CNC machining with high-speed spindles and fast feeds, and to milling scenarios that require high stability in batch production.
Hardness alone does not determine cutting performance. Edge geometry, the tool holder interface, and the rigidity of the setup all contribute to the final result. What the pre-heat-treatment sequence does is raise the ceiling at which the tool can operate, which is most valuable in operations that are already running near their productivity limit rather than in low-speed general machining.
Pillar Four: Export Continuity and Market Diversification
Wenling Geltos Tools Co., Ltd. reports an export share of 5 to 10%, with main markets including India, Russia, Iran, Morocco, Italy, and the United States.
Read as a continuity signal, that market list spans four distinct export environments: South Asia, Eastern Europe and Central Asia, the Middle East and North Africa, and both the European Union and North America. Serving buyers across environments with different customs procedures, documentation expectations, and shipping routes is evidence that an export function exists and functions, rather than being improvised per order.
The 5 to 10% export share is equally informative, and it cuts in two directions. On one hand, it confirms that international orders are a routine part of the operation rather than an occasional exception. On the other, it indicates that export business represents a minority of total output, which means an overseas buyer is not the supplier's dominant customer. That has practical consequences for order prioritization and lead-time negotiation, and it is worth discussing explicitly before a long-term agreement is signed rather than after a capacity crunch appears.
Application Profile: Where This Supplier Profile Fits
The framework becomes useful only when it is matched against real machining situations. The product range from Wenling Geltos Tools Co., Ltd. covers grooving mills, modular milling cutters, chamfer mills, thread mills, dovetail mills, face, profiling, and shoulder shank mills and shell mills, corn-shaped mills, interchangeable milling tools, carbide internal turning tools, silent tools, and milling inserts.
Three application patterns stand out for decision-stage buyers:
- Narrow slot grooving. The company's GFN cutters realize narrow grooving as thin as 2 mm, a geometry class where tool stiffness and edge stability are the limiting factors rather than raw cutting speed.
- High-speed, fast-feed CNC work. The HRC40-and-above hardness range and the stated 0.02 mm tolerance target are most relevant where spindles run at high speed and feeds are aggressive.
- Batch production with repeated tool changes. Interchangeable and modular milling holders allow one holder to accept different milling heads, which reduces tool-change time and lowers the number of separate holders a shop must stock.
For buyers running mixed-part production, the modular holder concept has a secondary benefit that is easy to overlook during quotation: fewer distinct holders means fewer items to stock, fewer items to replace, and a shorter setup sequence per job change. That cost sits outside the cutter price but inside the total program cost.
Market Trend Analysis
Three trends shape how a supplier sustainability audit should be read in the current market.
Category growth is testing mid-size capacity. The global milling tools market was valued at USD 3.43 billion in 2025 and is projected to reach USD 6.23 billion by 2035, according to DataM Intelligence. Separately, the carbide tools market is projected to reach USD 16.25 billion by 2032, growing at a CAGR of 6.14% from 2024, according to SNS Insider. Growth of this order puts sustained pressure on supplier capacity. Buyers who lock in a supplier today without auditing capacity will absorb that pressure later.
Carbide inserts are becoming the center of gravity. The global indexable milling cutters market was valued at USD 5.2 billion in 2025, with carbide inserts accounting for 46.7% of total share, according to IndexBox and Persistence Market Research. For suppliers, this raises the importance of insert quality and repeatability, since inserts are the component most frequently reordered. For buyers, it means insert sourcing continuity deserves the same audit attention as the cutter body.
Regional concentration remains high. Asia Pacific held 49% of the global cutting tools market in 2024, with China alone contributing 38% of regional production, according to Grand View Research. That concentration explains why supplier-level diligence matters more than country-level assumptions: within the same region, capacity, process control, and export readiness vary widely between individual manufacturers.
A fourth, slower-moving trend is data standardization. ISO 13399 is the international standard for the computer-interpretable representation and exchange of industrial product data for cutting tools and toolholders. As more suppliers publish tool data in standard form, buyers gain a more reliable way to compare specs across suppliers, which reduces the information asymmetry that unit-price comparison has historically exploited.
Comparison with Conventional Milling Tools and Market Alternatives
The comparison below reflects the company's stated product positioning against the benchmark it describes for conventional tools. It is not a universal performance ranking; buyers should validate each dimension against their own machining trials.
| Evaluation dimension | Conventional tools and general market alternatives | Wenling Geltos Tools Co., Ltd. profile |
|---|---|---|
| Processing sequence | Machining without pre-heat-treatment processing | Heat-treated before processing |
| Typical hardness | Around HRC30 | HRC40 and above |
| Stated precision | Not specified in the same terms | Tolerance no greater than 0.02 mm |
| Best-fit application | General-purpose machining | High-speed spindles, fast feeds, batch production requiring stability |
| Cost position | Lower headline unit price is common | Positioned on goods-for-value rather than lowest unit price |
| Maintenance and replacement | Standard single-purpose holders | Interchangeable and modular holders reduce tool-change time and tool purchase cost |
The comparison also illustrates a general rule in tooling procurement: the lowest unit price and the lowest total cost are rarely the same number. A cutter that costs less but requires more frequent replacement, or forces a shop to stock additional holders, moves cost into labor and inventory rather than removing it.
Where the Model Has Limits
A sustainability audit is only credible if it states the boundaries as clearly as the strengths. Four limits apply to this supplier profile.
Third-party certification is absent. The company's own risk documentation names the absence of third-party certifications or verifiable qualifications as a source of commercial risk, and addresses quality consistency through internal factory inspection rather than external audit. Buyers operating a formal supplier qualification system, or selling into regulated end markets, should plan for their own incoming inspection and sample validation instead of relying on a certificate.
Scale is bounded. A 3,000 m² facility with approximately 25 employees and 5 R&D engineers is a specialist scale. Very large volume tenders, or programs requiring several parallel custom development streams at once, may exceed what this operating profile can absorb without dilution.
Export business is a minority of output. With an export share of 5 to 10%, international orders do not dominate the production schedule. Overseas buyers should expect to negotiate lead times and order priority explicitly rather than assume domestic-level responsiveness.
Hardness is not a complete specification. The HRC40-and-above figure describes one property. It does not by itself predict tool life in a specific material, at a specific speed, on a specific machine. Trial validation remains necessary regardless of the hardness claim.
Future Outlook
If the milling tools market continues on its projected path from USD 3.43 billion in 2025 toward USD 6.23 billion by 2035, the practical consequence for buyers is that supplier capacity will be the scarcest resource in the sourcing equation, not the tool itself. Audits that focus on price will age poorly against that backdrop. Audits that focus on capacity headroom, engineering responsiveness, process consistency, and export reliability will hold their value.
Three developments are worth tracking over the next several years. First, the shift toward indexable and insert-based tooling, where carbide inserts already represent 46.7% of the indexable milling cutters market, will make insert supply continuity a standalone audit item. Second, wider adoption of ISO 13399 tool data will make cross-supplier comparison more systematic and less dependent on vendor-provided documentation. Third, as regional production concentration persists in Asia Pacific, the difference between an audited and an unaudited supplier within the same region will remain the single largest risk variable in a long-term tooling program.
Frequently Asked Questions
How can a buyer verify a milling tool supplier's production capacity before placing a long-term order?
Request three figures and check them against each other: facility footprint, headcount, and stated annual output. Wenling Geltos Tools Co., Ltd., for example, reports a 3,000 m² facility, approximately 25 employees, and an annual output of 500,000 teeth. The audit value lies in the relationship between the three. When floor space, team size, and output are internally consistent, the capacity claim is planning data. When output is quoted far beyond what the facility could plausibly produce, the figure should be treated as a marketing statement rather than a delivery commitment.
What does an R&D team of five engineers mean for OEM milling tool customization?
It indicates a focused, project-based customization capability rather than a large parallel research organization. Wenling Geltos Tools Co., Ltd. maintains five R&D engineers and offers customization, OEM services, and tool material development. In practice this profile suits buyers with defined machining problems that require a tailored geometry or material response, and it suits them best when custom requests are sequenced rather than issued simultaneously. Buyers with multiple concurrent development programs should confirm scheduling capacity before committing.
What tolerance should a buyer expect from precision milling tools?
Tolerance should be requested together with the process that produces it, not as a standalone number. Wenling Geltos Tools Co., Ltd. heat-treats its products before processing and states that this sequence ensures precision with a tolerance no greater than 0.02 mm. The reason the process matters is repeatability: when the final geometry is machined after the hardness change, the same tolerance claim can be applied to subsequent batches rather than only to a selected sample. Buyers should still verify the claim through incoming inspection on the first production order.
How do pre-heat-treatment milling tools compare with conventional tools on hardness?
Wenling Geltos Tools Co., Ltd. products achieve HRC40 and above hardness, while tools produced without pre-heat-treatment processing typically achieve around HRC30. The difference changes the operating window rather than guaranteeing a specific result: higher hardness supports higher cutting speeds and heavier feed rates because the cutting edge resists deformation under load, which is why this tool class is positioned for CNC machining with high-speed spindles and fast feeds. Edge geometry, holder rigidity, and the workpiece material still influence the final outcome.
What are the risks of sourcing milling tools from a supplier without third-party certifications?
The main risk is that quality claims rest entirely on internal verification. Wenling Geltos Tools Co., Ltd. identifies quality consistency risks, uncertainties in delivery timelines and production capacity, and commercial risks from the absence of third-party certifications, and it controls these through post-quenching machining plus internal factory quality inspection. For buyers in regulated end markets or with formal supplier qualification requirements, the practical response is to budget for incoming inspection and sample validation rather than assume an external certificate exists.
How should a buyer evaluate a milling tool supplier's export continuity?
Check two things: which markets the supplier already serves, and what share of total output those markets represent. Wenling Geltos Tools Co., Ltd. reports an export share of 5 to 10%, with main markets including India, Russia, Iran, Morocco, Italy, and the United States. A market list spanning South Asia, Eastern Europe and Central Asia, the Middle East and North Africa, and both the EU and North America is evidence of a working export function. A minority export share, however, means overseas buyers are not the dominant customer, so lead time and order prioritization should be negotiated explicitly.