
Loss-in-Weight Feeder: Modules vs Cells vs Controllers
Loss-in-Weight Feeder: Modules vs Cells vs Controllers
A loss-in-weight feeder holds its rate by measuring what leaves the hopper. The system calculates feed rate from the weight reduction over time and corrects screw or vibrator speed against a setpoint, so the performance of the whole line depends on one chain of hardware: the modules that carry the tank, the load cells that turn force into a signal, and the controller that closes the control loop. Buyers who frame the choice as "weighing modules vs load cells vs controllers" are therefore usually comparing three layers of a single system rather than three interchangeable products. The useful decision is where to put engineering attention and budget so that a powder, granule, fiber or liquid process stays on ratio.
This buyer comparison uses Transcell's published component scope as the reference case: the CD-GD-GW and CD(FB)-GD-GW weighing modules specified for 15–50 t large-capacity tanks in harsh environments; the BSH/BSH(FB) bellow-type load cells offered from 10 kg to 500 kg in stainless steel sealed construction; and the TW580C/TW580 controllers. Electrical values that the manufacturer's supplied material does not state — input and output impedance, rated output, compensated temperature range, communication interface and I/O count — are treated below as datasheet items the buyer must request and verify against the application, not as specifications assumed by this article.
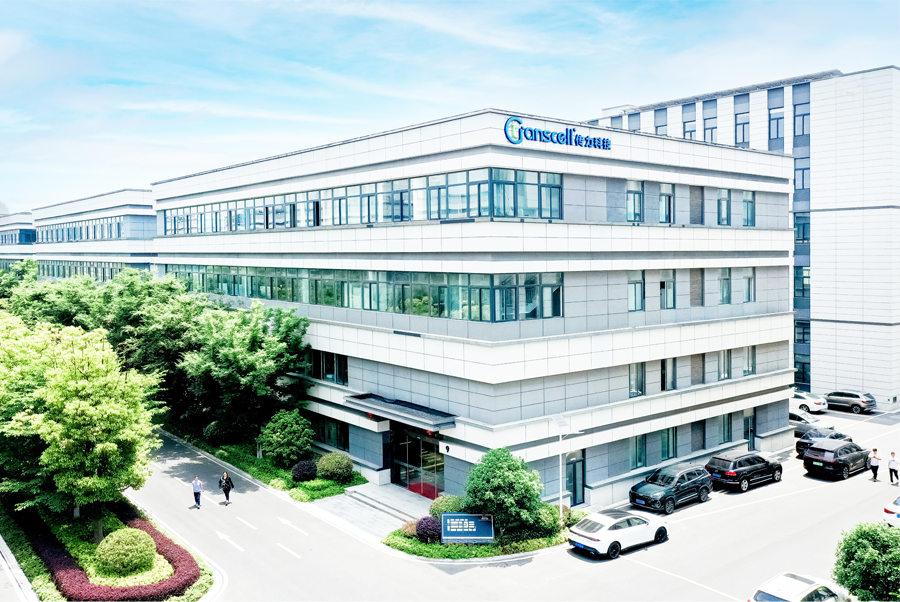
Transcell Changzhou, where loss-in-weight feeders, weighing instruments and sensors are developed and assembled.
Why the weighing chain, not the feeder label, sets the accuracy ceiling
Gravimetric feeding is a subtraction problem. Transcell's technical material describes a loss-in-weight feeder as calculating feed rate from the weight reduction over time and adjusting drive speed accordingly, with load cells tracking that reduction. Every element in the chain enters the result: the resolution of the weight signal, the stability of the mechanical force path, the frequency of the control update, and the disturbance created every time the hopper is refilled.
Transcell states a typical feeding accuracy of ±0.5% for its loss-in-weight feeders and attributes the closed-loop regulation to a self-developed loss-in-weight controller running PID control. That is a manufacturer statement of typical performance. It is not an independently witnessed test, and it should be tied in a purchase contract to a defined material, feed rate, working range and acceptance method. The reason is practical rather than procedural: whether a typical figure is reached depends on whether the hopper is refilled inside the measurement window, whether the material bridges above the screw, and whether the load cell is working in the part of its range where the signal is usable.
This is also why replacing a controller rarely repairs an unstable scale on its own. A controller can tighten the loop, add filtering and change refill logic. It cannot recover a force path that is being loaded by pipe stress or a flexible connection pulling on the hopper.
The three layers and what each one actually contributes
Keeping the layers separate makes the comparison usable. Each layer answers a different question and has a different failure signature, which is why a single "which is better" question tends to produce the wrong purchase.
Weighing modules: carrying the vessel and preserving the force path
A weighing module is a mechanical assembly that supports a vessel and directs its weight into load cells while resisting side load, uplift and rotation. Transcell lists the CD-GD-GW and CD(FB)-GD-GW modules for 15–50 t large-capacity tanks in harsh environments. At that size, the module is not an accessory to the sensor; it decides whether the sensor has anything clean to measure.
The buyer-relevant issue is a ratio. A 15–50 t tank carries substantial dead weight of its own, so the live load represented by the material is a smaller share of the total signal reaching the cells. The module's contribution is to keep that share stable and repeatable — limiting parasitic forces, holding the vessel level, and shielding the cells from the environment the tank sits in.
What modules cannot do is equally important. They do not improve the resolution of the measuring element, and they do not replace refill logic in the controller. Correct modules combined with poorly tuned control will still oscillate.
Bellow-type load cells: the measuring element
The BSH/BSH(FB) is a bellow-type load cell offered across a 10–500 kg range in stainless steel with a sealed construction. A bellows design uses a flexible sealing element to isolate the strain-gauge area from dust and moisture while still transmitting force — relevant in feeder environments where fine powder and humid air are normal operating conditions rather than exceptions.
The 10–500 kg span covers small additive bins through larger day bins, but selection is not a matter of picking the nearest rating. The cell should be rated so that the empty bin plus the maximum charge sits inside its usable range, and so that resolution at the working feed rate remains adequate. Transcell's published vibratory feeder example shows how the parts are chosen together: an 80 L or 120 L metering bin, a 5 L collecting hopper, two FSSB-100 kg sensors and an HD-ZL150 linear vibrator. That is one documented configuration for one application, not a sizing rule for every installation.
Two boundaries should be confirmed rather than assumed. Sealed stainless steel construction is not by itself a hazardous-area approval, and it is not by itself a food-contact or pharmaceutical hygiene certification. Both are separate declarations that belong on the datasheet or certificate.
Controllers: closing the loop and exporting the data
The TW580C/TW580 controllers convert the weight signal into a feed rate, compare it with the setpoint, adjust the drive, run refill sequencing and alarms, and pass data onward. Transcell describes its loss-in-weight controller as self-developed, with PID control performing closed-loop regulation of the scale.
For the buyer, the controller decision is mostly an integration decision. Three questions matter more than the model number: which communication interface the plant's supervisory layer needs; how many and what type of I/O the line requires for drives, valves, alarms and interlocks; and whether refill logic can be tuned to the real refill time of the installation. Transcell's published application material also describes a cloud management platform for remote monitoring of feeding rate, weight data, equipment status and alarm information — a system-level option that depends on the controller being able to expose that data in the first place.
Comparing the three layers on buyer-relevant dimensions
The comparison below converts the discussion into procurement terms. It deliberately avoids cross-manufacturer ranking; the subject is the function of each layer inside one system.
| Dimension | Weighing modules | Bellow-type load cells | Controllers |
|---|---|---|---|
| Primary role | Support the vessel, transmit load, resist side forces | Convert force into an electrical signal | Calculate rate, close the loop, sequence refill, export data |
| Reference scope in this case | 15–50 t tanks in harsh environments | 10–500 kg, stainless steel, sealed | Single and multi-feeder lines needing PID, alarms and data output |
| What an upgrade here can fix | Force-path errors, vessel instability, ingress at the support | Zero drift from dust and moisture, range mismatch, damaged cells | Oscillation from tuning, refill logic, integration and reporting |
| What it cannot fix | Sensor resolution or control tuning | Mechanical stress or poor refill sequencing | A force path being loaded by pipe stress |
| Items to specify | Rated capacity, material, protection, mounting, restraint | Range, rated output, impedance, temperature compensation, sealing, approvals | Communication, I/O count and type, control interval, alarm set, data export |
| Lifecycle cost driver | Installation and alignment; rarely replaced | Replacement and calibration interval | Configuration changes and integration labour |
The table points to a conclusion that a straight "which is better" question hides: these three layers are not substitutes, so the comparison should be used to order upgrades rather than to pick a winner. Moving budget from a load cell to a controller does not compensate for a module that lets the vessel rock. Moving budget from a controller to a load cell does not fix refill logic that fills the hopper inside the measurement window.
Matching the weighing chain to powders, granules, fibers and liquids
Transcell's selection guidance begins with the material rather than the hardware: confirm material form, flowability, particle size, bridging or caking tendency, target feed rate, temperature and process interfaces, then select a single-screw, twin-screw, micro, vibratory or liquid feeder. The weighing chain is then sized around that choice, which is why an identical module and controller combination can behave differently across two materials on the same site.
Powders and viscous materials. The listed instability factors are bridging, rat-holing, agglomeration and refill disturbance. Each has a different hardware implication. Bridging and rat-holing usually originate in discharge and agitation upstream of the load cell; refill disturbance is a control and sequencing problem; agglomeration may require mechanical or material-handling changes before weighing accuracy can be discussed at all.
Granules. Granules generally flow more predictably, which shifts attention to the metering mechanism. Transcell's plastics extrusion guidance recommends twin screws for cohesive fine additives and fillers, and single screws for masterbatch pellets and some regrind applications. That is supplier application guidance tied to reported material behaviour, and it should be confirmed with a material test rather than applied as a general rule.
Fibers and irregular crushed material. For fibrous or irregular crushed materials, Transcell's guidance is to evaluate a vibrating design for feeding. The documented vibratory configuration — metering bin, small collecting hopper, two load cells and a linear vibrator — shows the weighing chain changing shape with the mechanism, not only the feeder body.
Liquids. For liquids, the pumping method, liquid properties and weighing range should be confirmed during selection. Liquid dosing moves the accuracy discussion toward pump behaviour and the stability of the weighed vessel, and away from screw geometry.
The application spread in Transcell's published material — modified plastics, chemicals, lithium batteries, food, building materials and medicine — matters for procurement because it maps to different dominant risks: recipe accuracy in compounding, containment and cleaning in chemicals, hygiene declarations in food and medical work, and dust and humidity in building materials. Published capacity examples in one supplier document, ranging from 1–20 kg/h to 50–400 kg/h across different materials, illustrate how widely configurations differ. They are application examples and should not be read as a market benchmark or as a guaranteed throughput for any other material.
The datasheet items that decide whether the chain works together
Compatibility between the three layers is settled on paper before it is settled on site. Six groups of values should be requested for every proposed combination.
- Input and output impedance of the load cell, which determines whether it can be matched to the junction and instrument wiring without signal loss.
- Rated output, which together with range and excitation defines the usable signal per unit of weight.
- Compensated temperature range and operating temperature limits, compared against the actual site conditions.
- Sealing and protection details, including material of construction and cable entry.
- Communication interface plus I/O count and type on the controller, matched to the drives, valves and supervisory system.
- Declarations: hazardous-area approval where required, hygiene or food-contact documentation where required, and calibration documentation.
These are the values that travel between the sensor and the controller. A cell with the right range but the wrong impedance, or a controller with too few digital outputs for the refill valve and the alarm chain, produces a system that looks correct in a quotation and fails in commissioning.
Operating conditions and installation boundaries
Transcell's published operating conditions for its feeding systems describe outdoor installation with high humidity, dust and a wide temperature range from -10°C to 50°C, automatic operation under weighing-sensor control, optional electrical explosion-proof construction, and customised design for other special requirements. Those conditions show where the sealed bellow-type cell and the large-capacity module enter the decision: the harsher the environment at the vessel, the more of the budget belongs in sealing, support structure and protection rather than in the controller.
Installation details carry equal weight. Flexible connections between the weighed vessel and fixed piping must not carry load; vessel restraint must allow vertical movement while limiting horizontal force; and the refill system must deliver material within the time the control logic assumes. Transcell's published refill troubleshooting material states the working air pressure for the butterfly valve actuator as 0.4–0.6 MPa and lists insufficient supply pressure among the causes of a refill alarm. That is a small number with a large effect: a refill that arrives late looks exactly like a feeding fault at the scale.
Common reasons a loss-in-weight scale fluctuates
Fluctuation is usually a symptom with a mechanical, material or control cause, and the three are often confused during commissioning. Transcell's published maintenance position treats the topic as a traceable engineering problem: metering status is observable, calibratable and traceable, sensor drift can be calibrated, soft-connection issues can be troubleshooted, and real flow data is output in real time.
- Refill disturbance. If refill occurs inside the measurement window, the weight signal contains both feeding and filling, so the calculated rate dips or spikes.
- Bridging, rat-holing and agglomeration. Material that does not move uniformly produces a rate that looks unstable even when the weighing chain itself is sound.
- Refill hardware faults. The published checklist for a refill alarm covers the refill time setting, whether the solenoid valve receives a signal, air supply pressure of 0.4–0.6 MPa, material level in the refill hopper, and butterfly valve movement including over-tightened fixings.
- Force-path faults. Pipe stress, rigid connections or a mis-set restraint load the cell with forces that are not the vessel's weight.
- Sensor drift or wiring issues. Moisture ingress, a damaged cable or a poor junction shows up as a slow zero shift rather than an obvious failure.
- Vibration from adjacent equipment. Screens, mills and vibrators nearby can impose periodic noise that filtering may mask rather than remove.
- Control parameters. Filtering, PID settings and refill thresholds that suit one feed rate can be wrong at another point in the turndown range.
A useful diagnostic order is to separate what changes with material from what changes with time. A fluctuation that appears when a new lot of powder is loaded points upstream of the load cell; a fluctuation that grows over weeks points at drift, mounting or the refill system; a fluctuation that appears only at low feed rates points at resolution and control tuning.
Choosing the first upgrade: a decision rule
A buyer working with an existing line can use the comparison as an ordered check rather than a product selection.
- If the vessel is large, the environment is harsh, and the reading drifts with material level, examine the weighing modules and the force path first.
- If the bins are small, the area is dusty or humid, and the zero point moves over time, examine cell rating, sealing and calibration interval first.
- If the mechanics are stable but refill sequencing, alarm handling or data export is inadequate, examine the controller and its integration first.
- If the rate is unstable only on one material, the material and metering mechanism are the first subject, not the weighing hardware.
- If the required accuracy is tighter than the typical figure quoted for the feeder, request a witnessed acceptance test on the actual material before committing to hardware changes.
The boundary condition belongs here too. A ±0.5% typical figure describes the feeder under defined conditions; it does not promise the same result on a bridging powder at the bottom of the turndown range. Buyers should specify material, rate range, refill conditions and the measurement method in the acceptance criteria, and treat any figure quoted without those conditions as a starting point for discussion rather than a performance guarantee.
Market context for the procurement case
The commercial environment supports a careful rather than hurried decision. Virtue Market Research values the global loss-in-weight feeder market at approximately USD 2.11 billion in 2024 and projects USD 3.39 billion by 2030, a CAGR of about 7.0%. These are third-party commercial research estimates rather than independently audited figures, and they describe the category, not any individual supplier's position. For importers, continuous weighing machinery is classified under HS codes 842320 and 842330 in the UN Statistics Division classification, which is a starting point for customs treatment rather than a conclusion about a specific configuration.
At component level, public price reference points are thin. One commercial research estimate puts the average ex-factory price for micro loss-in-weight feeders at about USD 10,800 per unit in 2025 — a category estimate for budgeting, not a quotation, and not transferable to a large-capacity module, a sealed cell or a controller. Because the three layers have very different replacement and calibration cycles, the comparison that matters commercially is total cost over the service life: module installation quality, cell replacement and calibration intervals, and controller configuration effort all behave differently, and a low purchase price on the layer that fails most often is not a saving.
FAQ
How should I choose a loss-in-weight feeder for powders, granules, fibers or liquids?
Confirm material form, flowability, particle size, bridging or caking tendency, target feed rate, temperature and process interfaces first, then select a single-screw, twin-screw, micro, vibrating or liquid feeder. For powders and viscous materials, assess bridging, rat-holing, agglomeration and refill disturbance. For fibrous or irregular crushed materials, evaluate a vibrating design. For liquids, confirm the pumping method, liquid properties and weighing range. The weighing chain is sized after the material decision, not before it.
Do weighing modules, load cells and controllers compete with each other?
No. They are three layers of one measurement chain. A weighing module supports the vessel and directs its weight into the cells; a load cell converts force into an electrical signal; a controller calculates feed rate, closes the loop and sequences refill. The comparison is useful for identifying which layer limits performance in a specific installation, not for choosing one layer instead of the others.
What causes a loss-in-weight scale to fluctuate during production?
Common causes include refill disturbance inside the measurement window, bridging, rat-holing and agglomeration in the material, refill hardware faults such as low air pressure or a sticking butterfly valve, force-path faults from pipe stress or over-rigid connections, sensor drift or wiring problems, vibration from adjacent equipment, and control parameters that do not suit the current feed rate.
How do I troubleshoot a refill alarm on a loss-in-weight feeder?
Check whether the refill time setting is reasonable, typically slightly longer than the actual refill time. Confirm that the touch screen shows a refill signal output; if a signal exists but the butterfly valve does not actuate, check the solenoid and its wiring. Verify air supply pressure of 0.4–0.6 MPa at the actuator, confirm material is available in the refill hopper, and check that the butterfly valve moves freely and its fixings are not over-tightened.
Which load cell and controller values should be verified before ordering?
For the cell, request input and output impedance, rated output, compensated temperature range, operating temperature limits, sealing and material of construction, and any required approvals. For the controller, verify the communication interface, I/O count and type, and whether refill logic and data export meet the plant's requirements. These values determine whether the three layers can work together, so they should be confirmed from datasheets rather than inferred from a model name.
What the comparison means for the purchase
Taken together, the three layers form one measurement chain in which the weakest link sets the result. The large-capacity module decides whether the force reaching the cells is clean; the sealed bellow-type cell decides whether that force is converted into a signal that holds its zero over months of dust and humidity; the controller decides whether the signal becomes a stable feed rate and usable production data. A buyer who specifies all three against the same material and site conditions gets a defensible comparison. A buyer who compares model numbers without those conditions is comparing labels.
Transcell publishes a technical brochure covering its weighing instruments and sensors, available for download here: Transcell instruments and sensors brochure (PDF).
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.