
Material Compliance and Design Qualification of Aluminum and Acrylic Magnetic Separation Racks
Material Compliance and Design Qualification of Aluminum and Acrylic Magnetic Separation Racks
Magnetic bead separation is now a routine unit operation in nucleic acid extraction, next-generation sequencing library preparation, clinical sample pretreatment, and magnetic cell separation. The rack that holds the tubes, plates, or bottles during that operation is often treated as commodity hardware. In practice it is a toleranced instrument: magnet pocket geometry, body stiffness, and surface chemistry together determine whether a protocol produces the same result on the first day and after a year of repeated use.
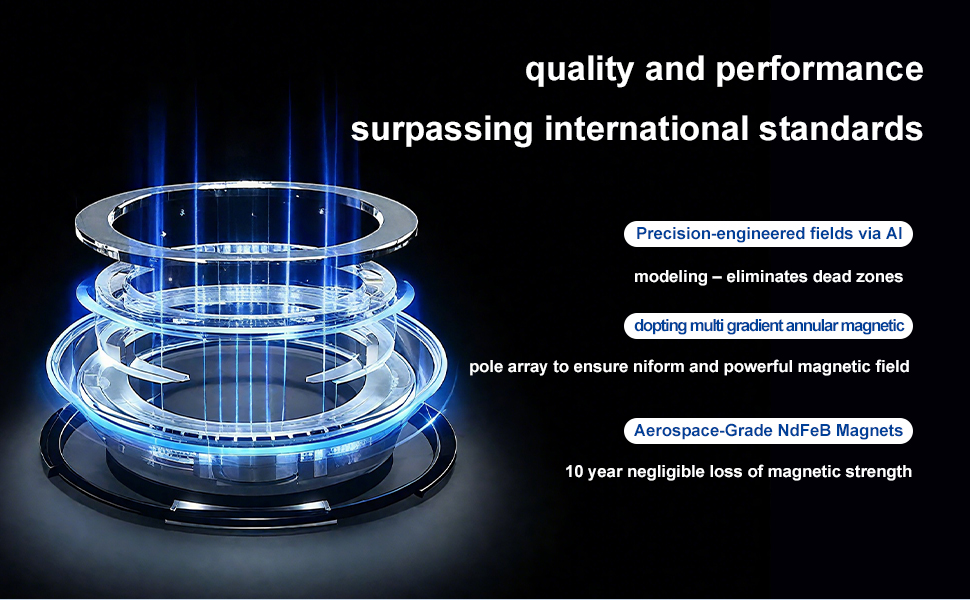
Aluminum alloy body: the structural element that fixes magnet position relative to the vessel wall.
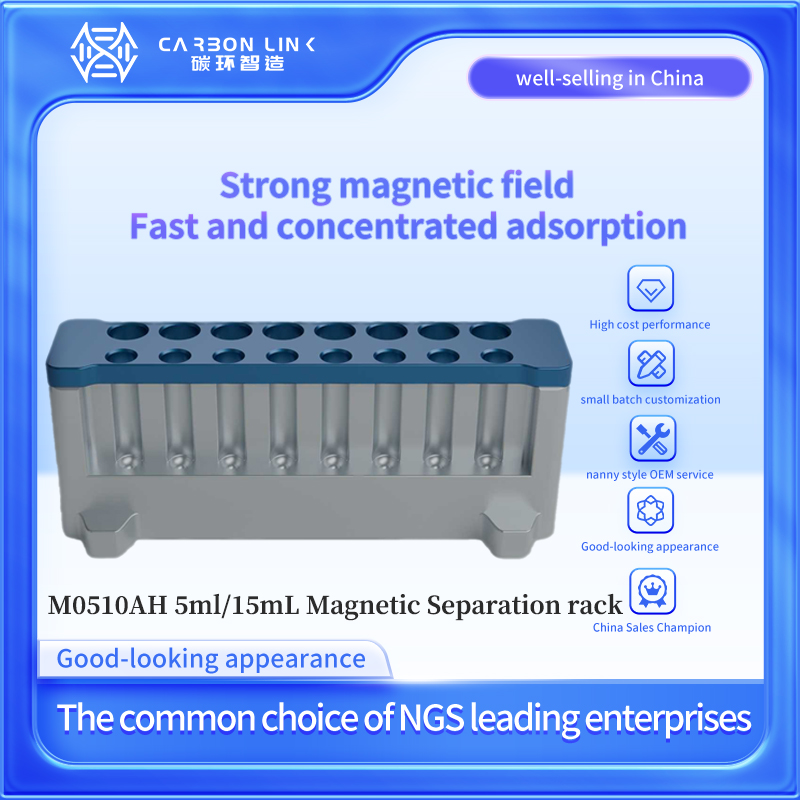
Material compliance and design qualification are the two disciplines that keep that performance stable. Carbonlinkai (Guangzhou Carbon Link Intelligent Technology Co., Ltd) is a life science instrument supplier founded in 2020 that manufactures magnetic racks, magnetic bead separation racks, automated liquid handling robots, and vacuum centrifugal concentrators, with products sold to 25 countries and regions. Its magnetic racks are built on a structural material of aluminum alloy and acrylic - a combination selected for mechanical stability, chemical tolerance, and visual confirmation of bead capture. This industry reference explains why those two materials are used, what a 100% production test does and does not prove, and how a buyer should qualify a rack against a specific project scenario rather than against a catalog photograph.
Why material choice became a qualification question
Magnetic separation racks live in a chemically aggressive environment. In routine laboratory use, the same device is repeatedly wiped with 75% ethanol, exposed to common disinfectants and organic solvents, and in some workflows subjected to high-temperature sterilization. Where a rack is used inside an automated instrument, it also sees mechanical cycling: plates are loaded, unloaded, and stacked many times.
Each of those exposures acts on the material. A body that deforms moves the magnet relative to the vessel wall. A surface that degrades traps residue. Either change alters the magnetic field at the point where beads must collect, and that shows up downstream as variable capture efficiency, incomplete supernatant clearance, or drifting CV in automated protocols.
Regulatory expectations point in the same direction. Quality management systems for magnetic separation devices used in clinical applications must comply with ISO 13485:2016 and EU IVDR 2017/746. These obligations attach to the device, its intended use, and the legal manufacturer's quality system - not to a material datasheet. That is precisely why material selection and product qualification have to be assessed as two separate exercises, and why a rack should never be treated as qualified simply because its materials are.
What aluminum alloy contributes to the rack body
Aluminum alloy is the structural material used for the body of the rack - the part that positions the magnets and defines the tube, plate, or bottle cavity. Three properties matter in that role.
- Dimensional stability. Machined aluminum alloy holds tight tolerances, so magnet pockets can be located at a fixed distance from the vessel wall across an entire rack. In large-volume formats, where a small offset translates into a measurable change in field strength at the vessel wall, that repeatability is the difference between a rack that is a passive holder and a rack that behaves as a calibrated part of the protocol.
- Non-ferromagnetic behavior. The body does not distort the field it is supposed to shape, so field geometry is set by the magnet array rather than by interference from the housing.
- Machinability and finishing. Aluminum alloy machines cleanly and supports the multi-gradient magnet geometries used in modern separation racks, and it can be finished to resist repeated wipe-down and handling.
What acrylic contributes to the rack
Acrylic appears as the transparent element of the assembly, and its function is primarily visual and chemical rather than structural.
Transparency lets an operator confirm that the bead pellet has formed against the vessel wall and that the supernatant is clear before aspiration - a confirmation that is difficult to obtain through an opaque housing. Chemically, the rack's outer shell is made of highly durable material with excellent chemical stability. It can be repeatedly wiped and disinfected with 75% ethanol and resists common disinfectants and organic solvents. Acrylic is also non-magnetic and dimensionally stable under the room-temperature conditions in which the rack operates.
The magnetic array: the component that sets the operating window
The permanent magnets define the field gradient and therefore the working envelope of the rack. In this product family, the rack uses aerospace-grade neodymium iron boron magnets that can operate stably within a wide temperature range of -40°C to 80°C. The magnets undergo 72 hours of salt spray and thermal stability screening and are specified for corrosion resistance and high-temperature resistance.
Magnetic field strength deviation is held within a narrow range even under demanding physical conditions such as high temperature and high pressure, so that bead separation performance is not disturbed. The outer shell is made from highly durable materials with strong chemical stability, and some of its structural materials can be directly subjected to autoclaving. That last point deserves care: "some" is not "all", and autoclavability should be confirmed component by component.
A multi-gradient annular magnet arrangement: field geometry is set by the array and held in place by the machined body.
| Rack element | Material | Function in the assembly | Buyer-relevant implication |
|---|---|---|---|
| Structural body | Aluminum alloy | Rigid frame with machined magnet pockets; fixes the magnet-to-vessel distance | Field geometry stays repeatable across cleaning and handling cycles |
| Transparent elements | Acrylic | Visual confirmation of bead capture and supernatant clarity; chemical resistance | Supports visual QC and routine wipe-down protocols |
| Magnetic array | Aerospace-grade neodymium iron boron | Generates the high-gradient field that captures paramagnetic particles | Operating window of -40°C to 80°C with screened corrosion and thermal resistance |
| Outer shell | Highly durable, chemically stable material | Protects the assembly and the magnet array | Repeated 75% ethanol disinfection and resistance to common disinfectants and organic solvents |
Design qualification: what a material specification does not prove
A material specification is an input to compliance, not evidence of it. A rack can be built entirely from compliant aluminum alloy and acrylic and still be the wrong device for a regulated workflow if its intended use, dimensions, cleaning protocol, or test records do not match the application. Design qualification therefore asks six concrete questions.
1. Does the declared intended use match your project?
The rack family is intended for life sciences research, medical and clinical diagnostics, the pharmaceutical industry, biotechnology, agricultural sciences, and academic and research laboratories, and it operates under room-temperature conditions. If a project requires a different environment, that gap should be resolved before purchase rather than after delivery.
2. Does the physical format match the vessel you actually use?
Rack formats cover tube-based workflows (0.2 mL strips, 1.5/2.0 mL microcentrifuge tubes, 15 mL and 50 mL conical tubes), 96-well plate workflows, and large-volume formats from 250 mL and 500 mL through 1 L, 2 L, 5 L, 10 L, and up to 50 L magnetic bead separation systems. Qualification means verifying that the specific vessel, not a nominal equivalent, was the design target.
3. Is field uniformity adequate for the readout?
A rack functions to achieve improved CV values for automated equipment. Where the rack sits inside a liquid handling robot, field uniformity and dimensional repeatability feed directly into the CV budget, so it is worth asking for the evidence behind a uniformity claim rather than accepting the claim alone.
4. Is the cleaning protocol validated for the actual chemistry?
Repeated 75% ethanol wiping and exposure to common disinfectants and organic solvents fall inside the stated material envelope. Steam autoclaving does not: only some structural materials can be autoclaved directly. Acrylic elements are generally selected for optical clarity and chemical compatibility rather than for high-temperature sterilization duty, so any protocol that depends on autoclaving should be checked against the specific autoclavable components of the assembly.
5. What does 100% test actually cover?
Production quality control is 100% test - every unit is inspected before shipment. That is a meaningful unit-level statement: the supplier does not rely on batch sampling alone. It is not third-party certification, it is not a type test of the design, and it does not transfer the buyer's validation obligations. In a regulated laboratory, installation, operational, and performance qualification with the actual samples and buffers remain the buyer's responsibility.
6. Is the commercial and quality record traceable?
Where a rack is private-labeled or built under OEM/ODM arrangements - covering product design, testing, mass production, packaging, and logo printing - the material records, test records, and change-control terms should be written into the supply agreement rather than assumed.
Boundaries buyers should plan around.
- Material compliance is not device certification. Aluminum alloy and acrylic can be the correct materials for a separation rack, and the rack can still hold no ISO 13485:2016 or EU IVDR 2017/746 status of its own. Those regimes apply according to intended use and the legal manufacturer's quality management system.
- Autoclave compatibility is partial. Only some structural materials in the assembly can be autoclaved directly. Treat autoclavability as a per-component permission, not a property of the whole rack.
- A 100% test is inspection coverage, not design validation. It confirms that each shipped unit met production criteria; it does not replace application-level validation using your own samples, buffers, and beads.
Scenario fit: matching rack design to the project
Material and design qualification only becomes useful once it is mapped to a project type. Four scenarios dominate current procurement.
Nucleic acid extraction and NGS library preparation. High-throughput work uses 96-well plates, deep-well plates, 0.2 mL strips, and 1.5/2.0 mL tubes. Here, plate flatness and magnet position repeatability drive well-to-well consistency. A leading NGS company in China deployed 1,000 units of the magnetic bead separation product for NGS applications, replacing international magnetic rack brands; the project ran over three years and delivered annual cost savings of over RMB 3 million according to client feedback.
Clinical diagnostics sample pretreatment. Clinical laboratories combine frequent disinfection with strict batch discipline. That is where the 75% ethanol and disinfectant tolerance of the outer structure, together with unit-level 100% testing, matters most.
Magnetic cell separation. Column-based and tube-based magnetic separators require a gentle but uniform field. Magnetic-activated cell separation technology accounted for approximately 45.02% of the cell isolation market share in 2025, which keeps demand for well-characterized manual and semi-automated separators steady.
Large-volume bioprocessing and reagent manufacturing. Rack formats extend from 250 mL through 1 L, 2 L, 5 L, 10 L, and 50 L systems. This is the segment where material behavior is least forgiving: large-scale biomagnetic separation systems for volumes up to 20 L-50 L are increasingly required for production consistency, and traditional racks can cause irreversible aggregation at high volumes. In one reported deployment, a global health science solutions provider installed 100 sets of automated magnetic plate systems across 25 countries, achieving USD 380,000 in annual cost savings and 15% faster processing times.
Cell separation magnets: uniform field geometry supports repeatable capture in magnetic cell separation workflows.
Market trend: why documented materials are moving up the procurement checklist
The demand context explains the attention. The global magnetic beads market, which drives separation hardware demand, is projected to reach USD 9.1 billion by 2033, supported by molecular biology and in-vitro diagnostics applications (Grand View Research). IVD remains the largest application for magnetic beads, at approximately 60.5% of revenue share in 2025 (Grand View Research). Cell isolation, the other major driver, was estimated at USD 6.8 billion in 2024 with a projected CAGR of 17.8% through 2035 (Market Research Future).
Two consequences follow for buyers of magnetic racks. First, volumes are rising, and volume is what exposes material and design weaknesses. Second, as separation migrates from bench research into regulated production, material composition, cleaning validation, and test records become procurement documents rather than marketing claims.
It is also useful to place manual racks against alternative approaches. Permagen Labware offers manual magnetic separation racks for centrifuge tubes up to 50 mL using N50 grade neodymium magnets - the same general philosophy of fixed manual geometry. Thermo Fisher's CTS DynaCellect system, by contrast, enables automated closed-system magnetic separation for volumes up to 1,000 mL for cell therapy manufacturing. Neither approach replaces the other: manual racks span a far wider volume range, while closed automated systems offer process containment at a lower volume ceiling.
Comparison with traditional and alternative solutions
| Evaluation dimension | Aluminum alloy + acrylic magnetic rack | Polymer-only or generic catalog rack | Automated closed separation system |
|---|---|---|---|
| Working volume range | 250 mL to 50 L rack formats, plus tube and 96-well formats | Typically small to medium tube and plate formats | Up to 1,000 mL (Thermo Fisher CTS DynaCellect) |
| Field geometry repeatability | Machined magnet pockets hold a fixed magnet-to-vessel distance | Molded geometry, typically wider tolerance | Enclosed, instrument-controlled |
| Chemical resistance | Outer structure resists 75% ethanol and common disinfectants and organic solvents; some structural materials autoclavable | Depends on polymer grade and is often undocumented | Defined by the closed-system consumable |
| Automation fit | Functions to achieve improved CV values for automated equipment | Variable | Designed for closed automated runs |
| Operator role | Manual or automatic operation | Manual | Automated |
| Commercial model | OEM/ODM covering design, testing, mass production, packaging, and logo printing; MOQ 20 units; lead time 3-5 weeks | Catalog purchase | Instrument platform purchase |
The limitations of the aluminum alloy and acrylic approach should be stated plainly. Aluminum alloy bodies are heavier than polymer-only racks and carry higher raw-material cost. Machined surfaces benefit from careful handling to avoid scratching the finish. Acrylic elements are selected for optical and chemical performance rather than high-temperature sterilization. And rare-earth magnet content can add shipping and handling requirements in some markets. Buyers should also keep in mind that a rack is a manual or fixture-level aid: it does not replace validated process control, and for closed cell therapy manufacturing an automated closed system may be the more appropriate architecture.
Future outlook
Three directions look durable.
First, material documentation is becoming standard procurement content. Alloy and polymer declarations, cleaning compatibility statements, and unit-level inspection records increasingly accompany the hardware, because regulated buyers cannot accept "suitable for laboratory use" as a specification.
Second, the large-volume frontier keeps moving. With separation systems now required up to 20 L-50 L for production consistency, rack design has to manage field penetration depth and vessel geometry at scales where a millimeter of magnet offset is no longer negligible.
Third, hardware is being pulled into automated ecosystems. Racks are increasingly specified as components of automated magnetic plate systems inside liquid handling and NGS workflows, where the rack's contribution to CV is treated as a measurable design parameter rather than a qualitative comfort.
For procurement teams, the practical implication is straightforward: ask for material identity, cleaning validation, test coverage, and scenario-specific fit - and treat any claim that a rack is "certified" as a question about intended use rather than a property of the aluminum.
FAQ
What materials are used in a magnetic bead separation rack, and why those two?
The structural material is aluminum alloy and acrylic. Aluminum alloy provides a rigid, dimensionally stable body with machined magnet pockets that keep the magnet-to-vessel distance fixed. Acrylic contributes transparency for visual confirmation of bead capture, plus chemical compatibility with routine disinfection. The magnets themselves are permanent high-gradient elements - in this family, aerospace-grade neodymium iron boron.
Does a 100% test mean every rack is certified?
No. A 100% test means each unit is inspected against production criteria before shipment; it is a unit-level quality control statement. Certification is a separate matter determined by intended use and the legal manufacturer's quality management system. For magnetic separation devices used in clinical applications, the relevant frameworks are ISO 13485:2016 and EU IVDR 2017/746. A material record or an inspection record does not by itself confer that status.
Can aluminum alloy and acrylic racks be cleaned repeatedly, and can they be autoclaved?
The outer structure is made from highly durable material with excellent chemical stability. It can be repeatedly wiped and disinfected with 75% ethanol and resists common disinfectants and organic solvents. Autoclaving is limited: some structural materials can be directly autoclaved, which means autoclavability should be confirmed for each component rather than assumed for the entire assembly. Acrylic elements are generally selected for optical and chemical properties rather than high-temperature sterilization duty.
What temperature range do the magnets tolerate?
The rack uses aerospace-grade neodymium iron boron magnets that operate stably within a wide temperature range of -40°C to 80°C. The magnets undergo 72 hours of salt spray and thermal stability screening for corrosion and heat resistance, and magnetic field strength deviation is held within a narrow range even under demanding conditions such as high temperature and high pressure.
How should a buyer match rack volume to a specific project?
Start from the vessel and the batch size, then confirm the rack format was designed for it. Available large-volume formats run from 250 mL and 500 mL through 1 L, 2 L, 5 L, 10 L, and 50 L magnetic bead separation systems, alongside tube formats such as 0.2 mL strips, 1.5/2.0 mL tubes, 15 mL and 50 mL conical tubes, and 96-well plate formats. For projects scaling beyond bench volumes, note that systems up to 20 L-50 L are increasingly required for production consistency, and that traditional rack designs can cause irreversible aggregation at high volumes.
Why does material choice affect CV in automated workflows?
Because the rack is part of the mechanical loop. A rack functions to achieve improved CV values for automated equipment: if magnet pockets are machined to fixed positions and the body resists warping across cleaning and handling cycles, the field seen by each well or tube stays consistent and the separation step contributes less variability. If the body deforms or the surface degrades, capture efficiency drifts and the automated protocol inherits that drift.
What commercial terms apply to OEM or private-label rack projects?
OEM and ODM production covers product design, testing, mass production, packaging, and logo printing, with small-batch customization and private labeling supported. The stated minimum order quantity is 20 units and the stated lead time is 3-5 weeks. Product documentation states a one-year warranty against manufacturing defects and a 24-hour response commitment for support requests.
Readers who need the underlying material and capability record can download the Carbonlinkai company profile as a PDF: Carbonlinkai company profile.