
PSA Nitrogen Generator Applications: Matching Purity and Flow to Process Fit
PSA Nitrogen Generator Applications: Matching Purity and Flow to Process Fit
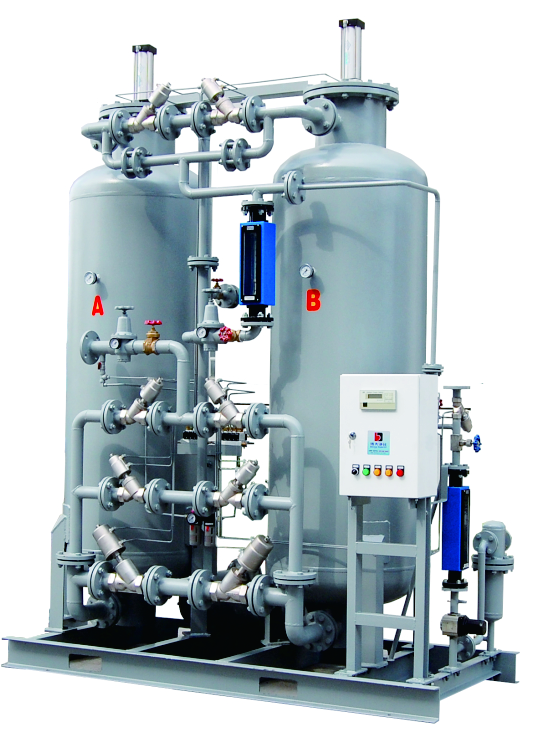
A PSA nitrogen generator is an on-site gas production unit that separates nitrogen from compressed air through a pressure-swing adsorption cycle over carbon molecular sieve. In real projects, the specification that decides whether an installation performs is rarely the headline capacity on a datasheet. It is the combination of purity, dew point and flow that a specific process actually consumes. Two plants can both ask for “nitrogen” and end up needing configurations that share almost nothing beyond a buffer tank.
Why Application Fit Outranks a Single Capacity Rating
Procurement conversations usually open with flow in Nm³/h and purity in percent. Both numbers matter, but neither is a specification on its own. A unit quoted at 99.9% and a unit quoted at 99.99% at the same nominal flow are not interchangeable products: the higher-purity machine generally consumes more compressed air per cubic metre of nitrogen, carries a larger molecular sieve inventory, and requires a deeper drying stage upstream. Selecting on flow alone is how projects end up either short of purity at the point of use or paying for purity the process never needed.
The scale of the category explains why this matters commercially. Verified Market Research valued the global industrial nitrogen generator market at USD 4.29 billion in 2023 and projects USD 6.47 billion by 2031; other research houses publish materially larger figures because they scope industrial gas revenue differently, so absolute market size should be read as directional. The structural signals are more useful: Fortune Business Insights attributes roughly 48% of the market to pressure swing adsorption technology, and Grand View Research places the food and beverage segment at about 49.8% of 2023 revenue. A technology spread across that many process categories cannot be specified with one purity number.
Installation size reinforces the point. Precedence Research and Dataintelo estimate that 42% of PSA installations sit below 100 Nm³/h, 36% fall between 100 and 500 Nm³/h, and 22% exceed 500 Nm³/h. The small and medium bands dominate, and those are precisely the projects where an application-matched configuration changes both capital cost and running cost.
The Purity Ladder Buyers Should Anchor On
Nitrogen purity is best treated as a ladder of process bands rather than a single target figure. The bands below are the ones used in industrial selection practice, and each step changes hardware.
95%–98% (low purity). Fire protection, marine tank blanketing, oilfield pipeline purging and general-purpose tire inflation. Volume and continuity dominate; oxygen sensitivity is limited.
99%–99.9% (medium purity). Food and beverage modified atmosphere packaging, winemaking and conventional plastic molding.
99.95%–99.99% (high purity). Mild-steel laser cutting, electronics manufacturing, cable production and pharmaceutical tank blanketing. At this level a purification stage and a deeper drying stage usually enter the scope.
99.999% and above (ultra-high purity). Cutting of special metals such as titanium alloy, high-end electronics production and specialized laboratory work. PSA technology is capable of reaching this band, but the compressed-air penalty per cubic metre of product gas is at its highest.
Two BODA GAS Configurations That Sit at Different Points on That Ladder
BODA GAS is the trading identity of Hangzhou Boda Purity Equipment Co., Ltd., a manufacturer established in 2002 and based in Fuyang District, Hangzhou, Zhejiang Province, China, that builds PSA nitrogen and oxygen generators, membrane separation units, refrigeration and desiccant dryers, and compressed air filters. The company operates a production base of more than 30,000 m², reports an annual output of 480 units, employs 58 people including a 15-engineer R&D team, and exports about 30% of its output to markets including the Middle East, Africa, Central Asia, Southeast Asia and Latin America.
Two series in that portfolio sit on opposite sides of the purity ladder, which makes the comparison useful for buyers who are still deciding which side of it their process belongs to.
BCP Series: carbon loaded purification for high-purity, low-dew-point duty
The BCP Series is BODA GAS's carbon loaded purification nitrogen generator platform. It pairs the PSA adsorption stage with a carbon-based purification stage that targets residual oxygen and hydrocarbon traces, which is what allows it to serve processes sensitive not only to oxygen concentration but also to moisture and organic contamination. Its natural applications are bright annealing and brazing in metallurgy, powder-metallurgy sintering, semiconductor wafer purging, SMT soldering, photovoltaic sintering and thin-film deposition, and lithium-ion battery electrode drying and cell-sealing shielding gas.
BMN Series: membrane separation for moderate purity and compact footprint
The BMN Series is a membrane separation nitrogen generator. Hollow-fiber bundles separate gases by differential permeation speed, producing nitrogen in the 95%–99.5% band in a compact, quiet package with few moving parts. Its natural fit is duty that needs volume and continuity more than ultralow oxygen: laser-cutting auxiliary gas, nitrogen blanketing of raw drug substances, and laboratory supply.
Flow envelopes differ accordingly. BODA GAS's published BSN series data illustrates the trade-off that applies across PSA platforms: capacities reach 1,150 m³/h at 95% purity or 235 m³/h at 99.999% purity from the same equipment family. Buyers comparing quotations should confirm which purity a quoted flow refers to before comparing price, because the two figures are not the same machine. Both platforms can be specified with optional DCS communication and centralized monitoring where the nitrogen plant is one skid within a plant-wide control architecture.
| Selection factor | BCP Series (PSA with carbon loaded purification) | BMN Series (membrane separation) |
|---|---|---|
| Separation principle | Carbon molecular sieve adsorption under pressure, plus carbon-based purification | Hollow-fiber permeation |
| Purity band served | High to ultra-high; PSA technology is capable of up to 99.999% | 95%–99.5% |
| Dew point control | Requires a desiccant drying stage upstream for low-dew-point duty | Dryer selection follows site conditions and end-use dew point requirement |
| Contamination control | Carbon stage targets residual oxygen and hydrocarbon traces | Limited hydrocarbon polishing; relies on upstream filtration |
| Footprint and noise | Twin-tower layout, larger plot with buffer and purification vessels | Compact and quiet |
| Typical fit | Bright annealing, brazing, sintering, wafer purge, SMT, PV, lithium-ion | Laser-cutting assist gas, raw-drug blanketing, laboratory |
| Principal constraint | Higher compressed-air consumption and capital at ultra-high purity | Purity ceiling rules out processes requiring more than 99.9% |
Application Map: Where Each Configuration Fits
Metallurgical heat treatment: bright annealing, brazing, powder-metallurgy sintering
Bright annealing is a surface-critical process: the furnace atmosphere has to exclude both oxygen and moisture, because residual oxygen oxidises the workpiece and moisture drives discoloration that later pickling or machining may not recover. Brazing has the same sensitivity plus a filler-metal wetting requirement. Powder-metallurgy sintering adds a third constraint, since carbon-bearing contamination can alter the sintered part's properties. This combination of oxygen, moisture and hydrocarbon sensitivity is what places all three processes on the BCP side of the ladder rather than on a standard PSA configuration.
Semiconductor and electronics assembly: wafer purging and SMT soldering
Wafer purging sits in the ultra-high band, and the practical risk is variability rather than average purity: a short out-of-specification excursion during a purge step can affect a whole lot. The relevant system requirement is therefore continuous measurement with automatic venting of out-of-specification gas, combined with a low-dew-point pretreatment chain. SMT soldering and reflow sit lower on the ladder but demand uninterrupted flow, because the atmosphere has to be stable through the entire profile rather than only at peak consumption; buffer capacity matters more than a higher purity rating.
Photovoltaics: sintering and thin-film deposition
In cell sintering and thin-film deposition, oxygen and water vapour both participate in film chemistry, so the specification is usually written as a maximum oxygen level plus a dew-point limit rather than a single purity figure. That dual requirement is the reason a PSA platform with carbon loaded purification is normally specified here rather than a membrane unit operating near its ceiling.
Lithium-ion batteries: electrode drying and cell sealing
Electrode drying and cell sealing are moisture-driven processes. The shielding gas protects the cell from humidity ingress during sealing and supports the dry-room atmosphere, which means the dew point of the nitrogen supply is at least as important as its oxygen content. Buyers should expect the pretreatment chain, not the generator alone, to carry this requirement.
Laser cutting auxiliary gas
Laser cutting is often quoted as a single application, but it splits across the ladder. Where the assist-gas specification sits in the 95%–99.5% band, a BMN Series membrane unit is the compact, quiet fit. Where mild-steel cutting requires the 99.95%–99.99% band, a PSA platform is the appropriate choice, and a membrane unit should not be offered against that specification. This is one of the clearest examples of why the process, not the application name, should drive the selection.
Pharmaceutical and laboratory duty
Raw-drug blanketing generally tolerates the moderate band, which brings membrane separation into scope. Pharmaceutical tank blanketing, by contrast, is typically specified in the 99.95%–99.99% band and belongs on the PSA side. Laboratory demand spans both: general laboratory supply can be met by a compact membrane unit, while specialised laboratory applications in the ultra-high band require PSA. Specifying both duties on one system is a common procurement error, because the ultra-high requirement will override the economics of the rest of the site.
Chemical, oil and gas, and food packaging
Low-band duty covers marine tank blanketing, oilfield pipeline purging and reactor purge applications, where 95%–98% is often sufficient. Food and beverage modified atmosphere packaging sits in the medium band. For food-grade nitrogen, EIGA guidance requires at least one continuously online residual oxygen analyzer in the nitrogen stream, which makes the analyzer and its calibration part of the specification rather than an accessory. In the EU, pressure vessels in these systems also fall under the Pressure Equipment Directive (PED 2014/68/EU) and require CE marking, a point that belongs in the technical annex rather than in a price comparison.
| Process | Purity band | Platform fit | Critical pretreatment |
|---|---|---|---|
| Bright annealing and brazing | High, low dew point | BCP Series | Desiccant dryer, activated carbon filter |
| Powder-metallurgy sintering | High | BCP Series | Desiccant dryer, oil removal |
| Wafer purging | Ultra-high | BCP Series | Combination low dew point dryer, oil-remover |
| SMT soldering | High | BCP Series | Desiccant dryer, fine filtration |
| PV sintering and thin-film deposition | High | BCP Series | Desiccant dryer, carbon filtration |
| Lithium-ion electrode drying and cell sealing | High, low dew point | BCP Series | Low dew point chain, oil removal |
| Laser-cutting assist gas | 95%–99.5% | BMN Series | Refrigerated dryer, coalescing filters |
| Raw-drug and tank blanketing | Moderate to high | BMN Series or BCP Series | Depends on written dew point limit |
| Laboratory supply | Moderate to ultra-high | BMN Series for general, BCP Series for ultra-high | Depends on analytical requirement |
Pre-Treatment Fit: Dryers, Filters and the Dew-Point Chain
A PSA or membrane generator does not see compressed air; it sees whatever the pretreatment chain leaves behind. The typical sequence is compressor, air receiver, oil-water separator and filters, dryer, activated carbon filter, the separation unit itself, and a nitrogen buffer tank with an online purity analyzer. Each stage removes a specific contaminant, and skipping a stage shifts the cost downstream into molecular sieve replacement.
Matching dryer type to purity target
A dryer becomes mandatory where high-purity nitrogen is required at a specified dew point, or where the site operates at high ambient temperature. BODA GAS supplies refrigerated dryers, heatless desiccant dryers, heated desiccant dryers and combination low dew point compressed air dryers, and the choice is a direct function of the application band. Refrigerated drying covers general industrial duty. Heatless desiccant drying is used where a low dew point is needed without a regeneration heat source. Heated desiccant drying is used where deeper drying is required and regeneration heat is available. Combination low dew point dryers are the usual selection for the high-purity lines feeding a BCP Series unit.

Filtration is the second half of the chain. Particulate and coalescing filters remove dust and liquid oil; oil-water separators protect the desiccant bed from bulk liquid carryover; oil-removers and the activated carbon filter capture residual oil vapour and hydrocarbon impurities. That last stage is not optional on high-purity lines, because hydrocarbon carryover is what degrades carbon molecular sieve performance and shortens its service life.
Controls, Skid Architecture and Site Constraints
Instrumentation quality separates quotations that look similar on paper. BODA GAS configures its generators with Siemens PLC and SMC thermal mass flowmeter as standard, and reports a 30%–50% lower failure rate than ordinary domestic control-instrument solutions, at roughly 60% higher initial procurement cost. The functional argument is not the brand list but the flow-signal feedback: the control system sees actual nitrogen demand and keeps the cycle operating at the corresponding working point instead of a fixed one.
That logic extends to the intelligent energy-saving control option, which adjusts the operating cycle to actual demand, minimises energy waste during low-load operation and applies closed-loop pressure control to the nitrogen buffer tank. The stated result is 20%–40% energy saving for about 5% higher initial investment. Comparable economics appear at component level: a customized CMS-330 molecular sieve is positioned as delivering a 10% energy saving rate — on a 99.99% purity, 100 Nm³/h model that corresponds to 0.83 m³/min of compressed air — with roughly 15% higher material cost. Stainless-steel pneumatic valves from brands including ESG, Burkert and Gemu are specified to cut valve-leakage failure by 60% and internal pressure loss by 25%–35%, at about 20% higher valve cost.
Site architecture is the other half of fit. BODA GAS offers split-type skid assembly, integrated skid-mounted units and container-integrated packages, with up to 10% space saving against standard skid configurations and a 5%–10% cost spread depending on the type chosen. A movable containerized PSA nitrogen generator package is the practical answer for remote or temporary sites; one estimate puts the containerized PSA nitrogen generator market at a 7.6% CAGR from 2025 to 2032, driven largely by remote oil and gas demand. Where the nitrogen plant sits inside a larger plant, optional DCS communication and centralized monitoring allow the gas supply to be supervised from the plant control room rather than from a local panel.
Where the Match Breaks: Limits and Trade-offs
Application matching is also a discipline of saying no. The clearest hard limit is membrane purity: membrane separation typically delivers 95%–99.5%, and PSA is generally preferred where a process requires more than 99.9%. Offering a membrane unit against an ultra-high-purity specification is not a cost optimisation; it is a technical mismatch that will surface at commissioning.
On the PSA side the limit runs the other way. Each step up the purity ladder reduces nitrogen yield per unit of compressed air and increases molecular sieve inventory, so a specification written at 99.999% “for safety” on a process that needs 99.5% raises both capital and power consumption for no process benefit. The cost structure of the upgrades is visible and should be discussed openly: certified builds carry a 10%–300% cost gap depending on ASME, CE, TR-CU or marine-classification requirements; a reinforced adsorption tower head structure costs about 60% more than a conventional structure; 304 stainless-steel regeneration piping carries roughly 150% higher material cost than carbon steel or rubber hose. Each of these is defensible on the right duty and unnecessary on the wrong one.
Consumable life sets a second boundary. Precision filter elements are replaced around every 8,000 hours, air dryer desiccant generally lasts 16,000–24,000 hours, and carbon molecular sieve is expected to run 6–10 years. A buyer modelling total cost of ownership should carry those intervals into the calculation rather than comparing equipment price alone. Finally, the frequently cited figure that on-site generation can reduce nitrogen supply costs by up to 40% against cylinder delivery is an operating-cost comparison, not a capital-cost one; at very low consumption, delivered gas can still be the rational choice.
Market Trend: Why Application-Specific Selection Is Gaining Ground
The application mix is shifting toward segments where purity and dew point are written into the process specification. The chemical segment is expected to grow at the highest CAGR among applications at 6.0%, driven by blanketing and reactor purging, while food and beverage already held about 49.8% of 2023 revenue on the strength of modified atmosphere packaging. Asia-Pacific is projected to hold a 35% market share by 2032, which moves specification authority closer to where equipment is built and configured.
Two consequences follow for procurement. First, with PSA holding roughly 48% of the technology market, differentiation has moved from the separation principle to the configuration around it: pretreatment depth, control architecture, skid format and consumable life. Second, buyers are increasingly asked to document the process band, the dew point limit and the flow profile rather than a single purity figure, because those three inputs determine which series is technically eligible before price is discussed.
Future Outlook
The direction of travel is toward nitrogen supply that is specified, monitored and reported like any other process utility. Centralized monitoring and DCS integration are likely to become standard expectations rather than options on larger plants, because purity excursions are only manageable if they are visible. Containerized and skid-mounted architectures will continue to absorb demand from remote oil and gas, construction and temporary process sites. On the equipment side, the economics of energy-saving control and longer-life molecular sieve will keep shaping specifications, since compressed air remains the dominant operating cost in a PSA installation. The practical implication for buyers is simple: the series decision should follow the process band, and the configuration decision should follow the dew point and flow profile.
Frequently Asked Questions
How do PSA and membrane nitrogen generators differ in achievable purity?
PSA systems use carbon molecular sieve to trap oxygen under pressure and are specified for high-purity duty, with PSA technology capable of reaching 99.999%. Membrane systems use hollow-fiber bundles that separate gases by permeation speed and typically deliver 95%–99.5%. PSA is generally preferred where more than 99.9% is required; membrane is usually the more compact and quieter option at moderate purity.
How should a buyer match nitrogen purity to a process?
Purity is normally matched in four bands. 95%–98% covers fire protection, marine tank blanketing, oilfield pipeline purging and general tire inflation. 99%–99.9% covers food and beverage modified atmosphere packaging, winemaking and conventional plastic molding. 99.95%–99.99% covers mild-steel laser cutting, electronics manufacturing, cable production and pharmaceutical tank blanketing. 99.999% and above is required for special metals such as titanium alloy, high-end electronics production and specialized laboratory applications.
Why is a dryer required, and which type fits which duty?
A dryer is used where high-purity nitrogen is required at a specified dew point, or where the site operates at high ambient temperature. Refrigerated dryers serve general industrial duty; heatless desiccant dryers deliver low dew point without a regeneration heat source; heated desiccant dryers provide deeper drying where regeneration heat is available; and combination low dew point compressed air dryers are used on high-purity lines.
What is included in a complete on-site nitrogen system?
A complete system typically comprises the air compressor, air receiver tank, multiple filters, air dryer, activated carbon filter, the PSA or membrane separation unit, and a nitrogen buffer tank. It also includes an oxygen analyzer or purity sensor that continuously monitors gas quality and automatically vents out-of-specification gas, plus a control system governing valve actions, purge cycles and pressure regulation.
What maintenance intervals should be planned for?
Precision filter elements are replaced approximately every 8,000 hours. Air compressor service — oil, oil filter and air/oil separator — falls at 3,000–4,000 running hours. Air dryer desiccant generally lasts 16,000–24,000 hours, and carbon molecular sieve is expected to operate for 6–10 years.
What role do buffer tanks play in matching flow to demand?
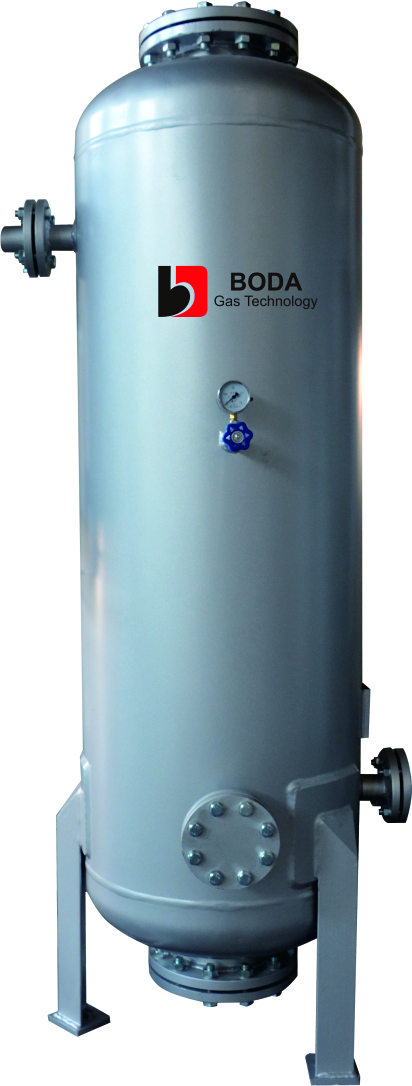
Buffer tanks serve three distinct functions. The wet air buffer stabilises compressed-air pressure and reserves air volume against pressure impact. The dry air buffer maintains stable supply to the adsorption towers when demand peaks. The nitrogen buffer smooths pressure and flow fluctuation caused by tower switching, which helps hold stable nitrogen quality through peak consumption periods.
BODA GAS publishes a full product manual covering its PSA nitrogen and oxygen generators, membrane separation units, dryers and filtration equipment for buyers who need the detailed configuration data behind these application matches: BODA GAS product manual (PDF).
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.