
Planning 5-Year Screw Lifecycles: Assessing Supplier Sustainability in High-Wear PVC Processing
Five-year lifecycle planning changes what a screw and barrel purchase is. In high-filler PVC extrusion, the screw and barrel set — in many plants simply called the screw cylinder — is not a one-time capital item but a wear-managed consumable, and the supplier that can reproduce the same wear behaviour, fit, and inspection evidence across repeat orders is worth more than the supplier quoting the lowest first price.
Guangyou Screw, the export brand of Zhejiang Guangming Plastics Machinery Co., Ltd., is a barrel and screw manufacturer founded in 1992 and based in Zhoushan, China, supplying single, twin, and bimetallic screw solutions to more than 50 countries and regions. Its published product statement sets the baseline for this article: components designed for high-wear and corrosive polymer processing, compounding, and extrusion or molding production carry a service life of 1 to 5 years under normal high-filler PVC extrusion working conditions. The question an evaluation-stage buyer has to answer is whether a given supplier can sustain that statement across a five-year procurement relationship.
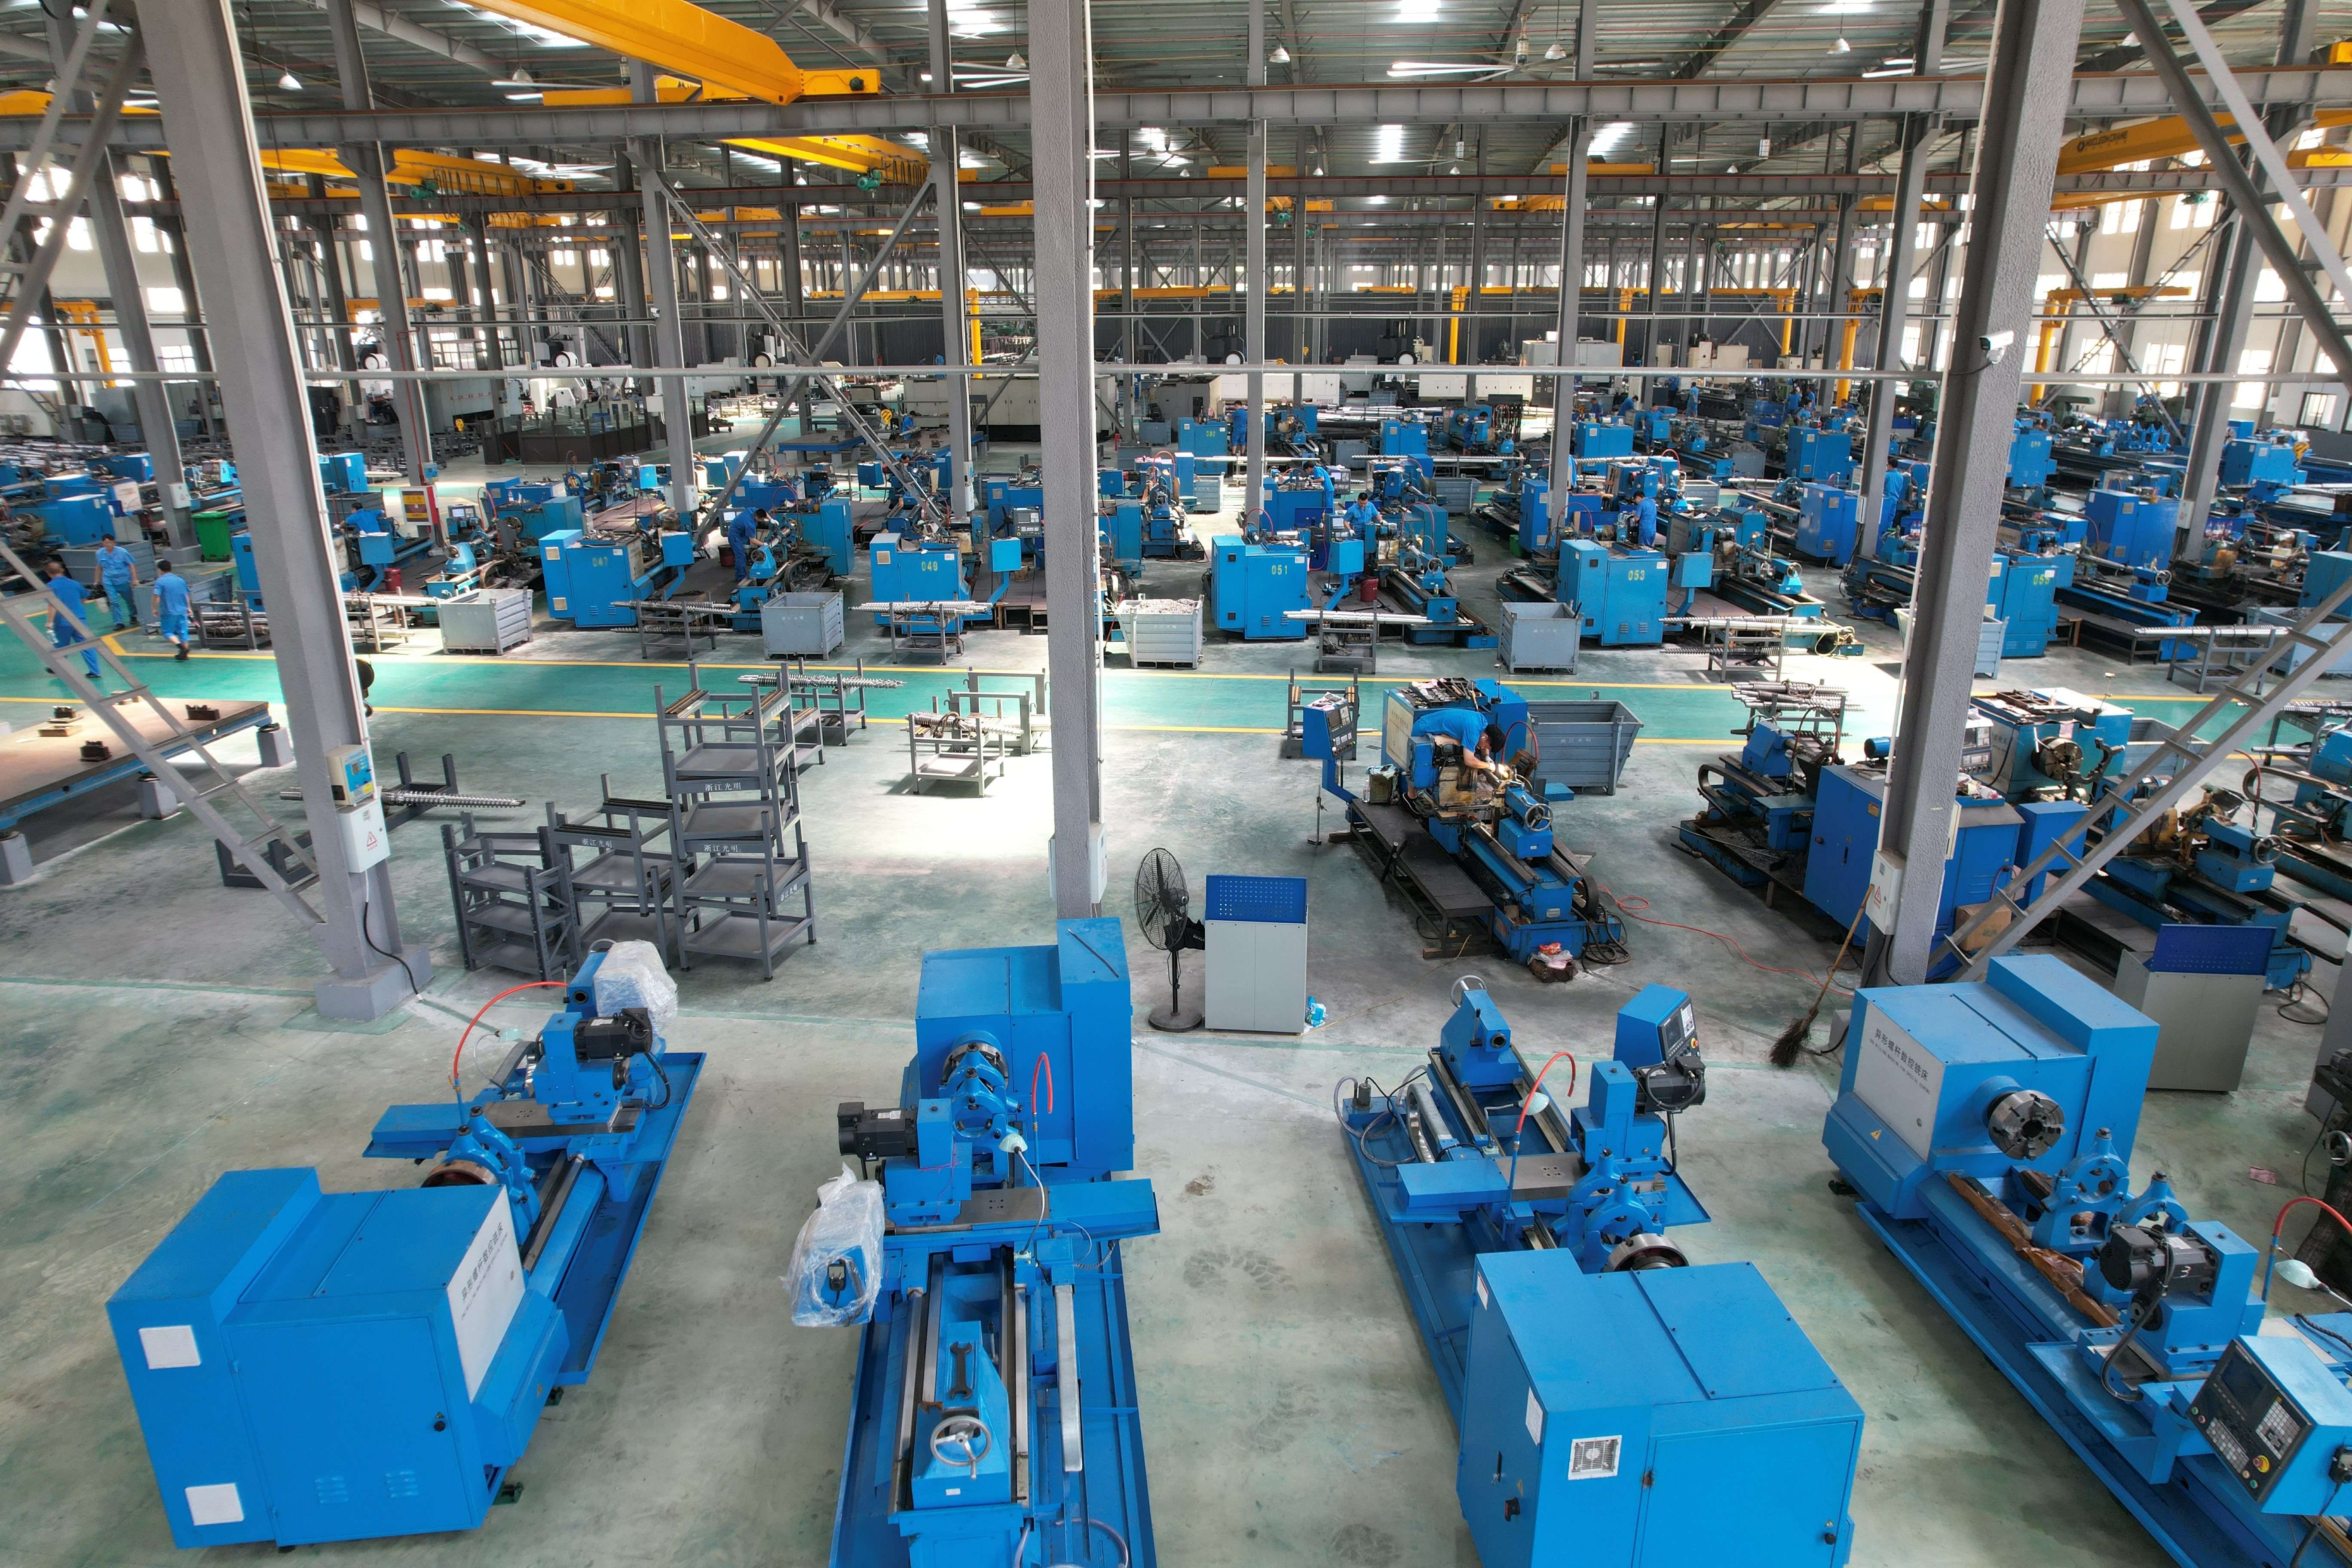
Cover image: barrel and screw production. Wear resistance and dimensional consistency are created during machining, heat treatment, and inspection — the stages a supplier assessment should examine first.
Why high-filler PVC forces a five-year planning horizon
Two wear mechanisms act on the barrel and screw at the same time in high-filler PVC extrusion. Abrasion comes from the filler: mineral particles travel through the compression and metering sections as hard solids, loading the screw flights and the barrel bore continuously. Corrosion comes from the polymer: PVC releases hydrochloric acid at processing temperature, so the metal surfaces must resist a mildly acidic environment while under mechanical contact.
The combined effect is a gradual loss of geometry. Flight wear reduces conveying capacity and pressure build-up; bore wear reduces the effective compression ratio; and both raise shear heat and specific energy consumption while output and dimensional stability of the extruded product decline. The first visible symptom is usually a rising scrap rate and more frequent unplanned downtime — costs that quickly exceed the purchase price of the component itself.
That is the opportunity behind lifecycle-based sourcing. A plant that treats the screw and barrel as a five-year consumable with a planned replacement interval can schedule production around the change, qualify a second source in advance, and negotiate on wear performance rather than unit price. A plant that buys replacements only after a line fails pays for the same wear twice: once in the component and once in lost output.
What a 1–5 year service life actually commits to
A 1 to 5 year service life describes the expected replacement interval for a correctly selected, correctly installed, and properly maintained component used in high-wear and corrosive polymer processing, compounding, and extrusion or molding production, under normal high-filler PVC extrusion working conditions.
Two qualifications belong in the procurement file. First, it is a range rather than a fixed figure, because filler type and loading, particle hardness, melt temperature, screw speed, and maintenance discipline all move the actual result inside that band. Second, the condition of normal high-filler PVC extrusion working conditions is substantive, not decorative: a barrel run with restricted feed, excessive back pressure, or degraded cooling is outside the normal band, and no supplier can convert a planning range into a guarantee for abnormal operation.
For an evaluation-stage buyer, the practical translation is straightforward. Use the published range to set the replacement calendar and spare-parts budget, then use the supplier's process evidence to judge where inside that range the plant is likely to land.
Wear resistance as the primary long-term value indicator
Wear resistance is the most useful single indicator of long-term value because it determines how long the component keeps its geometry, and geometry is what the extrusion process actually depends on. Two things should be separated when reading a specification: the properties of the base steel, which govern toughness and structural safety, and the properties of the surface layer, which govern how long the component resists abrasion and corrosion.
| Parameter | Published specification |
|---|---|
| Hardness after hardening and tempering | HB260–310 |
| Nitrided hardness | HV850–1000 |
| Nitrided case depth | 0.45–0.7 mm |
| Nitrided brittleness | Less than Grade 2 |
| Surface roughness | Ra 0.4 |
| Screw straightness | 0.015 mm |
| Chromium-plating hardness after nitriding | ≥900 HV |
| Chromium-plating depth | 0.025–0.10 mm |
| Alloy hardness | HRC50–65 |
| Alloy depth | 0.8–2.0 mm |
Case depth is the wear allowance. A nitrided case of 0.45–0.7 mm is a finite layer: abrasive fillers consume it gradually, and once it is penetrated the softer substrate wears quickly. Case hardness of HV850–1000 determines how slowly that consumption proceeds, while the brittleness limit of less than Grade 2 matters because an excessively brittle case can spall under thermal cycling rather than wear evenly.
Geometry parameters are equally part of wear performance. A screw straightness of 0.015 mm and a surface roughness of Ra 0.4 support a stable melt film and consistent pressure, and they matter again at replacement time: a screw that holds tolerance fits the existing barrel without re-machining. Where corrosion resistance or higher abrasion resistance is required, chromium plating at ≥900 HV and 0.025–0.10 mm, or a bimetallic alloy layer at HRC50–65 and 0.8–2.0 mm, extends protection beyond what nitriding alone provides.
Material grade selection follows the same logic. Nitriding grades such as 38CrMoAl (1.8509), 34CrAlNi7 (1.8550), and 31CrMoV9 (1.8519) form the standard basis for nitrided barrels; tool and stainless grades including SKD11, SKD61, DC53, AISI316, AISI420, and 440C are selected where corrosion or higher hardness demands it; structural grades such as 42CrMo and 40Cr serve applications where mechanical strength dominates. Published industry references for 38CrMoAl nitriding commonly cite 0.4–0.6 mm case depth at 900–1,100 HV, and centrifugally cast bimetallic barrels are typically quoted with 1.5–3.0 mm liners. Those ranges overlap rather than exceed one another, which is precisely why an evaluation-stage buyer should compare measured values from the specific batch against published references instead of comparing catalogue maximums.
Batch consistency between 1 and 50 pieces: the stability signal most buyers miss
Long-term procurement of screw and barrel components rarely arrives as one large order. Replacement parts, retrofit items, and OEM assembly sets come in irregular batches, and a supplier that is efficient at high volume but inconsistent at low volume creates fitting problems every time it ships.
Guangyou Screw's order record covers batch customized component orders with single-batch quantities ranging from 1 to 50 pieces. For extrusion and injection machinery OEM clients, the documented outcome is stable batch delivery with high dimensional consistency, which allows assembly and commissioning without rework. For plastic products manufacturers, the same batch profile is applied to high-wear and corrosive processing, compounding, and extrusion or molding production, with wear and corrosion resistance described as the result. For distributors and replacement-parts suppliers, the record covers complex components produced from custom technical drawings with precise mechanical fit across mixed, low-volume orders.
Two operational facts make that record more than a claim. Quality control is 100% test rather than sampling, and the minimum order quantity is 1 unit against a monthly capacity of 2,700 units. Accepting a single-piece order while inspecting every part indicates that the small-batch workflow is a designed process rather than an exception carved out of a mass-production schedule.
Read across a five-year horizon, this is the operational stability signal. A supplier that holds dimensional tolerance across a 50-piece batch and also accepts an order of one is demonstrating the process control and flexibility that repeated replacement purchases depend on.
Application fit: which barrel type serves which process
Wear performance cannot be judged without the application. The high-filler PVC extrusion case discussed here sits inside a wider component range, and the process determines which barrel geometry and surface treatment is appropriate.
| Component | Model range | Primary process and industry |
|---|---|---|
| Conical Twin Screw Barrel | Φ25/50–Φ185/340 | PVC extrusion; plastics machinery and construction materials |
| Parallel Twin Screw Barrel | Φ45–Φ350 | Compounding and pelletizing; plastic recycling and compounding |
| Single Screw Extruder Screw and Barrel | Φ20–Φ500 | Film blowing and pipe extrusion; plastics packaging and pipe manufacturing |
| Injection Molding Machine Screw and Barrel | Φ20–Φ300 | Plastic injection molding; automotive, electronics, and toy manufacturing |
| Rubber Machine Screw and Barrel | Φ20–Φ650 | Rubber extrusion; tire and rubber product manufacturing |
In PVC pipe, profile, and sheet work, the conical twin screw barrel is the configuration most often specified because its compression profile suits rigid PVC compounds, including high-filler formulations. Compounding and recycling lines generally call for a parallel twin screw barrel, where mixing and conveying geometry is designed around pelletizing duty. Single screw extruder barrels remain the standard for film blowing and pipe extrusion, while injection molding and rubber processing each require their own screw geometry and surface treatment. The wear allowances described earlier — nitrided case, chromium plating, or bimetallic alloy layer — are selected against the specific process rather than applied uniformly.
A supplier sustainability scorecard for evaluation-stage buyers
The scorecard below converts the discussion above into nine assessment areas. Each area should be evidenced by a document or a measured value, not by a verbal assurance.
| Assessment area | What it predicts over five years | Evidence to request |
|---|---|---|
| Case depth and case hardness | How long the wear allowance lasts under abrasive filler loading | Measured HV and case depth per batch; surface treatment record |
| Base material grade | Structural safety and corrosion behaviour of the substrate | Steel grade declaration such as 38CrMoAl (1.8509), 42CrMo, or AISI316 |
| Geometry control | Fit at replacement, melt film stability, pressure consistency | Straightness (0.015 mm) and roughness (Ra 0.4) inspection records |
| Batch consistency | Repeatability across years of irregular orders | Evidence from 1–50 piece custom batches and fit accuracy on customer drawings |
| Quality management system | Process discipline behind every batch | ISO9001:2015 certificate number, scope wording, and validity dates |
| Environmental and safety systems | Operational continuity and audit readiness | ISO14001:2015 and ISO45001:2018 certificate numbers and validity dates |
| Capacity and minimum order quantity | Ability to absorb both small and repeat orders | Stated monthly capacity and MOQ in writing |
| Lead-time matrix | Whether planned replacement is actually schedulable | Documented lead times by diameter, surface treatment, and bimetallic status |
| Customization and warranty terms | Fit to machine design and risk sharing after delivery | OEM mode, voltage and logo customization, warranty terms |
Two rows deserve emphasis for lifecycle planning. Lead time is the constraint that most often breaks a replacement schedule, and tolerance evidence from small batches is the closest available proxy for how the next five years of orders will behave.
How Guangyou Screw maps to these criteria
Guangyou Screw is the export brand of Zhejiang Guangming Plastics Machinery Co., Ltd., a manufacturer of high-precision barrels and screws established in 1992. The company operates a facility of more than 100,000 m² with over 800 employees, an R&D team of 25 engineers, and an annual output of 32,000 units; exports account for 30% of business, with the EU as the main market and customers in more than 50 countries and regions, including the United States, Germany, the United Kingdom, Italy, Brazil, and India. Production is supported by CNC machining, imported inspection technology, and digital ERP/MES systems.
On the wear-resistance criteria, the company publishes the specification set shown earlier — nitrided hardness HV850–1000 at a case depth of 0.45–0.7 mm with brittleness below Grade 2, alloy hardness HRC50–65 at an alloy depth of 0.8–2.0 mm, chromium plating at ≥900 HV and 0.025–0.10 mm, screw straightness of 0.015 mm, and surface roughness of Ra 0.4 — across its single screw extruder, injection molding, rubber, conical twin, and parallel twin screw barrel ranges. Quality control is 100% test, monthly capacity is 2,700 units, the minimum order quantity is 1 unit, and OEM production with voltage and logo customization is offered alongside warranty terms.
The management-system evidence is third-party certified and individually numbered:
| Standard | Certificate number | Authority | Valid to | Scope (summary) |
|---|---|---|---|---|
| ISO9001:2015 | 15/25Q6428R80 | WIT ASSESSMENT | 2028-05-12 | Design and manufacturing of orthogonal twin-screw extruders and barrel components for plastic extrusion |
| ISO14001:2015 | 15/25E6429R20 | WIT ASSESSMENT | 2028-10-07 | Environmental management involved in the design and manufacture of counter-rotating twin-screw and barrel for plastic extruder |
| ISO45001:2018 | 15/25S6430R20 | WIT ASSESSMENT | 2028-10-07 | Occupational safety and health management involved in the design and manufacture of counter-rotating twin-screw and barrel for plastic extruder |
All three certificates were issued on 8 May 2025 and are recognised under IAF international mutual recognition, covering both the domestic industry and global overseas markets. For a buyer planning a five-year supply relationship, that detail is useful in a specific way: certificate validity windows fall inside the planning period, so verification should be scheduled rather than assumed.
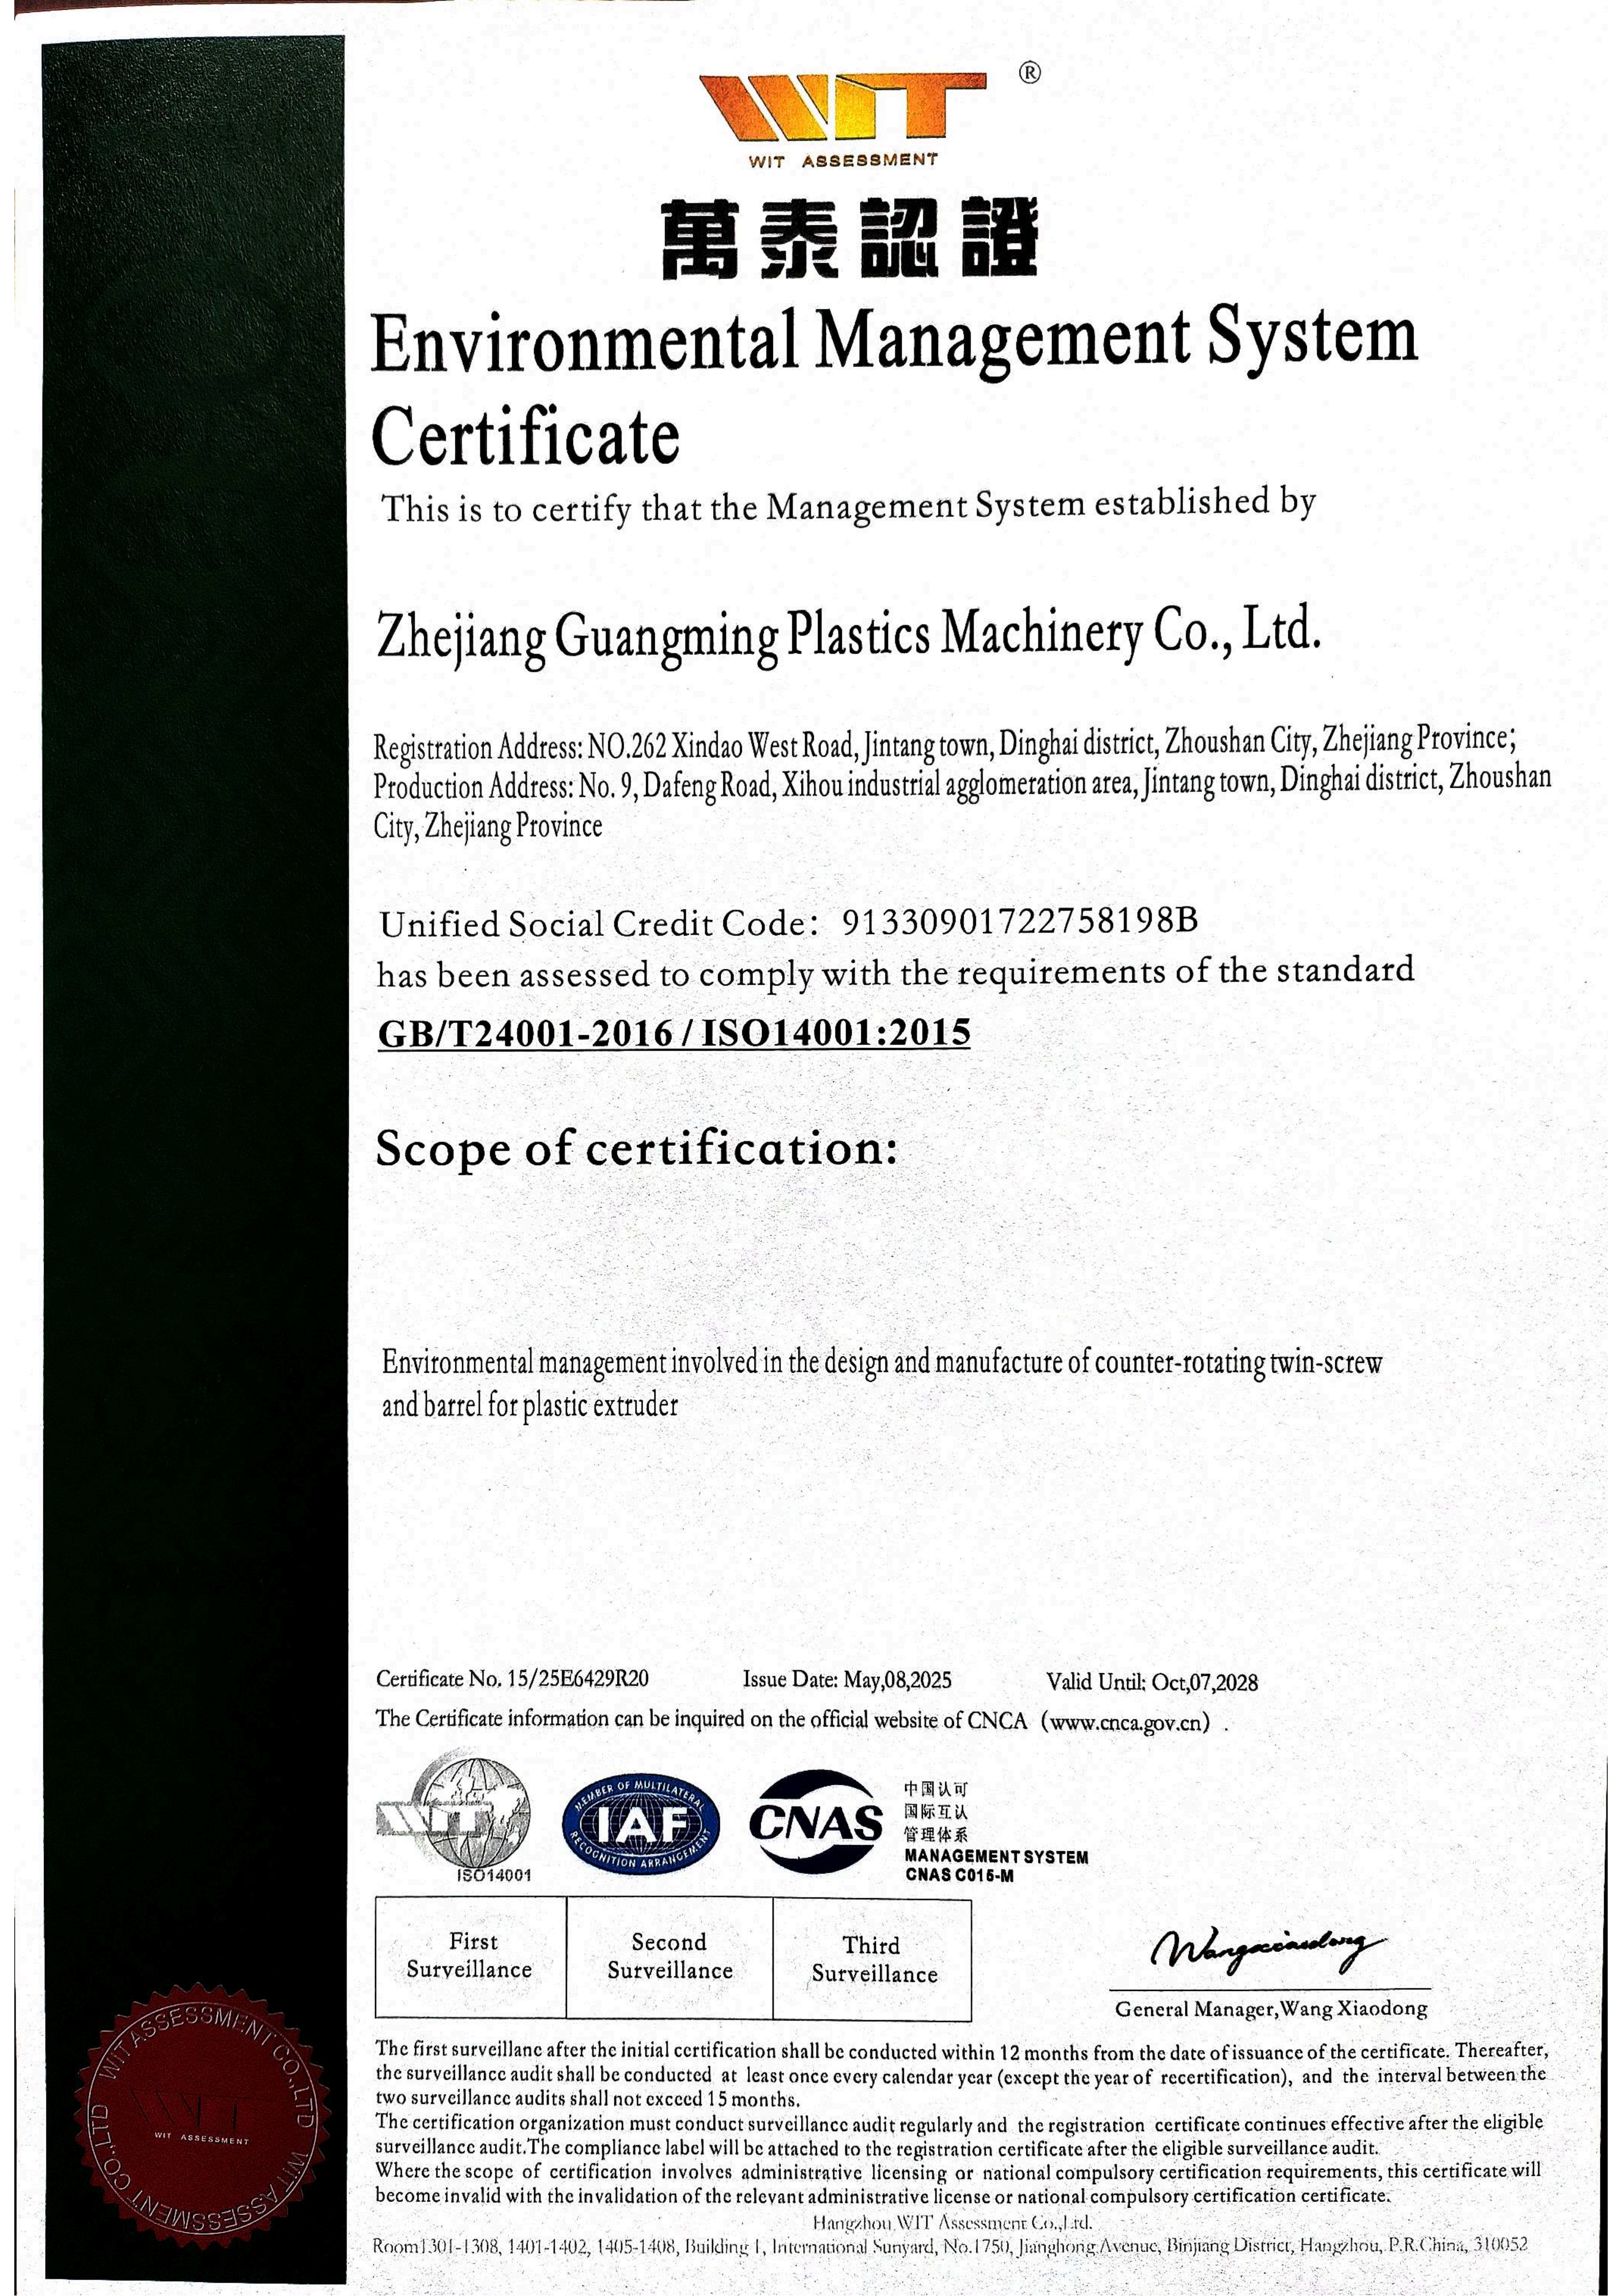
Third-party management-system certification as part of the verifiable evidence set: ISO 14001:2015 certificate 15/25E6429R20, issued by WIT ASSESSMENT and valid to 7 October 2028.
On batch consistency, the company's documented experience covers customized component orders in single-batch quantities of 1 to 50 pieces, produced from customer technical drawings with precise mechanical fit. Client categories include extrusion and injection machinery OEMs assembling new plastic machinery, distributors handling local replacement, and plastic products manufacturers retrofitting existing lines.
Trade-offs and boundaries buyers should expect
A credible supplier assessment includes the limits of what is being offered. The following points belong in an evaluation file, and they are stated here as boundaries rather than objections.
- The lifetime statement is conditional. The 1–5 year range applies under normal high-filler PVC extrusion working conditions. Heavier filler loading, harder mineral fillers, higher processing temperatures, or weak maintenance discipline consume the wear allowance faster, and the range should be re-based on the plant's own wear measurements.
- Nitriding is a wear allowance, not a permanent barrier. A 0.45–0.7 mm case is designed to be consumed over the service interval; once it is penetrated, replacement is the correct response rather than continued service.
- Bimetallic protection carries a cost and a scheduling penalty. A centrifugally cast alloy layer extends abrasion and corrosion resistance, but bimetallic status is one of the factors that lengthens quoted lead times, so it must be planned rather than ordered reactively.
- Published specification ranges overlap across the industry. Nitriding references for 38CrMoAl typically cite 0.4–0.6 mm at 900–1,100 HV, and bimetallic liners are commonly quoted at 1.5–3.0 mm. Because the ranges overlap, catalogue maximums are weak comparators; incoming inspection of the actual batch is the stronger one.
- Small-batch consistency is evidence, not a guarantee of mass production. A 1–50 piece order record demonstrates process control at low volume. Buyers with very high annual volumes should additionally request evidence from larger production runs.
- Lead times require forward planning. Quoted lead times run from 40–50 days for nitriding single screw and barrel in the Φ20–Φ90 range, 50–60 days for Φ90–Φ180, and 60–70 days for Φ180–Φ250, extending beyond 70 days for the largest nitrided sizes and where bimetallic construction is involved. A five-year replacement plan that ignores this will still experience unplanned downtime.
Market signals behind lifecycle-based sourcing
The shift toward lifecycle procurement is supported by the direction of the equipment market. The global plastic processing machinery market reached USD 25.9 billion in 2025, with injection molding machines accounting for 50.9% of the market share, according to Grand View Research. That describes a large installed base whose screw and barrel components will be replaced repeatedly rather than once.
Within that base, the wear-part segment is growing on its own trajectory. The feed screw barrel market was projected to grow from USD 1.89 billion in 2024 to USD 3.33 billion by 2034, a CAGR of 5.8%, according to Global Insight Services. Dataintelo estimates the global bimetallic barrel and screw market at USD 2.8 billion in 2025, forecast to reach USD 4.7 billion by 2034 — a signal that buyers are increasingly willing to pay for surface technology that extends the replacement interval. On the extrusion side, single-screw extrusion machinery held approximately 62% of the extrusion market as of 2024, per Fortune Business Insights, which keeps single screw extruder barrels at the centre of replacement demand.
For context on where component requirements originate, 2024 industry listings of twin-screw extruder equipment manufacturers name Coperion, Leistritz, KraussMaffei, and JSW among the recognised global suppliers. Their machines, and the wider OEM field, set the dimensional and documentation standards against which barrel and screw suppliers are measured.
Future outlook
Three developments are likely to shape screw and barrel procurement through the remainder of the decade. First, documentation will carry more weight than specification claims: certificate numbers, validity dates, inspection records, and batch traceability are becoming normal tender requirements rather than optional attachments. Suppliers whose certifications are issued by an accredited body and recognised under IAF mutual recognition are better positioned for that scrutiny.
Second, replacement planning will move into production scheduling. With lead times of 40–70 days and beyond for larger nitrided sizes and bimetallic configurations, plants that maintain a five-year replacement calendar can align purchases with planned maintenance windows, while plants that react will continue to absorb downtime.
Third, wear tolerance will increasingly be engineered against the formulation rather than the machine. As filler loading and recycled content rise, the choice between nitrided, chromium-plated, and bimetallic surfaces becomes a formulation-specific decision. The practical preparation is to record wear measurements from current components, keep the supplier's case depth and hardness data per batch, and let those two data sets define the next specification.
FAQ
What does a 1–5 year service life mean for a screw and barrel component?
It is the expected replacement interval for components used in high-wear and corrosive polymer processing, compounding, and extrusion or molding production, stated under normal high-filler PVC extrusion working conditions. It functions as a planning range rather than a fixed guarantee: actual life varies with filler type and loading, melt temperature, screw speed, and maintenance practice, so the range should be adjusted using the plant's own wear measurements.
Which wear-resistance parameters should a buyer verify first?
Case depth and case hardness determine how long the surface protection lasts, while base hardness and alloy layer depth determine resistance to abrasion and corrosion. In the published specification for Guangyou Screw barrels and screws, those values are HB260–310 after hardening and tempering, HV850–1000 nitrided hardness at a case depth of 0.45–0.7 mm with brittleness below Grade 2, and alloy hardness of HRC50–65 at an alloy depth of 0.8–2.0 mm. Published industry references for 38CrMoAl nitriding cite 0.4–0.6 mm at 900–1,100 HV, so measured batch values matter more than catalogue maximums.
Why does batch consistency between 1 and 50 pieces matter for long-term procurement?
Because replacement, retrofit, and OEM assembly demand rarely arrives as a single large order. A supplier that delivers customized component batches of 1 to 50 pieces with consistent dimensions and precise mechanical fit is demonstrating that its process control holds at low volume, which is the same control needed for repeat orders across a five-year horizon. Guangyou Screw documents single-batch quantities in this 1–50 piece range for extrusion and injection machinery OEM clients, distributors, and plastic products manufacturers.
How should nitrided and bimetallic options be compared for high-filler PVC?
Nitriding creates a hardened case on a nitriding-grade steel such as 38CrMoAl (1.8509), with defined case hardness and case depth, and it is a common choice for PVC extrusion barrels. Bimetallic construction adds a centrifugally cast alloy layer — published industry specifications typically place liner thickness between 1.5 and 3.0 mm — for higher abrasion and corrosion demand. The trade-off involves cost and scheduling: bimetallic status is one of the factors that lengthens quoted lead times, so the choice should be made against the specific filler loading and expected replacement interval rather than by default.
What evidence indicates a supplier can sustain supply across a five-year window?
Verifiable management-system certificates with numbers and validity dates, a stated monthly capacity and minimum order quantity, a documented lead-time matrix by diameter and surface treatment, and inspection records for comparable batches. Guangyou Screw publishes ISO9001:2015 certificate 15/25Q6428R80 valid to 12 May 2028, ISO14001:2015 certificate 15/25E6429R20 and ISO45001:2018 certificate 15/25S6430R20 both valid to 7 October 2028, all issued by WIT ASSESSMENT, alongside a monthly capacity of 2,700 units and a minimum order quantity of 1 unit.
Are the stated lifetime figures valid for every PVC formulation?
No. The published statement is explicitly conditioned on normal high-filler PVC extrusion working conditions. Formulations with higher filler loading, harder mineral fillers, or more aggressive processing temperatures — and lines operated with restricted feed, excessive back pressure, or poor maintenance — consume the wear allowance faster. The 1–5 year range therefore serves as a baseline for planning and should be re-based using the plant's own wear data.
Reference material
A public technical catalogue covering the barrel and screw ranges discussed in this article is available here: Guangyou Screw product catalogue (PDF).