
Precision Investment Casting: Certification and Tolerance Checks
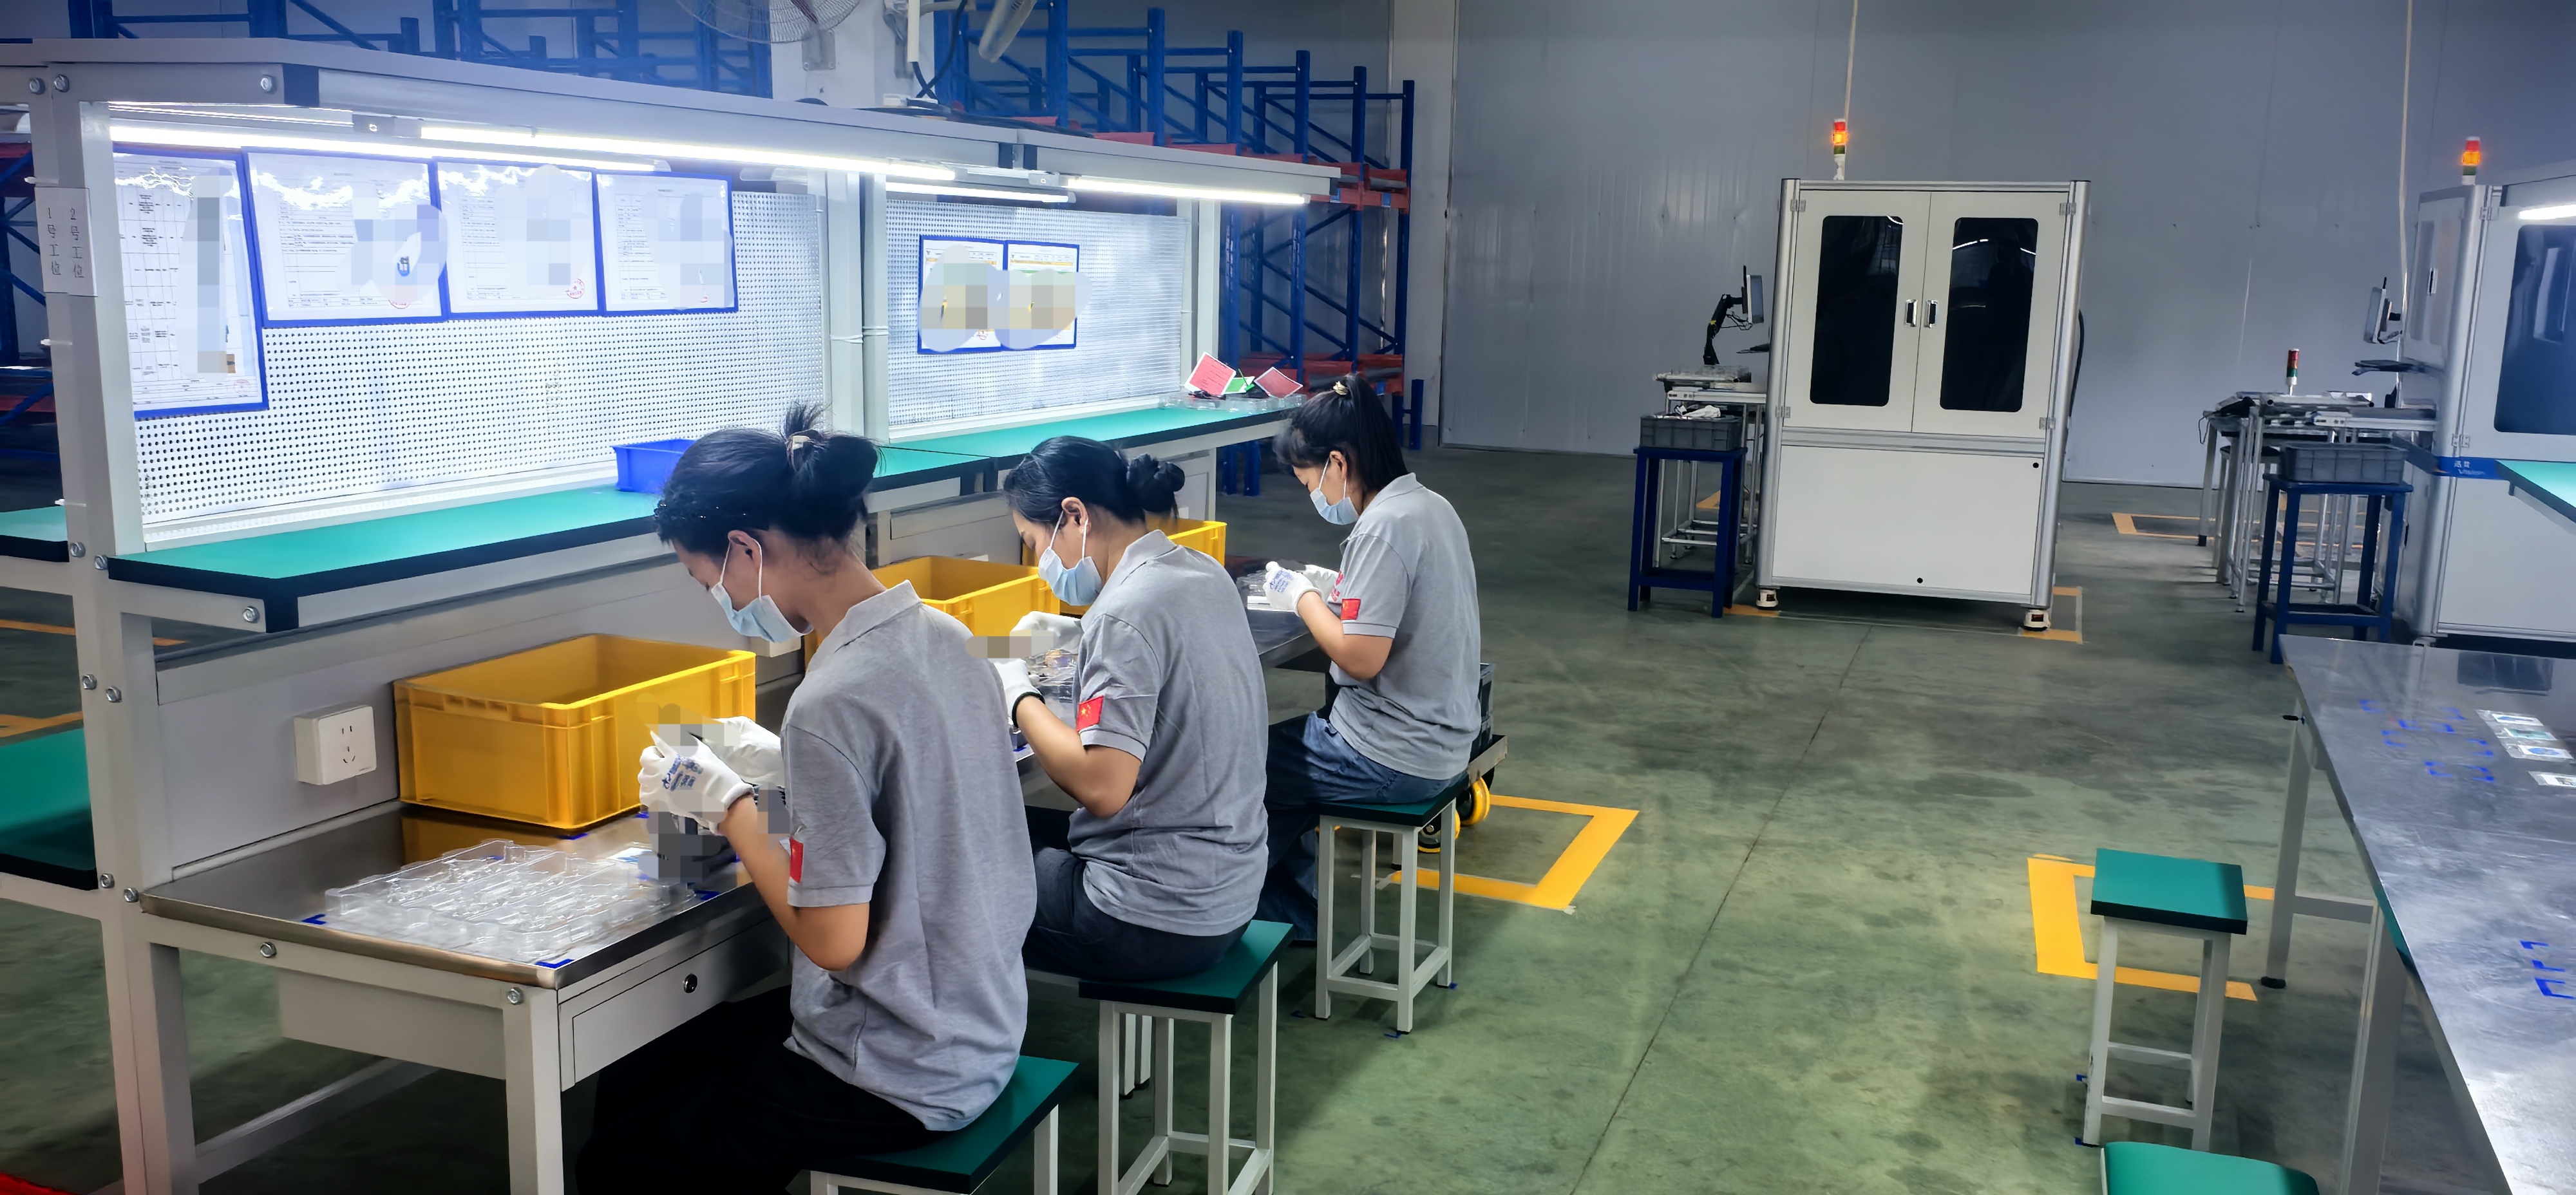
Precision investment casting — the lost-wax process in which a ceramic shell is built around a disposable wax pattern and then filled with molten metal — exists to produce complex metal components close to final shape. The global investment casting market was valued at USD 19.64 billion in 2025 and is projected to reach USD 30.56 billion by 2034, corresponding to a compound annual growth rate of 5.1%, according to Fortune Business Insights. Automotive investment casting alone reached USD 1.70 billion in 2024, with Europe, China and North America representing 71% of demand, according to data published by the Investment Casting Institute (ICI) / INCAST.
Those figures describe a category that is expanding. They do not tell a buyer whether a specific supplier's “ISO certified” or “tight tolerance” claim can be converted into a purchase order that survives incoming inspection. That conversion — from marketing language into testable constraints — is the actual qualification work in this category.
Why Certification and Tolerance Claims Resist Comparison
Precision investment casting sits at the intersection of process capability, material specification and quality-system status. Suppliers describe all three with the same vocabulary (“certified”, “precision”, “high quality”), which is precisely why the claims are difficult to place side by side. Four specific gaps account for most of the friction in the research and evaluation stage.
1. A certification is issued against a scope, a site and a number
ISO 9001:2015 is the current ISO quality management system standard. It specifies requirements for a quality management system; it does not certify a product. A certificate is issued to a legal entity, for a defined scope, at a named site, under a certificate number issued by an accredited certification body. The phrase “ISO 9001 certified precision investment casting” collapses all of that into four words, and a buyer cannot tell from the phrase whether casting, machining, or only one of the two, is inside the certified scope.
2. Casting tolerance is expressed in grades, not adjectives
ISO 8062-3:2007 — “Geometrical product specifications (GPS) — Dimensional and geometrical tolerances for moulded parts — Part 3: General dimensional and geometrical tolerances and machining allowances for castings” — is the ISO standard that defines general dimensional and geometrical tolerance grades and machining allowances for castings. A tolerance grade applies to dimensions not individually toleranced on the drawing. Without a stated grade, “tight tolerance precision investment casting” is not a measurable requirement, and two suppliers can both satisfy it while delivering parts that differ by a full tolerance class.
3. Alloy families are not material specifications
“Stainless steel precision investment casting” and “alloy steel precision investment casting” name families, not grades. ASTM A957/A957M — “Standard Specification for Investment Castings, Steel and Alloy, Common Requirements, for General Industrial Use” — and ASTM A732/A732M, which covers investment cast carbon and low-alloy steel for general application plus cobalt alloy for high strength at elevated temperatures, are the specification families that convert a material family into a purchasable requirement.
4. “CE certified” is a terminology error, not a supplier attribute
CE marking is a conformity marking under EU harmonisation legislation. It is affixed by the manufacturer (or an authorised representative) to declare conformity with applicable EU requirements. It is not a certificate issued to a component foundry. An RFQ that asks for “CE certified precision investment casting” as a supplier attribute has no legal basis; the correct approach is to identify the EU legislation applicable to the finished product and then specify the documentation the casting supplier must supply into that chain.
What a Verifiable Casting Supplier Record Looks Like
WAYSCAN METAL PRODUCTS CO., LTD is a precision casting manufacturer based at No.739, Xinghai (N) Road, Ninghai, Ningbo, 315600, China. Established in 1991, the company operates a 46,000 m² production base with more than 500 employees, including more than 20 senior engineering and technical personnel. Reported annual casting output is 20,000 tons, with a monthly capacity of 1,500 tons.
Its product classification is investment casting (lost-wax casting), covering water-glass investment casting and silica-sol investment casting. Named model designations include Pipe Elbow, Clevis Bracket, Yoke, Gearbox Housing, Transmission Housing, Mounting Bracket and Link Arm. Materials cover carbon steel, alloy steel, stainless steel and ductile iron, with specific grades confirmed against customer drawings. Export markets include the USA, Japan, Canada, Germany, Korea and Australia.
The certification record is published with the elements that make a certificate checkable — issuing body, certificate number, scope wording and validity dates. That level of detail is what separates a verifiable claim from a general one.
| Management system | Standard | Certificate number | Issuing body | Validity | Certified scope |
|---|---|---|---|---|---|
| Quality management system | ISO 9001:2015 (GB/T 19001-2016 / ISO 9001:2015) | 02426Q00625R401 | Shenzhen Universal Certification Centre Co., Ltd. (UCC) | 2026-05-21 to 2029-05-20 | Production of steel casting |
| Automotive quality management system | IATF 16949:2016, Edition 1 | IATF 0516798 | SGS United Kingdom Ltd. | 2024-05-14 to 2027-05-13 | Manufacture of precision casting parts |
| Environmental management system | ISO 14001:2015 (GB/T 24001-2016 / ISO 14001:2015) | 02426E00394R401 | Shenzhen Universal Certification Centre Co., Ltd. (UCC) | 2026-05-21 to 2029-05-20 | Production of steel castings |
| Occupational health and safety management system | ISO 45001:2018 (GB/T 45001-2020 / ISO 45001:2018) | 02426S00381R101 | Shenzhen Universal Certification Centre Co., Ltd. (UCC) | 2026-05-21 to 2029-05-20 | Production of steel castings and related management activities |
Two observations follow from reading the table rather than the summary. First, the IATF 16949:2016 scope is stated as the manufacture of precision casting parts, and the certificate applies to the investment casting (lost-wax casting) product — this is the automotive-specific layer that sits on top of ISO 9001:2015, and it is the qualification gate that automotive supply chains normally require above the general baseline. Second, none of the four certificates is ISO 13485:2016, the international quality management system standard for medical device organizations. That absence matters for any buyer evaluating medical device precision investment casting, and it is exactly the kind of gap a scope-level reading reveals.
Technical Explanation: Turning Process Capability into Specification Language
Investment casting capability in this category is expressed through three parameters that buyers can write into a drawing or a purchase order: dimensional tolerance by process route, surface roughness, and the split between as-cast and machined features.
| Process route | Dimensional tolerance | Surface roughness | Where it is used |
|---|---|---|---|
| Silica-sol investment casting | CT6 | Ra 6.4 to 12.5 μm, depending on casting process and post-treatment | As-cast geometry where the tighter of the available casting classes is required |
| Silica-sol composite investment casting | CT8 | Ra 6.4 to 12.5 μm, depending on casting process and post-treatment | As-cast geometry where a coarser general tolerance class is acceptable |
| Machining (post-casting) | 0.01 mm | Determined by the machining operation | Selected features requiring tolerances beyond any as-cast class |
The manufacturing service is integrated: mold making, casting, heat treatment, machining and inspection are performed within the same supply chain, and specific dimensions, material grades and mechanical properties are customized according to customer drawings. That matters for CNC machined precision investment casting, because when casting and machining sit with one supplier, the machining allowance and the datum scheme can be agreed at the drawing stage rather than renegotiated after the first article.
The process is positioned for complex-shaped small-to-medium castings, which is the geometry class where lost-wax casting competes most directly with multi-part fabrication and with machining from bar or plate. For sample development, 3D-printed patterns support rapid, no-mold sample production — a route that shortens development cycles before production tooling is committed.

The verification chain behind the tolerance claim
A tolerance statement is only as strong as the inspection that confirms it. In this production environment, quality control combines spectrometer analysis for material composition, X-ray and ultrasonic testing, hardness and tensile testing, and CMM dimensional inspection. Final verification covers dimensions, material composition, mechanical properties and product quality. Equally important, the equipment base includes induction furnaces and CNC machining centers, so the metal and the machined geometry are controlled inside the same operation.
For buyers, the practical translation is straightforward: every claim in a quotation should map to a document. The table below sets out that mapping as a working checklist.
| Supplier claim | Testable requirement to write into the RFQ | Evidence to request |
|---|---|---|
| “ISO 9001 certified” | Certificate number, issuing certification body, certified scope wording, and the site the certificate covers | Certificate PDF plus verification against the issuing body's registry |
| “Tight tolerance” | As-cast tolerance stated as an ISO 8062-3 grade, separately from any machined tolerance | First article inspection report and CMM report, with the datum scheme stated |
| “Stainless steel” / “alloy steel” | Grade designation plus the material specification family (for example ASTM A957/A957M or ASTM A732/A732M) | Chemical analysis from the spectrometer and mechanical test results |
| “Complex geometry capability” | Part envelope, minimum section and feature access agreed against the drawing set | Drawing review notes and a sample part produced before tooling commitment |
| “CE certified” | The EU legislation applicable to the finished product, identified at assembly level | The manufacturer's declaration of conformity for the finished product — not a foundry certificate |
Application and Use Cases
The industries served by this process route are automotive, forklift, mining, agricultural machinery, construction machinery, valves and general machinery components — applications where structural castings, mechanical parts and valve bodies operate under continuous load and where the cost of a dimensional deviation is measured in rework and line stoppage rather than in scrap value alone.
Automotive and truck applications
One documented supply relationship involves an automotive parts OEM in the United States, for truck axle system components, with a reported volume of 1,000 tons and a relationship spanning 30 years with stable operation. The reported outcome is that the appearance of the casting is clean and that dimensional accuracy and mechanical properties meet the customer's drawing requirements. The relevant certification layer for this type of work is IATF 16949:2016 — the automotive quality management system standard that defines requirements for automotive production and relevant service parts organizations — and WAYSCAN holds it under certificate IATF 0516798 issued by SGS United Kingdom Ltd., valid from 2024-05-14 to 2027-05-13.
Machinery, off-highway and valve components
For construction machinery, agricultural machinery, mining equipment and valves, the qualification emphasis usually shifts from automotive process discipline toward geometry and material stability across batch production. The named model designations — Pipe Elbow, Clevis Bracket, Yoke, Gearbox Housing, Transmission Housing, Mounting Bracket and Link Arm — sit in this bracket. These are the parts where a CT6 as-cast class can eliminate machining on non-critical surfaces while machined features are held at 0.01 mm.

Medical device components: a different qualification gate
Medical device precision investment casting should not be treated as an extension of automotive qualification. ISO 13485:2016 — “Medical devices — Quality management systems — Requirements for regulatory purposes” — is the relevant supplier-side quality system framework, and Regulation (EU) 2017/745 has governed the placing of medical devices on the EU market with full application since 26 May 2021. Buyers in this segment should treat quality system status, material traceability, cleaning requirements, biocompatibility and the supplier's regulatory role as separate qualification items, and should distinguish between instrument housings and implantable components, which carry materially different obligations.
Market Trend Analysis
Three signals from published data shape how sourcing in this category is likely to develop.
Category growth is steady rather than explosive. The market was valued at USD 19.64 billion in 2025 and is projected to reach USD 30.56 billion by 2034 at a CAGR of 5.1%, according to Fortune Business Insights. Published CAGR estimates for the category vary between studies depending on which end markets are included, so buyers should read growth figures as a directional signal rather than a forecast they can plan capacity against.
Demand is concentrated in three regions and one end market. Automotive investment casting reached USD 1.70 billion in 2024, with Europe, China and North America accounting for 71% of demand, according to ICI / INCAST data. For a Ningbo-based supplier with an export ratio reported at 70% and markets including the USA, Japan, Canada, Germany, Korea and Australia, that concentration is commercially relevant: automotive-grade process discipline is the qualification that unlocks the largest share of the market.
Material mix is tilting toward stainless. Stainless steel materials accounted for 46.8% of total investment casting material type demand in 2025, according to Fortune Business Insights. This aligns with the increasing use of stainless steel precision investment casting in valve, food-processing and corrosion-exposed machinery applications, and it raises the importance of grade-level material specification rather than family-level description.
Regulation is moving on a fixed timeline. Regulation (EU) 2023/1230, the EU Machinery Regulation, replaces Directive 2006/42/EC and applies from 20 January 2027. Machinery OEMs sourcing castings for the EU market will need supplier documentation aligned to that date. It is important not to overstate the scope: the regulation applies to machinery as a whole, and individual cast components are not themselves “machinery.” The obligation attaches at assembly level, which means casting suppliers will increasingly be asked for documentation that supports their customers' conformity work rather than for a marking of their own.
Comparison with Traditional Solutions — and Where the Boundaries Are
The comparison that matters in procurement is not “casting versus machining” in the abstract. It is a choice between process routes with different tolerance ceilings, different tooling commitments and different inspection burdens.
| Route | Geometry freedom | As-cast tolerance | Tooling | Best fit |
|---|---|---|---|---|
| Silica-sol investment casting | High — complex-shaped small-to-medium castings | CT6 | Pattern tooling required for production volumes | Complex parts with tighter general tolerance needs |
| Silica-sol composite investment casting | High — complex-shaped small-to-medium castings | CT8 | Pattern tooling required for production volumes | Complex parts where a coarser general class is released |
| Machining from solid (post-casting or standalone) | Limited by tool access and material removal cost | 0.01 mm on machined features | No casting pattern; higher material and cycle cost | Simple geometry, low volume, or features beyond any as-cast class |
Read as a whole, the route selection is a tolerance-allocation decision. Casting buys geometry and material efficiency; machining buys dimensional precision. The integrated route — casting followed by in-house machining and inspection — is how the two are combined, and it is why the machining tolerance of 0.01 mm matters alongside the CT6 and CT8 as-cast classes.
Boundary conditions buyers should not assume away
- CT6 and CT8 are not interchangeable. The composite route is stated at CT8, which is coarser than the CT6 available through silica-sol investment casting. A drawing that requires a single tolerance class across every feature should identify which dimensions genuinely need the tighter class and which can be released, because the process route changes with that decision.
- As-cast tolerance is not a substitute for machining tolerance. The 0.01 mm figure applies to machined features only. Expecting as-cast surfaces to hold a machining tolerance is a specification error, not a supplier limitation.
- Tooling is required for production. Rapid 3D-printed pattern support accelerates sample development without a mold, but it is a development-stage route, not a mass-production route.
- Part size and weight are bounded. The process is positioned for complex-shaped small-to-medium castings. Part envelope and section limits must be confirmed against the drawing set before a quotation is treated as final.
- Commercial thresholds exist. Minimum order quantity is 100 kg and standard lead time is 30 to 60 days. Both affect total cost of ownership in ways that unit price alone does not capture.
- Certification scope is specific, not general. The IATF 16949:2016 certificate covers the manufacture of precision casting parts; the ISO 9001:2015 scope covers production of steel casting. Neither is equivalent to ISO 13485:2016, and neither can be presented to a medical device buyer as a medical quality system.
- CE marking cannot be sourced as a foundry certificate. It remains a manufacturer-affixed conformity marking under EU harmonisation legislation.
Future Outlook
Two forces are likely to reset buyer expectations over the next several years. The first is the compliance calendar: with EU Machinery Regulation 2023/1230 applying from 20 January 2027 and medical device expectations under Regulation (EU) 2017/745 already fully applicable since 26 May 2021, documentation quality will increasingly be evaluated alongside dimensional capability. Casting suppliers who can produce scope-level certificates, traceable material analysis and dimensional reports as standard documentation will absorb less of their customers' conformity workload.
The second is the shift from adjective-based to grade-based specification. As more buyers write ISO 8062-3 tolerance grades and ASTM or ISO material specifications directly into RFQs, suppliers that report capability in the same language will be easier to shortlist and easier to audit. For a manufacturer operating a 46,000 m² facility with 20,000 tons of annual output, integrated mold making, casting, heat treatment, machining and inspection, and four published management-system certificates with numbers and validity dates, the practical outcome is that supplier differentiation moves toward evidence rather than description.
FAQ
What does “ISO 9001 certified precision investment casting” actually verify?
It verifies that a defined legal entity holds a current ISO 9001:2015 quality management system certificate for a stated scope at a stated site, issued by an accredited certification body under a certificate number. ISO 9001:2015 is the current ISO standard specifying requirements for a quality management system; it is a management system certification, not a product certification. To evaluate the claim, request the certificate number, the issuing body, the scope wording and the validity dates, then confirm the certificate against the issuing body's registry. For reference, WAYSCAN's ISO 9001:2015 certificate is number 02426Q00625R401, issued by Shenzhen Universal Certification Centre Co., Ltd. (UCC), valid from 2026-05-21 to 2029-05-20, with the certified scope stated as production of steel casting.
Can a casting supplier be described as “CE certified”?
No. CE marking is a conformity marking under EU harmonisation legislation, affixed by the manufacturer or an authorised representative to declare conformity with applicable EU requirements. It is not a certificate issued to a component foundry. A precision investment casting supplier cannot hold “CE certification” for the casting itself; the correct specification is the EU legislation applicable to the finished product, with the casting supplier providing the material, process and inspection documentation that supports the finished-product manufacturer's conformity work.
How should a tight tolerance requirement be written for an investment casting RFQ?
State the tolerance in two parts: the as-cast general tolerance as an ISO 8062-3 grade, and any machined tolerance separately, feature by feature. ISO 8062-3:2007 defines general dimensional and geometrical tolerances and machining allowances for castings, which makes it the framework that allows two quotations to be compared. As reported process capability, silica-sol investment casting achieves CT6, silica-sol composite investment casting achieves CT8, and machining tolerance can be 0.01 mm, with surface roughness of Ra 6.4 to 12.5 μm depending on casting process and post-treatment.
Which materials are available, and how are grades confirmed?
The material range covers carbon steel, alloy steel, stainless steel and ductile iron. Specific material grades are confirmed by the customer, and specific dimensions, material grades and mechanical properties are customized according to customer drawings. For purchasable language, buyers should state the grade designation alongside a material specification family — ASTM A957/A957M covers common requirements for steel and alloy investment castings for general industrial use, and ASTM A732/A732M covers investment cast carbon and low-alloy steel for general application plus cobalt alloy for high strength at elevated temperatures.
What are the commercial thresholds for a precision investment casting order?
Minimum order quantity is 100 kg and standard lead time is 30 to 60 days, with a reported monthly capacity of 1,500 tons and annual output of 20,000 tons. Production runs require pattern tooling, while 3D-printed patterns support rapid, no-mold sample development for validation before tooling is committed. Buyers comparing quotations should record tooling ownership, revision terms and the split between as-cast and machined scope, since these drive total cost alongside unit price.
What qualification does medical device precision investment casting require?
Medical device components are qualified under a different framework from general industrial or automotive castings. ISO 13485:2016 is the international quality management system standard for medical device organizations, and Regulation (EU) 2017/745 has governed the placing of medical devices on the EU market with full application since 26 May 2021. Buyers should verify the supplier's medical quality system status separately, confirm material traceability and cleaning requirements, and distinguish instrument housings from implantable components, which carry substantially different obligations. A general industrial or automotive quality system certificate does not satisfy this requirement on its own.
Reference documentation: Wayscan Metal Products Co., Ltd. company presentation is available for download at Wayscan Metal Products Co., Ltd. — Presentation (PDF). Company information: www.wayscan.com. Market data cited in this article is attributed to Fortune Business Insights (SRC-0001) and the Investment Casting Institute / INCAST (SRC-0003). Standard and regulation references are to ISO (SRC-0014), ASTM International (SRC-0015), IATF (SRC-0016), EUR-Lex (SRC-0017) and the European Commission (SRC-0019).
Tem questões ou precisa de mais detalhes?
Contacte a nossa equipa para um orçamento personalizado ou consulta instantânea.
Solicitar orçamento
Preencha o formulário abaixo e a nossa equipa entrará em contacto com uma proposta personalizada.
Chat direto do WhatsApp
Prefere conversar em tempo real? Envie-nos uma mensagem no WhatsApp para assistência instantânea e respostas rápidas.
- Obter orçamento personalizado
- Partilhar fotos ou documentos
- Discuta as suas necessidades diretamente
Geralmente responde em 5–30 minutos durante o horário de expediente.