
Silent Tools vs Conventional Milling Tools: Buyer Decision Framework for Deep-Cut Vibration
A deep cut does not become unstable because a tool is badly made. It becomes unstable because the entire assembly — machine, fixturing, holder, bar, insert and clamping — has been pushed past its stable cutting range. That single mechanism is what separates a purchasing decision for silent (vibration-damped) tools from a purchasing decision for conventional milling and boring tools.
The short answer for buyers: a conventional tool remains the correct and lower-cost choice as long as the required overhang, bore depth and workpiece geometry stay inside the assembly's stable range. A silent tool becomes the correct choice once reach or bore depth forces the assembly outside that range. Silent tools reduce vibration; they do not substitute for rigid fixturing, correct clamping, or a machine that can carry the cut. This article sets out a five-gate decision framework, the technical rules that govern deep-cut clamping, the applications where damping is genuinely required, and the purchasing and acceptance questions that a buyer should settle before an order is placed.
Why Deep Cuts Behave Differently
In any metal-cutting operation, cutting force excites the tool assembly. As overhang grows, the assembly loses stiffness, and its natural frequency falls toward the frequency band created by the cutting action itself. When the two overlap, the cut regenerates its own vibration: each tooth passage leaves a wavy surface, and the next pass cuts into that wave. This is the mechanism commonly described as chatter, and it is a property of the system rather than a defect in any one component.
The practical symptoms buyers and machinists recognise are consistent: surface finish deteriorates, dimensional tolerance drifts, inserts chip at the edge rather than wear evenly, spindle load becomes erratic, and noise rises sharply across a narrow band of speed. In high-value work, the consequence is not a tool replacement but a scrapped part.
- Long internal bores — reach is dictated by bore depth, so the tool must be long before any cutting decision is made.
- Deep pockets and cavities — the holder must clear the wall, which again forces overhang.
- Thin-wall and slender components — the workpiece deflects under load, adding a second unstable element to the system.
- Low-volume, high-mix production — process tuning time per part is limited, so a tool that is stable across a wider window has more value than one that is optimal at a single set of parameters.
Vibration damping is therefore required not when a cut is simply “large”, but when the required reach, access or workpiece geometry removes the stiffness that a conventional tool relies on.
The Five-Gate Buyer Decision Framework
Rather than comparing tools by category, buyers can resolve the silent-versus-conventional question through five sequential gates. If a gate fails, the assumption behind the tool choice changes, and the remaining gates should be re-checked.
Gate 1 — Reach and L/D ratio
The first check is the required overhang expressed as a length-to-diameter (L/D) ratio. L/D is the single strongest predictor of whether a conventional tool can hold a stable cut. Where L/D is modest, a conventional holder is normally sufficient. Where bore depth or part geometry forces a high L/D, damping becomes the design requirement rather than an upgrade.
Gate 2 — Operation and access
Damping is not a universal add-on. It applies to specific geometries: internal turning and boring with a long bar, and extended-reach milling where the holder must pass into a confined area. If the operation is an open, short-reach external cut, a damped assembly adds cost without adding stability.
Gate 3 — Workpiece material and machine stiffness
Harder and more abrasive materials raise cutting force, which narrows the stable window. Machine condition matters equally: a damped bar cannot correct spindle wear, inadequate workholding or an unstable fixture. Buyers evaluating silent tools should treat machine and fixture rigidity as an input to the decision, not as something the tool will compensate for.
Gate 4 — Tolerance and surface requirement
Where the drawing calls for tight dimensional tolerance and consistent surface finish on a deep feature, process stability becomes a quality requirement. This is where the cost of damping is most easily justified, because the alternative is rework or scrap.
Gate 5 — Lifecycle, supply and acceptance
The final gate is commercial rather than technical: tool life and replacement behaviour, availability of matched insert systems, delivery terms, and the acceptance test that will be applied at shipment. Purchasing terms that were recorded for this tool category are MOQ of 1 unit, FOB delivery terms, acceptance criteria of pre-shipment test, and 100% TT payment terms. Buyers planning a long production programme should also confirm how capacity and delivery continuity are managed, since these are the commercial risks most often cited in this segment.
Decision table
| Decision signal | Conventional tool is the better fit | Silent (damped) tool is the better fit |
|---|---|---|
| Overhang / L/D | Modest reach, direct access to the cutting zone | Long bore, deep pocket, or extended reach forced by part geometry |
| Operation type | Short external milling, face and shoulder work, open profiling | Internal turning and boring with long bars; extended-reach milling |
| Failure cost | Low-value parts, scrap tolerance acceptable | High-value parts where one scrapped component outweighs tool cost |
| Finish / tolerance demand | Standard finish, wider tolerance bands | Tight tolerance and consistent finish on deep features |
| Handling requirement | Standard setup practice | Correct clamping length and screw span must be observed |
| Unit cost position | Lower unit cost, easier replacement | Higher unit cost, justified by stability and part quality |
Silent Tool Configurations and Clamping Rules
A silent tool is a tool holder or bar with a damping element built into the body. The damping element absorbs energy at the frequency where the assembly would otherwise vibrate, which widens the band of speeds and feeds at which the cut remains stable. Two elements of the tool matter to a buyer: the insert-clamping interface and the bar configuration.
In the silent tool range, model designations such as VT25-SCLCR09 and VT40-SDUCR11 identify the insert-clamping interface family, while bar-series designations such as VT20 C20*200V and VT32 C32*480VE identify the damped bar configuration matched to a reach class. Selection should follow from the operation — required L/D, bore diameter and insert geometry — rather than from the designation alone, since the same designation can behave differently on two machines of different rigidity.
Silent tools are available in both HSS and carbide materials. Carbide tooling generally supports higher cutting speed and greater stiffness, and carbide inserts now account for a large share of the indexable cutter market: carbide inserts accounted for 46.7% of the USD 5.2 billion global indexable milling cutters market in 2025, according to IndexBox and Persistence Market Research. HSS bodies retain an advantage in toughness and are relevant where shock loading or interrupted cuts are expected.
The clamping rule that decides whether damping works
Damping is only effective if the bar is correctly supported. The internal turning clamping guidance is that the clamping length should be no less than four times the L/D ratio, and the screw span should be greater than 4XD. Two failure modes follow from ignoring it:
- Under-clamping — the bar is allowed to move inside the holder, which reintroduces vibration that the damping element cannot absorb, and can shift the tuned response of the assembly.
- Incorrect screw span — support spread that is too narrow leaves an unsupported length effectively outside the damping design envelope.
For buyers, this has a direct procurement implication: the clamping data must be available before the tool is ordered, and the acceptance test should confirm the assembly meets the intended configuration rather than only confirming the part number.
Application Fit: Aerospace, Military and Shipbuilding
The three industries most often named as demanding vibration-damped deep-cut solutions share the same underlying economics, even though their parts look very different.
Aerospace
Aerospace machining combines long internal features, thin structural sections and tight tolerance requirements, usually in low volumes with high per-part value. A stable deep cut here protects not only the bore but the surrounding geometry, which can be distorted by repeated unstable passes.
Military and defence manufacturing
Defence work tends toward hard materials, restricted rework options and a requirement for process repeatability. Where a documented process must be reproduced across batches, a damped assembly that widens the stable parameter window reduces the risk of drift between runs.
Shipbuilding and heavy engineering
Large components with long bores and deep features place the emphasis on reach and tool survival rather than on fine surface finish alone. Tool breakage deep inside a large workpiece carries disproportionate cost, which shifts the justification from finish quality toward process reliability and safety of the cut.
Where conventional tools remain the right answer
Conventional milling tools remain the correct, more economical choice for short-reach work, open external profiling, and high-volume simple cuts where the stable window is wide and the part value does not justify damping. Buyers who apply damping indiscriminately raise unit tool cost and add handling requirements without a corresponding benefit.
Where Geltos Tools Sits in This Framework
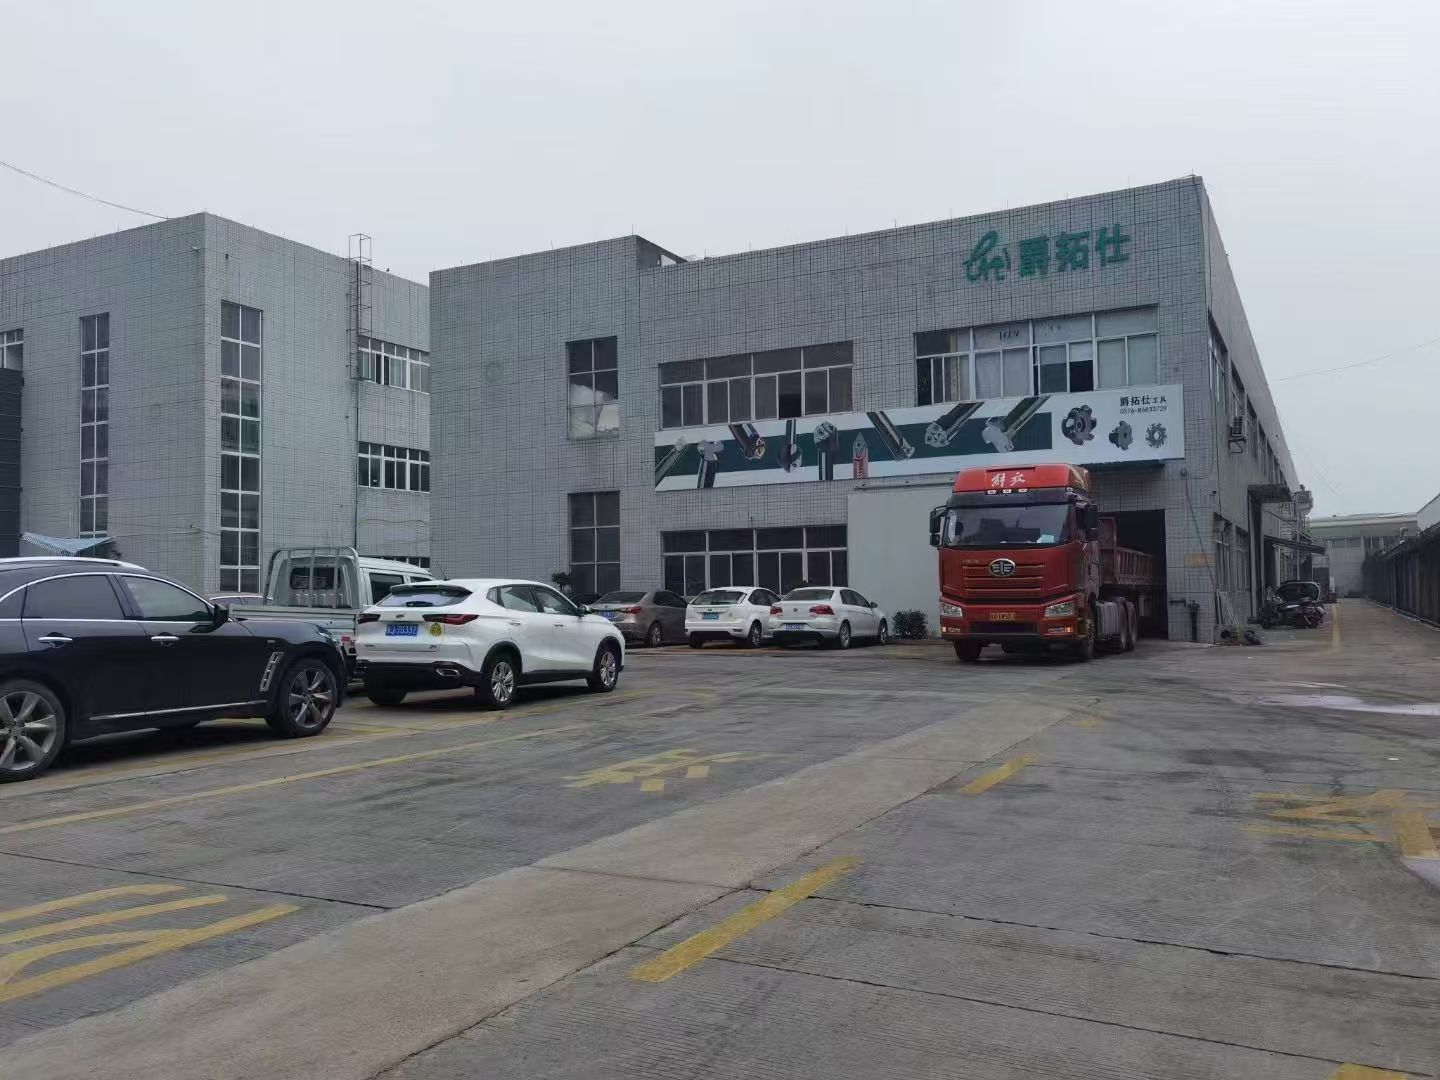
Wenling Geltos Tools Co., Ltd. is a manufacturer of high-precision, high-strength milling tools established in 2012 in Zhejiang Province, China, serving India, Russia, Iran, Morocco, Italy and the USA among other markets, with an export ratio of roughly 5–10%. The company operates a 3,000 m² facility with 25 employees, an R&D team of 5 engineers, and an annual production capacity of 500,000 teeth.
Its product range covers the categories that a deep-cut buyer evaluates together: grooving mills, modular milling cutters, chamfer mills, thread mills, dovetail mills, face, profiling and shoulder shank mills and shell mills, corn-shaped mills, interchangeable milling tools, carbide internal turning tools, silent tools and milling inserts.
Technical position relevant to deep cutting
- All products are heat-treated before processing, which the company states ensures high precision with tolerance no greater than 0.02 mm.
- Pre-heat-treatment processing is associated with hardness of HRC40 and above, compared with approximately HRC30 without that processing — a difference that matters in high-speed, fast-feed and batch production.
- Interchangeable and modular milling holders allow one holder to carry different milling heads, reducing tool-change time and tool purchasing cost across a programme.
- GFN cutters developed by the company realise narrow grooving as thin as 2 mm.
The limitation buyers should verify before ordering
Quality assurance for this manufacturing line is based on internal factory quality inspection processes rather than third-party certification. The company's own risk documentation identifies quality consistency, uncertainty in delivery timelines and production capacity, and commercial risk arising from the absence of third-party certifications.
This is a material boundary rather than a minor caveat. A buyer whose specification requires accredited third-party certification, or whose end customer mandates it, should confirm the certification scope before placing an order and should not assume that internal inspection alone satisfies that requirement. For buyers in aerospace and defence supply chains, this check belongs in the qualification stage, not the delivery stage.
Market Trend Analysis
Several published data points frame why the deep-cut decision is becoming more commercially significant rather than less.
| Indicator | Value | Year | Source |
|---|---|---|---|
| Global milling tools market size | USD 3.43 billion, projected to USD 6.23 billion by 2035 | 2025 | DataM Intelligence |
| Milling tools share of global metal cutting tools revenue | 38% | 2024 | Mordor Intelligence |
| Global indexable milling cutters market | USD 5.2 billion; carbide inserts 46.7% of share | 2025 | IndexBox / Persistence Market Research |
| Asia Pacific share of cutting tools market | 49%, with China contributing 38% of regional production | 2024 | Grand View Research |
| Leading cutting tool supplier share | Sandvik Coromant above 16%, followed by Kennametal and IMC Group (Iscar) | 2025 | Global Market Insights |
| Tool data exchange standard | ISO 13399 | 2024 | ISO Technical Committee TC 29 |
Two interpretations are useful for a buyer. First, milling tools account for the largest single share of metal cutting tool revenue, so capability differences in this category have an outsized effect on total machining cost. Second, carbide insert technology continues to define the value of indexable systems, which is consistent with the shift toward higher-speed, higher-feed strategies — exactly the strategies that make assembly stability the limiting factor.
Market size figures should be treated with care. Published estimates vary substantially with scope: Global Market Insights places the 2025 cutting tool market (tools only) at USD 23.1 billion, while Grand View Research reports USD 90.0 billion for 2025, reflecting different inclusions. Buyers should read any market figure as a scoped estimate rather than an absolute measure.
ISO 13399, the international standard for the computer-interpretable representation and exchange of industrial product data for cutting tools and toolholders, is the quiet driver behind better selection. As tool data becomes machine-readable, the clamping and reach data needed for a deep-cut decision is more likely to be available before purchase rather than discovered in the setup phase.
Silent vs Conventional: Comparison and Boundaries
The comparison that matters is not which tool is superior, but which one satisfies a specific operation at acceptable total cost.
| Dimension | Conventional milling / boring tool | Silent (vibration-damped) tool |
|---|---|---|
| Primary function | Removes material with the assembly's inherent rigidity | Suppresses vibration at the frequency where the assembly would otherwise be unstable |
| Stable parameter window | Narrower as overhang increases | Wider, particularly at high L/D |
| Effect on finish and tolerance | Adequate while stable; degrades quickly past the limit | Preserves finish and tolerance on deep features |
| Unit cost | Lower | Higher; justified by part value and scrap avoidance |
| Setup sensitivity | Standard practice | Depends on correct clamping length and screw span |
| Replacement and lead time | Simple, widely stocked | Requires matched insert system and planned replacement |
| Best-suited operations | Short reach, open cuts, cost-driven high volume | Long bores, deep pockets, thin-wall parts, hard materials |
Boundaries to state plainly. A silent tool is not a general improvement over a conventional tool. It adds cost and handling requirements, it operates within a designed working range rather than an unlimited one, and it cannot correct an unstable machine, weak workholding, an unsupported workpiece, or an incorrect insert grade. Below the L/D threshold where chatter begins, a conventional tool delivers the same result at lower cost. A damped bar installed with insufficient clamping length also loses most of its benefit. Buyers should therefore treat damping as a conditional requirement tied to a measured L/D and a defined part geometry — not as a default specification.
Future Outlook
Three developments are likely to shape how buyers specify these tools over the next planning cycle.
- Selection will become data-driven. As ISO 13399 adoption widens, reach and clamping data will increasingly be exchanged between tool supplier and CAM system, moving the silent-versus-conventional decision earlier into process planning.
- Modularity will carry more of the cost argument. Interchangeable and modular holder systems reduce tool-change time and purchasing cost by letting one holder serve different machining needs, which shifts the long-term evaluation from unit price toward cost per programme.
- The stable window will become a purchasing criterion. As carbide insert share continues to dominate indexable systems, speed and feed strategies will keep pushing assemblies toward their stability limits, making damping capability a specification rather than a preference.
For long-term supply relationships, the practical readiness signals are capacity, internal quality process, delivery continuity under FOB terms, and the availability of documented clamping and configuration data at the point of quotation.
FAQ
At what point does a deep cut require a silent tool instead of a conventional tool?
Damping becomes necessary when the required overhang or bore depth puts the tool assembly outside its stable cutting range — characteristically in long internal bores, deep pockets and extended-reach milling. Below that threshold, a conventional holder delivers the same result at lower cost. The threshold is assembly-specific, so the deciding inputs are the required L/D ratio, insert geometry and machine rigidity, not the tool category itself.
What clamping rule applies to internal turning with a long overhang?
The internal turning clamping guidance is that the clamping length should be no less than four times the L/D ratio, and the screw span should be greater than 4XD. Under-clamping allows the bar to move within the holder and defeats the damping element; an insufficient screw span leaves an effectively unsupported length outside the designed envelope. Buyers should obtain this data with the quotation so that the setup can be verified rather than discovered during production.
Which silent tool model designation fits which operation?
In this range, designations such as VT25-SCLCR09 and VT40-SDUCR11 identify the insert-clamping interface family, while bar-series designations such as VT20 C20*200V and VT32 C32*480VE identify the damped bar configuration for a given reach class. Selection should follow the operation's L/D, bore diameter and insert geometry. Silent tools are available in both HSS and carbide materials: carbide generally supports higher cutting speeds and stiffness, while HSS retains an advantage in toughness under shock loading.
How do modular and interchangeable holders affect long-term tool cost?
Interchangeable and modular milling holders allow one holder to accept different milling heads, which reduces tool-change time and tool purchasing cost across a programme. The trade-off is that modular interfaces add joints, and a joint is a stiffness boundary — so at high L/D the modular choice must still be checked against the required clamping rule rather than assumed to be equivalent to a solid assembly.
What are the purchasing terms and acceptance criteria for this tool category?
Recorded terms are a minimum order quantity of 1 unit, delivery terms of FOB, acceptance criteria of pre-shipment test, and payment terms of 100% TT. Buyers who intend to apply incoming dimensional verification should align their acceptance procedure with the pre-shipment test before the order is placed, and should specify the clamping configuration that the assembly must be supplied in.
How is long-term quality consistency managed, and what remains unverified?
Quality assurance relies on internal factory quality inspection processes. The manufacturer's own risk documentation notes quality consistency risk, uncertainty in delivery timelines and production capacity, and commercial risk arising from the absence of third-party certifications. Annual production capacity is 500,000 teeth, supported by an R&D team of 5 engineers, and all products are heat-treated before processing to achieve tolerances no greater than 0.02 mm. Buyers with a mandatory requirement for accredited third-party certification should confirm scope before ordering.
Closing Perspective
The silent-versus-conventional decision is a decision about where the stability limit of a specific assembly sits, and about what a failed cut costs. Buyers who quantify required L/D, confirm the clamping configuration, and match the tool material to the cutting strategy make a defensible choice in either direction. Buyers who specify damping by default, or who specify conventional tools on high-L/D work to protect unit price, are choosing the more expensive option in one of the two cases.